Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
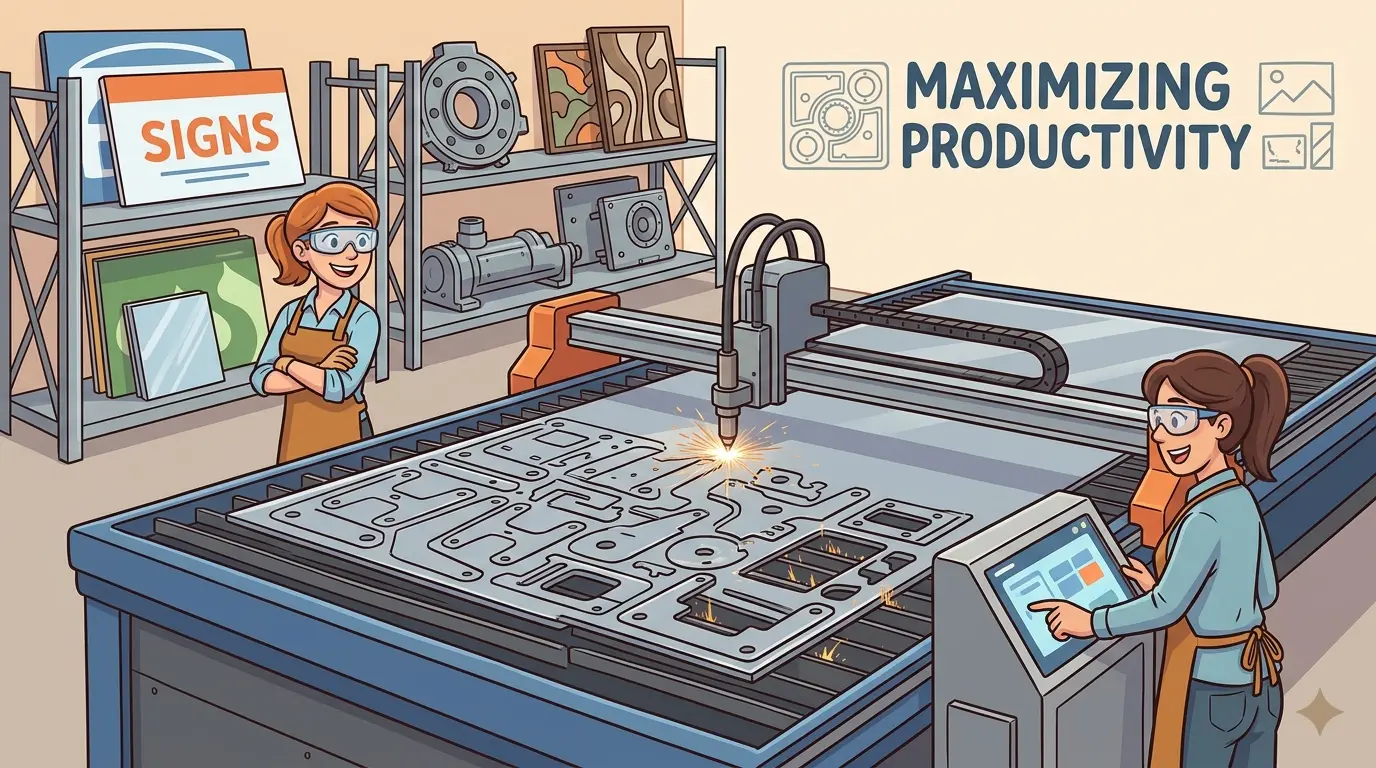
Moving from a 4×8 to a 5×10 plasma table is not a matter of raw capacity but of eliminating recurring production waste. If your operators routinely pre-cut plate to fit the bed, split nests that should stay intact, or reposition long parts mid-cut, the smaller format is dictating your layout logic and burning labor before the torch fires. The upgrade only pays when your normal plate mix repeatedly demands the larger footprint—not when oversized jobs appear occasionally. Before comparing specs, audit your job history and material path to confirm the larger bed simplifies loading, nesting, and unload rhythm across the entire workflow.
When a 5×10 Plasma Table Stops Being a Luxury and Starts Paying Rent
The decision to move up to a 5×10 plasma table is rarely about wanting more steel. It is about eliminating a specific, recurring set of compromises that a smaller bed forces on the shop floor. If your current cutting process is smooth, your nests fit well, and operators are not constantly fighting the table size, a larger format will simply add footprint and handling burden without a return.
However, when the 4×8 or smaller bed starts dictating how you stage material, how you lay out parts, and how much time you spend moving plate, the larger cutting area becomes a production tool rather than an expensive indulgence. The key is identifying whether your shop has crossed that threshold.
The Threshold Is Defined by Repeated Workarounds, Not Occasional Inconvenience
Shops typically justify a 5×10 plasma table when the current route forces the same operational workarounds on a regular basis. Look for these specific patterns in your daily routine:
- Pre-cutting plate to fit the table. If you are shearing or using a handheld torch to break down a 5×10 sheet into pieces that fit a smaller bed, you are adding labor and losing nesting flexibility before the CNC process even starts.
- Splitting nests that should stay intact. When a job with long parts or a high part count requires multiple setups because the bed cannot hold the full layout, you are paying for extra pierces, extra torch travel, and extra handling between runs.
- Repositioning long parts mid-job. If operators have to stop the cut, move a part, and re-fire the torch to finish a single component, you are introducing alignment risk and cycle time penalties.
- Losing plate efficiency because the table sets the layout rules. When your nesting software is constrained by bed dimensions rather than by the actual part geometry and material size, you are leaving usable steel on the table—literally.
- Burning operator time on plate movement. If the crew spends more time staging, loading, and shuffling material than they do managing the cut, the bottleneck is material flow, not torch speed.
The operative word here is repeated. One difficult week with an oversized job does not justify a permanent larger-format cell. But if these compromises appear in the normal weekly schedule—if they are part of how the shop routinely operates—the bed-size problem is real and measurable.
Start with Plate History, Not Growth Anxiety
Before you talk to a sales rep or start comparing machine specs, pull your job history and review the actual plate usage over the last several months. Ask specific questions:
- How often did you run plate that would have genuinely benefited from a 5×10 bed?
- How often did your nesting choices become worse because the current table was too small?
- How many extra material touches did operators create before the torch even fired?
If larger-format work shows up as a regular part of the weekly mix—say, a consistent percentage of jobs that require long parts or high-density nesting—the upgrade case has real evidence behind it. If the larger work is exceptional, you may be about to buy a permanent solution to a temporary problem. The machine will sit idle for most of the week, and you will have paid for floor space and capital that could have gone elsewhere.
A Bigger Table Only Pays If It Simplifies the Full Plate Path
The gain from a 5×10 plasma table is not just more cutting area. The real gain is a cleaner route for the plate from receiving to downstream fabrication. Consider the full material path:
- Plate arrives and gets staged. Does the larger bed allow you to stage full sheets without pre-cutting?
- Plate loads without awkward pre-cutting. Can the operator load a full 5×10 sheet directly, or does the material still need to be broken down for other reasons?
- The nest runs with fewer layout compromises. Are you getting more parts per cycle, longer parts in one piece, and better material utilization?
- Skeletons, parts, and remnants leave in an organized way. Can the operator clear the table without creating a traffic jam in the aisle?
- Downstream fabrication receives the output without new confusion. Does the larger release pattern match what the next process can absorb?
If the bigger bed improves only step three—the cutting itself—the business case is incomplete. The machine will produce more parts per cycle, but if loading and unloading become slower or more awkward, the net throughput gain may be marginal.
Utilization Improves Only When the Plate Mix Really Demands the Space
Large cutting area does not automatically mean higher utilization. In some shops, a 5×10 table simply creates more idle surface because the actual plate mix still fits a smaller format most of the time. The torch spends its day cutting in one corner of the bed, and the rest of the table is dead space.
In other shops, the larger bed removes so much nesting and handling compromise that the torch spends more of the day cutting commercially useful layouts. The difference comes down to the plate mix. If you regularly cut long parts—say, structural members, frame components, or trim pieces over four feet long—the larger bed keeps those parts in one layout. If you cut mostly small, dense parts, a 4×8 bed may already give you all the nesting density you need.
The right question is not “can we occasionally use a 5×10 table?” It is “does our normal plate mix repeatedly lose efficiency because the current table is constraining layout?” If the answer is yes, the larger bed pays. If the answer is no, it does not.
Handling Labor Is Still the Real Cost Driver
Plasma buyers often start with cut speed and amperage, but a larger table usually wins or loses on handling. The torch speed is a fixed variable; the labor around the machine is where the cost accumulates.
Before you commit to a larger format, map the practical sequence in your shop:
- Where raw plate is staged. Is there a dedicated area near the table for incoming material, or does the forklift have to navigate around other equipment?
- How it is loaded. Does the operator use a crane, a forklift, or manual handling? Does the larger bed require a different loading method?
- Where finished parts go. Is there a clear path from the table to the next process—drilling, forming, welding, or assembly?
- Where skeletons and reusable remnants go. Does the shop have a disciplined system for identifying, storing, and retrieving remnants? A larger bed creates larger skeletons, and if those are not managed, they become a safety hazard and a space problem.
- Whether the operator can reset the table for the next job without congestion. Can the crew clear the bed, load new plate, and start the next nest without creating a bottleneck in the aisle?
If those answers stay vague, the shop is usually trying to buy bed area before it has designed the cell around the bed. The machine will arrive, and the crew will figure out the handling on the fly—which is exactly how you end up with a $50,000 machine that runs at 60% utilization.
Unload Rhythm Often Separates Productive Large Tables from Awkward Ones
A larger-format plasma cell does not only ask how the plate is loaded. It also asks how the cell is cleared between jobs. Large nests can release more parts, larger parts, or more awkward scrap patterns in a single run. If the operator cannot clear the table without turning the aisle into temporary storage, the bigger bed may increase output on paper while slowing the job-to-job rhythm that actually determines daily throughput.
Consider the unload sequence carefully. If the table produces a nest with 200 parts, the operator has to sort, stack, and move those parts before the next plate can be loaded. If the table produces a nest with 50 larger parts, the sorting burden is lower, but the parts are heavier and may require a crane or forklift to move. The unload rhythm must match the shop’s material handling capacity.
Nest Integrity Matters More Than Raw Area Alone
One of the strongest arguments for a larger plasma table is that it protects nest integrity. Long parts can stay inside one coherent layout. Plate can remain intact longer. Programming decisions are less likely to be dictated by bed limits.
Each forced split in the nest creates another operational penalty: more handling, more sorting burden, and more chances to lose material logic. When a part is cut in two pieces and welded back together, you add fit-up time, weld time, and the risk of distortion. When a nest is split across two runs, you add a second setup, a second pierce sequence, and more torch travel.
A 5×10 bed eliminates many of those splits. The programming team can design layouts around the actual part geometry and material size, not around the bed limits. That is a real productivity gain, but it only materializes if the shop’s programming software and nesting practices are mature enough to take advantage of the larger format.
Remnant Discipline Matters More on Larger Formats
A 5×10 table can improve material utilization, but only if remnant tracking is disciplined enough to capture that theoretical gain. Without good identification, storage, and reuse habits, the larger table may simply create larger leftovers with weaker control.
When you cut a 4×8 sheet, the remnants are small enough to be managed casually. When you cut a 5×10 sheet, the remnants can be substantial—sometimes large enough to be useful for future jobs. But if those remnants are not marked, stored, and tracked, they become scrap. The shop loses the material value and pays for new plate on the next job.
Programming maturity and remnant handling belong inside the purchase case, not outside it. If the shop does not have a system for managing remnants today, a larger table will not fix that. It will just make the problem bigger.
Downstream Pace Must Be Part of the Decision
The larger bed often releases more parts or larger parts in a single cycle. That only helps if downstream fabrication can keep up. If the next process loses time on part sorting, cleanup, cart availability, or staging, the bigger table may increase work-in-progress instead of profitable flow.
Consider the downstream processes carefully. If the plasma table feeds a press brake, does the brake have the capacity to handle the larger batch sizes? If the table feeds a welding station, does the welder have the space to stage the incoming parts? If the table feeds a paint line, does the line have the throughput to absorb the new release pattern?
If the downstream processes are already at capacity, the larger table will just create a pile of work-in-progress. The parts will sit on carts, taking up floor space and tying up capital, while the bottleneck moves from the plasma table to the next operation.
Site Readiness Is a Production Variable, Not an Installation Detail
A larger plasma table changes what the site must support. More area means more live cell boundary, more plate-movement discipline, and more dependence on clean staging. Before approval, the team should judge whether the current floor layout, material approach paths, unload zones, and scrap-removal habits are ready for larger-format reality.
If they are not, the cost of the table will include fixing a cell design that was never ready for it. You may need to reconfigure the aisle, add a dedicated staging area, or invest in a better material handling system. Those costs belong in the purchase case, not in the installation budget.
A Useful Pressure Test Before Approval
Before you sign the purchase order, ask five direct questions and demand specific answers:
- Which recurring jobs become materially cleaner on 5×10 rather than the current format? Name the jobs. Estimate the time savings per job.
- Which current workaround disappears if the larger bed is installed? If you cannot name a specific workaround that goes away, the upgrade case is weak.
- How will loading and unload stay repeatable every shift? Describe the exact sequence. Identify who does it and what equipment they use.
- How will remnants and finished parts be controlled after the cut? Show the tracking system. Explain how remnants are identified, stored, and retrieved.
- Can downstream fabrication absorb the new release pattern? Confirm that the next processes have the capacity and the staging space to handle larger batch sizes.
If those answers are specific and grounded in the shop’s actual production data, the upgrade case is probably real. If they stay abstract—if the answers are “we will figure it out” or “it should be fine”—the shop may be buying on instinct instead of evidence.
A 5×10 plasma table is a significant capital investment and a significant floor space commitment. It pays off when it removes real, recurring waste from the plate path. It does not pay off just because it is bigger. Run the numbers, map the material flow, and let the evidence decide. If you are in the market for a new cutting cell, reviewing the available plasma cutting equipment alongside your production data is a reasonable next step.