Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
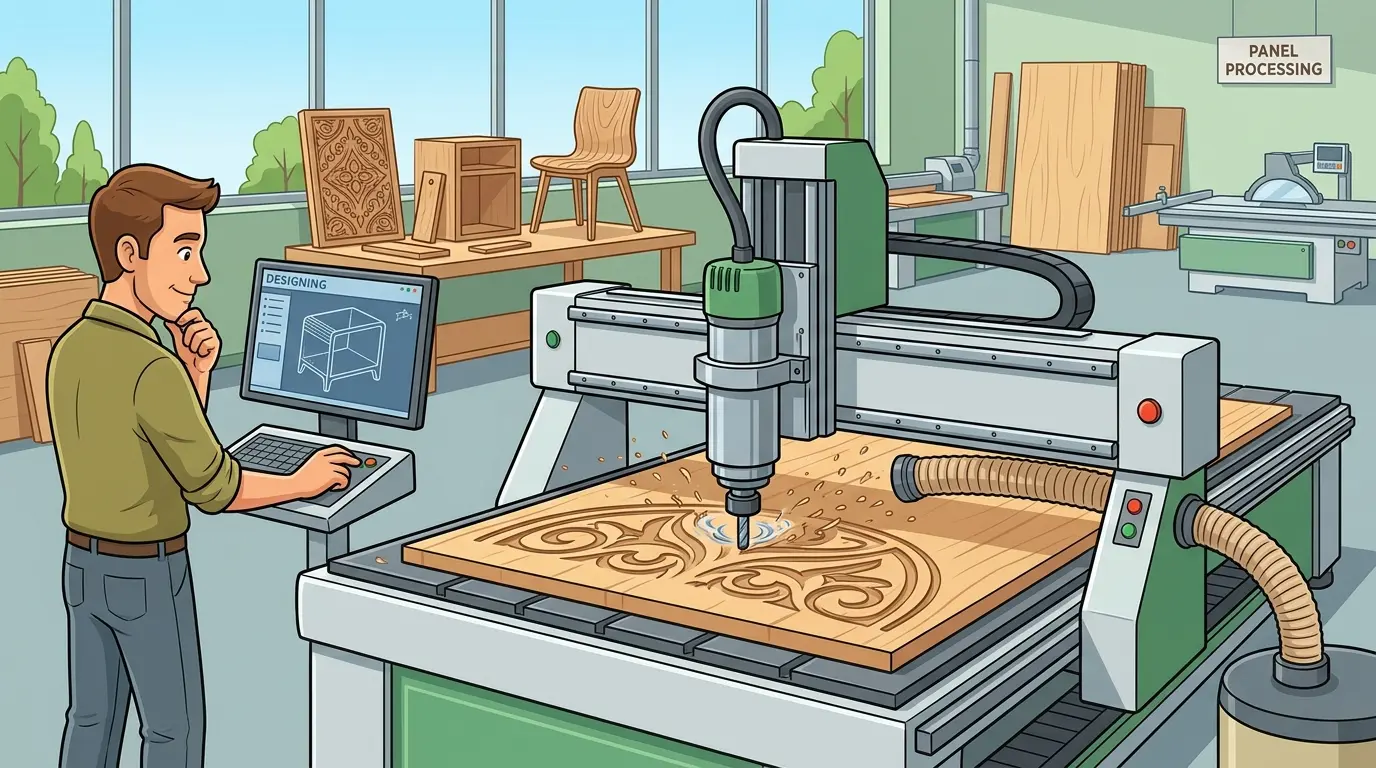
Before you commit budget to a CNC router, you need to know whether your bottleneck is shape complexity or straight-line throughput. This article cuts through the marketing language to show why a router is a coordinate-based cutting platform, not just a fancier panel saw. It explains when the machine earns its keep by compressing handoffs between cutting and drilling, and when it becomes expensive unused capability. If you are weighing nested panel conversion against simple rectangular breakdown, this breakdown helps you match the machine to the actual production pain you are paying to remove.
When a CNC Router Becomes the Right Machine for the Job
A CNC router earns its place in a woodworking plant when the work demands something that saw-centered workflows handle poorly. That is the clearest way to evaluate the machine. A router is not simply a more advanced panel saw. It is a digital cutting and shaping platform that justifies its cost when geometry, drilling integration, and part variation matter more than straight-line sheet throughput.
That distinction matters because many buyers first encounter routers through marketing language rather than production logic. Automation, precision, digital control, and flexibility all sound appealing, but those words do not tell you whether the machine solves a real bottleneck in your specific line. The useful question is not “what is a CNC router?” It is “what kind of woodworking or panel-processing problem does it solve better than the machines we already run?”
Think of a Router as a Coordinate System, Not Just a Cutter
The simplest way to explain a CNC router is that it cuts by coordinates rather than by fences, templates, or manual layout. That sounds obvious, but the consequence is significant. The machine does not just remove material. It keeps shape features, pockets, slots, cutouts, and drilling tied to the same programmed reference. That is what makes it valuable when jobs become more varied or more feature-dense.
In practical terms, the router matters when alignment across operations becomes more important than the act of cutting alone. A panel saw can break down a sheet efficiently. A drill can place holes efficiently. But when contours, slots, reliefs, drilling, and nested shapes need to live together inside one digital reference, the router becomes the more natural platform.
That is why the machine appears so often in cabinet parts, custom furniture components, shaped panels, fixtures, and decorative work. It keeps multiple operations governed by one geometry instead of spreading them across several manual or semi-manual steps where reference drift can occur.
Shape Variation Is Where Router Value Starts to Show
The easiest place to see router value is in jobs that stop being purely rectangular. Curved profiles, pockets, grooves, internal cutouts, irregular furniture shapes, drilled hole patterns, decorative panel features, and mixed part families all push beyond the natural comfort zone of saw-centered production.
Once that happens, the old workflow starts accumulating hidden costs. Operators measure more. Templates appear. Repeated setups multiply. Saw stations need secondary operations. Simple shape changes become process changes instead of just file changes. Those are exactly the conditions that make routers attractive.
At that point, the router is not only cutting material. It is reducing layout labor, consolidating reference control, and lowering the number of times a part has to be re-established by hand. The savings show up in labor hours, rework rates, and the ability to accept new designs without disrupting the whole floor.
Routers Compress Handoffs Between Operations
One useful way to evaluate a router is to track handoffs. How many times does a sheet or part move between stations before it is ready for the next stage of production? How many times does an operator have to re-reference it? How many opportunities exist for location drift between cutting and drilling? How many short tasks survive only because no single machine currently absorbs them together?
The router often becomes valuable precisely because it compresses those handoffs. Instead of one station cutting an outline, another drilling, and another adding shaped or recessed features, the machine can keep multiple operations inside one cycle. That does not mean it replaces every specialized machine in the shop. It means it removes the cost of scattered reference control when the part family is complex enough to justify it.
In production terms, the gain is less about dramatic speed increases and more about fewer chances for small errors to multiply across stations.
Nested Panel Conversion Is a Primary Router Role
In cabinetry, wardrobes, modular furniture, and mixed sheet-based products, the router often earns its place through nesting logic. Full sheets can be digitally converted into many different parts while keeping contours, holes, slots, and cutouts tied to the same programmed geometry. That reduces marking work, simplifies part flow, and usually makes later assembly more consistent.
When this is the real workload, it helps to think in terms of CNC nesting machines rather than a generic woodworking router. The business case is no longer only about cutting shape. It is about digital sheet conversion with fewer manual decisions along the way.
That distinction matters because buyers sometimes describe nested panel work as if it were just “using a router on sheets.” In a real plant, it is more than that. It is a workflow model built around one digital reference moving material from full sheet to identified part set with fewer manual interventions. The software does the part layout, the machine does the cutting and drilling, and the operator’s role shifts from measuring to managing the process.
Custom Woodworking Uses Routers for Different Reasons
Not every router use case is high-volume nesting. In smaller or more flexible shops, the machine often earns its place for a different reason: it makes variation cheaper. A shop building custom furniture, shaped components, carved details, display pieces, or short-run architectural panels may never run large repetitive nests all day. But it may still save significant time by replacing templates, repeated measuring, and multi-step manual shaping.
Here the router is not mainly a throughput machine. It is a variation-control machine. It helps the shop repeat complex geometry without turning every new design into a setup burden. When a customer changes a dimension or requests a different cutout pattern, the operator updates the file rather than building a new template or reconfiguring stops.
That is why two shops can both justify a router while using it in very different ways. One shop may run it as the center of digital sheet conversion. Another may use it as a flexibility station that absorbs design change without throwing the rest of the shop into disorder.
Straight-Panel Throughput Is Not the Router’s Strength
This is where many buyers get misled. If a factory mainly needs straight panel sizing in repeated volumes, a router may not be the most direct answer. In those environments, the shop should compare routing flexibility against the simpler production logic of panel saws, which are built around rectangular throughput rather than shape freedom.
The same caution applies when the real bottleneck is not cutting at all. If edge finishing, boring consistency, or downstream sanding is the true production constraint, adding routing capacity may not solve the problem that matters most.
The router is strongest when the shop is losing money to complexity. It is weaker when the shop is mostly losing money to simple throughput problems that another machine family addresses more directly. A shop that mostly cuts standard cabinet boxes from full sheets may find that a panel saw with a good fence system handles the work faster and at lower cost per part.
The Machine Only Works Well If the Line Around It Is Ready
A router does not repair weak material flow, poor hold-down, unstable tooling, weak extraction, or confused part handling. Shops that treat it like a standalone miracle machine usually end up disappointed. Shops that treat it like one station inside a connected production system usually get more from it.
That matters because the router changes more than cutting. It affects sheet loading, offloading, scrap removal, labeling, queue balance, and the pace of the next process. In woodworking and panel production, the machine’s value is often highest when it is considered together with the surrounding line, not as a one-machine symbol of modernization.
If upstream sheet preparation is chaotic, the router waits. If hold-down is inconsistent, operators hesitate. If part identification and downstream sorting are weak, the gains made at the table get lost immediately after the cut. None of those are abstract concerns. They are the practical reasons one shop gets strong value from a router while another claims the same machine category was overrated.
Cutting and Drilling Stay Married on One Coordinate System
One of the strongest router use cases appears when cutting and drilling need to stay locked to the same coordinate system. Cabinet components, furniture panels, hardware-prep parts, fixture pieces, and many shaped panels benefit from this because location accuracy no longer depends on a part surviving several separate setups without reference drift.
That does not mean routers replace all drilling equipment. Dedicated boring and drilling machines remain valuable when hardware-hole throughput, row drilling, or specialized repetitive boring becomes the main priority. But when drilling belongs inside a more varied cut-shape workflow, the router often wins by preserving one digital relationship across the whole part.
That is why buyers should think less in terms of machine prestige and more in terms of reference integrity. If a cabinet door needs a shaped profile, hinge holes, and handle cutouts, doing all of that in one setup on a router eliminates the cumulative error that comes from moving the part between stations.
Routers Have Clear Boundaries Inside a Full Woodworking Line
A healthy buying decision acknowledges what the router does not do best. It is not the most direct answer for every rectangular breakdown task. It is not the natural replacement for edge finishing. It is not automatically the best machine for every repetitive drilling burden. It is not a shortcut around bad part flow.
In many plants, the router becomes most valuable when it works alongside other machine types rather than pretending to replace them all. Straight sizing may still belong to saw-based equipment. Edge quality may still depend on edgebanders. Surface readiness may still point toward wide belt sanders. The router earns its place by taking on the geometry and integration problems that those other stations do not solve economically.
That is a stronger way to think about automation: not one machine doing everything, but each machine family carrying the work it is structurally best at.
Shops That Benefit Most Share a Common Pattern
The strongest router applications usually reward digital flexibility more than mechanical simplicity. That includes:
- Cabinet and wardrobe parts with cutouts and drilling
- Custom furniture components with frequent dimensional change
- Decorative or shaped panels that exceed saw-friendly geometry
- Sign, display, and fixture parts where contour matters
- Mixed sheet jobs where programming removes repeated setup labor
In all of these, the router earns money by reducing variation pain. The more the shop loses time to manual layout, templates, scattered reference control, and inconsistent repetition, the more likely the router is solving a real problem.
Shops That Benefit Least Also Share a Pattern
Router value becomes less convincing when the work is mostly straight, repeated, and already well served by simpler means. If the line mainly breaks down panels into rectangular parts, or if another more focused machine already handles the true bottleneck efficiently, routing flexibility can become expensive unused capability.
That is why honest job mapping matters more than generic automation language. A router is not automatically a wrong purchase in a simple shop, but it is often over-justified when management confuses digital capability with economic fit.
Ask Which Production Pain You Are Actually Paying to Remove
Before buying, the team should answer a short but important set of questions:
- Are we losing time on shape variation or on straight panel throughput?
- Do cutting and drilling need to remain aligned on one coordinate system?
- Are manual templates, repeated measuring, or mixed product designs slowing output?
- Is the machine meant to support nested panel conversion or occasional custom shaping?
- Will the surrounding flow support the router, or will the machine inherit upstream and downstream disorder?
Those answers usually clarify the router’s role better than a generic product description ever will.
The Router’s Value Is in the Handoffs It Eliminates
That is the most practical way to understand the machine. In woodworking and panel processing, a CNC router is strongest when shape complexity, drilling integration, and frequent variation create more cost than a saw-centered process can absorb efficiently. It is weaker when the factory mostly needs high-speed rectangular breakdown or when the true bottleneck sits elsewhere in the line.
Factories that buy routers for the specific handoffs and reference problems routers actually remove usually get strong results. Factories that buy them as a general symbol of modernization often discover they paid for flexibility they did not really need.