Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
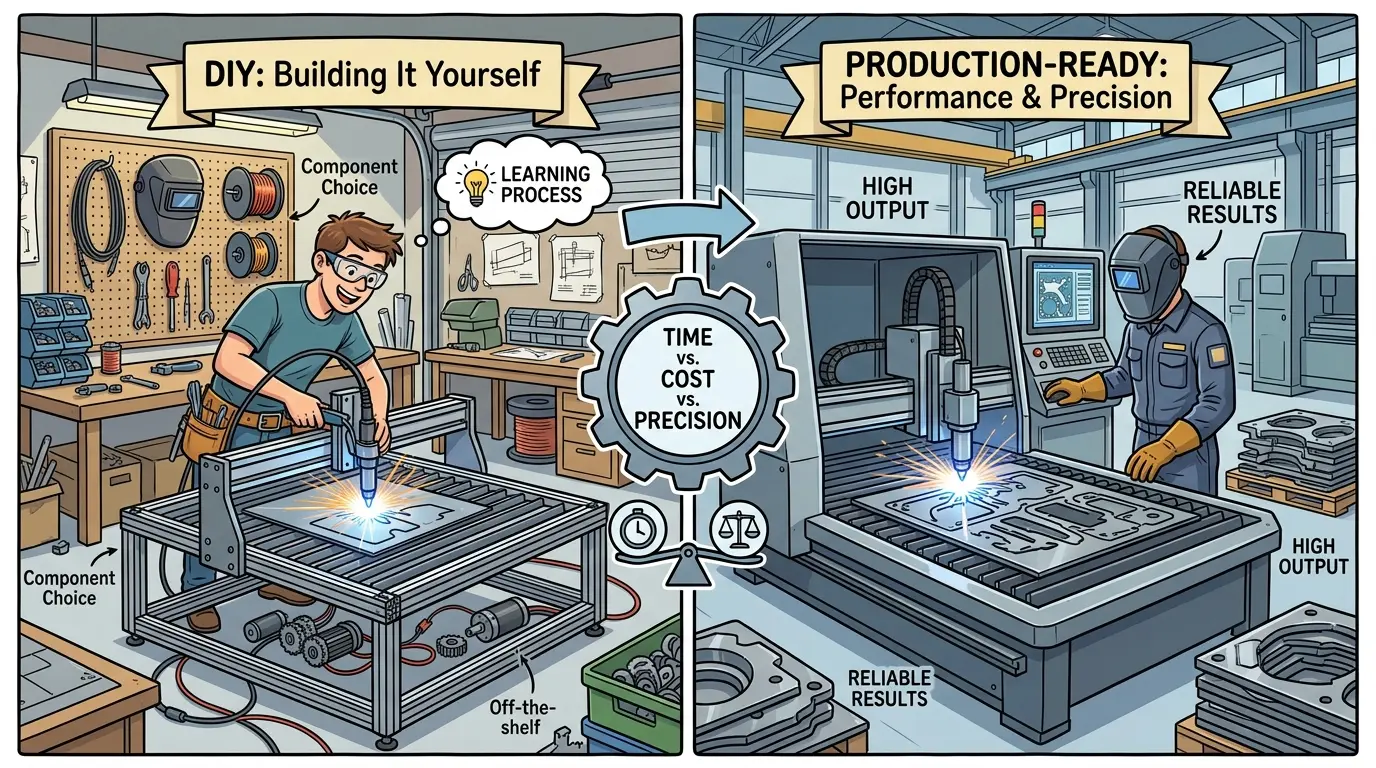
Fabrication shops evaluating CNC plasma cutting often fixate on amperage, travel speed, and drive resolution before confronting the real question: are you buying a production tool or building a project? This article forces that decision into the open by contrasting the operating models behind a DIY table and a production-ready system. The distinction matters because plasma punishes weak integration—torch-height calibration, grounding, air quality, and process tuning—far faster than most builders expect. Before you compare component prices, define whether the machine is the product or the tool, because throughput pressure will expose the difference.
Start With The Operating Model, Not The Torch Specs
When a fabrication shop starts evaluating CNC plasma cutting, the first decision is rarely about amperage, travel speed, or drive resolution. It is about whether you are buying a machine or building a project. The DIY route promises lower apparent entry cost, full control over the design, and the satisfaction of creating the equipment yourself. The production-ready route sells a faster path to stable, repeatable output. Both approaches can cut steel, but they represent fundamentally different operating models. Confusing the two is where most of the disappointment comes from.
This comparison is not about which approach is morally superior or which one produces better parts in absolute terms. It is about matching the machine strategy to the actual business goal. A one-person shop moving from manual fabrication to CNC has different needs than a job shop quoting repeatable parts for local manufacturers. A prototyping shop that values flexibility has different needs than a production floor that runs the same nest three times a week. Before you compare component prices or invoice totals, decide whether the table is the product or the tool.
Define The Return Before You Define The Budget
In a DIY plasma build, the machine is partly the product. Designing the gantry, selecting linear rails, wiring the controllers, tuning the torch height, and debugging the software are part of the reason the project exists. The learning value is real. For some owners, that engineering experience is the primary return on investment. They come away with a deeper understanding of motion control, electrical systems, and plasma physics than any turnkey purchase would provide. That knowledge carries over to every other piece of automated equipment in the shop.
In a production-ready system, the machine is strictly a tool. Its value appears in cut parts, schedule reliability, and reduced uncertainty. The shop does not want to think about the machine architecture; it wants to think about the parts going out the door. The operator should be focused on nesting efficiency, material utilization, and consumable life, not on whether the THC board is communicating properly with the motion controller.
When buyers blur these goals, disappointment follows. A DIY build gets judged by commercial uptime expectations it was never engineered to meet. Conversely, a ready-made system gets rejected because it does not offer the same freedom to tinker. Both are mistakes. The decision needs to be made before the purchase, not after the first production deadline is missed.
Plasma Punishes Weak Integration Faster Than Many Builders Expect
Plasma cutting is unforgiving of casual system design. Motion control matters, but it is only one layer of the stack. Torch-height behavior, consumable condition, grounding quality, cable routing, slat condition, cut-table flatness, air quality, fume handling, and pierce strategy all influence the final cut quality. A gantry that moves accurately is necessary, but it is not sufficient.
Consider what happens on a typical first production run with a newly built DIY table. The operator loads a 4×8 sheet of 10-gauge mild steel, sets the pierce height manually, and starts the first cut. The motion looks smooth. The torch fires. But halfway through the nest, the cut quality drifts. The dross buildup increases. The edge angle becomes inconsistent. The operator stops the machine, checks the torch height, and discovers that the plate has warped slightly from heat input. The THC did not compensate because it was not calibrated for this material thickness and amperage combination.
This is not a motion problem. It is a process problem. A table does not become mature simply because the axis moves correctly. The first time a torch crashes into a warped plate or the cut quality drifts halfway through a nest, the operator discovers that plasma is a process problem, not just a motion problem. Production-ready systems justify part of their cost by arriving with more of these unknowns already resolved or at least narrowed to a manageable set.
What A DIY Build Actually Requires Beyond The Kit
If you are considering the DIY route, be honest about the full scope of work. The kit price is only the beginning. You need to account for the following:
- Mechanical assembly and alignment: The gantry must be square, the rails must be parallel, and the drive system must be tensioned correctly. Misalignment of even a few thousandths of an inch across the table length will show up as inconsistent cut quality and premature wear on racks and pinions.
- Electrical integration: You are wiring the motion controller, the plasma power supply interface, the torch-height controller, the limit switches, the emergency stop circuit, and the grounding system. Each of these has failure modes that are difficult to diagnose when they are all interconnected.
- Software configuration: The CAM software, the post-processor, the motion controller settings, and the THC parameters all need to be configured to work together. A post-processor that outputs incorrect arc voltage values will cause the THC to chase the wrong target.
- Torch-height calibration: This is the most process-critical element. The initial pierce height, the cut height, the pierce delay, and the voltage setpoint all need to be tuned for each material thickness and amperage combination. Getting this wrong results in torch crashes, consumable damage, and inconsistent cut quality.
- Air and gas delivery: Plasma cutting requires clean, dry, adequately pressurized air. If your shop compressor is undersized or your filtration is inadequate, you will see erratic arc behavior and shortened consumable life. This is a common source of frustration for DIY builders who assumed the torch would behave like a handheld plasma cutter.
- Fume and debris management: Plasma cutting generates significant smoke, fine particulate, and hot slag. A downdraft table, water table, or adequate extraction system is not optional for a production environment. It is a safety and compliance issue.
Each of these areas represents hours of work and potential troubleshooting. The question is not whether you can solve these problems. It is whether solving them is the best use of your shop’s time.
DIY Makes Sense When Learning And Customization Are Part Of The Return
There are legitimate reasons to build your own plasma table. You may want to learn machine integration from the ground up. You may enjoy mechanical and electrical problem solving. You may need a very specific format for a narrow job that no off-the-shelf system addresses. You may be transitioning from manual fabrication into CNC and want to understand the process from the inside before committing to a larger investment.
In that context, a DIY table can be highly worthwhile. The hours spent on wiring, tuning, and troubleshooting are not wasted; they are tuition. The knowledge gained carries over to every other piece of automated equipment in the shop. An operator who understands why the THC behaves the way it does is better equipped to diagnose cut quality issues on any plasma system, regardless of brand.
The build becomes a bad fit only when the same machine is expected to behave like a turnkey production asset before it has been engineered or proven at that level. A DIY table can produce excellent parts, but it usually requires more operator attention per cycle and more time to reach consistent quality. If your shop is quoting jobs with tight deadlines, the cost of a mid-day crash or a persistent torch-height issue is not just the cost of the consumable; it is the cost of the missed delivery.
Production-Ready Systems Earn Their Cost By Removing Unknowns
A production-ready plasma system is not valuable merely because it arrives assembled. It is valuable because it removes a large number of unknowns from the route to stable output. Table geometry, motion integration, controller stability, torch interface, cable management, service expectations, and general compatibility are already worked out. The buyer is not trying to prove the machine architecture; they are learning to operate it.
That does not mean every ready-made system is perfect. Plasma still requires operator understanding, consumable management, and process tuning. The operator still needs to know how to set pierce height, choose cut speeds, and manage slat wear. But the system-level burden is lower because the user is not simultaneously debugging the machine and learning the process.
Consider the difference in onboarding. With a production-ready system, the typical path is: install the machine, connect the power and air, load the software, run the manufacturer’s recommended test cuts, and begin producing parts. The manufacturer has already determined the optimal pierce heights, cut speeds, and voltage setpoints for common material thicknesses. The operator’s job is to verify those settings and adjust for specific material lots.
With a DIY build, the onboarding path is: assemble the machine, wire the electronics, configure the software, calibrate the THC, run test cuts, discover that the cut quality is inconsistent, troubleshoot the grounding, adjust the air pressure, recalibrate the THC, run more test cuts, and eventually reach a state where the machine produces acceptable parts. This process can take days, weeks, or months depending on the builder’s experience level and the quality of the components.
Throughput Reveals The Real Difference
In a low-pressure environment, a DIY plasma table can look very capable. Cutting a few parts here and there, with time to adjust between cycles, masks a lot of integration weaknesses. The real difference between DIY and production-ready systems usually shows up under throughput pressure.
Ask yourself these questions about your intended production environment:
- Can the table start reliably day after day, or does the operator need to fiddle with settings before every run?
- Can parts be loaded and cut with a predictable rhythm, or does the operator need to watch every cycle closely?
- Does troubleshooting keep interrupting the schedule, or does the machine run unattended for extended periods?
- Can one operator trust the route enough to move on to the next task, or does the machine demand constant attention?
- What happens when a consumable wears out mid-run? Is the replacement process straightforward, or does it require recalibration?
These questions matter more than the initial purchase price. A machine that requires 30 minutes of setup and adjustment before every run is not a production tool; it is a hobby project that happens to cut steel. A machine that starts reliably, cuts consistently, and alerts the operator only when intervention is needed is a production asset.
Production-ready systems justify themselves when the business needs that repetition to be commercially dependable. If the shop is quoting jobs with tight deadlines, the cost of a mid-day crash or a persistent torch-height issue is not just the cost of the consumable; it is the cost of the missed delivery. It is the cost of the rework. It is the cost of the customer relationship damaged by a late shipment.
Cut Quality And Edge Consistency In Real Production
The difference between DIY and production-ready systems also shows up in cut quality consistency. A well-tuned DIY table can produce excellent cuts. The question is whether it can produce the same quality across an entire nest, across multiple sheets, and across multiple days of operation.
Plasma cut quality is judged by several factors: edge angularity, dross formation, kerf width consistency, and heat-affected zone. In a production environment, the operator needs these factors to remain stable so that downstream processes, such as welding, grinding, or machining, can be planned with confidence.
A production-ready system typically includes features that support this consistency:
- Automatic torch-height control with arc voltage feedback: This maintains a consistent torch-to-work distance even when the plate warps or the slats wear unevenly.
- Pierce height management: The system raises the torch to a safe pierce height, fires, waits for the pierce to complete, and then lowers to cut height. This reduces torch crashes and consumable damage.
- Cut speed monitoring: The controller can detect when the torch is cutting too fast or too slow and adjust accordingly, or alert the operator.
- Consumable life tracking: Some systems track arc hours and alert the operator when consumables are due for replacement, reducing the risk of mid-run failures.
A DIY system can replicate some of these features with aftermarket components, but the integration quality varies. A THC that responds too slowly or too aggressively can cause more problems than it solves. A THC that is not properly tuned for the specific plasma power supply can cause erratic torch behavior.
Safety, Fume Management, And Maintenance Are Core Scope
Plasma systems are not just motion platforms. They bring sparks, fumes, heat, cut debris, grounding concerns, slat maintenance, power considerations, and often water-table or extraction decisions. These are not side tasks; they are core scope.
DIY builders can absolutely solve these problems well, but they should not be treated as afterthoughts. A table that moves accurately is still not a mature plasma system if the surrounding plan for fume control, maintenance access, material handling, and electrical safety remains improvised. The first time a shop has to stop production to deal with a fume issue or a grounding problem, the cost of the DIY approach becomes clear.
Consider the grounding requirement specifically. Plasma cutting requires a solid work lead connection to the material being cut. A poor ground causes arc instability, erratic cut quality, and premature consumable wear. In a DIY build, the grounding path may pass through multiple connections: the work lead to the table frame, the table frame to the slats, the slats to the material. Each connection is a potential failure point. A production-ready system is designed with a clear, robust grounding path that minimizes resistance and maintains consistency.
Fume management is another area where the difference is significant. Plasma cutting generates fine particulate that is hazardous to breathe. A downdraft table or an adequate extraction system is not optional for a production environment. The cost of this equipment should be included in the total investment calculation for either route. A DIY builder who skips fume management to save money is making a decision that will affect operator health and regulatory compliance.
Maintenance And Consumable Cost Over Time
The cost comparison between DIY and production-ready systems extends well beyond the initial purchase. Consumables, replacement parts, and maintenance labor are ongoing costs that differ between the two routes.
Plasma consumables include electrodes, nozzles, swirl rings, and shields. These wear out based on arc hours, material thickness, and cut quality. A system that maintains consistent torch height and pierce parameters will extend consumable life. A system that crashes the torch into the plate or runs with incorrect pierce settings will consume parts faster.
In a DIY build, the operator is responsible for diagnosing consumable wear patterns and adjusting parameters accordingly. This requires experience and attention. In a production-ready system, the manufacturer’s recommended settings provide a baseline, and the operator can focus on monitoring and adjusting for specific material lots.
Replacement parts availability is another consideration. A production-ready system from an established manufacturer has a defined parts catalog and a service network. If a drive motor fails, you can order the exact replacement and install it. With a DIY build, you may need to source components from multiple suppliers, verify compatibility, and handle warranty claims yourself.
Commercial Shops Usually Need Time-To-Stable-Output, Not Just Low Hardware Cost
This is where many financial comparisons go wrong. Buyers compare frame, electronics, and torch-integration cost to the invoice price of a ready-made system. The more important comparison is time-to-stable-output.
How long until the system cuts well enough, consistently enough, and safely enough to support the intended work? How much owner attention does that path consume? What is the cost of troubleshooting when the shop should be quoting, cutting, or shipping?
If the build experience itself is part of the return, those hours may be worth it. If the shop’s real goal is dependable fabrication capacity, those hours are cost. A shop that spends three months debugging a DIY table has lost three months of production capacity, and that loss is rarely captured in the component-cost comparison.
Consider a concrete example. A job shop quotes a contract that requires cutting 500 identical brackets per month. The shop has two options: a DIY table that costs $8,000 in components and requires two months of evenings and weekends to build and tune, or a production-ready system that costs $25,000 and is cutting acceptable parts within a week of delivery.
The DIY route saves $17,000 in hardware cost. But if the shop’s billing rate is $80 per hour, and the owner spends 200 hours building and debugging the table, that is $16,000 in opportunity cost. If the table then requires an additional 30 minutes of operator attention per hour of cutting compared to the production-ready system, that is an ongoing labor cost that compounds over time.
The production-ready system costs more upfront, but it is generating revenue sooner and requiring less operator attention per cycle. The total cost of ownership over the first year may favor the production-ready system, even though the hardware cost is higher.
A Hybrid Route Often Makes More Sense Than Either Extreme
Some buyers do not need to choose between total DIY and total turnkey logic. A hybrid strategy can work well. A shop may buy a production-ready core system and still build custom material supports, workflow tables, consumable storage, shielding, or extraction improvements around it.
That approach captures some of the customization benefit without asking the entire machine platform to be self-engineered. The buyer gets the stability of a proven motion and torch integration, while retaining the freedom to optimize the peripheral workflow. For many shops, this is the practical middle ground.
For example, a shop might purchase a production-ready plasma table with a standard 4×8 cutting area, then build a custom roller conveyor system for loading and unloading sheets. The conveyor is not part of the machine’s critical path; it is a workflow improvement that the shop can design and build without risking the machine’s core performance.
Similarly, a shop might buy a production-ready system and then build custom fixturing for repeatable parts, a dedicated consumable storage area, or a specialized slat system for a particular material type. These peripheral customizations add value without compromising the machine’s integration quality.
Buy The Operating Model You Actually Need
DIY CNC plasma tables make sense when the build itself is part of the return and the user is willing to invest time in integration, tuning, and learning. Production-ready plasma systems make sense when the business needs stable output, lower uncertainty, and a faster path to dependable cutting.
Both routes can produce parts, but they do not produce the same daily operating experience. The DIY route rewards patience and problem-solving. The production-ready route rewards consistency and schedule reliability. Choose the one that matches how your shop actually works, not the one that looks cheaper on paper.
If you are leaning toward a production-ready system, reviewing the available plasma and cutting equipment options can help you scope the investment realistically. If you are leaning toward a DIY build, budget for the full scope of work, including the hours you will spend on integration and troubleshooting. Either way, make the decision based on the operating model you need, not the price tag alone.