Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
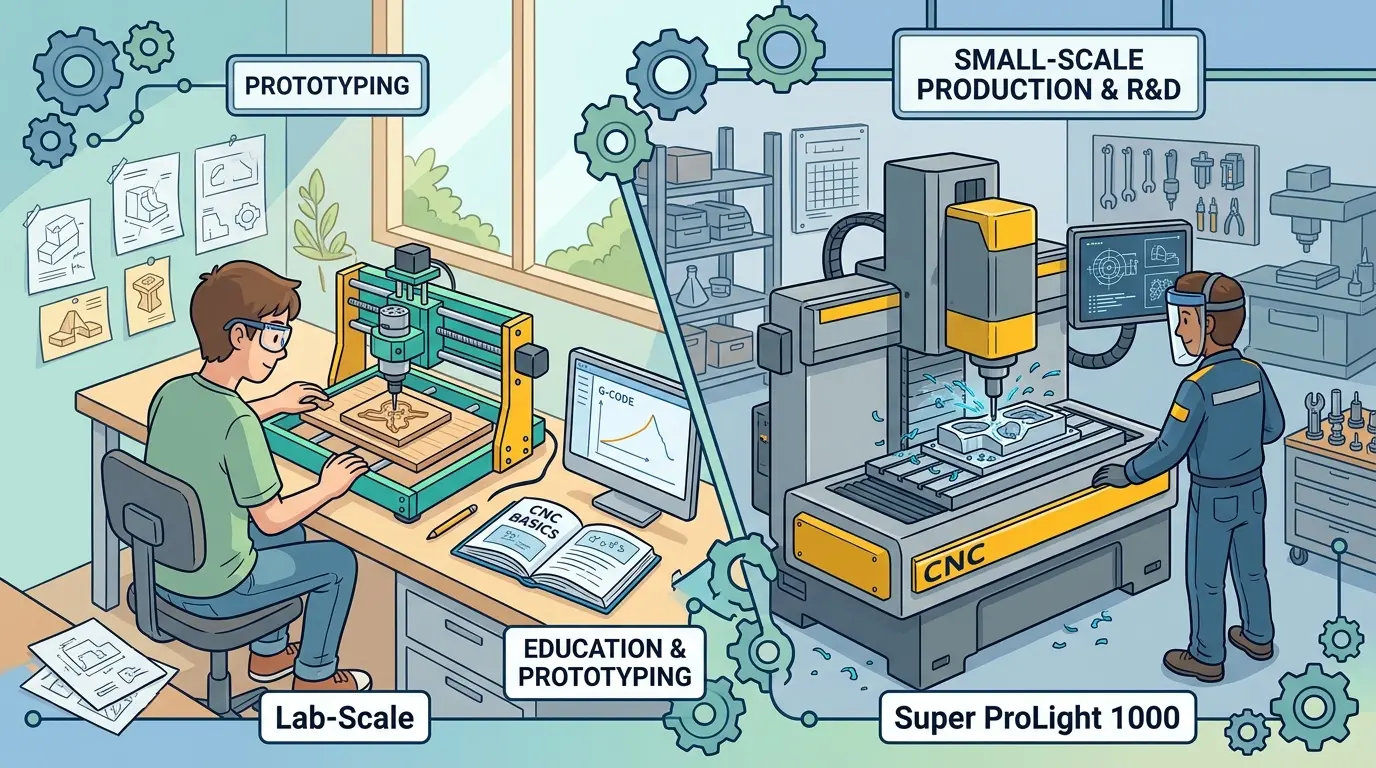
Buyers evaluating a Prolight 1000 or similar lab-scale CNC mill against a full-size vertical machining center are measuring the wrong problem. These compact machines exist for supervised training rooms, engineering labs, and prototype benches where access, floor space, and instructional control outweigh spindle power and throughput. The real selection decision hinges on part family, workholding discipline, and support burden, not raw capacity. Before comparing specs, define whether the workflow demands controlled iteration or sustained outputâbecause a machine that fits a classroom will fail under production pressure, and that mismatch surfaces only after purchase.
Lab-Scale CNC Mills Are Not Miniature Production Centers
The most common mistake buyers make with machines like the Prolight 1000 is evaluating them against the wrong benchmark. Comparing a compact training mill to a full-size vertical machining center produces a predictable result: the smaller machine loses on spindle power, travel, tool capacity, and throughput. That comparison misses the point of the category entirely.
Lab-scale CNC mills solve different problems. They address access, supervision, floor space, and instructional control before they address raw machining capacity. A school, technical college, engineering lab, or R&D group often needs real CNC capability in a format that fits a room rather than a production hall. The machine needs to be teachable, physically contained, and appropriate for bench-scale or small-room use. When those conditions define the purchase, a compact mill is not a compromised version of something larger. It is correctly sized for the job.
Who Actually Buys These Machines
The strongest fit for Prolight-class equipment is institutional and technical. Schools, training centers, engineering departments, and research groups benefit from a mill that is compact enough for a lab but still serious enough to teach core machining concepts and support genuine small-part work.
The goal in these environments is not throughput. It is controlled exposure to CNC workflow. Students and early-stage engineers need to learn setup logic, toolpath behavior, fixturing discipline, process planning, offsets, and machine interaction in a space that is easier to supervise than a production floor. A lab-scale mill makes that possible without requiring the infrastructure, safety protocols, and floor space of industrial equipment.
Prototype teams get similar value. A compact mill supports quick part validation and process experimentation when the work envelope and volume demands are modest. The machine shortens design-learning cycles. It does not replace a job shop or a machining center, and it should not be asked to.
Small Footprint Does Not Mean Casual Use
Buyers often assume that a small machine implies light-duty expectations. That assumption is not always correct. A compact lab-scale mill can be a serious tool when the work is genuinely small and the environment benefits from controlled operation.
The distinction is not whether the machine is “real.” The distinction is what kind of reality it serves. In a supervised training room, research lab, or small prototype space, the right machine is the one that makes real CNC practice manageable. That can be more valuable than larger capacity that the space, users, or workflow cannot support properly.
This is also why these machines hold more credibility in structured technical settings than typical hobby options, even when the work envelope is limited. Their value is tied to how well they fit the environment around them.
Lab-Scale Mill vs. Hobby Router: Compare Part Type First
Some buyers compare lab-scale mills to hobby routers because both fit in smaller spaces. The comparison is only partly useful. Router-style systems are better aligned with flat materials, sheet goods, wood parts, and sign work. A lab-scale mill makes more sense where parts are small, milling-oriented, and tied to fixture-based bench work rather than panel routing.
Start with the part family. If the work is closer to small machined components than routed panels, the mill format has clearer logic. If the work is mostly wood, plastics, and flat custom pieces, a router category may be more appropriate.
Lab-scale mills also tend to outperform hobby systems in formal environments where consistency, structure, and instructional value matter. A hobby machine may cost less, but it may not provide the same operational discipline or instructional credibility when the machine must serve multiple users across repeated training cycles.
Older Named Lab Mills Need Extra Scrutiny
When comparing older named platforms like the original Prolight 1000 with newer small mills, the right question is not which one was once respected. It is whether the support path, control familiarity, documentation depth, and maintenance burden make sense today.
An older lab machine may still be useful if it is well understood and supported internally. It can also become a liability if replacement knowledge is fading, service information is thin, or the machine starts consuming technical time the institution never planned to spend.
This matters especially for schools and businesses that do not want the machine to become a restoration project disguised as a training asset. A small machine is not automatically simple to own over time. Legacy control assumptions and spare parts issues can create more operational drag than the machine’s size suggests.
Buyers considering older Prolight-class equipment should look beyond historical reputation. The real ownership question is whether the team can support it practically over the next few years.
Controlled Prototyping: Where These Machines Earn Their Keep
In engineering offices and development groups, a lab-scale mill is extremely useful when parts are small, fixtureable, and tied to fast iteration rather than volume production. The machine may never become a high-output asset, but it can save substantial time by making design checks, trial parts, and process experiments possible without waiting for outside machining support.
This benefit holds when the machine stays inside its proper lane. If the work involves validating geometry, testing fit, checking a concept, or supporting technical learning, a compact mill is a strong workflow tool. If the work expands into delivery pressure, repeated output, or broader material ambition, the same machine becomes restrictive.
Not all prototype workflows are the same. Some stay small and controlled. Others are really early production in disguise. Judge the machine against the actual prototype work happening, not the work you hope to grow into.
Where the Category Breaks Down: Production Pressure
The harder comparison is between a lab-scale machine and a full industrial solution. This is where many buyers overreach. A compact mill can be very useful in R&D, learning, and small-part contexts, but it is not automatically a wise answer for repeat production, broader material ambition, or fast-growing output requirements.
If the workflow already depends on sustained throughput, heavier cutting, multi-shift use, or formal process integration, the lab-scale machine is a detour rather than a solution. The right answer is not to ask the small machine to work harder. It is to reassess machine class.
This is the trap many buyers fall into after an initially successful purchase. The machine performs well in a contained role, so the organization gradually asks it to support more responsibility. Once production pressure sneaks in, the buying assumptions that made the machine look ideal stop holding.
Questions to Answer Before Choosing This Class
Before selecting a Prolight-class machine, work through these questions explicitly:
- Is the main purpose education, supervised training, prototyping, or light production?
- Are the parts genuinely small enough that the machine will remain convenient rather than restrictive?
- Does the machine need to serve many learners, a few engineers, or one experienced operator?
- Will the environment benefit from a compact, easier-to-place machine more than it would from greater industrial capacity?
- Can the team support the controls, tooling, maintenance, and documentation path without turning ownership into an unexpected technical burden?
- Will the machine still fit the workflow twelve months from now, not only on delivery day?
These questions sound basic, but they prevent many weak purchases. A lab-scale machine is most valuable when its role is clearly defined from the beginning.
Positioning in the Wider CNC Landscape
Lab-scale mills sit between hobby access and industrial capacity. They are more structured and institution-friendly than hobby options, yet far less production-oriented than industrial machines. That middle position is their value.
If the buyer needs a personal machine for casual exploration, a desktop prototyping mill built around small precision work may be the more relevant comparison. If the buyer is drifting toward heavier commercial work, the more useful frame is how small mills differ from industrial ones once workflow capacity starts to matter. If the purchase discussion includes older machines, used-equipment questions, or support uncertainty, it also helps to think through what to inspect before paying for second-hand CNC equipment.
How Pandaxis Helps Frame the Decision
Pandaxis is centered on industrial machinery categories, which is useful context because it highlights how machine logic changes once throughput and workflow coordination become more important than contained scale. Buyers who are choosing a lab-scale mill as a bridge into more serious production planning may benefit from examining the Pandaxis shop to understand where industrial categories begin to solve problems that compact educational or prototype mills are not meant to carry.
That wider view forces a more honest internal discussion. Is the organization solving for access and learning, or is it actually trying to postpone a larger production decision? Once that question is answered honestly, the correct machine class often becomes clearer.
Right Environment, Right Machine
Prolight-class and other lab-scale CNC mills are best for educational programs, technical training, prototype work, and small bench-scale parts in environments where accessibility, manageable size, and supervised use matter. They make CNC machining practical in places where full industrial equipment would be excessive or impractical.
They are not substitutes for production machines, nor are they the automatic answer for every small part. Buyers who define the work clearly and respect the machine’s intended role get excellent value. Buyers who expect lab-scale equipment to carry industrial responsibility usually discover the mismatch after the purchase, when support, workload, and workflow demands begin to diverge.
In the right environment, these machines are not compromised. They are correctly sized. In the wrong environment, they become small reminders that the buying problem was never really about footprint at all.
Spindle and Tooling Realities on a Lab-Scale Mill
The spindle on a Prolight-class machine is not a scaled-down version of a production spindle. It is a different tool entirely, and understanding that difference prevents most of the disappointment that follows an over-ambitious purchase. These machines typically run lighter-duty spindles that suit small end mills, engraving cutters, and light finishing passes in softer materials. They are not built to hog material out of a solid block of steel in a single pass.
That limitation is not a flaw. It is a design boundary that keeps the machine affordable, quiet enough for a classroom, and safe for less experienced operators. The practical consequence is that toolpaths must be planned differently. Shallow depth-of-cut, higher spindle speed, and smaller stepovers become the default strategy. Feed rates need to be conservative enough to avoid chatter, but aggressive enough to keep the cut clean and the tool life reasonable.
Tooling selection matters more on these machines than on industrial equipment. Because the spindle has less torque, a dull or mismatched cutter will stall the cut or produce a poor surface finish long before it would on a heavier machine. Carbide tooling, proper chip load, and correct tool holding become essential habits rather than optional refinements. For a training environment, this is actually a benefit: it forces operators to learn proper toolpath strategy and tool selection discipline from the start.
Workholding Is the Real Bottleneck
The most common failure mode on a lab-scale mill is not the machine itself. It is the workholding. Small machines amplify workholding mistakes because there is less mass and rigidity to absorb the consequences of a poorly secured part.
A part that shifts during a cut on a production machine may produce a scrapped component. The same shift on a compact mill can break a cutter, damage the spindle, or create a safety hazard in a supervised environment. The work envelope is small, which means fixturing solutions must be precise and repeatable. Standard vises, toe clamps, and modular fixturing systems all work, but they require more care in setup than on larger machines where the mass of the machine itself provides some forgiveness.
For schools and labs, this creates a valuable teaching moment. The discipline of proper workholding, torque specifications, and fixture verification transfers directly to industrial practice. For prototype teams, it means the machine rewards careful setup with consistent results and punishes shortcuts with wasted time and broken tooling.
Software and Control Familiarity Matter More Than Hardware Specs
Buyers comparing older Prolight machines against newer compact mills often focus on travel, spindle speed, and table size. Those specifications matter, but the control software and post-processor compatibility deserve equal attention.
A machine that requires proprietary software, obscure post-processors, or outdated communication protocols will consume technical time every time a new part is programmed. A machine that works cleanly with common CAM packages and standard G-code workflows becomes transparent to the process. The difference shows up in setup time, not in the spec sheet.
For institutions running multiple machines, control consistency across the lab reduces training overhead. Students who learn on one control should be able to transfer that knowledge to the next machine without relearning basic navigation. If the lab-scale mill uses a control that is far removed from what students will encounter in industry, the instructional value drops regardless of how well the machine cuts.
Maintenance Burden: Small Machine, Real Responsibilities
Compact mills still require lubrication, way cleaning, spindle inspection, and periodic calibration. The maintenance interval may be longer than on a production machine, but the consequences of skipping it are not proportionally smaller.
A neglected lab-scale mill develops backlash, lost steps, or spindle runout that quietly degrades part quality. In a training environment, that degradation is worse than lost production. Students learn to accept poor surface finish and dimensional drift as normal, which builds bad habits that carry into their professional work.
The maintenance question is also a staffing question. Who owns the machine? If the answer is unclear, the machine will drift into disrepair faster than a production asset, because no one’s daily output depends on it. Assigning a named owner, even part-time, and building a simple preventive maintenance schedule into the lab routine keeps the machine accurate and the training value high.
Material Selection Defines the Machine’s Usefulness
The material range of a lab-scale mill is broader than many buyers assume, but narrower than they hope. Aluminum, brass, plastics, and machinable wax are all realistic candidates. Steels and harder alloys are possible but require patience, light cuts, and appropriate tooling. Exotic materials should be treated as exceptions rather than routine work.
For prototype teams, this material envelope covers most early-stage validation work. Aluminum prototypes, plastic test parts, and fixture components are the bread and butter of product development. The machine handles these well when the part geometry respects the machine’s rigidity limits.
The trap is material ambition creep. A team that starts with aluminum and plastics may begin asking for steel parts as the project matures. At that point, the lab-scale mill becomes a source of frustration rather than a tool. The honest conversation is not about whether the machine can cut steel at all, but whether the time required to do so is a sensible use of the team’s schedule.
Comparing Against the Right Alternative
The most useful comparison for a Prolight-class machine is not against a full machining center. It is against the alternative ways to get small parts made. That alternative might be an outside machine shop, a manual mill with a DRO, or a larger machine that the organization already owns.
Against an outside shop, the lab-scale mill wins on turnaround time and design iteration speed. It loses on material range and surface finish capability. Against a manual mill, it wins on repeatability and the ability to run unattended for short cycles. It loses on operator skill requirements and the tactile feedback that manual machining provides.
Against a larger machine already in the building, the compact mill wins on accessibility and scheduling flexibility. A small job does not need to wait for a break in the production schedule. It loses on capability, but that loss only matters if the small machine is asked to do work that should have been routed to the larger asset.
When the Purchase Is Justified
The clearest justification for a Prolight-class machine is a workflow that generates small, repetitive, fixture-based parts in soft materials, with a team that benefits from immediate access and controlled operation. That combination appears in engineering labs, technical schools, and prototype shops that value iteration speed over raw output.
The purchase is harder to justify when the work is one-off, highly varied, or likely to grow in size and material difficulty. In those cases, the machine will either sit idle or be pushed beyond its design envelope. Both outcomes waste the investment.
Buyers who can articulate which of these two patterns describes their work have already done the hardest part of the selection process. The machine itself is secondary to that clarity.