Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
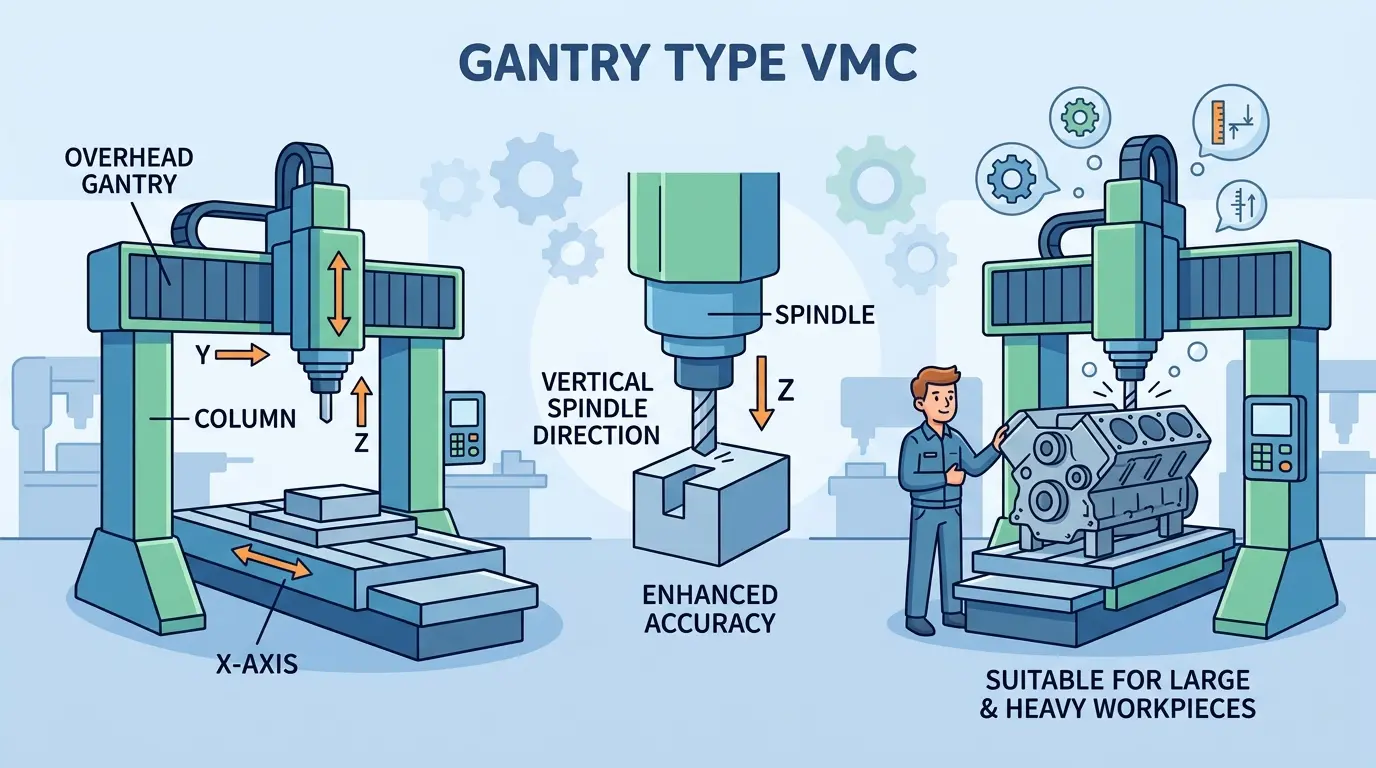
When a supplier quotes a “gantry-type VMC,” the label can mask a wide gap between envelope and actual cutting capability. The bridge layout genuinely solves a load-path problem for wide tables, but it does not automatically deliver machining-center-grade tooling, spindle torque, or sustained duty cycle. Buyers who treat the phrase as a specification risk comparing machines that look alike yet differ sharply in process ceiling. Before any quote comparison begins, verify the taper, tool changer, coolant strategy, structural mass, and floor-loading reality against your specific workload—otherwise you may pay machining-center money for a large-format machine that cannot hold the cut.
Start With the Work, Not the Label
When a machine supplier or builder uses the term “gantry-type VMC,” it sounds like a precise specification. In practice, it is often a starting point for a conversation that needs to go much deeper. The phrase combines two attractive ideas: the reach and envelope of a gantry layout with the tooling discipline and cutting seriousness implied by the VMC designation. That combination is commercially powerful, but it can also compress several unresolved questions into one impressive-looking label.
The practical question for a shop floor is not whether the machine has a bridge structure and a vertical spindle. It is whether the machine behaves like a machining center in the ways that matter for the workload. A gantry layout can be the right structural answer for large parts, but it does not by itself prove the machine belongs to a full machining-center class. Buyers who treat the term as a conclusion rather than a clue often end up comparing machines that look similar but have very different process ceilings.
What the Gantry Layout Actually Solves
The gantry or bridge arrangement exists for a real structural reason. As work envelopes grow, table width increases, and part sizes change, the load path through a conventional column-and-table design becomes less practical. A bridge layout distributes structure across the span and provides top access over a broad working area. For large plates, wide workpieces, or parts that need access across the whole table, that geometry makes sense.
Think about what happens on a conventional vertical machining center when the table gets wider. The column must reach farther to cover the full table width, and the cantilevered load grows. The spindle head hangs further from the column face, which increases deflection under cutting forces. At some point, the column-and-table architecture stops being the economical answer. A gantry design solves this by moving the structural burden to the bridge itself. The spindle carrier travels along the crossbeam, and the crossbeam spans the work area. The load path is more direct, and the structure can be made stiffer for a given envelope.
This matters most in specific production situations. A mold shop cutting large die plates needs the spindle to reach across a wide table without losing rigidity at the extremes. A manufacturer of large aluminum frames or structural components needs consistent positioning accuracy whether the spindle is working near the left edge, the center, or the right edge of the table. A shop processing thick plate stock needs the Z-axis to maintain stiffness at depth without the whole column flexing. In all these cases, the gantry layout is not a marketing choice. It is an engineering response to a real geometric problem.
What the gantry does not solve is machine class. The layout addresses a geometry and load-path question. It does not automatically deliver heavy-duty cutting stability, tooling sophistication, thermal control, or machining-center-level duty cycle. A machine can be honestly gantry-based and still sit below the performance class a buyer assumes when hearing the word VMC. That is the central warning behind the term.
Why the Term Misleads So Easily
The phrase is easy to misuse because it combines two ideas buyers already like. “Gantry” suggests envelope, reach, and large-part capability. “VMC” suggests machining-center seriousness, tooling discipline, and metal-cutting legitimacy. Put them together and many buyers instinctively assume the machine must be both large and fully machining-center-grade. That is not always true.
The term can also be used loosely to make a lighter large-format processing machine or a router-like platform sound closer to a full machining-center class than it really is. Until the buyer verifies the spindle system, tool management, coolant or dust strategy, structure, rigidity, enclosure logic, and duty expectations, the phrase is not a conclusion. It is only a description of layout.
This is exactly where bad quote comparisons start. Machines with similar external forms get grouped together even though their tooling logic, material-removal environment, and daily workload behavior may be very different. A shop that cuts aluminum plate with a 12,000 RPM spindle and a 20-tool magazine has different requirements than a shop cutting steel weldments with a geared head and a 40-tool carousel. Both machines might be described as gantry-type VMCs. They are not the same machine class.
Spindle and Tooling Architecture Reveal the Truth Fastest
If a seller presents a machine as a gantry-type VMC, the fastest way to test the claim is to inspect the spindle and tooling system. Useful verification questions include:
- What spindle interface or taper is actually in use? A CAT-40 or BT-40 taper with a power drawbar is a different animal from a quick-change collet system designed for lighter work.
- What tool magazine and changer arrangement does the machine have? A true machining center typically has an automatic tool changer with a magazine that holds tools in a protected environment, with a changer arm that swaps tools quickly and reliably.
- Is the tool system designed for real machining-center workflow, or for lighter large-format processing? Look at how tools are held, whether the spindle has a positive drawbar retention force, and whether the changer can handle the tool weights and lengths your jobs require.
- Does the spindle and tooling package support sustained metal-cutting logic, or is the label floating above the machine’s true intent? Check the spindle motor rating, the torque curve, and whether the machine has a spindle orientation function for rigid tapping.
These questions matter because tooling logic exposes machine philosophy quickly. A machine intended for true machining-center work usually reveals that intention clearly through how tools are held, changed, protected, and managed. A lighter or different class of machine often reveals itself just as clearly. Experienced buyers do not stay at the brochure level for very long. They move straight to the spindle and tooling architecture.
Consider a concrete example. A shop cutting large aluminum plates for jigs and fixtures needs to run a 1-inch end mill at 8,000 RPM with a 0.75-inch depth of cut. The machine must hold that tool securely, deliver enough spindle torque to maintain the cut without stalling, and change tools quickly between roughing and finishing operations. A gantry machine with a 40-taper spindle, a 15-horsepower motor, and a 24-tool magazine can handle that work. A similar-looking machine with a 3-horsepower spindle and a manual tool change cannot, regardless of how impressive the bridge structure looks. The envelope is the same. The process capability is not.
Cooling, Chip Handling, and the Working Environment
Another fast reality check is to look at the cutting environment the machine is built to survive. If the machine is being presented as machining-center-grade, buyers should ask how coolant is handled, how chips are evacuated, how the enclosure supports sustained cutting, and whether the daily operating environment looks like real machining-center work or something lighter.
Machines reveal their intended process class through environment design just as much as through spindle specs. A machine genuinely organized around sustained cutting usually looks prepared for that reality in its enclosure logic, chip-management behavior, and serviceability around fluid or debris handling. These questions are often more honest than marketing labels because machines are difficult to disguise at the process-environment level.
Walk around the machine and look at the details. Does the enclosure have proper doors that seal well enough to contain coolant mist? Are there chip augers or a conveyor system to move swarf out of the cutting zone? Is the coolant tank sized for the flow rate the spindle and cutting tools will demand? Are the way covers protecting the linear guides robust enough to keep chips from packing into the bearing surfaces? A machine built for light engraving or routing might have minimal chip management because it does not generate significant swarf. A machine built for real metal removal must have a serious answer for the debris it creates.
The working environment also includes thermal behavior. A machining center running sustained cuts generates heat in the spindle, the ball screws, and the structure itself. If the machine has no thermal compensation or coolant temperature control, positioning accuracy will drift over a long shift. A gantry machine with a large structure is especially sensitive to thermal growth because the bridge spans a wide area. If the machine is not designed to manage that heat, the first part of the morning may be accurate while the parts cut after lunch are progressively out of tolerance.
Large Envelope Does Not Mean Heavy-Duty Capability
One reason the phrase survives is that buyers often associate large physical scale with process seriousness. If a machine is large, enclosed, and vertical, it feels intuitive to assume it belongs to a full machining-center category. That is a dangerous shortcut.
A large machine can still be optimized for lighter or different work than the buyer assumes. It can still sit below the machining-center class implied by the term VMC. Size may support capability, but it does not define capability by itself. This is where buyers get caught paying for impressive envelope while still not getting the process class they expected. The machine may be physically large enough for the parts, yet not built to own the cutting behavior, tool logic, or duty cycle the application really needs.
Look at the structural details rather than the overall dimensions. How thick are the column walls and the crossbeam section? What material is the structure made from—welded steel fabrication, cast iron, or a lighter aluminum or composite construction? What is the mass of the machine relative to its envelope? A heavy machine with a robust casting is likely built to absorb cutting forces. A lighter machine with a fabricated frame may be built to move quickly but not to take deep cuts in tough materials.
The linear guide system also tells a story. A machine with wide, preloaded linear guides on all axes and large-diameter ball screws is built for rigidity and thrust. A machine with narrower guides and smaller screws may be adequate for lighter cutting but will flex or wear prematurely under sustained heavy loads. The same logic applies to the spindle housing. A massive, ribbed spindle casting with a large bearing set is built for radial and axial loads. A slim spindle housing with smaller bearings is built for lighter work.
Bigger Machines Create Bigger Plant Consequences
As machine size grows, installation reality becomes part of machine capability. A large gantry-style platform may look attractive on a quote because the working envelope seems generous, but that value only becomes real if the plant can load, service, and operate it honestly. Buyers should evaluate more than just the cutting zone:
- Floor or foundation suitability: A large gantry machine distributes its weight over a wide footprint, but the floor must still support the total mass plus the dynamic loads from cutting and rapid moves. A concrete slab that is too thin or poorly reinforced can allow the machine to settle unevenly, which destroys alignment.
- Service access around the machine: The spindle head, the tool magazine, the coolant system, and the electrical cabinet all need maintenance access. If the machine is pushed against a wall or crowded by other equipment, routine service becomes difficult and expensive.
- Material-handling paths into and out of the working area: A large part must get onto the table and off again. If the shop has no overhead crane, no forklift path, or no roller conveyor system that can handle the part weight, the machine’s envelope is theoretical rather than practical.
- Loading method for large or heavy parts: Some gantry machines have a fixed table that the bridge travels over. Others have a moving table that shuttles in and out of the cutting zone. The loading method affects how easily the operator can position and clamp the workpiece.
- Coolant, chip, or dust management at the scale the machine will actually produce: A machine cutting large volumes of metal generates large volumes of chips. If the chip conveyor is undersized or the coolant filtration is inadequate, the machine will spend more time stopped for cleanup than cutting.
Large-envelope machines punish vague planning. If the floor cannot support the full workflow, the travel numbers become brochure assets rather than production assets. This is especially important when comparing a large gantry machine against a more conventional machining-center layout. The decision is not only about machining. It is also about how the machine will live inside the factory.
A shop that already has a 10-ton overhead crane and a clean, level concrete floor can handle a large gantry machine without much additional investment. A shop that currently moves parts with pallet jacks and has a floor with visible cracks will need to budget for foundation work, possibly a new crane or lift system, and a chip-handling solution before the machine can run at full capacity. These costs are often omitted from the initial machine quote, but they are real and they can exceed the price difference between a large gantry machine and a more conventional VMC.
The Expensive Mistake: Paying for the Wrong Kind of Seriousness
The common buying failure here is not misunderstanding what a gantry is. The common failure is paying for the wrong kind of seriousness. Some buyers need genuine machining-center behavior on a large format. Others really need a large-format machine for lighter or different work. Trouble starts when the first buyer purchases large-format appearance without machining-center substance, or when the second buyer overpays for machining-center vocabulary while the process does not actually require it.
That is why the label must be tested against the real job. If the work requires machining-center-grade tool logic, metal-cutting environment control, and reliable structural behavior under sustained load, the machine should prove that clearly. If the process is actually closer to large-format but lighter-duty work, the buyer should be honest about that too. Good buyers do not buy machine identity. They buy fit.
Consider two different production situations. The first is a job shop that cuts steel weldments for heavy equipment. The parts are large, the tolerances are moderate, but the material removal rate is high. This shop needs a machine that can take a 0.25-inch depth of cut in mild steel with a 2-inch face mill, hold that cut for hours without thermal drift, and change tools automatically between operations. The machine must have a robust spindle, a serious coolant system, and a chip conveyor that can handle the volume of steel swarf produced each shift.
The second situation is a manufacturer of large acrylic signs and displays. The parts are big, but the cutting forces are low. The shop needs a machine that can route, drill, and engrave acrylic sheets with high speed and good surface finish. The spindle can be lighter, the tooling system can be simpler, and the chip management is really dust and small chip evacuation rather than heavy swarf handling. This shop does not need machining-center-grade metal-cutting capability. It needs a large-format CNC router with good accuracy and fast traverse rates.
Both shops might be quoted a “gantry-type VMC.” The first shop needs the full machining-center package. The second shop would be overpaying for capability it will never use. The label does not tell either buyer which machine is right. Only a careful analysis of the actual work does.
Process Discipline Before Comparison
The same discipline applies when the comparison is between a large bridge-style machine and a more conventional machining-center format. The two layouts diverge significantly when large-part production becomes the real issue. Similarly, if the confusion is actually between woodworking-style CNC and metalworking milling language, it helps to separate wood-processing CNC logic from machining-center logic before categories get mixed together.
A woodworking CNC router and a metal-cutting VMC share some vocabulary—both have spindles, tables, and tool changers—but they are built for different process realities. The woodworking machine typically has a higher spindle speed, a lighter structure, and a dust-collection system instead of a coolant system. The metal-cutting machine has a lower spindle speed with higher torque, a heavier structure, and a flood-coolant system. If a buyer is evaluating a machine that could be used for either material, the process category must be defined before the machine comparison begins.
For buyers working through this evaluation, the practical habit worth copying is simple: keep the process category honest before the comparison becomes expensive. That means reading past the label every time. If the machine proves its class through structure, tooling, operating environment, and workload fit, then the term is meaningful. If not, it is only compressed marketing language.
The safest rule is straightforward: treat “gantry-type VMC” as the start of technical due diligence, not the end of it. That is usually what protects a buyer from paying machining-center money for a machine whose real class was never fully confirmed.
Building a Verification Checklist
To make the due diligence concrete, build a checklist before you start comparing quotes. The checklist should cover the machine’s structural class, its tooling architecture, its cutting environment, and its installation requirements. For each item, write down what your application actually needs rather than what the brochure claims.
Start with the spindle. What taper does your tooling require? What spindle speed range do your cutting tools need? What torque is required for the heaviest cut you plan to take? What duty cycle will the spindle see—continuous roughing, intermittent finishing, or a mix? Write these numbers down before you look at any machine.
Next, define the tooling workflow. How many tools does a typical job require? How often do you change tools between operations? Do you need rigid tapping? Do you need through-spindle coolant for deep-hole drilling? These requirements will tell you whether a simple tool changer is adequate or whether you need a full machining-center tool management system.
Then define the cutting environment. What material are you cutting? What is the expected chip volume per hour? Do you need flood coolant, mist coolant, or dry cutting with vacuum dust collection? What enclosure level is required to keep the work area safe and clean? These answers will tell you whether the machine’s coolant and chip-handling systems are adequate.
Finally, define the installation reality. What is the floor load capacity where the machine will sit? What is the ceiling height? What material-handling equipment is available to load parts? What is the service access situation? These answers will tell you whether the machine can actually operate in your facility.
The Bottom Line for Buyers
The term “gantry-type VMC” is useful as a starting point, but it is not a specification. It describes a layout, not a performance class. The bridge structure solves a real geometric problem for large workpieces, but it does not guarantee machining-center-grade cutting behavior, tooling discipline, or duty cycle.
Buyers who succeed with large-format machining do not rely on labels. They verify the spindle and tooling architecture, inspect the cutting environment, evaluate the structural details, and plan for the installation reality. They compare machines based on what the machine can actually do for their specific workload, not on what the category name implies.
If you are evaluating a gantry-style machine for your shop, use the checklist above to separate the machines that genuinely belong to the machining-center class from those that merely look the part. The machine that passes the verification is the one worth buying. The machine that fails it is the one that will cost you in rework, downtime, and missed deliveries. The label is only the beginning. The verification is what protects your investment.