Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
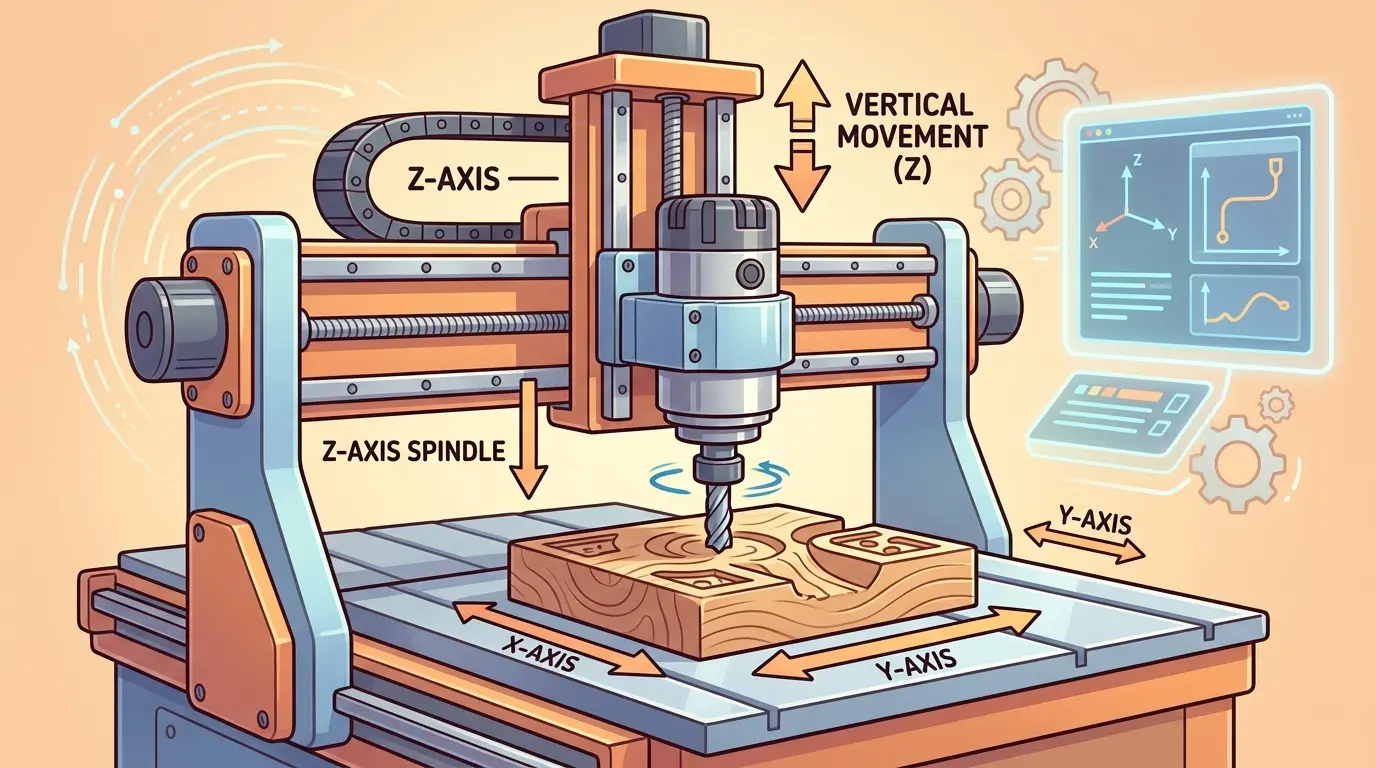
When a spec sheet lists a “Z-axis spindle,” the label can mask the real production risk: the entire vertical load path that carries the cutter into the material. A powerful spindle mounted on a weak carriage, undersized guides, or an overextended stroke will chatter on plunge, drift on depth, and force operators to slow feeds or add verification cuts. Before you compare spindle badges or travel numbers, trace the tool tip upward through the mounting plate, carriage, and frame. That structural honesty determines whether your machine holds tolerance on deep pockets, long tooling, and tall fixtures—or merely moves convincingly in an air cut.
Read “Z-Axis Spindle” As a Load-Path Question, Not a Part Number
When a sales rep or spec sheet mentions a “Z-axis spindle,” it sounds like a specific component you can compare across machines. In practice, the term is a shortcut for something broader: the spindle plus the entire vertical structure that carries it into the cut. That distinction matters because buyers who treat the phrase as a product category often miss the real issue it points to.
A spindle can look strong on paper—good power, high RPM, reputable brand—but if the Z-axis carriage guiding it is weak, poorly supported, or mismatched to the job, the machine’s practical limit shows up there first. The spindle never works alone. It works through a stack of components: the spindle body, the mounting plate, the vertical carriage, the guide rails, the drive mechanism, and the machine frame that resists plunge and cutting forces.
So the useful way to read “Z-axis spindle” is not as a new technology but as a reminder to inspect the vertical load path. Instead of asking what kind of spindle it is, ask how it is mounted, how the carriage is supported, how much mass the Z system is managing, and how honestly the machine holds depth once the tool engages the material.
Start at the Tool Tip and Walk Upward
The clearest way to evaluate a vertical cutting stack is to trace the load path from the cutter back to the machine frame. The tool enters the work. Cutting force travels through the tool, into the spindle nose, through the spindle body, across the mounting plate, into the Z carriage, down the guide system, and finally into the machine structure. Every weak point in that chain affects how the cut feels and how repeatable the result becomes.
This is why two machines with similar spindle specifications can behave completely differently in production. One may carry the spindle through a short, well-supported vertical path with minimal overhang. Another may use a taller, lighter arrangement that flexes as tool reach and cutting resistance increase. The spindle label alone will not reveal that difference. The load path will.
Z-Axis Is Where a Machine’s Honesty Shows Up First
Many machines look convincing in light motion, dry runs, or headline specifications. The Z-axis is where the machine has to prove itself. That is where the tool enters the cut, where plunge loads become real, where tool stickout creates leverage, and where depth accuracy stops being theoretical. If the vertical structure is weak, problems appear there first.
Typical symptoms include chatter on entry, unstable wall finish, inconsistent depth across repeated parts, or a nervous feel once passes get deeper and the tool must stay controlled over more vertical distance. These problems can show up even when the spindle motor itself seems capable. That is why experienced buyers watch the vertical structure more carefully than the spindle badge.
Tool Length Changes the Whole Conversation
Tool length is one of the fastest ways to expose whether the vertical stack is genuinely capable. A short tool held close to the spindle nose asks relatively little from the Z-axis structure. A longer tool introduces leverage that magnifies any weakness in the carriage or guide system. The farther the cutting force acts from the supporting structure, the more quickly instability becomes visible.
This is one reason demonstration cuts can mislead buyers. A machine that behaves well with short tooling in shallow work may become much less convincing once the real job calls for longer reach, deeper pockets, taller fixtures, or aggressive plunge behavior. The spindle did not change. The leverage did.
Travel Is Not the Same Thing as Usable Stroke
Buyers often read Z travel as a simple capacity number. More travel sounds flexible, and sometimes it is. But travel alone does not tell you whether the machine holds the spindle steadily through that range, whether the carriage remains rigid at different extension positions, or whether the machine loses confidence once tooling, fixtures, and workpiece height combine in ordinary production.
Usable stroke matters more than travel as a brochure number. A machine can advertise generous movement yet still offer less honest cutting capacity than expected once real tool length, material thickness, spoilboard height, vacuum pods, clamps, or custom jigs enter the setup. Travel is easy to print. Usable vertical stability is harder to claim and more valuable to understand.
Clearance Matters Because Shops Rarely Cut on an Empty Table
Vertical cutting almost never happens in a vacuum. Parts sit on spoilboards, vacuum pods, fixtures, vises, blocks, or custom supports. Operators need enough clearance to load safely, set tools properly, avoid collisions, and still keep the spindle carried in a structurally honest range.
This is where buyers make a subtle mistake. They see travel and assume setup freedom, without asking whether the machine stays comfortable when that freedom is actually used. A machine that technically clears the setup but becomes less stable at the required extension is not offering the same practical value as a machine that holds the spindle confidently through the same work envelope.
Spindle Mass Has to Be Carried, Not Just Installed
The vertical structure is not only moving. It is carrying weight. As spindle packages become heavier, the Z-axis has more to support and control. That affects acceleration, deceleration, plunge behavior, and how the machine reacts once the tool meets resistance in the material. The spindle’s value cannot be separated from the carriage carrying it.
This is one reason spindle upgrades sometimes disappoint. Shops improve the spindle in isolation and then discover that the Z-axis carrying it was never comfortable with the added load. The machine may still move, but the upgraded spindle can expose the fact that the vertical stack was already near its comfort limit. The real question is not only whether the spindle is better. It is whether the vertical system is honest with that spindle installed.
Guidance Quality Matters More on Z Than Many Buyers Expect
Because the Z-axis manages entry, exit, and depth-sensitive motion, the quality of the guidance system matters a great deal. Rail support, bearing quality, carriage stiffness, alignment, and the drive method for vertical travel all contribute to whether the spindle feels planted or vague once cutting starts. A machine can feel acceptable in light lateral movement while still revealing weakness in vertical motion, because plunge and depth control make small errors more visible.
Vertical instability is frustrating in practice because it affects not only finish but operator confidence. When the machine feels uncertain in Z, operators begin changing feed rates, depth of cut, toolpaths, or tooling strategy to work around the machine instead of trusting it to support the process honestly.
Plunge Behavior Is Often the First Honest Test
Air cuts hide a lot. The spindle moves, the machine sounds fine, and the travel numbers look usable. The first plunge into real material is where the truth arrives. That moment loads the spindle vertically, asks the carriage to stay aligned, and exposes whether the whole stack is calm or whether the machine enters the cut with visible hesitation. If the spindle chatters on entry, if the finish immediately worsens near the top or bottom of the feature, or if operators start reducing ambition every time the tool must descend aggressively, the vertical stack is already speaking clearly.
Plunge behavior deserves more attention in demonstrations and early production trials. It shows whether the machine is only moving the spindle or actually controlling it under load.
Depth Holding and Restart Confidence Come From the Same Stack
Z-axis honesty affects more than surface finish. It also affects restart confidence, depth repeatability across repeated parts, and whether the machine can return to a known cutting condition after tool changes or interruptions. If the vertical system is weak or inconsistent, operators start distrusting the machine in subtle ways. They add verification cuts, extra checks, shallower passes, or unnecessary setup caution because they no longer trust depth to stay honest by default.
That hidden cost matters. A machine that looks acceptable in a first test part can still lose real productivity if the Z-axis carrying the spindle creates doubt every time the process has to be restarted, repeated, or handed to another operator.
Router and Mill Language Often Get Mixed in Unhelpful Ways
The phrase becomes more confusing because people move between router and mill vocabulary too casually. In lighter CNC router conversations, the spindle is often treated like a standalone performance symbol. In milling conversations, the structure carrying that spindle is usually considered more explicitly. When buyers combine the two habits of thinking, they can overestimate what the machine’s vertical system will tolerate.
This matters especially when router buyers start using milling language for operations that demand more from the Z stack than the machine class was built to support. A router can carry a spindle that sounds serious while still struggling in plunge-heavy or rigidity-sensitive work. The spindle alone does not convert the machine into a stronger vertical platform. The whole stack has to deserve the claim.
Small Vertical Weaknesses Surface Quickly in Real Cutting
The Z-axis leaves the machine with less room to hide weakness. Surface flatness, fixture height, tool length, plunge rate, and workholding all converge there. A slight lack of rigidity or guidance quality that looks tolerable elsewhere can become obvious when the tool enters the work, especially with longer tools or deeper features.
Buyers who ignore the vertical stack often discover problems only after installation. The machine may jog smoothly and sound convincing in a demonstration. The first real plunge-sensitive job reveals whether the spindle is actually being carried honestly. That is usually where the machine stops performing like its headline specs suggested.
Upgrades Often Fail Because Shops Improve the Wrong Layer
One practical reason to understand the so-called Z-axis spindle concept is that it prevents bad upgrade logic. When shops see disappointing cut behavior, they often look first at spindle power or spindle quality. Sometimes that is correct. But just as often the machine is exposing limits in the carriage, guide system, usable stroke, or total vertical rigidity. Upgrading the spindle without checking the load path can make the mismatch more visible instead of less.
Good upgrade decisions start with symptoms. Is the problem heat, runout, and spindle capability? Or is the problem that the vertical stack becomes uneasy once the tool reaches deeper, the setup gets taller, or the spindle package gets heavier? These are different faults, and the machine will not respond well if the wrong one is diagnosed.
Better Buyer Questions Replace Confusing Vocabulary
If the term appears in a quote, sales conversation, or product discussion, the productive response is not to ask what mysterious spindle type it names. The better questions are operational:
- How rigid is the vertical carriage under load?
- How much spindle mass is the Z system carrying?
- What is the usable vertical range with real tooling and setup height?
- Does the machine stay stable in plunge-heavy work?
- How does the structure behave when the tool is deep enough for leverage to matter?
- What kind of work is this vertical stack genuinely comfortable supporting every day?
Questions like these reveal far more than trying to decode the phrase as though it describes a special class of spindle.
What This Means for Machine Selection
For shops evaluating CNC routing equipment, this topic is directly relevant because router-based performance depends on matching spindle behavior, Z travel, clearance, and structural honesty to the real job. Buyers evaluating CNC nesting machines for panel processing, deeper routing, mixed-geometry work, or heavier spindle packages need to understand that the spindle is only as convincing as the axis carrying it.
The same logic applies to other machine categories. A sliding table saw with a weak carriage will not hold cutting quality regardless of motor power. An edgebander with poor pressure rollers will not produce clean joints regardless of glue pot quality. The principle is consistent: evaluate the machine as a cutting stack, not as a collection of disconnected terms.
The Most Useful Translation Is Still Simple
If someone says “Z-axis spindle,” the best shorthand translation is: check the vertical load path. Look at how the spindle is mounted, how the carriage is supported, how much mass the Z system is carrying, how much usable stroke remains once real tooling and fixtures are installed, and how the machine behaves once cutting load appears.
That reading is practical because it turns vague language into a clear inspection habit. It makes the term helpful instead of distracting.
Judge the Stack, Not the Label
A Z-axis spindle in CNC routing and milling usually means the spindle as carried by the machine’s vertical motion system, not a separate spindle category. The value of the phrase is that it pushes attention toward the whole vertical cutting stack: support, travel, clearance, plunge behavior, tool leverage, and structural load path.
That is what buyers should evaluate. If the vertical stack is strong, stable, and matched to the actual work, the machine has a real chance of performing well. If it is weak, no refinement of terminology will rescue it from a structural mismatch. That is the practical lesson behind the phrase and the reason it is still worth understanding.