Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
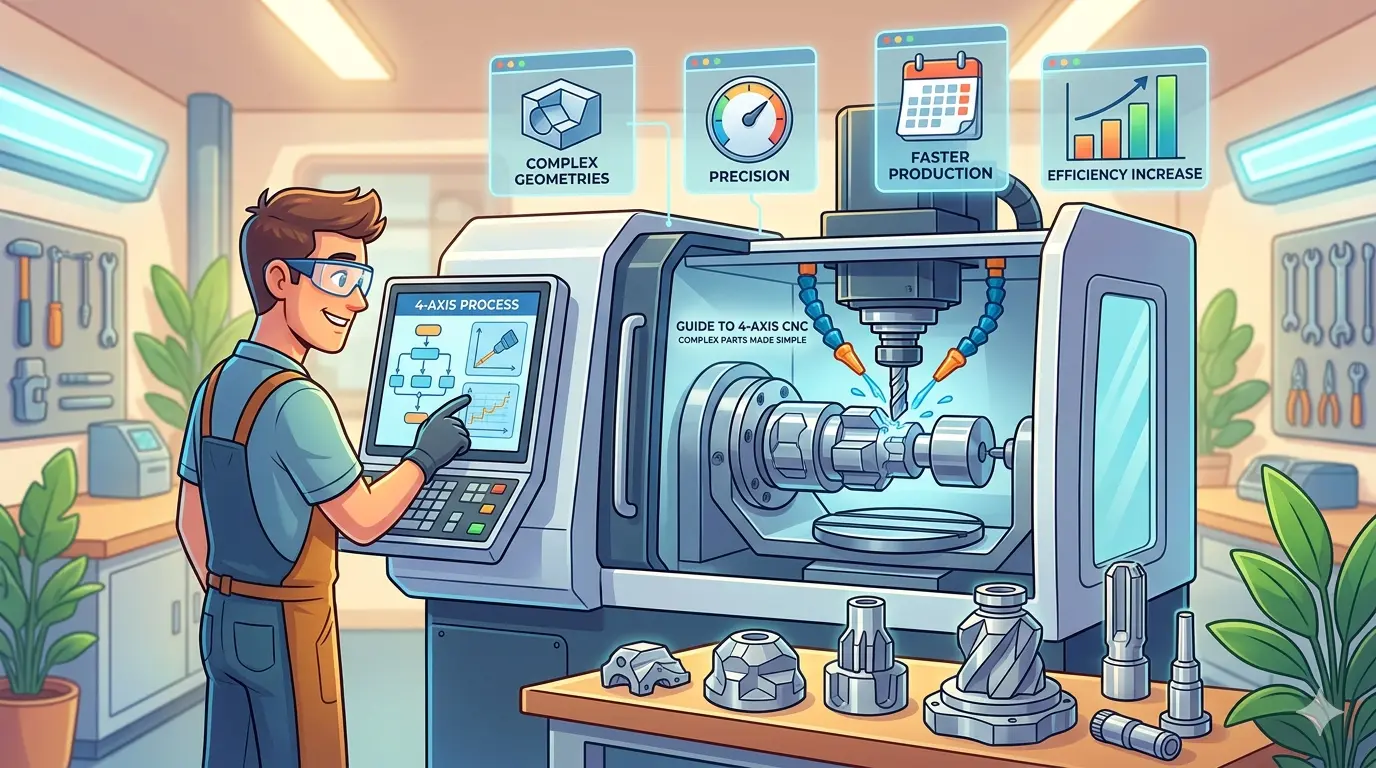
Before comparing rotary tables or controller specs, the four-axis decision has to start with your job history, not a showroom demo. The article walks through the real production logic: identifying recurring parts that bleed time in re-clamping, distinguishing indexed positioning from continuous rotary interpolation, and matching the axis to a repeat part family rather than a few impressive samples. Setup compression is the actual return, but that payback only holds if the rotary unit stays rigid under load, the fixture strategy is repeatable, and the CAM and post support are owned. If the bottleneck is sheet flow or drilling throughput, a rotary axis is the wrong fix entirely.
Start With the Jobs That Keep Costing You Setup Time
Before you compare rotary tables, trunnions, or controller options, pull the job history for the last three to six months. The decision to move from three-axis to four-axis machining should come from a recurring production problem, not from a machine demonstration or a single impressive sample part.
Look specifically for parts that keep losing time in re-clamping. Side holes, radial patterns, multi-face features, wrapped details, cylindrical work, and angular machining all create the same complaint on a three-axis route: the machine can cut the features, but the workflow pays too much for handling and alignment. The extra axis only matters if rotary motion removes real setup loss, protects positional relationships, and lets a recurring part family move through production more predictably.
Review which recurring parts keep costing time because they must be rotated and re-datumed, side-drilled or cross-machined in separate setups, manually indexed between faces, or re-clamped in ways that keep weakening positional confidence. If those jobs appear only occasionally, better fixturing or indexed manual methods may solve more than a rotary purchase. If they appear every week, the four-axis conversation becomes much more concrete.
Indexing vs. Continuous Rotary Motion: Know Which One You Actually Need
Many buying mistakes happen because “four-axis” covers two different needs. One need is indexed positioning. The part rotates to a known angle, holds still, and the machine cuts conventionally from there. The other need is continuous rotary interpolation. The rotary axis moves during the cut, supporting wrapped geometry and more complex surface relationships.
| What the Shop Actually Needs | What It Usually Points Toward |
|---|---|
| Side features, angular drilling, repeatable indexed faces | Indexed rotary capability |
| Wrapped contours and coordinated rotary motion during the cut | Stronger continuous four-axis capability |
| Undercuts or tool-angle problems beyond rotary indexing | A broader five-axis discussion |
Many factories need reliable indexing much more often than they need full simultaneous rotary motion. If your parts are essentially prismatic with features on multiple faces, an indexed rotary axis will eliminate the re-clamping waste without the added cost and programming complexity of full simultaneous interpolation. If you are cutting wrapped grooves, spiral features, or cam-like contours, you need the continuous capability and the CAM and postprocessor support that comes with it.
The Strongest Business Case Comes From a Repeat Part Family
Not every visually complex part deserves rotary investment. The strongest case usually comes from repeat families where geometry and setup burden stay linked. Typical strong-fit examples include:
- Cylindrical or partly cylindrical components with repeated angular features
- Long parts that lose too much accuracy when re-clamped by hand
- Multi-face parts where datum relationships matter more than pure removal speed
- Jobs that keep wasting operator time in reorientation rather than cutting
The weakest case usually appears when the buyer is reacting to a few impressive sample parts instead of a stable queue of recurring work. A rotary axis that eliminates two setups on a part you run once a year is a poor investment. The same axis that eliminates two setups on a part you run weekly, with the same datum held throughout, changes the economics entirely.
Rotary Hardware Only Pays If It Holds Confidence Under Load
A quote that only says “rotary included” does not say much. Buyers still need to know how the rotary unit behaves under interrupted or off-center loads, how much table and clearance remain once it is installed, how stable long or imbalanced parts really are, how backlash and repeatability are checked, and what support exists when rotary-specific problems appear after installation.
Four-axis value disappears quickly if the axis adds motion but not trust. A rotary table that flexes under an interrupted cut, or a trunnion that loses position when the part is clamped off-center, will create scrap and rework that quickly offsets the setup savings. Ask the supplier how the rotary axis is braked during indexed operations, what the rated clamping torque is, and how the unit handles the kind of cutting forces your toolpaths actually generate.
Fixture Logic Usually Decides Whether the Purchase Pays Back
Many rotary purchases disappoint because the machine gets all the attention while fixturing stays vague. The right questions are practical: How will real production parts actually be held? Will they need tailstock support? How much overhang will the setup create? Can one fixture concept support a family of parts, or will each new job become a new holding problem?
If the fixture story is weak, the rotary machine may still move impressively while the real route stays fragile and operator-dependent. A rotary axis without a matching fixture strategy simply moves the alignment problem from the machine table to the rotary faceplate. The parts still need to be located, clamped, and verified, and if that process is not repeatable, the four-axis investment will not deliver the setup compression you are paying for.
The Return Comes From Fewer Setups, Not From the Axis Itself
The strongest four-axis ROI case is rarely prestige. It is setup compression. Ask the investment question in production terms: How many setups disappear from the recurring job? How much inspection burden drops when the part stays tied to one datum? How much scrap is currently tied to re-clamping variation? How much operator time is being spent aligning instead of cutting?
If those answers are small, the machine may be unnecessary. If they are large and recurring, the added axis may remove more waste than buyers expect. A part that currently requires three setups, each with its own datum establishment and inspection, can often be completed in one clamping on a four-axis machine. That compression affects not just cycle time but also the indirect labor of setup, the inspection time between operations, and the scrap rate tied to datum drift across multiple clampings.
CAM, Post Support, and Verification Are Part of the Purchase
Four-axis buying is never just hardware buying. The real purchase also includes CAM workflow, postprocessor ownership, verification discipline, and prove-out logic. Buyers should ask early which CAM systems are normal for this machine, who owns the post after installation, how rotary offsets are checked, and how the first representative part family will be proved out.
When quotes use loose phrases such as “rotary-ready” or “simultaneous-capable,” it helps to compare machinery details line by line so the software and support burden is visible instead of assumed. A machine that requires a custom postprocessor you have to develop in-house, or a CAM system your programmers do not know, will add weeks to the implementation timeline regardless of how capable the hardware is.
Sometimes Four-Axis Is Still the Wrong Fix
Some shops reach for four-axis because the route feels inefficient, but the inefficiency is not always rotary-related. If the real pain sits in sheet flow, panel handling, or integrated furniture production, CNC nesting machines may solve more of the bottleneck. If the recurring pain sits in hole patterns, hardware prep, or drilling throughput, a boring and drilling machine may move the business further.
Four-axis pays when geometry-driven setup loss is the recurring tax. It is weaker when the real bottleneck sits elsewhere. Be honest about where the time actually goes. If operators are spending more time moving sheets, staging panels, or waiting on drilling operations than they are re-clamping complex parts, a rotary axis will not fix the production constraint.
What a Good Trial Should Prove
A useful trial should show more than one attractive sample part. It should prove a representative setup condition, measured repeatability across indexed positions or repeated runs, setup time rather than only cut time, inspection logic that matches real acceptance standards, and clear documentation of fixture, post, and operating assumptions.
That is much more valuable than a showroom part that only proves possibility. Ask the supplier to run one of your actual recurring parts, with your fixture approach, and to document the full setup-to-finished-part sequence. Measure the repeatability across multiple runs. Confirm that the postprocessor produces usable code without manual editing. Verify that your operators can load, run, and unload the part without special training. If the trial cannot demonstrate those things, the machine will not perform them in production either.
Beyond the Axis: Machine Stiffness and Spindle Considerations
A four-axis retrofit or new machine purchase changes the load path through the entire structure. When a rotary table or trunnion is added, the workpiece is no longer sitting directly on the machine table with a simple vise or clamp arrangement. The part is now supported through the rotary unit’s bearings, housing, and mounting interface. That chain of components must be stiff enough to handle the same cutting forces you currently apply on a three-axis machine. If the rotary unit is undersized, you will find yourself reducing depth of cut or feed rate to avoid chatter, which quietly erases the productivity gains you expected from eliminating setups.
Spindle selection matters more on four-axis work than many buyers initially realize. When you machine a part in a single clamping with the rotary axis presenting different faces to the tool, the tool engagement angle changes constantly. A spindle with limited torque at low RPM will struggle with heavy roughing passes on large diameters, while a spindle that is too high-speed oriented may not have the low-end grunt needed for stainless or tougher alloys. Match the spindle characteristics to the material and the typical feature sizes in your recurring part family. A machine that is perfectly adequate for aluminum prototypes may be completely wrong for production runs of hardened steel components with large radial features.
Work Envelope and Interference Checking
One of the most overlooked aspects of four-axis selection is the actual work envelope once the rotary unit is installed. A rotary table consumes vertical space, and a trunnion consumes both vertical and horizontal space. The advertised X, Y, and Z travels of the base machine are not the same as the usable envelope with a rotary axis in place. Buyers frequently discover after installation that their longest part, when mounted on the rotary table with a tailstock, does not fit within the machine’s travels. Or the part swings into the machine column during rotation, creating a collision risk that requires reprogramming or fixture redesign.
Before committing to a specific machine, model the worst-case part in your recurring family. Account for the rotary unit’s height, the fixture height, the part’s maximum radius when rotated, and the clearance needed for the tool holder and spindle nose. If the machine has a tool changer, verify that the tool change arm does not interfere with the rotary unit or the workpiece at any point in the travel. Interference checking is not a luxury; it is a fundamental requirement for safe four-axis operation. A machine that cannot accommodate your largest recurring part without collision risk is not a four-axis solution for your shop, regardless of how capable the rotary unit is on paper.
Programming Complexity and Operator Skill Level
Four-axis machining introduces a step change in programming complexity. On a three-axis machine, the CAM programmer thinks in terms of planar toolpaths and simple Z-level finishing. With a fourth axis, the programmer must understand rotary motion, tool orientation relative to the rotating part, and the relationship between angular position and linear feed. The postprocessor must correctly convert the CAM output into rotary axis commands, including the proper direction of rotation, the shortest path between angles, and the handling of rotary axis unwinding for continuous motion.
Operator skill is equally important. A three-axis operator can usually load a part, zero the tool, and run with minimal training. A four-axis operator needs to understand how to set the rotary zero position, how to verify that the part is concentric with the rotary axis, and how to recognize when the rotary axis is losing position. If your shop does not currently have anyone with four-axis experience, factor in the cost of training or hiring. The machine will not run itself, and the learning curve for four-axis operation is steeper than many buyers anticipate. A machine that sits idle because no one can program or operate it effectively is a worse investment than no machine at all.
Maintenance and Long-Term Reliability of Rotary Units
Rotary axes are mechanical systems with bearings, gears, worm drives, or direct-drive motors. They wear, they lose adjustment, and they require periodic maintenance. Unlike a linear axis that moves in a straight line with relatively predictable loads, a rotary axis experiences varying loads depending on the part position and the cutting forces at any given moment. The rotary unit’s braking system, which holds the axis stationary during indexed operations, is a wear item that will eventually need adjustment or replacement.
Ask the supplier about the expected service life of the rotary unit, the recommended maintenance schedule, and the availability of spare parts. A rotary unit from an obscure manufacturer with no local distributor can become a costly downtime problem when a bearing fails or an encoder needs replacement. Check whether the rotary unit is a standard product from a well-known manufacturer or a custom integration that only the machine builder can service. The long-term reliability of the rotary axis is just as important as the initial purchase price, and buyers who ignore maintenance considerations often face unexpected repair bills within the first few years of operation.
Comparing New Machines vs. Retrofitting Existing Equipment
Some shops consider retrofitting an existing three-axis machine with a bolt-on rotary table rather than purchasing a new four-axis machine. This approach can work for indexed applications where the rotary table is used for positioning and the machine’s existing controller can handle the additional axis. However, retrofits have limitations. The machine’s original controller may not support simultaneous four-axis interpolation, which means continuous rotary motion is not possible. The mechanical interface between the rotary table and the machine table must be rigid enough to maintain accuracy, and the existing machine’s structure may not have been designed to handle the additional loads imposed by rotary work.
For shops that need indexed positioning only, a retrofit can be a cost-effective solution. For shops that need continuous four-axis capability, a new machine with a controller and postprocessor designed for simultaneous motion is usually the better choice. The retrofit route also requires careful consideration of the electrical interface, the safety interlocks, and the potential for voiding the original machine’s warranty. If you are considering a retrofit, ask the rotary table manufacturer for examples of successful installations on your specific machine model, and verify that the controller can actually handle the additional axis before committing to the purchase.
Workholding Accessories That Extend Four-Axis Capability
The rotary axis itself is only the beginning. A complete four-axis workholding strategy often includes tailstocks for long parts, steady rests for slender workpieces, collet chucks for round stock, and custom fixtures for irregular shapes. Tailstocks are particularly important for parts that are longer than the rotary table’s clamping capacity. Without a tailstock, a long part will deflect under cutting forces, causing taper and dimensional errors. The tailstock must be aligned with the rotary axis centerline, and the alignment must be verified periodically as the machine is used.
Steady rests are useful for slender parts that would otherwise vibrate or deflect during machining. They support the part at intermediate points along its length, reducing deflection and improving surface finish. Collet chucks provide quick and repeatable clamping for round stock, which is a common workholding solution for cylindrical parts. Custom fixtures are often necessary for complex parts that do not fit standard workholding solutions. The cost of these accessories should be included in the four-axis purchase decision, as they can add significantly to the total investment.
Measuring and Verifying Four-Axis Accuracy
Accuracy verification for a four-axis machine is more complex than for a three-axis machine. In addition to checking linear axis positioning, you must verify the rotary axis positioning accuracy, the repeatability of the rotary axis, and the relationship between the rotary axis and the linear axes. A common test is to machine a part with features at known angular positions and then measure the part on a CMM to verify that the features are at the correct angles. Another test is to machine a cylindrical part and measure its roundness to verify that the rotary axis is concentric with the spindle.
The rotary axis’s backlash is a critical parameter. Backlash is the amount of play in the drive system when the direction of rotation is reversed. Excessive backlash causes positional errors when machining features on both sides of the rotary zero position. Ask the supplier for the backlash specification and verify it during the trial. The rotary axis’s clamping torque is also important. When the axis is clamped during indexed operations, it must hold the part rigidly against cutting forces. If the clamping torque is insufficient, the part will move during machining, causing scrap.
Making the Final Decision: A Checklist for Buyers
When you have narrowed down your options, use a structured checklist to compare machines and suppliers. The checklist should cover the following areas:
- Rotary axis type: indexed, continuous, or both
- Rotary axis capacity: maximum part weight, maximum part diameter, maximum part length
- Rotary axis accuracy: positioning accuracy, repeatability, backlash
- Rotary axis clamping: braking system, clamping torque, holding rigidity
- Machine envelope: usable work envelope with rotary unit installed, clearance for tool changer
- Spindle: power, torque, speed range, suitability for your materials
- Controller: support for four-axis interpolation, ease of programming, postprocessor availability
- CAM compatibility: which CAM systems are supported, who owns the postprocessor
- Fixture strategy: tailstock availability, steady rest options, custom fixture support
- Maintenance: service interval, spare parts availability, local distributor support
- Trial results: measured repeatability, setup time reduction, part quality
A four-axis machine is a significant investment that should pay for itself through reduced setup time, improved accuracy, and lower scrap rates. The decision should be driven by data from your own production floor, not by marketing materials or showroom demonstrations. If the numbers support the purchase, a four-axis machine can transform your shop’s capability for complex part machining. If the numbers do not support it, the money is better spent elsewhere in your production process.
For shops that are ready to move forward, reviewing the available machinery options from a supplier that understands both the hardware and the production context is a practical next step. A machine that fits your part family, your operator skill level, and your maintenance capabilities will deliver the setup compression and accuracy improvements you are paying for. The right four-axis machine is not the most expensive one or the one with the most features; it is the one that eliminates the specific waste in your recurring production jobs and holds the accuracy your parts require.