Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
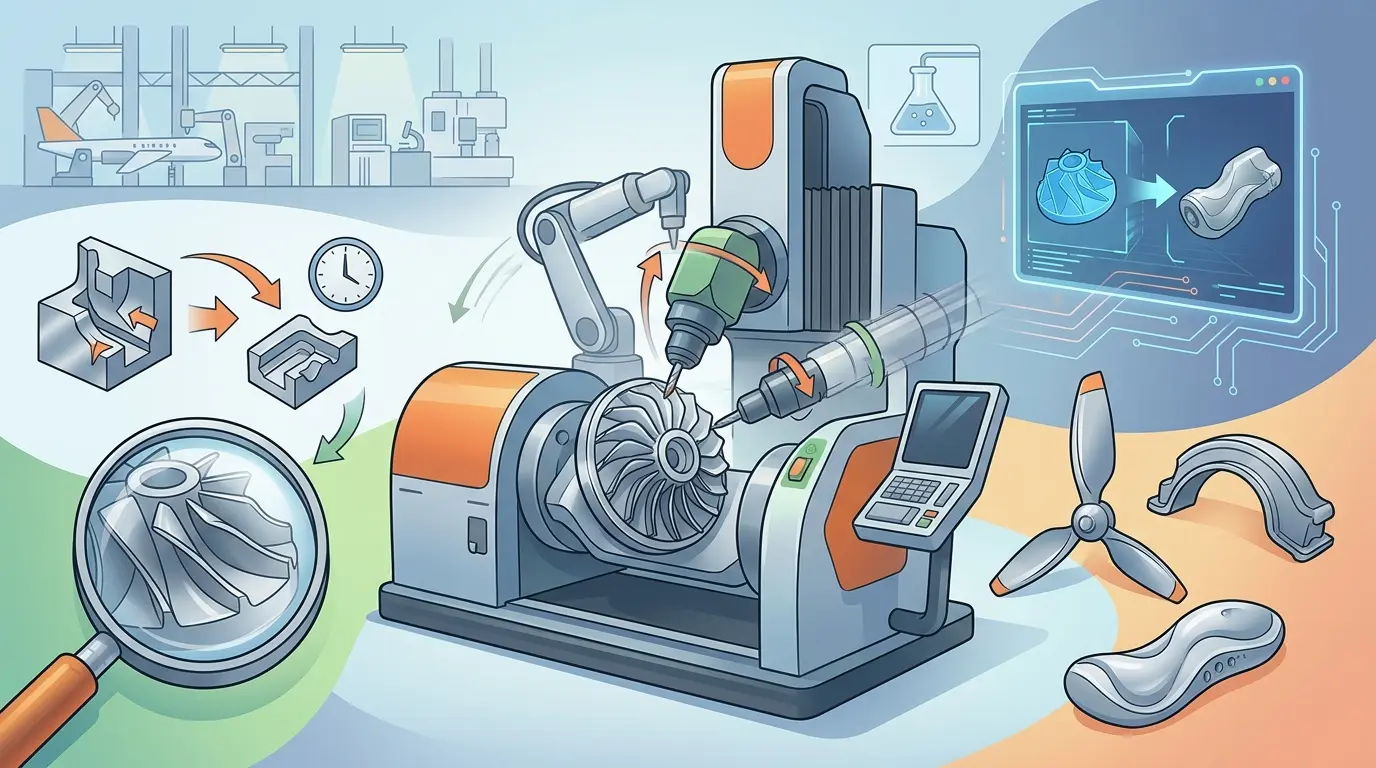
Five-axis CNC capability is rarely a technology upgrade; it is a response to a specific cost problem. When recurring parts force repeated reclamping, unstable long tool stick-out, or hand correction on compound geometry, the vertical-only route starts consuming labor hours and scrap risk that simpler equipment cannot recover. The decision hinges on distinguishing indexed 3+2 positioning from full simultaneous motion, because overbuying continuous capability without the programming discipline, validated postprocessors, and rigid low-profile fixturing it demands will quietly turn the investment into an expensive monument. Match the axes to the actual part mix before committing capital.
When the Vertical-Only Route Starts Costing Real Money
Five-axis CNC machining earns its place on the shop floor when the part itself becomes expensive to keep vertical. The decision rarely starts with a desire for more axes. It starts with a production problem: repeated reclamping, unstable long tools, awkward access angles, or hand correction on compound geometry that keeps eating labor hours.
If those conditions describe your recurring work, five-axis can remove genuine production pain. If your parts already run cleanly on simpler equipment, adding two rotary axes may create more engineering burden than useful gain. The key is knowing which situation you are actually in before you commit capital and floor space.
What Problems Usually Push a Shop Toward Five-Axis
The need for five-axis capability typically appears when one or more of these conditions starts showing up in your cost numbers:
- Several faces must stay related to one another within tight tolerances.
- The feature sits at an angle or deep inside the part where vertical access is blocked.
- Tool stick-out becomes too long to stay stable at required feed rates.
- Surface quality matters across changing contours that a fixed orientation cannot reach cleanly.
- Fixturing keeps multiplying because access keeps changing between operations.
Five-axis helps because it changes orientation instead of forcing the entire machining route to stay trapped in one vertical approach. That single capability cascades into setup time, tool life, surface finish, and inspection burden.
Consider a typical scenario in a woodworking shop that produces contoured architectural components. On a three-axis machine, a curved rail with angled tenons requires at least three separate setups: one for the face, one for each angled end. Each setup introduces alignment error, and the operator must re-establish datums every time. The same part on a five-axis machine can be completed in a single clamping, with the rotary axes positioning the workpiece for each angled cut. The cycle time may not drop dramatically, but the indirect labor and scrap risk do.
Separate Indexed 3+2 From Full Simultaneous Five-Axis
This distinction matters early in the evaluation, because it determines what you actually need to buy and program.
Some parts only need indexed positioning. The rotary axes move to an angle, lock, and the cut proceeds like a controlled three-axis operation. This is often called 3+2 machining. Other parts genuinely need continuous orientation during the cut, with all five axes moving together to follow a compound surface.
| Part Situation | What Usually Helps Most |
|---|---|
| Multi-face work with known access angles | Indexed 3+2 often delivers most of the value |
| Compound contours and orientation-sensitive surfaces | Simultaneous five-axis matters more |
| Simple prismatic work with stable fixtures | Simpler machines usually remain more economical |
Many shops overbuy here. They pay for continuous five-axis capability when the real daily win would have come from better setup reduction on indexed work. A 3+2 machine with a solid postprocessor and good probing can handle a large share of multi-face work without the programming complexity of full simultaneous motion.
The programming difference is substantial. Indexed 3+2 work can often be programmed with standard three-axis toolpaths that are simply rotated into different orientations. The CAM system does not need to calculate continuous tool-axis vectors or manage the complex collision avoidance that simultaneous motion requires. This means a shop with experienced three-axis programmers can usually transition to 3+2 with modest additional training. Full simultaneous five-axis programming, by contrast, demands a deeper understanding of tool-axis control, surface normal vectors, and machine kinematics.
The First Payback Usually Comes From Fewer Setups
Five-axis is often sold as a motion story, but on the floor it usually pays back first as a setup story. When a part can stay in one better-controlled setup instead of moving through several weaker ones, the shop usually gains:
- Less handling time between operations.
- Less alignment risk from re-fixturing.
- Less inspection burden from re-establishing datums.
- Better protection of feature relationships across faces.
If your current route already burns time re-establishing datums and rechecking relationships between features, the value of five-axis may be visible before anyone even measures cycle time. The reduction in indirect labor and quality risk often outweighs the raw cutting speed gains.
Let us put some numbers on this. A typical multi-face part that requires three setups on a vertical machine might consume 20 minutes of setup time per operation, plus 10 minutes of inspection between operations. That is 90 minutes of non-cutting time per part. On a five-axis machine with a single setup, the same part might require 30 minutes of setup and 10 minutes of inspection. The 50 minutes saved per part may not sound dramatic, but across a batch of 50 parts, that is over 40 hours of recovered capacity. In a shop running two shifts, that is nearly a full week of productive machine time reclaimed from handling and verification.
Tool Approach Improves When Orientation Improves
Many parts become difficult not because the material is impossible to cut, but because the cutter approaches from a poor angle on a vertical-only route. An overlong tool forced into an awkward position usually brings chatter, shorter tool life, and weaker surface control.
Five-axis helps when it lets the tool or workpiece tilt into a shorter, calmer, more natural cutting posture. That often means:
- More stable finish quality across the cut.
- Less tool deflection under load.
- Better tool life because the cutter engages more favorably.
- Less need to cut conservatively just to avoid trouble.
This is not a theoretical advantage. On deep pockets, angled features, and contoured edges, the difference between a stable short tool and a deflecting long tool shows up directly in scrap rates and rework hours.
Consider a deep pocket in a mold base. On a three-axis machine, the tool must reach the bottom of the pocket with a long stick-out. The extended tool deflects under cutting load, producing tapered walls and poor surface finish at depth. The programmer compensates by reducing feed rates and taking lighter passes, which extends cycle time. On a five-axis machine, the workpiece can be tilted so the tool approaches the pocket wall at a more favorable angle, allowing a shorter, stiffer tool to do the work. The result is faster cutting, better finish, and longer tool life.
Surface Quality Can Improve, But Only With Discipline Around It
On sculpted surfaces, contoured edges, molds, and shaped wood or stone parts, five-axis can reduce the amount of hand correction required later. The machine can maintain a more consistent tool engagement angle across the surface, which produces a more uniform finish.
But that benefit is conditional. Tool libraries, holder definitions, step-over strategy, post behavior, probing, and machine calibration still decide whether the theoretical finish quality appears on the real part. Five-axis improves the opportunity for a better finish. It does not replace process discipline.
If your CAM data is incomplete, your holders are poorly modeled, or your postprocessor has not been validated against the actual machine kinematics, the finish quality will suffer regardless of how many axes are moving.
A common failure mode appears in shops that purchase a five-axis machine and immediately attempt simultaneous finishing passes on contoured parts. The CAM system generates toolpaths that look correct on screen, but the postprocessor has not been tuned to the machine’s specific rotary axis configuration. The result is a surface with visible tool marks or scalloping that requires extensive hand finishing. The shop then blames the machine, when the real problem was an unvalidated postprocessor and incomplete tool holder models in the CAM system.
Better Access Does Not Remove the Need for Better Fixtures
With five-axis, fixtures usually need to be rigid, low-profile, and digitally trustworthy. They must support the part without blocking the angles the machine needs to reach. Five-axis can reduce fixture count or setup changes without making fixture thinking optional.
If workholding stays weak, extra axis freedom disappears quickly into vibration, blocked access, or too much manual setup judgment. A five-axis machine with poor fixturing will chatter, lose position, and produce inconsistent results just like any other machine with poor fixturing, only with more expensive consequences.
The fixture design challenge is different on a five-axis machine. A conventional vise or clamp that works perfectly on a three-axis machine may block the rotary axis from reaching the required angle. The fixture must be designed with the full range of motion in mind, which often means lower-profile clamps, custom soft jaws, or vacuum fixturing that holds the part from below rather than from the sides.
The Main Limits Usually Come From Engineering Readiness
The machine can be installed quickly. Stable five-axis production usually cannot. Reliable five-axis output depends on:
- CAM strategy that matches the machine’s actual kinematics.
- Proven postprocessors validated against real cuts.
- Accurate tool and holder models in the CAM system.
- Strong collision verification before programs reach the floor.
- Controlled program release with clear ownership.
If those systems are weak, the machine often becomes underused because the team avoids risk except on a narrow slice of work. The machine sits idle while simpler equipment handles the majority of jobs, and the investment never pays back.
The collision risk deserves particular attention. On a three-axis machine, the toolpath is relatively easy to visualize, and most collisions are obvious from the program geometry. On a five-axis machine, the tool can collide with the workpiece, the fixture, or the machine itself in ways that are not visible in a standard toolpath view. Robust simulation software is not optional; it is a prerequisite for safe five-axis operation. Shops that skip this step often learn the lesson through a crashed spindle or a damaged workpiece.
Strong Use Cases Share the Same Pattern
Five-axis is strongest when geometry is difficult and the cost of getting it wrong is high. Typical strong cases include:
- Sculpted tooling and mold surfaces.
- Blades, impellers, and flow-path geometry.
- High-value prototypes with changing geometry.
- Multi-face precision parts where relationships matter.
- Contoured architectural wood components.
- Complex stone forms such as basins or multi-face details.
What ties these together is not industry. It is the cost of awkward access and the value of preserving geometry in fewer setups. When a part is expensive to make and difficult to reach, five-axis earns its keep.
In the stone fabrication sector, for example, a sculpted basin with an integrated drain channel and angled outer profile is nearly impossible to produce economically on a three-axis machine. The operator would need to reposition the stone multiple times, and each repositioning risks chipping or misalignment. A five-axis stone machine can cut the entire form from a single block, maintaining the relationship between the interior bowl, the drain channel, and the outer profile. The result is a higher-quality product with less labor and less material risk.
Where Five-Axis Is Usually Overkill
Five-axis is usually weaker when the daily work is mostly flat panels, routine pockets, standard profiles, or simple repeated shapes that already fit stable fixtures. It is also often overkill when:
- The current route is already stable on simpler equipment.
- The part family rarely needs changing tool angles.
- Tolerance and finish demands are already met without reclamping pain.
- Programming capacity is too limited to support more complex release discipline.
For many shops, that matters a great deal. If the dominant workload is still flat sheet processing, routing-and-drilling integration on CNC nesting machines may create more daily value than a five-axis investment. In stone fabrication, if the work is still mostly straightforward cutouts and repeat profiling, a simpler route through stone CNC machines may be easier to adopt and keep productive.
The economics are straightforward. A five-axis machine costs significantly more than a comparable three-axis machine, and the programming and maintenance burden is higher. If the part mix does not require the extra axes, the machine becomes an expensive way to do work that a simpler machine handles just as well. The capital that went into the five-axis purchase could have been spent on additional three-axis capacity, better tooling, or automation that directly addresses the actual bottleneck.
Staffing and Process Ownership Matter More Than Brochures Admit
Five-axis productivity depends on who owns CAM strategy, who proves out risky programs, who maintains tool and holder data, and who decides when a part is ready for release. If those responsibilities are scattered across too few people, the machine may become politically impressive but operationally cautious.
That is not a reason to avoid five-axis automatically. It is a reason to judge readiness honestly. A five-axis machine without a dedicated programmer who understands simultaneous motion, collision avoidance, and postprocessor behavior will not deliver the results the brochure promises.
The staffing question is often the one that shops underestimate. A three-axis machine can be programmed by someone with basic CAM training and a few years of experience. Five-axis programming requires a deeper understanding of tool-axis control, surface geometry, and machine kinematics. The programmer must also be comfortable with simulation software and postprocessor configuration. If your shop does not have that person on staff, you need to budget for training or hiring before the machine arrives.
A Practical Reality Test Before Saying Yes
Ask one direct question of the current workload: which recurring parts become meaningfully cheaper, calmer, or more accurate if the machine can change orientation during the cut or between faces?
If the answer is vague, five-axis is probably being discussed too early. If the answer points clearly to setup reduction, tool stability, surface control, or access on specific valuable parts, five-axis may be justified.
It also helps to ask the reverse question: which parts would still run just as well on simpler equipment even after the five-axis machine arrives? That reverse view stops buyers from turning occasional hard jobs into a broad argument for daily over-complexity.
The right decision comes from matching machine capability to the actual part mix, not from the appeal of having more axes available. If the parts justify it, five-axis will pay back through fewer setups, better tool life, and reduced rework. If they do not, the extra engineering burden will quietly consume the productivity gains it was supposed to create.
What Actually Drives the Cost of 5 Axis CNC Machining Explained
The purchase price of a five-axis machine is only the beginning. Shops that budget only for the machine itself often find themselves surprised by the associated costs that follow. These include:
- CAM software upgrades or additional seats for five-axis programming.
- Postprocessor development and validation, which can take weeks of engineering time.
- Simulation software licenses for collision verification.
- Probing systems and calibration routines to maintain accuracy across all five axes.
- Tooling and holders designed for five-axis work, which may differ from existing inventory.
- Training for programmers and operators, both initial and ongoing.
These costs can add 20 to 40 percent to the total investment over the first year. Shops that ignore them often find themselves with a machine that runs at 30 percent utilization because the support systems were never funded.
Maintenance and Calibration Considerations
Five-axis machines have more moving parts than their three-axis counterparts, and each additional axis introduces another potential failure point. The rotary axes, in particular, require regular calibration to maintain positioning accuracy. A machine that was accurate to within a few microns when new can drift significantly if the rotary axes are not periodically checked and adjusted.
The calibration routine typically involves machining a test part with known geometry, measuring the results, and comparing them to the expected values. Any deviation is then corrected through the machine’s compensation tables. This process should be performed on a regular schedule, not just when problems appear.
Shops that run three-axis machines on a “fix it when it breaks” maintenance philosophy will need to change their approach. Five-axis machines reward proactive maintenance, and the cost of a calibration failure is often a scrapped part or a damaged spindle, not just a minor adjustment.
Software Integration and Data Flow
The software ecosystem around a five-axis machine is more demanding than for simpler equipment. The CAM system must generate toolpaths that respect the machine’s kinematics, the postprocessor must convert those toolpaths into correct machine code, and the simulation software must verify that the program will run without collisions.
This data flow must be reliable and well-documented. If the CAM system is updated but the postprocessor is not, the machine may receive incorrect code. If the tool library is not maintained, the simulation may show a tool that does not match the one actually loaded in the spindle. Each of these failures can result in a scrapped part or a damaged machine.
Shops that already have strong data management practices will find the transition easier. Shops that rely on informal communication between programmers and operators will need to formalize their processes before five-axis work becomes routine.
Make the 5 Axis CNC Machining Explained Decision
The decision to invest in five-axis machining should come from a clear understanding of your part mix, your engineering capacity, and your willingness to invest in the supporting systems. The machine itself is only one component of a successful five-axis operation.
Start by auditing your current workload. Identify the parts that cause the most pain in terms of setups, tool stability, surface quality, or access. Estimate the cost of that pain in labor hours, scrap, and rework. Then compare that cost to the investment required for five-axis capability, including the machine, software, training, and maintenance.
If the numbers work, five-axis is a legitimate investment. If they do not, the machine will become an expensive monument to a decision that was made on enthusiasm rather than analysis. The shops that succeed with five-axis are the ones that treat it as a production system, not just a machine purchase. They invest in the people, the software, and the processes that make the extra axes productive. That is the difference between a machine that pays for itself and one that quietly consumes the budget.