Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
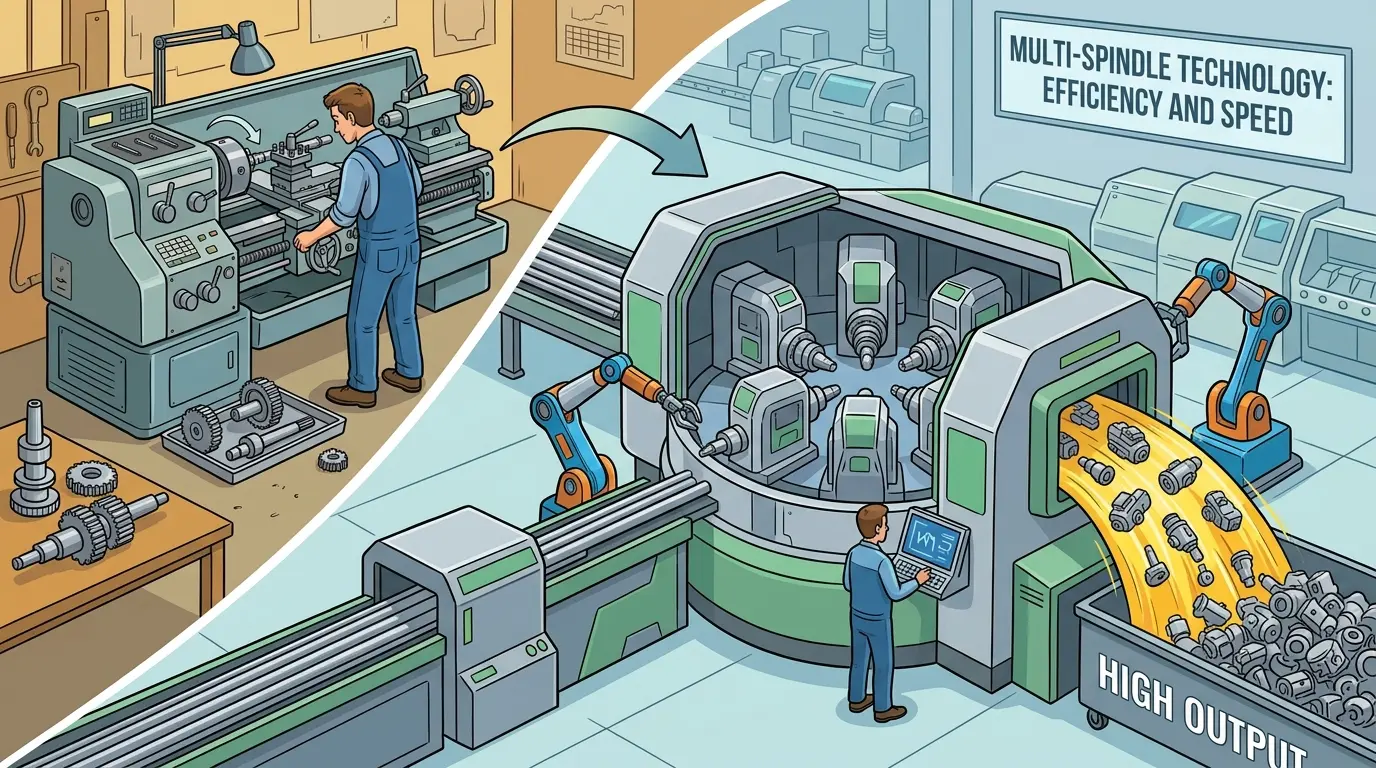
Index multi-spindle machines promise dramatic cycle-time compression, but that headline throughput only pays off when your order book, tooling discipline, and changeover routines are built for sustained repetition. This article walks production engineers and factory managers through the real justification logic: matching the machine to a stable part family, pricing the hidden tooling and setup burden, and verifying that a genuine bottleneck—not demo-floor fascination—drives the capital decision. Before you commit to high-volume infrastructure, you need a clear fit test that separates genuine economic fit from an expensive mistake.
What an Index Multi-Spindle Machine Actually Buys You
The economic case for an index multi-spindle machine rests on one idea: time compression. Instead of a single spindle executing every operation in sequence, the workpiece moves through multiple indexed stations where different tools work in parallel within the same cycle. The result is dramatically lower cycle time per piece on the right part family.
That last qualifier matters more than any headline output figure. Index multi-spindle machines are not general-purpose CNC upgrades. They are volume infrastructure. Their value depends on repetition—stable geometry, predictable demand, and disciplined tooling. When those conditions hold, the economics are compelling. When they do not, the machine becomes one of the most expensive mistakes a shop can make.
The Demand Profile Comes First, Not the Machine
Before any conversation about spindles, stations, or cycle times, the buyer needs to answer a blunt question: does the order book actually feed this machine?
The ideal candidate workload looks like this: a stable part family with long recurring runs, limited engineering changes, predictable material, and standardized tooling. The machine needs enough repetition to amortize the engineering effort, tooling packs, setup time, and organizational discipline required to keep all stations running correctly.
A high-mix shop with frequent design revisions, unstable schedules, and varied workholding will likely lose efficiency. Changeover and tooling preparation will consume the day. The machine becomes a very powerful answer to a production question the factory is not actually asking.
The safest justification model uses confirmed demand, not the most optimistic sales forecast. How many parts per month truly fit the machine’s ideal lane? How many of those parts will remain stable for several years? How much engineering change is typical? How much time will be lost to conversion, tooling reset, first-article proving, or station recovery?
Multi-spindle returns are highly sensitive to utilization. A plant can be impressed by demo-cycle output and still fail to earn the investment if repeat volume comes in lower or more volatile than planned. Conservative demand assumptions should be the baseline; extra volume is upside, not the reason the project works.
Tooling Is the Hidden Factory Inside the Machine
The visible machine gets the attention, but the tooling strategy determines whether it delivers. Multi-spindle productivity depends on repeatable tool packs, standardized station logic, predictable wear behavior, and replacement discipline.
That means tool-life policies need to exist before launch. Replacement timing needs to be understood. Spare tooling needs to be stocked. Setup references and station assignments need to stay stable. In practice, a multi-spindle machine asks the organization to industrialize tooling behavior, not just part output.
Many buyers underestimate this commitment. They price the machine and forget to price the discipline around it. The seconds saved in cycle time then disappear into setup confusion, inconsistent wear handling, and delays around station preparation.
Changeover Is the Real Economic Enemy
On the right part family, parallel operations strip seconds aggressively out of each cycle. On the wrong mix, those saved seconds vanish into hours of preparation. Changeover is the central risk variable.
If the next job needs different tooling arrangements, different references, different guide components, or different station logic, the plant has to convert cleanly and confidently. Shops without standardized changeover methods often discover that a more flexible single-spindle CNC lathe, Swiss machine, or machining center outperforms the multi-spindle investment in real calendar time simply because it absorbs change more gracefully.
Analyze not only cycle time but also changeover frequency, setup labor, engineering overhead, and the true cost of switching from one repeat family to another. Seconds saved during cutting do not matter if the machine spends the rest of the day trying to become the next machine.
High Output Concentrates Risk
Fast output creates concentrated risk. If the machine stops, a meaningful portion of daily output disappears at once. Support readiness matters far more than many buyers expect.
Night-shift coverage, spare-part availability, diagnostic skill, preventive maintenance routines, and tooling rebuild discipline all deserve attention before the purchase. These systems do not forgive neglect well. Their value comes from sustained output, so downtime has larger economic consequences than on lower-intensity equipment.
Ask who will maintain the machine, how spares will be stocked, and how the organization will respond when wear, station timing, or tooling events begin to appear. Capacity lives in the machine plus the people and systems that keep it running correctly.
Quality Control Gets Amplified in Both Directions
Index multi-spindle systems can deliver very strong repeatability because the process is highly structured. Once tooling, timing, and references are stabilized, the machine can produce large quantities of consistent parts efficiently. That is a real advantage.
But repeatability depends on control, not architecture alone. If the blank varies, tooling drifts, a station wears unpredictably, or maintenance is deferred, the machine will repeat the same problem at very high speed. The cost of poor control rises with output rate.
Fast output amplifies good process governance and bad process governance equally. This is another reason multi-spindle investment belongs in mature production settings.
Labor Structure Changes, and Not Always in the Obvious Direction
Multi-spindle economics are often discussed as though the machine automatically reduces labor cost. That is too simple. The machine may reduce labor per finished part, but only if the plant can reorganize around that reality.
If the machine still requires highly specialized setup labor, off-line tooling prep, repeated inspection intervention, or engineering support for frequent conversions, the labor story changes. What labor disappears? What labor becomes more specialized? What labor moves upstream into tooling preparation, scheduling, and maintenance planning?
A machine that reduces operator touches but increases hidden support burden may still be worth it, but only if the business models that correctly.
A Practical Fit Test for Candidate Part Families
Describe the candidate workload in one sentence. If it sounds like “high volume, stable geometry, repeat orders, limited changes, predictable material, and standardized tooling,” the machine is in the right conversation. If it sounds like “mixed work, frequent revisions, short runs, and recurring setup improvisation,” the machine is in the wrong lane.
Multi-spindle equipment is best when the part family already wants industrial repetition. The machine does not create that condition. It exploits it.
Justification Matrix: Separating Genuine Fit from Fascination
| Signal | What It Usually Means |
|---|---|
| Stable part family with long recurring runs | Strong case for multi-spindle consideration |
| Frequent design changes or mixed short batches | High risk of losing value to changeover |
| Standardized tooling and setup discipline | Better chance of capturing cycle-time gains |
| Strong maintenance coverage and spare planning | Higher chance of protected uptime |
| Quality system already supports repeat production | Better chance of sustaining output without drift |
| Shop still relies on heroic setup knowledge | Weak foundation for multi-spindle economics |
| Demand model based on one optimistic forecast | High financial risk |
Scheduling Logic Has to Match the Machine’s Rhythm
Multi-spindle equipment wants a cleaner planning rhythm than many mixed shops naturally provide. If upstream material supply is inconsistent, downstream inspection is overloaded, or customer release patterns change every few days, the machine’s theoretical throughput becomes harder to capture. A system built for repetition cannot perform at its best when the rest of the factory treats every week like a fresh emergency.
The plant does not need perfect scheduling before the investment. It needs enough production discipline for the machine to stay in its lane. If planners keep forcing unstable work into the asset because the machine is expensive and “should be used,” the economics deteriorate. The machine becomes busy, but not necessarily profitable. Good scheduling protects the machine from misuse as much as it feeds it with work.
Capital Should Follow the Real Bottleneck
Multi-spindle investments often look compelling because the output number is dramatic. But capital should follow the verified constraint, not the most impressive demonstration. If the current bottleneck is tooling prep, inspection delay, material inconsistency, or weak demand visibility, the multi-spindle machine sits downstream of the wrong problem. The investment creates motion without solving the actual limitation.
Map the whole value stream before committing. Where is the true delay? Which step is throttling shipment? Can the organization actually exploit a step-change in part output, or will the next process absorb the gain and turn it into queue time? A multi-spindle purchase is strongest when it relieves a verified bottleneck inside a stable product family. It is weakest when it is expected to rescue a factory that still has more basic process problems upstream.
Build a Pilot Logic Before Building a Purchase Narrative
The safest plants identify one or two part families that would clearly live on the machine, define the expected tooling package, estimate realistic changeover burden, and model how inspection and maintenance would support the asset. That exercise often reveals whether the machine belongs in the plant now or belongs on a future roadmap after more groundwork is done.
Multi-spindle success is rarely accidental. It comes from plants that know exactly what the first production lane will look like. They are not buying generalized speed. They are buying a very specific throughput advantage for a very specific class of work. Buyers who cannot describe that first lane clearly are still too early, no matter how attractive the headline cycle time looks.
What to Demand in a Serious Supplier Conversation
Ask the supplier to show what a real changeover looks like, not just what the machine does during a stable demonstration. Ask how tooling is prepared between part families. Ask which spare parts are critical enough to keep on-site. Ask how training is handled for off-shift coverage. Ask how long it typically takes to recover from a station fault, a tooling event, or a timing issue.
Strong answers sound practical and specific. Weak answers drift back toward generalized output language. For equipment this specialized, the practical answers matter much more.
When Another Process Is the Better Investment
If demand is volatile, part families are unstable, or the production challenge is really about flexibility rather than extreme piece-rate output, another process may be better. Single-spindle CNC lathes, Swiss-type machines, machining centers, or even outsourced capacity can outperform a multi-spindle plan when the plant does not have enough stable work to keep the machine in its ideal lane.
The same principle appears across manufacturing. Buyers comparing high-volume efficiency against flexibility often discover that the smarter decision is really about line design rather than maximum single-machine output. Automation pays when the surrounding process is ready for it.
The Bottom Line on Index Multi-Spindle Investment
Index multi-spindle machines justify their cost when output volume is high, geometry is stable, tooling is standardized, and the plant can support rigorous setup and maintenance behavior. They are poor choices when buyers need flexibility but are drawn to impressive throughput numbers.
The right decision is not based on how exciting the machine looks in a demo. It is based on whether the organization can feed it, change it, maintain it, and protect it well enough to turn parallel operations into real financial return. Buyers who work through that logic first—demand stability, tooling discipline, changeover burden, maintenance readiness, and bottleneck verification—will make the right call. Buyers who skip that work will own a very fast machine that cannot earn its keep.