Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
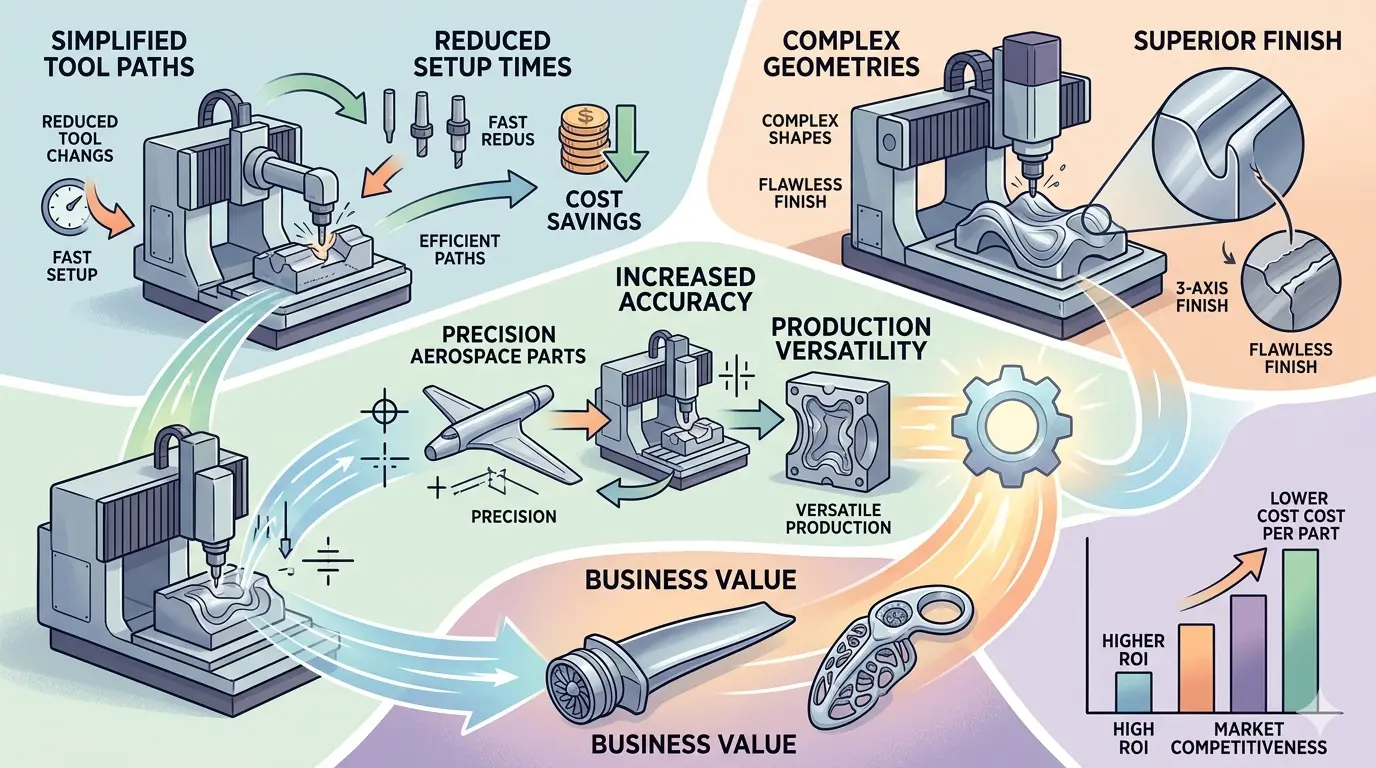
Before you approve a six-axis CNC purchase, the axis count itself is not the business caseâthe penalty it removes is. This article forces buyers to separate machining value from handling value, asking whether the sixth axis actually eliminates a measured setup step, a manual flip, or idle spindle time, or whether it simply adds programming and calibration burden. For furniture, panel, and stone shops, the decision hinges on naming the specific recurring loss and pricing simpler alternatives first. If you cannot quantify what disappears, the extra motion is likely ahead of your factory’s real need.
Start With The Penalty, Not The Axis Count
Six-axis CNC machines only make commercial sense when the extra motion removes a penalty the factory can already measure. If the current route keeps paying for manual flips, repeated re-clamps, awkward repositioning, or too much idle time between operations, the sixth axis may have a real job. If the pain is still vague, the extra axis is usually being asked to solve a process problem that belongs somewhere else.
The first discipline is to resist the brochure. Axis count is a specification, not a business case. A machine with six axes can be the right answer for one shop and a costly mistake for another, even when they run similar parts. The difference is not the machine. It is the clarity of the production data behind the purchase request.
First Clarify What The Supplier Is Calling The Sixth Axis
Suppliers do not always count axes the same way. Sometimes the sixth axis participates directly in machining. Sometimes it mainly positions the part. Sometimes it belongs more to the handling system than to the cutting kinematics.
The first screening step is simple:
- Which axes interpolate during cutting?
- Which axes move only between cuts?
- Does the sixth axis solve geometry, handling, or both?
Without those answers, buyers are not comparing like with like. A machine with a rotary table that indexes between operations is not the same proposition as one with full simultaneous six-axis interpolation, even if both are sold under the same label.
Consider a typical panel-processing environment. A nesting machine with a rotary table might be described as having extra motion, but the rotary function exists to present a new sheet or to flip a panel for second-side work. That is handling value, not machining value. The spindle still cuts in the same three linear axes. Compare that with a stone machining center where the additional rotary axis actually moves the workpiece during a contour cut, changing the tool engagement angle and the surface finish. Those are fundamentally different machines with different programming requirements, different maintenance profiles, and different payback logic.
The Sixth Axis Usually Has To Earn Its Keep In One Of Three Ways
An extra axis tends to make financial sense only when it improves one of these conditions:
- Setup compression. The axis eliminates a clamp, a fixture, or a separate operation.
- Handling reduction. The axis removes a manual flip, a crane lift, or a risky reorientation.
- Better spindle utilization. The axis keeps the spindle cutting longer by reducing dead time between operations.
If the proposed sixth axis does not remove one of those penalties clearly, the value case is weak. The machine may still be a fine piece of equipment, but it is not solving the problem the factory actually has.
Take a furniture component that currently requires three setups. The part is machined on the top face, flipped, machined on the bottom face, then moved to a separate station for an angled drilling operation. Each setup change costs 15 minutes of labor plus the risk of misalignment. If a six-axis machine can hold the part once and complete all three operations in a single cycle, the math is straightforward. The question is whether the machine actually delivers that capability or whether the supplier is describing a machine that still requires manual intervention between operations.
Do Not Assume A Sixth Axis Automatically Means Better Machining
One of the most common buying errors is assuming that a sixth axis is simply a better five-axis machine. Sometimes it is not. Sometimes it adds positioning options or handling support without changing cut quality in the way buyers expect.
The blunt question is: what is the current five-axis or multi-axis route already failing to do? If the geometry is already reachable and the part still runs slowly because of loading, flipping, or staging, the sixth axis may be solving a handling problem rather than a cutting problem. That distinction matters because the two solutions carry different costs, different programming burdens, and different maintenance profiles.
Consider a cabinet door with a decorative profile on the front edge. A five-axis machine can reach that profile without difficulty. The bottleneck is that the door must be flipped to machine the back face, and the flip requires a second operator or a crane for larger doors. The sixth axis might eliminate the flip by rotating the workpiece in the machine. That is genuine value, but it is handling value. The cutting itself was never the problem.
The reverse situation is more dangerous. A shop buys a six-axis machine hoping it will solve a surface finish problem on a complex contour. The real issue is tool selection, spindle speed, or feed rate. The sixth axis adds cost and complexity without addressing the actual defect. The shop would have been better served by a faster spindle, better tooling, or a more rigid five-axis platform.
Separate Machining Value From Automation Value
One common mistake is blending cutting complexity and automation value into one story. A robot, shuttle, or flip device may absolutely improve output, but that does not automatically mean the shop needs more machining interpolation.
| Real Factory Problem | What May Deserve More Attention |
|---|---|
| Waiting between cycles, slow part handoff, too much idle time | Automation or better cell design |
| Difficult access during the cut, unstable orientations, awkward geometry | Extra machining motion |
| Large or awkward parts that keep forcing risky reorientation | A combination of handling and motion improvements |
Keeping those categories separate helps buyers avoid paying for machining sophistication when the real loss sits between operations. A shop that measures 20 minutes of idle time per part between cycles does not need a sixth axis; it needs a better handoff sequence or a second fixture station.
The distinction becomes especially important in panel processing. A typical production line might have a panel saw, a nesting machine, an edgebander, and a drilling station. The bottleneck is often the transfer between these machines, not the cutting capability of any single unit. Adding a sixth axis to the nesting machine will not speed up the edgebander or reduce the queue at the drilling station. The shop would gain more from a better conveyor system, a buffer station, or a second edgebander.
Handling Value Is Still Real, But It Should Be Measured Honestly
If the sixth axis mainly reduces awkward presentation of large or unstable parts, that can still be a real gain. Examples include:
- Fewer manual flips.
- Less crane dependency between cuts.
- Lower reorientation risk.
- More predictable positioning on awkward workpieces.
- Shorter dead time before the next cut sequence starts.
Those are meaningful benefits. They should just be measured as handling value instead of being inflated into a vague promise of superior machining. If the axis saves 12 minutes per part by eliminating a crane-assisted flip, that is a concrete number worth putting into the payback calculation. If the axis simply makes the machine feel more flexible without changing the cycle time, the purchase decision needs more scrutiny.
Consider a stone fabrication shop that produces large countertop blanks. The blanks are heavy, fragile at the edges, and difficult to reposition manually. A six-axis stone machine that can rotate the blank between the edge profiling pass and the sink cutout eliminates a crane lift and reduces the risk of chipping. The value is real and measurable. The shop can calculate the labor saved, the reduced scrap rate, and the shorter cycle time. That is a defensible purchase.
The same logic applies to a woodworking shop producing large table tops or conference room panels. If the current process requires two operators to flip a 3-meter panel between face and edge operations, the sixth axis eliminates that labor and the associated safety risk. The payback calculation should include the reduced injury risk, not just the labor hours saved.
Programming Burden Often Decides Whether The Idea Survives
Every additional controlled motion increases software responsibility. More motion usually means:
- More collision states to simulate and verify.
- More prove-out work before the first part runs.
- More postprocessor sensitivity to small changes in the CAM setup.
- More dependence on accurate digital models of the part, fixture, and machine envelope.
If the shop already struggles to release five-axis work confidently, the sixth axis can slow adoption instead of improving output. The programming team should therefore be involved early. A platform may look commercially attractive until the team maps what must happen to run it safely and repeatably. In many shops, the bottleneck is not the machine’s motion range but the CAM department’s ability to generate collision-free toolpaths and verify them under realistic conditions.
The programming burden is not just about the first part. It is about every part after that. A six-axis machine requires the programmer to think in six degrees of freedom for every toolpath. Small changes in the part geometry, the fixture position, or the tool length can create collision states that did not exist on a simpler machine. The postprocessor must be validated for each new part family. The simulation software must have an accurate model of the machine kinematics, including the sixth axis. If the digital model is wrong, the first prove-out will find the error in the worst possible way.
Shops that already run five-axis work understand this burden. They have the simulation tools, the postprocessor expertise, and the prove-out discipline. Adding a sixth axis is an incremental step. Shops that are new to multi-axis machining face a steeper curve. They should budget for training, simulation software, and a longer prove-out period before the machine reaches full production speed.
In Many Plants, Simpler Improvements Still Beat More Motion
Before approving a six-axis machine, buyers should price the simpler alternatives honestly:
- Better fixturing that holds the part in a more accessible orientation.
- Better part orientation at the design stage to reduce the number of setups.
- Better pallet discipline so that workpieces arrive at the machine ready to cut.
- Improved staging so that the next part is already positioned when the current cycle ends.
- Cleaner cell layout that reduces travel distance and waiting time.
In many cases, those changes remove most of the real delay without adding the maintenance and software burden of another axis. That matters especially for shops in furniture, panel, and stone environments. Many operations gain more from stronger flow between cutting, drilling, edging, sanding, and assembly than from extreme axis capability on one station. In stone work, the answer may differ when the route repeatedly involves large shaped pieces, contour transitions, and difficult repositioning, but the buyer should still judge the full stone machine workflow context rather than assuming axis count alone explains the return.
Consider a cabinet shop that produces standard boxes with occasional custom pieces. The standard boxes run fine on a three-axis nesting machine. The custom pieces require angled cuts and edge profiles that a five-axis machine can handle. The shop does not need six axes. It needs a reliable five-axis machine and a better scheduling system that groups the custom work into efficient batches.
The same logic applies to a panel processing plant. If the bottleneck is the edgebander, adding a sixth axis to the saw or the nesting machine will not help. The shop should invest in a faster edgebander or a second unit. If the bottleneck is the drilling station, the answer is a dedicated drilling machine or a better fixture that reduces changeover time.
The Best Use Cases Usually Combine Geometry Pain And Handling Pain
Six-axis becomes most persuasive when the factory is fighting both kinds of loss at the same time: difficult access during the cut and difficult repositioning between cuts. A part that requires the tool to reach an undercut from multiple angles and also needs to be flipped twice between operations is a strong candidate. The sixth axis can eliminate both the tool-access compromise and the manual handling step.
The weakest use case is the opposite. Geometry is already manageable, and the shop mainly hopes the sixth axis will create a general sense of flexibility. That hope rarely survives contact with the programming queue. The strongest six-axis buyers can usually point to specific part families and say exactly what disappears: one clamp, one flip, one crane-assisted reposition, one waiting interval, or one repeated setup verification step. If the buyer cannot name the specific penalty being removed, the axis is probably ahead of the factory’s real need.
A strong use case might look like this. A stone fabricator produces curved vanity tops with an integrated sink bowl. The part requires a contour cut on the top surface, a profile cut on the edge, and a sink cutout on the underside. On a five-axis machine, the part must be flipped between the top and bottom operations. The flip requires a vacuum lifter and two operators. On a six-axis machine with a rotary table, the part stays clamped and the table rotates to present the underside to the spindle. The cycle time drops by 18 minutes per part, and the risk of edge chipping during the flip disappears. The payback is clear.
A weak use case might look like this. A furniture shop produces flat panels with simple edge profiles. The current three-axis machine handles the work comfortably. The shop owner reads about six-axis machines and imagines that more axes will make the shop more competitive. There is no specific part family that requires the extra motion. There is no measured handling penalty. The purchase is driven by a vague sense that more capability is better. That is how capital gets wasted.
Maintenance And Recovery Burden Also Rise
A sixth axis is not only a purchase. It is more bearings, more encoders, more calibration exposure, and more ways for the machine to move out of known condition. Buyers should therefore treat service depth, spare parts, and calibration routines as part of the commercial decision from the start.
If the plant cannot recover the added motion with discipline after a crash, move, or heavy use, the machine may be easier to buy than to sustain. A five-axis machine that loses calibration is already a serious event. A six-axis machine adds another set of joints, another set of zero points, and another set of alignment checks that must be verified before production resumes. Shops with limited maintenance staff should weigh that burden carefully.
The calibration issue is not theoretical. A rotary axis that drifts by a fraction of a degree can produce a visible mismatch on a contoured edge. The error may not appear until the part reaches the assembly stage, where two components no longer fit together. Finding and correcting that error costs more than the original setup time. The maintenance team needs the right tools, the right training, and the time to perform regular verification checks.
Spare parts are another consideration. A six-axis machine has more servomotors, more gearboxes, more encoders, and more cables than a three-axis machine. Each of those components can fail. The buyer should confirm that the supplier stocks the critical spares and can support the machine for the expected service life. A machine that cannot be repaired quickly is a machine that does not produce revenue.
A Fast RFQ Filter
Before approving six-axis capital, force the supplier to answer these questions clearly:
- What exact recurring setup or handling step disappears?
- What part families benefit enough to justify the added motion?
- What extra CAM, simulation, and prove-out burden comes with it?
- What simpler solution was considered and rejected?
- How will the machine be kept in known condition after crashes, moves, or heavy use?
If the answers stay abstract, the axis is probably ahead of the factory’s real need. If the answers are concrete and tied to measured losses, the sixth axis may be exactly the right investment. The difference between those two outcomes is not the machine’s brochure. It is the clarity of the factory’s own production data.
Run The Numbers Before You Run The Machine
The decision to buy a six-axis machine should start with a spreadsheet, not a demonstration. List the part families that might benefit. For each family, document the current cycle time, the number of setups, the handling steps, and the labor cost. Then estimate what the six-axis machine would change. If the savings are concrete and the payback period fits the company’s capital policy, the purchase deserves serious consideration. If the savings are speculative, the money is better spent elsewhere.
The same discipline applies to the softer benefits. Reduced operator fatigue, lower injury risk, and better surface quality are real, but they need to be valued honestly. A shop that has had two back injuries from manual panel flips in the past year has a measurable safety problem. A shop that has never had an injury and does not track near misses is guessing.
Match The Machine To The Production Mix
The value of a sixth axis depends heavily on the production mix. A shop that runs long batches of identical parts will amortize the setup savings over thousands of units. A shop that runs short batches of highly varied parts will spend more time programming and proving out than cutting. The second shop may be better served by a simpler machine and a more flexible fixture system.
The production mix also affects the maintenance burden. A machine that runs the same part for weeks at a time stays in calibration longer. A machine that changes parts every few hours is constantly being pushed to new positions, new angles, and new collision states. The second machine needs more frequent verification and a more disciplined maintenance schedule.
Consider The Downstream Effect
A six-axis machine does not operate in isolation. The parts it produces feed into downstream operations: edgebanding, sanding, assembly, and finishing. If the six-axis machine produces parts faster but the downstream stations cannot keep up, the bottleneck simply moves. The shop gains nothing.
The buyer should map the entire production flow before approving the machine. If the six-axis machine reduces the cycle time on a critical part from 40 minutes to 25 minutes, but the assembly station still takes 30 minutes per part, the overall throughput does not improve. The shop has spent significant capital to move the bottleneck from one station to another.
The Final Test Is The Part, Not The Axis
When the supplier brings the machine for a demonstration, do not ask for a generic sample. Bring a part from the actual production line. Ask the supplier to program it, set it up, and run it in front of your team. Measure the cycle time. Watch the handling sequence. Check the surface quality. Then compare the results with the current process.
If the demonstration part runs faster, requires fewer setups, and produces an acceptable finish, the six-axis machine has a real case. If the demonstration part runs at the same speed or requires extensive programming to match the current quality, the machine is not solving the problem. The axis count was never the issue.
The best six-axis buyers do not buy the axis. They buy the elimination of a specific, measured penalty. They can name the part family, the setup step, the handling move, and the labor hour that disappears. They have the production data to support the purchase. They have the programming team ready to handle the added complexity. They have the maintenance plan in place. They have checked the downstream flow. They have run the numbers.
If that description fits your shop, a six-axis machine may be exactly the right investment. If it does not, the extra motion will cost more than it returns. The machine will sit in the corner, the programming queue will grow, and the maintenance team will spend its time chasing calibration drift. The axis count will look impressive in the brochure and painful in the monthly cost report.
The decision is not about whether six axes are better than five. It is about whether the sixth axis removes a penalty that your factory can measure today. If it does, buy it. If it does not, fix the real problem first.