Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
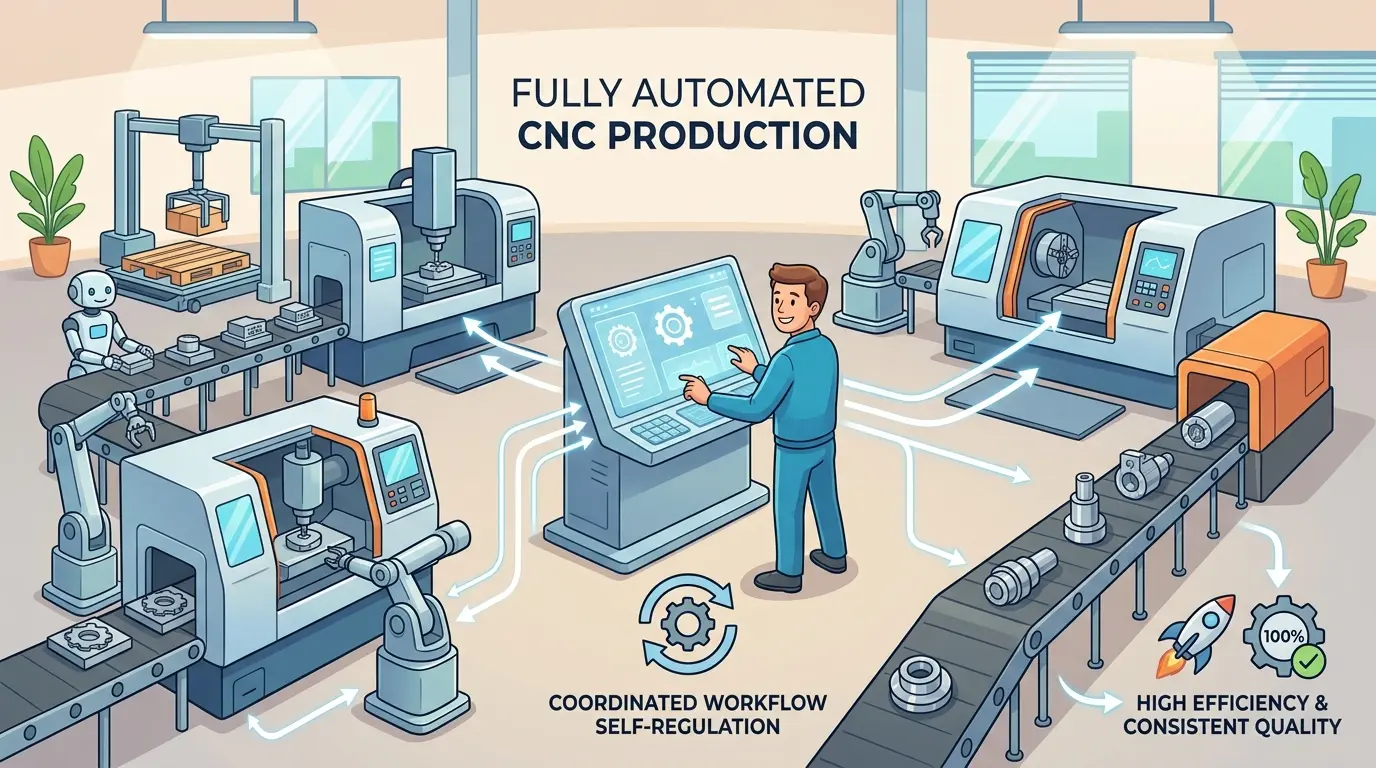
Before comparing quotations, factories must separate the label “automatic” from the specific interruption it removes. Tool-change automation pays back inside the cycle, while loading and unloading automation pays back between cycles—and confusing the two leads to expensive misinvestment. This article walks production teams through the layered reality of CNC automation, from programmed motion to linked-line transfer, and explains why the queue, not the catalog, should drive the decision. If your plant cannot name the repeated stoppage, the feature list will not save you.
Start With the Queue, Not the Catalog
Every meaningful automation decision begins with a sentence that sounds operational instead of aspirational. “We keep stopping to swap tools in the middle of one part family.” “One operator spends too much time loading heavy sheets instead of keeping the cell moving.” “Finished parts back up because unloading is slower than cutting.” “Changeover quality varies too much between shifts.” “The next machine waits because parts do not arrive in sequence.”
Those sentences matter because they point to a real interruption. Once the interruption is named, the automation conversation becomes specific. Buyers can compare whether the proposed machine removes tool-change delay, setup variation, handling labor, transfer lag, or information drift between stations.
Without that discipline, two very different machines can be compared under the same “automatic” label and the decision becomes guesswork. In practice, the queue tells the truth faster than the catalog does. If the plant already knows where it keeps stopping, it is much easier to judge whether an automatic feature is valuable or just impressive.
Automatic Is a Stack of Layers, Not One Single Machine Class
At the most basic level, every CNC machine already performs automatic motion once the program starts. The control follows coordinates, executes the path, and repeats movement more reliably than a manual machine can. That base layer of automation is real, but it is not what most buyers mean in capital-equipment discussions.
In purchasing terms, automation usually appears in layers above that foundation.
| Automation Layer | What It Removes or Stabilizes | What the Factory Usually Gains |
|---|---|---|
| Programmed machine motion | Manual movement during the machining cycle | Repeatable path execution |
| Automatic tool change | Stop-and-swap interruption between tools | Shorter cycle interruption and fewer handling mistakes |
| Setup and positioning assistance | Operator variation during referencing or locating | Faster changeover and more consistent starts |
| Automatic loading and unloading | Repeated material handling between cycles | Better spindle utilization and less manual strain |
| Part transfer or linked line handling | Manual handoff between stations | Smoother flow and lower queue instability |
| Tracking, labeling, or production data automation | Paper-based or memory-based part control | Better sequencing, traceability, and scheduling discipline |
This is why the word automatic becomes misleading when used on its own. One machine may automate tool change only. Another may automate handling while leaving most setup judgment manual. Another may connect several machines and change the whole line balance. All three may be sold as automatic, but they solve different problems and create different maintenance responsibilities.
Tool Change Automation and Material Handling Automation Pay Back Differently
Factories often talk about automation as if every automatic feature returns money through the same path. It does not.
Automatic tool change usually pays back inside the cycle. It matters when one part family needs several tools, when repeated manual swaps interrupt spindle time, or when manual intervention between operations adds avoidable variability.
Loading and unloading automation pays back between cycles. It matters when the spindle waits for the next sheet, when panels are awkward or physically demanding to move, or when finished parts block the next run because the machine can cut faster than the team can clear.
That difference matters because the right investment depends on where the time is actually being lost. A shop that loses time through repeated tool interruptions should not automatically prioritize the same automation as a shop whose real bottleneck is material staging and unload pace. One is a cycle-interruption problem. The other is a flow problem.
This is one of the most common automation buying errors. Buyers pay for visible automatic features in the wrong part of the route because they never separated the kinds of interruption in the first place.
Automation Pays Fastest Where Repetition Is Already Strong
Automation is strongest where the factory already has repeated behavior worth stabilizing. Repeated tool changes, repeated sheet loading, repeated drilling sequences, repeated part sorting, repeated handoff delay, and repeated queue buildup are all strong candidates.
That is why automation tends to pay back clearly in panel furniture, cabinetry, drilling lines, edge-finishing flow, and sheet-based routing environments. The plant is not guessing where labor goes. It can already see where the same interruption appears every shift.
For example, a shop working around CNC nesting machines may discover that spindle capability is not the main limiter at all. The real limit may be how quickly the next sheet is staged, how reliably finished parts are unloaded, or how well the next process receives sorted output. In that setting, automatic handling may create more real value than a nominal increase in raw cutting speed.
The common thread is repetition. If the same interruption keeps reappearing, automation has something real to remove. If the interruption is vague or always changing, the return will be much harder to capture.
High-Mix Chaos Often Makes Full Automation Underperform
The opposite condition matters just as much. Automation often disappoints in environments where the workflow changes too frequently for the automatic layer to stay productively utilized. High-mix custom shops, short-run prototype environments, and businesses still rewriting process rules every week may gain more from stability and visibility than from deeper automation.
That does not mean such factories should reject automation forever. It means sequence matters. If fixture logic, material flow, part sequence, and workholding assumptions are still unstable, then heavy automation can add another layer of setup and troubleshooting before the underlying process has even settled.
In that situation, a semi-automatic machine may outperform a more automated one because it is easier to understand, easier to change over, and easier to recover when a nonstandard job appears. The machine is less impressive on paper, but more productive in the real mix.
That is why the better question is not “How much automation can we afford?” It is “Which level of automation can we keep productive every day?”
Automatic Never Means Unattended or Self-Managing
One of the most expensive buying assumptions is the idea that automatic means unattended. Real factories do not work that way. Even highly automated CNC cells still depend on people for material staging, program approval, tool management, consumable checks, quality verification, alarm recovery, and schedule decisions.
Automation changes what people do. It does not remove the need for ownership. In many cases it shifts labor from repeated intervention to supervision.
- Operators spend less time on basic handling and more time watching flow and exceptions.
- Supervisors spend more time on queue balance and recovery logic.
- Maintenance becomes more important because stoppages now involve sensors, actuators, interfaces, and sequencing.
- Engineering and planning become more important because bad data is exposed faster in connected cells.
Plants that ignore this often feel disappointed after installation. The machine runs automatically in a narrow technical sense, but the organization never reassigned responsibility clearly enough to support it. The result is not too much automation. The result is automation without a matching operating model.
A Bad Process Still Looks Bad at Higher Speed
Automation should never be treated as a cure for upstream disorder. If the nesting strategy is poor, automation will process poor nests faster. If part identification is weak, automatic transfer can move confusion downstream more efficiently. If incoming data is unstable, automated cells will expose that instability sooner and more expensively.
That is why good automation projects begin with process questions rather than equipment envy.
- Are released files consistent enough?
- Are tooling and setup assumptions standardized enough?
- Is part identification already reliable?
- Are downstream stations ready for the pace increase?
- Does the team know how the line recovers if one part is rejected or one sheet is loaded incorrectly?
If those answers are weak, the plant may still need automation later, but it should not expect automation alone to create order. In many factories, the first win is not adding automation. It is making the current route stable enough that automation has something clean to accelerate.
In Woodworking, the Biggest Gains Usually Show Up in Line Balance
Woodworking plants often discover that the biggest automation gain does not come from maximizing one machine. It comes from reducing mismatch between machines. Cutting may be fast enough already, but unloading is slow. Drilling may be accurate enough already, but sequencing is weak. Edge finishing may be capable enough already, but transfer arrives in the wrong order.
This is why automation should be judged as part of a route, not as a hero feature on one machine. A connected line only feels automatic when the stations behave like parts of one system. If the router, boring center, edgebander, and sorting step all run at different rhythms with no coordination, the factory has purchased islands of automation rather than a coherent flow.
That is also why it helps to study how shops build connected machine flow across a woodworking line instead of judging automation by one station in isolation. In many factories, line balance is the real return driver.
Maintenance and Recovery Decide Whether Automation Stays Valuable
Automation is often justified through labor reduction, but that is only half the economics. More automation usually means more electrical components, more sensors, more sequence dependencies, and more recovery procedures after interruptions. If the plant is not ready for that, the automatic layer may become the main source of stoppage anxiety.
A realistic automation review should therefore include questions like:
- Who diagnoses faults during the shift?
- Which spare components should be held locally?
- How quickly can support restore sequence after a stoppage?
- What preventive-maintenance tasks become more important?
- How does the line recover without losing part identity, order, or queue logic?
These are not pessimistic questions. They are what keep automation valuable after the honeymoon period. A machine that saves labor only while everything is ideal is not yet a strong automation investment.
Semi-Automatic Is Often the Smart Intermediate Step
Many factories do not need maximum automation as the next move. They need targeted automation tied to one repeated bottleneck. A machine with dependable cycle control, better setup repeatability, and a manageable automatic tool change package may produce a stronger return than a full loading and transfer system if the plant is still building discipline around schedule flow and material handling.
This is especially true in smaller workshops, custom production, and growth-stage operations. In these environments, flexibility, visibility, and recoverability often matter more than theoretical labor removal. A semi-automatic solution that the team understands deeply may outperform a more automated cell that keeps falling out of rhythm.
That is why semi-automatic should not be treated as “not there yet.” In many real factories it is the most rational level of automation for the current state of the process.
Compare Automatic Features by the Bottleneck They Remove
When buyers compare quotations, the safest method is to translate every automatic feature into a specific operating result.
- Automatic tool change should reduce interruption on multi-operation part families.
- Automatic loading should reduce waiting time between sheets or parts.
- Automatic unloading should keep finished parts from blocking the next cycle.
- Automatic positioning aids should shorten setup and reduce operator variation.
- Automatic transfer should reduce queue buildup between stations.
- Automatic tracking should strengthen sequencing and traceability discipline.
If the feature does not remove a repeated operating problem in one of those ways, it may still be convenient, but it should not carry the same weight in the buying decision. This is also why feature count can mislead. A longer automation list is not automatically a better investment. A shorter list tied directly to the plant’s real interruption is often the stronger buy.
How Pandaxis Buyers Should Read Automatic Machine Claims
Pandaxis readers should approach automatic machine claims with a routing mindset rather than a label mindset. Ask what labor, waiting time, or queue instability is actually being removed. Ask whether the route already contains enough repetition to justify the feature. Ask whether the rest of the line is ready to benefit from the faster or more stable station.
That perspective matters whether a buyer is comparing one station or stepping back to review the Pandaxis machinery lineup. The right automatic machine is the one that removes a named interruption in a believable production context. The wrong one is the machine that sounds more automatic while leaving the real bottleneck untouched.
Automation Is Worth Buying Only Where the Queue Already Tells the Truth
An automatic CNC machine is not defined by one universal feature package. It is defined by which part of the workflow no longer depends on repeated human interruption once the machine is in place. That may be tool changes, setup variation, sheet handling, part transfer, or production tracking. Each layer changes the factory in a different way.
The safest approval rule is simple: buy automation only when the plant can name the interruption, measure how often it happens, and explain how the new machine changes that exact point of friction. If the constraint is real, automation can improve throughput, repeatability, and labor use quickly. If the constraint is vague, the machine may still look impressive, but the return will be harder to capture and even harder to defend.