Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
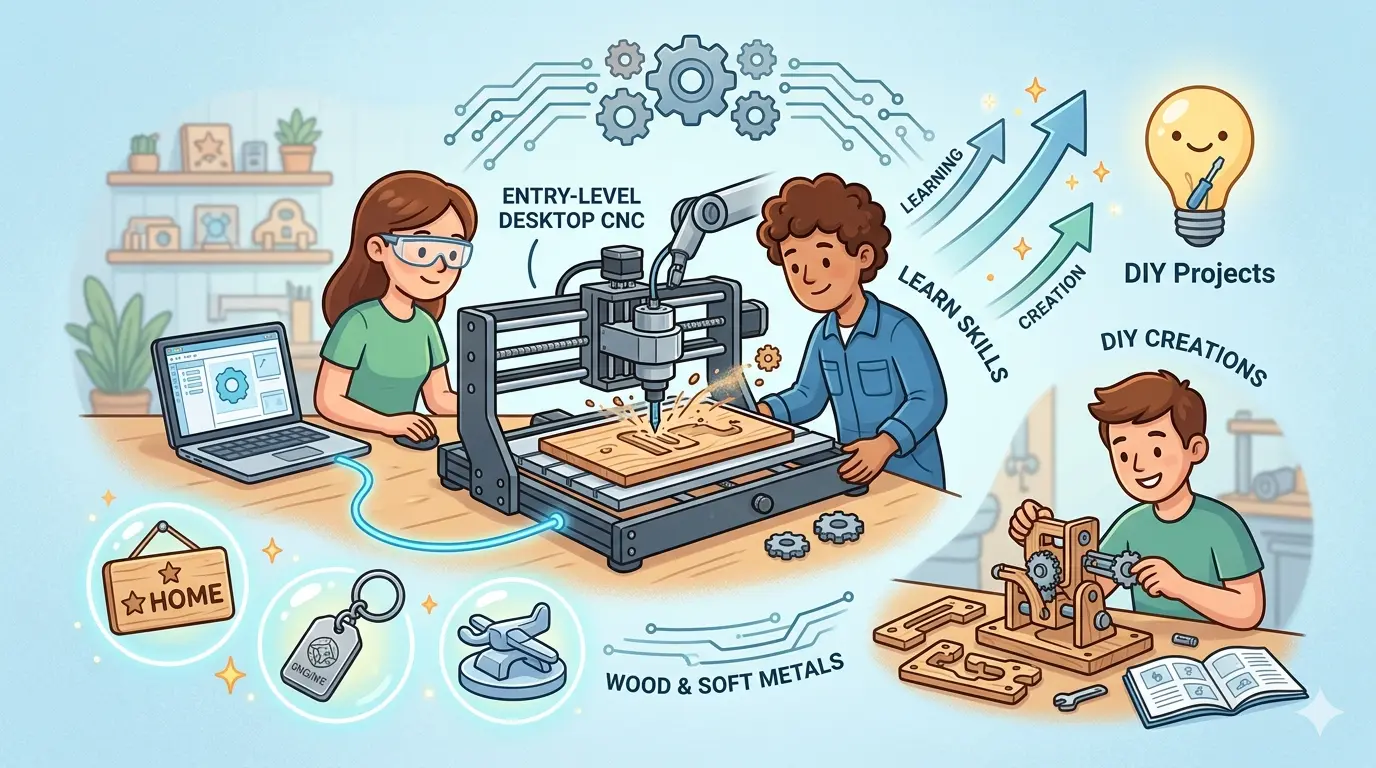
Before you dismiss the 3018-class desktop router as a hobbyist toy or overbuy a production spindle for light bench work, you need to separate its advertised work envelope from its real operational limits. This article cuts through the confusion around that nominal 300 by 180 millimeter travel, explaining why two identically named machines can behave completely differently on the shop floor. It addresses the practical decision of whether your workload is a learning-and-prototyping problem or a delivery-and-throughput problem, and why setup discipline, workholding, and workflow friction—not part size alone—should trigger your upgrade to a more stable machine class.
Why the 3018 Class Keeps Selling
The 3018-class desktop router remains one of the most common entry points into CNC machining, and the reason is straightforward: it lets a buyer test the entire digital manufacturing workflow without committing the floor space, electrical budget, or capital that a production machine requires. That accessibility is a genuine strength. It is also the source of most of the confusion around this category.
The name “3018” describes a nominal working envelope of roughly 300 by 180 millimeters. It does not describe rigidity, spindle quality, controller maturity, or long-term repeatability. Two machines with the same advertised travel can behave very differently on the shop floor because of differences in frame construction, linear motion components, spindle bearings, and the quality of the electronics package. Treating the number as a performance specification rather than a size class leads to predictable disappointment.
The practical way to evaluate a 3018 is not to ask whether it can cut a given material once. Almost any of these machines can produce a decent sample part if the operator slows the feed rate, takes light passes, and supervises the entire cycle. The better question is whether the work you actually need to do is a learning-and-prototyping problem or a delivery-and-throughput problem. A 3018 answers the first question well. It usually struggles when buyers quietly expect it to answer the second.
The Real Use Case: Process Access Before Process Scale
The 3018 class exists because many buyers need access to the CNC process before they need production scale. That is a legitimate purchasing reason, not a consolation prize.
Typical buyers in this category include:
- Operators and engineers who need to learn the CAD-to-CAM-to-cut chain before specifying larger equipment.
- Small prototype users testing part ideas, material choices, or joint details before committing to a more expensive machine.
- Designers and makers who need light engraving or small-format routing on a bench.
- Maintenance and product-development teams exploring whether CNC will become a recurring internal capability.
The educational value here is real. On a small desktop router, the consequences of weak setup appear immediately. The operator sees when stock is not secure, when a cutter is too long for the job, or when the chosen sequence creates chatter, poor finish, or a ruined part. That visibility is the core value of the category. A 3018 is a low-cost way to decide whether CNC will become a lasting skill or a passing experiment.
What Counts as a Good Fit for a 3018
People often say these machines are good for small parts. That is true but incomplete. A job can be small on paper and still be a poor fit in practice because of clamping difficulty, tooling complexity, or finish expectations.
The best 3018 work is small in every practical sense:
- The stock is easy to stage and clamp without elaborate fixtures.
- The cutter choice is simple and repeatable across jobs.
- The cycle does not depend on aggressive material removal rates.
- The finish expectations are reasonable for a compact desktop machine.
- The operator can recover from a mistake without losing an expensive production day.
That profile points to tasks such as engraving plates and tags, cutting test pieces, small acrylic or wood samples, fixture concepts, simple jigs, and very compact prototype parts. These jobs fit the table, and they fit the ownership model. That second point matters more than most first-time buyers realize.
If a part technically fits the advertised area but requires awkward tabs, crowded clamps, repeated repositioning, or constant supervision, the workload has already started to outgrow the class. A 3018 is strongest when the setup feels calm, not merely possible.
What This Category Teaches Better Than Larger Machines
One reason desktop CNC can be worth buying is that it exposes process truth without much insulation. On a small router, you learn quickly:
- How a drawing becomes a toolpath instead of a wish.
- How work zero errors multiply into a visibly wrong part.
- How weak stock preparation creates more trouble than the spindle ever will.
- How cutter selection affects not just finish but stability and confidence during the cut.
- How clamp placement changes what is actually safe to machine.
That is why 3018 ownership can be more educational than productive and still count as a success. A beginner who learns to standardize stock, save reliable CAM templates, document tool offsets, and repeat the same setup cleanly three times has gained more than a buyer who chases a single dramatic demo cut and learns nothing repeatable from it.
The machine does not reward vague enthusiasm. It rewards discipline. That can feel strict at first, but it is useful strictness. It builds habits that still matter later on larger benchtop or shop-level equipment.
Where Buyers Start to Overestimate a 3018
Most disappointment with this class comes from the gap between what is possible once and what is sustainable every week. A 3018 can sometimes do more than people expect. That does not mean it should become the plan for routine work that involves tighter delivery pressure, more expensive blanks, or customer-visible quality requirements.
One careful sample cut in a harder material or one successful sign does not automatically mean the machine has become a dependable small production platform. Buyers see proof of capability and assume they now have proof of fit. Those are not the same thing.
A useful rule is simple: if the machine only succeeds when the operator slows everything down, watches every pass, accepts a lot of setup friction, and treats each run like a small rescue mission, then the machine may be demonstrating capability but not delivering workflow stability. Commercial value comes from repeatable calm, not isolated heroics.
The most common overestimation patterns look like this:
- Turning a learning machine into a quoted-delivery machine too early.
- Treating nominal work area as if clamps and clearance do not exist.
- Assuming a slightly successful sample proves long-term repeatability.
- Believing a low entry price somehow cancels the cost of time, scrap, and operator frustration.
When those assumptions stack up, the buyer is no longer evaluating the machine honestly.
Setup Quality Decides More Than the Spec Sheet
On a 3018, setup quality usually matters more than the marketing photo. The real working area is never just the published envelope. It is the published envelope minus the space taken by clamps, tabs, stock variation, safe tool approach, and the operator’s need to avoid collisions while still holding the material securely. That is why a part that looks small in CAD can feel crowded on the machine.
Workholding is not a side topic on this class. It is the topic. If the stock can move, lift, vibrate, or deflect under light cutting loads, the rest of the setup becomes unstable. The spindle may still run. The cut may still continue. But finish quality, dimensional confidence, and operator trust all start to erode at the same time.
Tooling decisions behave the same way. A short, sharp, sensible tool with modest stick-out often does more to improve results than chasing aggressive cutting behavior the frame and setup do not support well. Beginners sometimes blame the machine first, when the actual problem is a long unsupported tool, a poor zero, weak stock prep, or a fixture plan that steals too much usable area.
That is another reason this class is educational. It teaches cause and effect with very little delay.
The Real Costs Show Up in Rework, Not in the Cart
People buy 3018 machines because the upfront cost is accessible. That is valid. But the machine price is only the clean part of the calculation. The real ownership cost often shows up in:
- Broken or worn small cutters.
- Scrap caused by weak zeroing or weak stock hold-down.
- Spoilboard replacement and resurfacing effort.
- Measurement tools, clamps, and setup accessories.
- Time spent testing, retrying, and cleaning instead of cutting finished parts.
None of that means the class is a bad purchase. It means the buyer should understand what the low price really buys. It buys access to the process, not freedom from process cost. The machine is not expensive because it is magically efficient. It is accessible because the owner is expected to contribute patience, attention, and learning effort. If the buyer wants a machine that protects time more aggressively, that need usually points toward a different class.
What Healthy Ownership Looks Like in the First Six Months
One of the best ways to judge whether a 3018 purchase is working is to look at the owner’s habits after the novelty fades. Healthy ownership usually looks surprisingly boring:
- The owner repeats a small number of manageable jobs instead of chasing every new challenge.
- The same stock sizes and fixture methods get reused because they are predictable.
- Tool choices narrow down rather than expand every week.
- CAM settings get documented instead of rediscovered each time.
- The machine becomes cleaner, calmer, and easier to trust.
That pattern is a good sign because it means the machine is creating process literacy. The owner is not using the router as a daily stress test. They are using it as a platform for consistency.
Bad ownership usually looks different. Every new week brings a different material, a different clamp improvisation, a different promised output level, and another attempt to force the machine into work it never handles comfortably. That path produces a lot of activity and very little clarity. For this class, boring is progress. A repeatable setup is more valuable than a dramatic one-off success.
The Signals That Desktop Logic Has Run Out
There is usually a clear moment when a 3018 stops being the right answer. The machine has not changed. The workload has. Common warning signs include:
- The clamp arrangement starts taking more thought than the actual toolpath.
- The part needs multiple awkward orientations just to stay inside the workable area.
- Finish or tolerance issues begin to matter because the parts are no longer only internal tests.
- The operator spends more time supervising or recovering jobs than creating the next setup.
- Small mistakes stop being educational and start becoming expensive.
- Customers, teammates, or delivery dates now depend on the machine behaving like stable equipment rather than a learning tool.
That last point is especially important. A 3018 is often a smart first machine and a poor machine to hide behind once outside expectations rise. If the router is now expected to protect delivery, keep throughput moving, or support repeat weekly demand, then the buying question has already changed. At that stage, the honest answer is usually not better optimism. It is a better machine decision.
The Upgrade Trigger Is Workflow Friction, Not Part Size Alone
Many people assume the next step comes only when the part becomes physically larger. In practice, the better upgrade trigger is workflow friction. If the machine is still cutting small parts but every job now depends on delicate clamp placement, long setup time, repeated babysitting, or fragile recovery after interruptions, the upgrade case may already be stronger than the part dimensions suggest.
A machine does not become wrong only when the table is too small. It also becomes wrong when the ownership model consumes too much attention for the value it returns. That is how many useful 3018 purchases naturally end. The owner has learned enough to recognize the next bottleneck clearly. That is not failure. That is the machine doing its real job.
Once the question becomes less about learning CNC and more about protecting workflow, it helps to stop comparing only desktop codes and start looking at what changes when routing becomes part of a larger production process. A broader view of how routing fits into panel-oriented manufacturing gives a better planning framework than one more round of entry-level machine browsing. The same shift applies when the decision is no longer about a single bench tool, but about where cutting, drilling, material handling, and repeatability sit inside a larger equipment strategy. At that point, the wider Pandaxis machinery lineup is the more relevant reference point because the conversation has moved from access to process fit.
That is the practical boundary. A 3018 is good for honest learning, tiny-format experimentation, and showing exactly where desktop CNC stops feeling calm. It is a sound purchase when the goal is to build skill, validate small recurring tasks, and discover what matters in setup. It becomes the wrong purchase when it is treated as a substitute for a more stable machine class after the work has already started asking for reliability, margin, and workflow protection.