Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
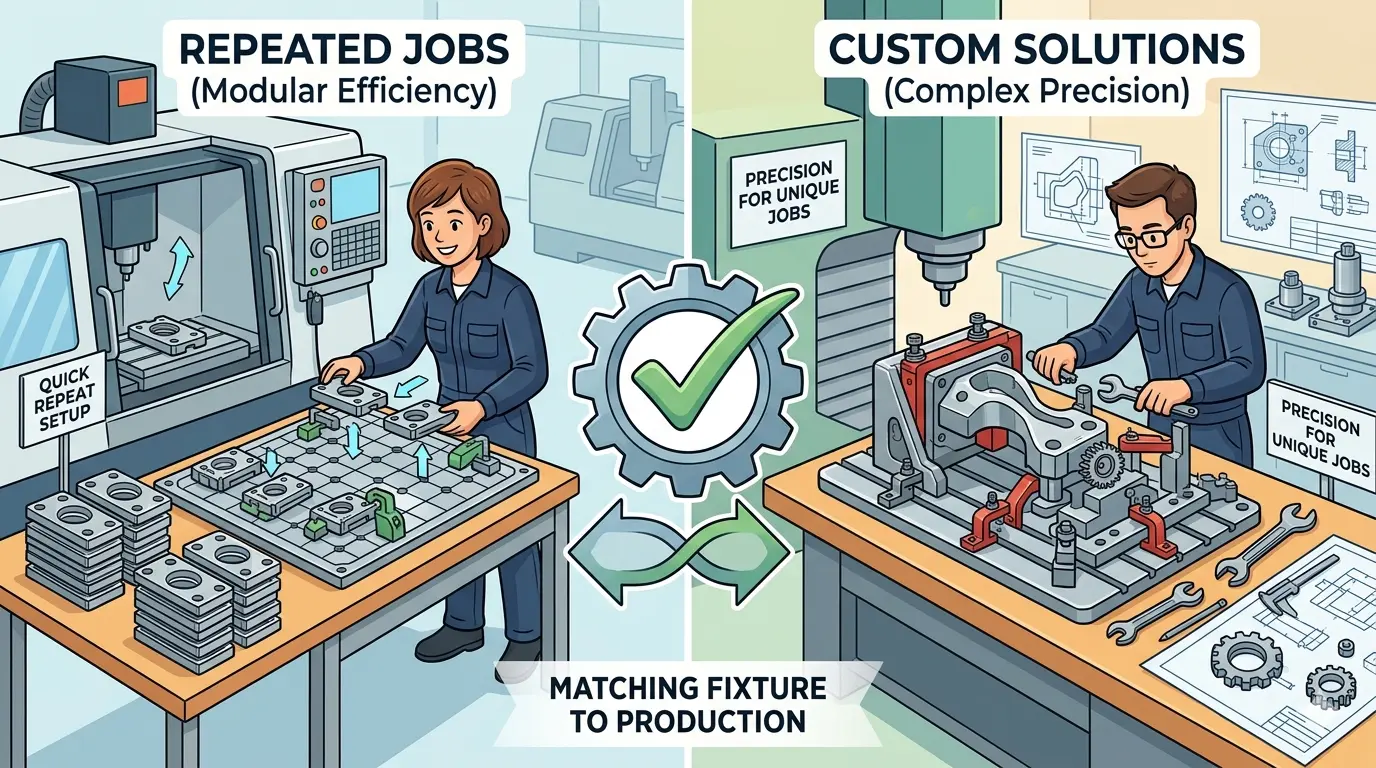
Repeated runs expose the real cost of improvised workholding: slow loading, awkward tool access, and datum repeatability that depends on the operator’s judgment rather than the setup itself. This article walks production teams through the practical decision between modular fixture plates and dedicated custom fixtures, framing the choice as an economic question about where setup knowledge should live. You’ll learn why part similarity matters more than volume alone, how reconfiguration friction quietly erodes productivity, and why a staged transition often beats a pure either-or commitment.
Repeated Work Exposes Setup Problems, Not Just Setup Habits
Early on, a few clamps and careful operator attention can carry a job. After several runs, the real costs surface. Loading takes too long. Tool access stays awkward. Operators still verify seating by hand. Datum repeatability depends on who set the job, not on the setup itself. That is usually when shops start comparing fixture plates with custom fixtures.
The comparison is not about which option sounds more advanced. It is about where the repeated waste sits. If the shop keeps rebuilding setup logic for many related jobs, a modular fixture plate often makes more sense. If one narrow family of parts keeps creating the same loading, location, or support problem, dedicated hardware becomes easier to justify. The decision is about setup economics, not fixturing prestige.
Think of it as an escalation path. Shops rarely jump from general clamping straight into a philosophical debate about fixturing. They reach a point where the work itself has started teaching them something. Either the operation needs one disciplined base that can be reconfigured quickly, or it needs to stop reconfiguring at all.
Start By Identifying What Keeps Repeating
Most fixturing decisions become clearer when the team stops discussing hardware and starts discussing recurring pain. Which burden returns every week?
For some shops, the burden is variation in the part mix. Different but related parts come through the same machine. Operators need a stable setup base, yet the details of locating and support change from job to job. In that situation, the waste usually comes from rebuilding setup logic too often.
For other shops, the burden is the opposite. One part family returns again and again. The geometry is stable. The route is known. The same loading and repeatability issues appear on every batch. In that situation, the waste often comes from making the operator repeat the same setup judgment long after the process should have been built into hardware.
This first distinction matters because shops often choose the wrong investment for the wrong kind of repetition. They buy a custom fixture when the part mix still changes too much, or they stay modular when the real problem is that the setup should have stopped being flexible months ago.
Fixture Plates Solve Repeat Variety Better Than Repeat Narrowness
Fixture plates are strongest when the shop wants one repeatable base for many related jobs. Their value comes from structured flexibility. The plate provides a stable, known mounting and reference platform while clamps, stops, nests, and support elements can be adjusted around that platform as the part family changes.
Fixture plates are not simply convenient hardware. They are a platform decision. The shop is choosing to standardize the base layer of workholding so that different jobs can inherit the same setup logic without recreating everything from scratch.
This works best when the part family shares enough common features for the base to matter. Similar stock orientation, similar datum zones, comparable support needs, or repeatable machine-access patterns all help a fixture plate pay back. The plate becomes a common language for workholding. Operators stop improvising every job because the starting structure is already disciplined.
That benefit is easy to undervalue. Structured flexibility is still a productivity gain. A shop does not need a single fixed geometry to benefit from more repeatable setup foundations.
Custom Fixtures Solve Repeat Uncertainty Better Than Repeat Changeovers
Custom fixtures make more sense when the work has stopped teaching the shop anything new. The same part or narrowly related family returns often enough that the repeated uncertainty has become the cost. Loading points are already known. Clamp strategy is already known. Support logic is already known. The only remaining question is why the operator still has to interpret it every cycle.
That is the moment dedicated hardware becomes attractive. A custom fixture is powerful because it moves knowledge out of people and methods and puts that knowledge into the hardware itself. If the part has one recurring orientation, one recurring support pattern, one recurring clamp path, and one recurring failure mode, a dedicated fixture can simplify the cycle dramatically.
This is not just about holding strength. Many custom fixtures pay back because they eliminate decisions. The operator no longer has to wonder whether the part is fully seated, whether the stop condition is correct, or whether support points were set the same way as last batch. The fixture itself answers those questions.
That is why custom fixtures are often calmer than modular setups on narrow repeat work. The point is not flexibility. The point is to remove avoidable judgment from the cycle.
The Core Economic Question Is Where Setup Knowledge Should Live
One useful way to compare these two directions is to ask where the shop wants setup intelligence to live.
With a fixture plate, more of the intelligence remains in the method. The base is standardized, but the team still decides how to position stops, supports, nests, and clamps for each job. That is efficient when the variation is real and the team benefits from reconfiguration.
With a custom fixture, more of the intelligence moves into hardware. The fixture itself defines orientation, seating, support, and often loading sequence. That is efficient when the same answer should be repeated with as little interpretation as possible.
Seen this way, the comparison becomes much clearer. A fixture plate is not simply the cheaper option, and a custom fixture is not simply the more advanced option. Each one places the problem-solving effort in a different part of the process. The better choice is the one that reduces the same repeated waste every week.
Similarity Matters More Than Volume Alone
Shops often try to make this decision using volume only. That is too simple. Volume matters, but similarity matters just as much.
A high number of parts does not automatically justify a custom fixture if the jobs still share a modular setup language and change enough that dedicated hardware would become stranded. At the same time, a moderate number of parts can absolutely justify a custom fixture if the geometry is awkward, the loading risk is real, and the same setup uncertainty keeps returning.
That is why better diagnostic questions are more useful than simple volume thresholds:
- Do the same locating surfaces keep returning?
- Are support and clamp zones broadly similar from lot to lot?
- Is the operator still making the same setup judgment repeatedly?
- Does the same loading error or mis-seating issue show up across batches?
- Would a dedicated nest remove a real source of scrap or time loss?
These questions separate part frequency from part sameness. Frequency tells you how often the pain appears. Sameness tells you whether the same physical answer can solve that pain repeatedly.
Reconfiguration Has A Cost Even When The Setup “Works”
One reason fixture plates get undervalued is that shops compare them against general clamping rather than against cumulative setup friction. A general setup may be technically workable, but that does not mean it is efficient. If the team keeps rebuilding logic, touching off stops, checking clearances, or explaining the method to different operators, the setup is still expensive.
Fixture plates reduce that cost by giving the shop a repeatable starting point. The part family may still vary, but the machine table no longer starts from zero. That can shorten changeovers, reduce interpretation, improve repeatability, and make training easier because the base logic stays familiar even as the work changes.
This is especially valuable in mixed production environments where nobody wants to build a full custom fixture for every recurring part, but improvisation has already become too costly. The plate stabilizes the process without forcing the shop into early over-specialization.
Dedicated Fixtures Earn Their Cost By Making The Wrong Load Harder
The strongest custom fixtures do more than hold parts firmly. They make mistakes less likely.
This matters because repeated jobs often carry hidden human cost. Operators learn the setup and perform it well, but the process still depends on attention staying high on every cycle. A good dedicated fixture changes that. It makes correct orientation obvious. It makes incorrect loading harder to complete. It makes support conditions more repeatable. It can also reduce setup touch time because the fixture itself carries the logic that used to live in setup notes and operator memory.
That is why dedicated fixtures often pay back even before raw cycle time is dramatically lower. They reduce variation, fatigue, and repeated checking. On narrow high-repeat work, those benefits can be more valuable than the hardware cost looks at first.
Many Shops Need A Transitional Stage, Not A Pure Yes-Or-No Decision
The smartest fixturing strategy is often neither fully modular nor fully dedicated at the start. Many shops get the best result by moving through a middle stage.
That middle stage usually looks like this: first the shop adopts a fixture plate as the repeatable base, then it adds part-specific locating blocks, nests, or support features for the families that appear most often, and only later does it promote the most stable geometries into fully dedicated fixtures.
This approach works because it lets the work teach the shop where true repetition really lives. Instead of building custom hardware too early, the team gains data. Which parts keep returning? Which setup issues still consume time? Which modular additions solved the issue, and which jobs still deserve dedicated treatment?
This staged path is often more honest and more economical than treating fixture plates and custom fixtures as mutually exclusive categories. In practice, many productive shops use both. The real skill is knowing when one should start giving way to the other.
The Wrong Choice Usually Shows Up As Drag, Not Collapse
Fixturing mistakes at this stage usually do not look dramatic. More often, they look like a setup that never becomes calm.
Loading still feels slower than it should. Operators still verify the same surfaces manually. Tool access is still tighter than it should be. Datum repeatability still depends on careful handling rather than on the setup itself. The run succeeds, but the process feels more labor-intensive than the part family should require.
That kind of drag is important evidence. Shops sometimes wait for obvious failure before reconsidering fixture strategy, but the earlier warning is usually that repeated work still carries too much attention cost. If the same part family is always asking for the same operator judgment, the setup philosophy may no longer match the work honestly.
That is why the best fixturing decisions often come from watching where calm never arrives. The setup may be functional, but if it never becomes routine, it is still too expensive.
Ask Whether The Problem Is Really Workholding Or Something Larger
Before committing to either direction, it helps to check whether the setup issue is truly a fixturing problem or whether it is exposing a broader machine or process limitation. If access is poor because the machine envelope is wrong, if cycle pressure is really coming from the wrong machine type, or if repeat accuracy is being compromised by broader workholding assumptions, then the fixture investment should be reviewed in that larger context.
Teams stepping back from that question should revisit how stronger workholding improves accuracy and repeatability, because the fixture decision often sits inside a larger process decision rather than outside it. And if the shop is already rethinking machine capability alongside setup strategy, it is worth comparing equipment quotations with the same discipline used on fixture decisions so hardware, workholding, and workflow assumptions are evaluated together.
Which Setup Fits Repeated Jobs?
If the shop keeps moving among related parts that share enough common setup logic to benefit from one stable base, fixture plates usually fit repeated jobs better. If one stable geometry or narrow family keeps coming back and the repeated pain is loading uncertainty, slow preparation, or part-specific drift, custom fixtures usually fit repeated jobs better.
That is the practical answer to the title, but the deeper rule is even simpler: choose the option that removes the same avoidable decision from the cycle every week. If flexibility is still where the value sits, keep intelligence in a reusable base. If interpretation has become the waste, move that intelligence into dedicated hardware. And if the factory is reviewing broader machine families as part of that decision, the Pandaxis product catalog gives the useful high-level view.
Once the shop sees fixture plates and custom fixtures as stages in a setup strategy rather than as competing symbols of sophistication, the decision becomes much easier to defend. The right choice is the one that makes repeated work feel less improvised and more controlled.