Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
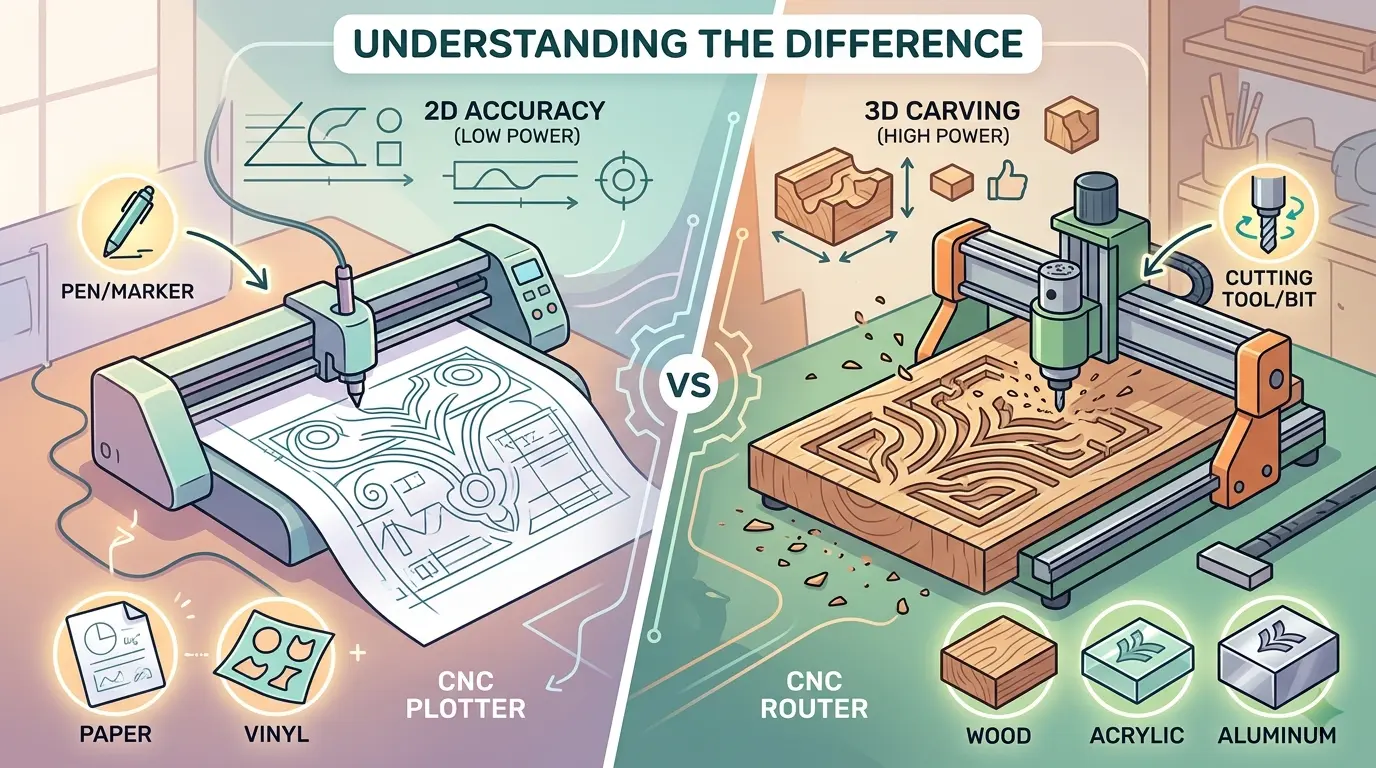
Define the workload before judging table sizes or control software, the real decision hinges on what the cutting head must physically do to your material. A plotter follows the surface with knives, crease wheels, or pens under light force, while a router engages a rotating spindle to remove stock from rigid panels. That single distinction drives everything downstream: rigidity, vacuum demand, tool wear, dust extraction, noise, and secondary finishing. If you process corrugated board, films, or textiles, plotter logic wins on changeover speed and clean edges. If you cut MDF, acrylic, or laminated panels with pockets, drilling, or edge shaping, router logic owns the geometry. Match the force profile to your weekly workload, not the machine’s appearance.
Start With The Contact Model, Not The Product Name
Buyers often confuse CNC plotters and CNC routers because both machines can look similar from across the shop floor. A flatbed table, a moving gantry, a control screen, and sheet material clamped or vacuumed in place. The visual similarity makes the machines seem closer than they really are. In production, they usually belong to different process lanes.
The cleanest difference is not the table, the gantry, or even the control software. It is the kind of contact the head makes with the material. A plotter is typically built to follow a path with relatively light force using knives, pens, crease tools, or similar heads. A router is typically built to cut with a rotating spindle that actually removes material from the workpiece. That one distinction changes nearly everything else: rigidity, vacuum demand, tool wear, dust control, feature range, housekeeping, noise, and downstream workflow.
So this is not really a naming question. It is a process question. If the buyer identifies what the head must physically do to the material, the correct machine class becomes far easier to spot.
Plotters Usually Follow The Surface; Routers Usually Attack It
This is the clearest operational split. Plotters are typically optimized for surface-following or through-cutting tasks that do not depend on deep material removal. They are commonly associated with drag-knife cutting, tangential knife work, creasing, light trimming, drawing, marking, or similar operations on softer and thinner materials.
Routers, by contrast, are typically chosen when the work needs true machining behavior. The spindle engages the material with enough force to profile, slot, drill, carve, or pocket rigid stock. That means the machine is not just tracing geometry. It is resisting cutting load while maintaining edge quality and feature control.
This sounds basic, but it is operationally decisive. Once the process moves from surface-following to true material removal, the entire machine environment changes with it.
Material Usually Exposes The Better Choice Faster Than The Brochure Does
If the shop mainly processes corrugated board, foam board, films, textiles, gasket materials, soft display stock, packaging materials, or other sheet goods that benefit from clean path control without heavy cutting load, plotter-style logic is usually the better fit. These materials often reward head flexibility, clean sheet handling, fast job change, and reduced dust more than they reward spindle strength.
If the shop mainly processes MDF, plywood, laminated panels, acrylic, rigid plastics, composites, or similar materials that need contour cutting, pocketing, drilling, carving, or edge shaping, router logic usually takes over. The work now requires real cutting force, real tool engagement, and the kind of rigidity that plotting systems are not primarily designed around.
That is why material is often the fastest filter. The wrong buying decision usually begins when the buyer keeps thinking about machine appearance after the material has already made the answer obvious.
Force Changes More Than Speed Or Finish
Many buyers compare size, price, or perceived versatility first. The better buying lens is process force, because force changes much more than the cut itself.
Once the operation needs higher cutting load, the machine needs stronger structure, more reliable hold-down, more serious spoilboard management, and better dust or chip extraction. Tool wear becomes a recurring operating cost. Noise rises. The material may need more support. Edge quality begins depending on spindle behavior, tool condition, and the way the work is held during machining.
Lower-force plotting tasks create a different operating environment. Waste is often trimmed sheet offcut instead of chips. The process may still need vacuum or registration, but it usually does not need the same level of rigidity, extraction, and tool management. That is why a plotter is not merely a light-duty router and a router is not simply a powerful plotter. They are optimized around different force profiles.
Plotter Workflows Usually Win When Sheet Handling Is The Real Priority
Plotters are often the cleaner answer when the business depends on handling softer or lighter sheet materials accurately without turning the process into a machining operation. Packaging samples, displays, printed graphics, patterns, foam and gasket conversion, and similar work often fit here.
The value in those environments usually comes from path accuracy, registration, toolhead flexibility, low cleanup burden, and quick switching between marking, cutting, and creasing functions. The machine is valuable because it can work delicately and efficiently across changing sheet tasks without burdening the shop with machining-level housekeeping.
That is an important point because many buyers interpret “lighter duty” as “less industrial.” In the right workflow, plotter logic is not a compromise. It is the better industrial answer because it avoids adding unnecessary spindle burden to a material family that does not need it.
Consider a packaging prototype shop that receives five different corrugated board specs per day. Each job requires a different crease pattern, a different cut depth, and a different turnaround time. A plotter with a tangential knife and crease wheel can switch between those jobs in minutes, with minimal dust and no tool-change downtime. The same shop would struggle with a router because the spindle is overkill for corrugated board, the dust extraction becomes a nuisance, and the edge quality on soft board is often worse than a clean knife cut. The plotter is not a weaker machine here; it is the correct machine for the material and the job mix.
Router Workflows Usually Win When The Part Needs True Geometry Ownership
Routers become the correct choice when the job needs more than a path across the surface. If the part needs profiles in rigid stock, internal pockets, slots, drilling patterns, edge shaping, engraving-like routing, or nested panel conversion with meaningful cutting load, a router is usually the stronger fit.
That is why routers dominate panel processing, woodworking, rigid non-metallic sheet work, and many acrylic or composite jobs. In the Pandaxis product mix, this is the lane where CNC nesting machines become the relevant reference because the workflow is built around routing, drilling, and panel conversion rather than low-force tracing.
The important distinction is that routers are not only cutting shapes out of sheets. In many jobs they are also owning depth, edge behavior, hole location, and productivity across repeated panels. That is a different production responsibility from plotting.
Take a cabinet shop that runs a standard panel batch: 18mm MDF, 12 sheets per job, each sheet nested with cabinet sides, shelves, and internal partitions. The router must plunge to exact depth, cut clean edges that will not need excessive sanding, drill dowel holes at precise locations, and maintain tolerance across all 12 sheets. A plotter cannot do this work because it lacks the spindle power, the rigidity, and the tooling flexibility. The router is not just cutting shapes; it is producing finished components that move directly to edgebanding and assembly.
Waste Type And Housekeeping Often Reveal The Wrong Choice First
One of the most practical ways to separate plotters from routers is to ask what the shop will be cleaning up every day. If the work mostly produces trimmed offcuts, kiss-cut waste, or light scrap from sheet processing, the workflow is often closer to a plotting lane. If the process creates chips, dust, tool-wear debris, and spoilboard wear, the workflow is behaving like routing.
This matters because daily housekeeping is not a side issue. It affects labor, maintenance rhythm, safety, consumables, and whether the shop can keep the process stable without constant friction. A router can add unnecessary extraction burden, tool management, and noise to a soft-material workflow that never really wanted machining behavior. A plotter can become the bottleneck immediately if the stock actually needs spindle force and edge control.
The wrong machine class often announces itself through recurring weekly irritation before it ever shows up as a catastrophic technical mismatch.
Imagine a signage shop that cuts acrylic letters and also does vinyl cutting for vehicle graphics. The vinyl work is a natural plotter job: kiss-cut the vinyl, weed the waste, and move on. The acrylic letters need routed edges, drilled mounting holes, and sometimes pocketed backlight channels. If the shop tries to use one machine for both, it will compromise on both. The plotter cannot route acrylic cleanly, and the router makes a mess of vinyl because the spindle tears thin film instead of cutting it cleanly. The shop needs two process lanes, not one machine that does neither well.
Hold-Down Strategy Changes With The Process
Both machine families care about material control, but they care in different ways. Plotter workflows often emphasize flat sheet handling, registration, and enough hold-down to keep lighter materials stable under relatively low process force. Routers usually need more robust hold-down because the tool is actively removing material and pushing against the stock with greater lateral and vertical force.
That brings spoilboards, stronger vacuum strategy, better support for thin or narrow remnants, and more attention to what happens as parts separate from the sheet during cutting. In other words, the hold-down strategy is not just stronger in routing. It is structurally more important to part quality and process stability.
This is another reason the visual similarity between the machines is misleading. Two tables may both use vacuum zones, but the commercial meaning of that vacuum is very different once the process shifts from light path control to real spindle cutting.
On a router, a poorly supported panel can vibrate during cutting, causing chatter marks on the edge, dimensional drift on the profile, and accelerated tool wear. On a plotter, the same panel might be fine with light hold-down because the knife force is minimal. The buyer who assumes that vacuum is vacuum will miss this distinction until the first bad batch of parts.
Software Usually Confirms The Better Machine Class
Another good test is to look at what the digital workflow is really trying to optimize. Plotter environments often emphasize vector cleanliness, registration, print-and-cut alignment, head switching, and fast response on varied sheet jobs. Router environments tend to emphasize nesting yield, cutting order, drilling logic, tool change strategy, pocketing sequence, and material-removal efficiency.
That means the software path often confirms what the physical process already suggested. Packaging and display teams usually care more about precise vector-driven sheet conversion. Panel and woodworking teams care more about how routed geometry, drilled features, and nested yield combine into a productive line.
If the software priorities feel misaligned with the shop’s real work, the hardware choice is usually being forced too.
For example, a shop that does printed graphics on rigid PVC foam board might be tempted by a router because the material is rigid. But the actual job is print-and-cut: register the printed sheet, cut the contour, and deliver a finished graphic. The software priority is registration accuracy and clean contour cutting, not deep pocketing or drilling. A plotter with a tangential knife can handle this job faster and with less dust than a router. The software workflow reveals this because the CAM toolpath is simple contour cutting, not multi-pass pocketing or drilling cycles.
Sometimes Plotter Vs Router Is Actually The Wrong Comparison
Some buyers comparing plotters and routers are really deciding among three lanes, not two. In signage, acrylic, displays, and some non-metallic sheet applications, laser may belong in the conversation as well. That is especially true when the buyer is not only deciding how to move the head across the sheet, but what kind of edge, detail, or workflow the material really rewards.
That is why it can help to review how CNC laser and CNC router workflows diverge instead of forcing every application into a plotter-versus-router argument. And where the material genuinely fits non-metallic laser work, the adjacent laser cutters and engravers category may be the more relevant buying path. The point is not to force laser into every comparison. It is to notice when the buyer is really sorting process families, not merely product labels.
Consider a shop that makes acrylic display stands. A router can cut the acrylic, but the edges will need flame polishing or sanding to be clear. A laser can cut the same acrylic with a polished edge straight off the machine, eliminating a secondary operation. But the laser will also produce a slightly beveled edge and may not handle thicker acrylic as efficiently as a router. The buyer who only compares plotter versus router misses the fact that laser might be the better process for the edge quality requirement. The comparison should be process-first, not machine-name-first.
Tooling And Consumables Tell The Real Cost Story
Beyond the machine purchase price, the consumable and tooling profile differs sharply between plotters and routers. A plotter consumes knives, crease wheels, and possibly pen cartridges. These are relatively inexpensive and wear slowly on soft materials. A router consumes end mills, drill bits, and sometimes compression bits for panel processing. These tools wear faster, cost more per unit, and require regular inspection and replacement to maintain edge quality.
Tool wear is not just a cost line item. It affects cycle time because dull tools cut slower and produce worse edges. It affects scrap because a worn tool can tear the material instead of cutting it cleanly. It affects maintenance because a broken tool can damage the spoilboard or the workpiece. The buyer who ignores tooling cost when comparing plotters and routers will get an unpleasant surprise in the first quarter of production.
For a plotter, the tooling question is mostly about knife type and sharpness. A drag knife works well for simple contours, but a tangential knife is better for sharp corners and complex geometry because it can rotate the blade to match the cutting direction. The buyer should ask whether the plotter supports both, and how quickly the head can switch between cutting and creasing tools.
For a router, the tooling question is about spindle power, tool change capability, and tool path strategy. A shop that runs nested panel jobs will want an automatic tool changer to switch between compression bits for cutting, spiral bits for pocketing, and drill bits for holes. A shop that runs simple acrylic contours might be fine with a single tool and manual changes. The tooling strategy should match the job mix, not the machine brochure.
Cycle Time And Throughput Are Not The Same Metric
Buyers often compare cycle time on a single part and assume that the faster machine is the better investment. But throughput is a shop-level metric that includes setup time, job changeover, material loading, and secondary operations. A plotter might be slower on a single contour cut than a router, but if the plotter eliminates dust extraction setup, reduces cleanup time, and allows faster job switching, the effective throughput can be higher for the right job mix.
Conversely, a router might be slower to set up for a new job because the spoilboard needs to be surfaced, the tooling needs to be changed, and the vacuum zones need to be configured. But once running, the router can produce parts with features that a plotter cannot match. The buyer should compare the full production cycle, not just the cutting time on one sample.
For example, a shop that produces 50 identical acrylic signs per week will benefit from a router because the setup cost is amortized over a large batch. A shop that produces 50 different packaging samples per week will benefit from a plotter because the setup cost per job is low and the changeover time is minimal. The same machine class is not the right answer for both shops, even if the material is similar.
Secondary Operations Often Decide The Machine Class
The buyer should also consider what happens after the cut. A plotter typically produces parts that are ready for assembly or finishing with minimal secondary work. A router often produces parts that need edge sanding, deburring, or additional machining before they are ready for the next step.
For wood panels, routed edges are usually clean but may need light sanding before edgebanding. For acrylic, routed edges are opaque and need flame polishing or sanding to be clear. For foam board, routed edges are acceptable but may have slight fuzz that needs trimming. The buyer should map the full process from raw sheet to finished part, including secondary operations, before choosing the machine class.
This is where the plotter often wins for soft materials because the knife cut is clean and does not create a secondary finishing burden. It is also where the router often wins for rigid materials because the spindle can produce features that a knife cannot, such as drilled holes, pockets, and precise edge profiles. The secondary operation cost is part of the total cost of ownership, and it should be included in the comparison.
Safety And Noise Are Shop-Floor Realities
Routers are louder than plotters because the spindle is removing material at high speed. A shop that runs a router for eight hours a day will need hearing protection for operators and possibly acoustic treatment for the workspace. A plotter is quieter because the knife or pen does not generate the same level of noise. This is not a minor consideration in a shared workspace or a shop near residential areas.
Safety is also different. A router has an exposed rotating spindle and produces chips and dust that can be hazardous if not properly extracted. A plotter has a knife or pen head that is less dangerous but still requires care during loading and unloading. The buyer should assess the shop’s safety culture and the operator’s familiarity with each machine class before making a decision.
Dust extraction is another cost driver. A router typically requires a dust collection system with adequate CFM to capture chips and fine dust. This adds capital cost, energy cost, and maintenance burden. A plotter may not need dust extraction at all, or only a light vacuum for offcut removal. The buyer who ignores dust extraction cost will underestimate the total cost of a router installation.
The Right Choice Usually Simplifies Weekly Work, Not Just One Demo Job
Buyers sometimes get trapped by demonstration logic. A machine looked impressive on one sample, so the team starts reasoning outward from the demo rather than inward from the weekly workload. The safer question is always which machine class simplifies the jobs the shop invoices most often.
If soft-sheet handling, graphics, packaging, sample making, or low-force conversion dominate the week, plotter logic will usually reduce more friction. If rigid stock, routed shapes, drilled features, carved details, or panel conversion dominate, router logic will usually remove more friction. That is the real commercial test.
The better machine class is not the one that sounds more advanced or seems broader in theory. It is the one whose contact logic matches the work without asking the team to fight the process every day. In practical terms, buy the force profile your workflow actually needs, not the table shape that happens to look familiar.
Before you sign the purchase order, walk through a typical week in your shop. List the materials you process, the features you cut, the secondary operations you perform, and the cleanup burden you accept. If the list points toward knife cutting and light sheet handling, a plotter is the right investment. If the list points toward spindle cutting, drilling, and panel conversion, a router is the right investment. If the list includes both, you may need two machines or a clear decision about which process lane deserves the capital first.
For shops that land clearly in the router lane, the Pandaxis shop offers a starting point for comparing nesting machines, panel saws, and related woodworking equipment. For shops that land in the plotter lane, the decision is about head flexibility, registration accuracy, and sheet handling, not spindle power. The machine class that matches your weekly workload is the one that will pay for itself fastest.