Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
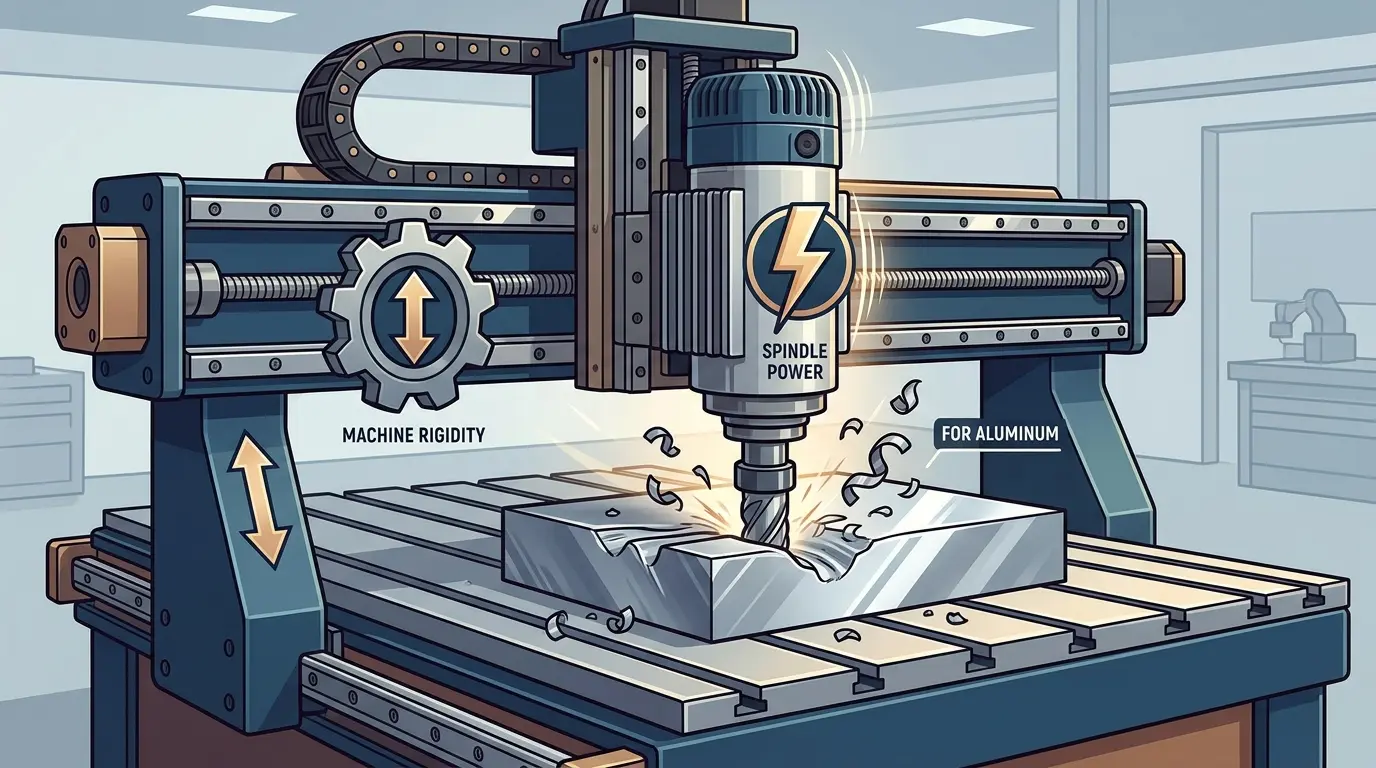
Aluminum routing fails not because a CNC router lacks a headline spindle rating, but because the entire cutting chain—frame stiffness, workholding, chip evacuation, and cutter geometry—cannot hold a stable operating window for your actual part mix. This article forces you past the binary “can it cut aluminum?” question and into the process-window reality that determines whether your investment produces clean parts or a constant battle with chatter, burrs, and premature tool wear. Before you compare quotes, you need to know whether your aluminum work is an extension of your router-based production or a core lane demanding a different machine class entirely.
Why Aluminum Routing Decisions Fail Before the Machine Arrives
Most buyers approach aluminum routing as a simple capability question: can this CNC router cut aluminum or not? That framing produces poor purchasing decisions because it treats the answer as a binary specification check. In practice, aluminum routing is a process-window question. The machine either holds a stable operating envelope across the specific parts you intend to produce, or it does not. And that stability depends on far more than the spindle rating printed in the brochure.
Aluminum exposes machine weaknesses faster than wood, MDF, or common routing plastics. It punishes deflection, rewards clean chip evacuation, and turns vague assumptions about fixturing into visible quality problems within the first few parts. Shops that treat aluminum as a stress test rather than a yes-or-no capability make better equipment decisions. They also avoid the most common failure mode: buying a router that can cut aluminum under ideal conditions, then discovering it cannot hold the process window for the actual production mix.
Aluminum Fails at the Weakest Link, Not the Average Specification
Many routers can cut some aluminum under some conditions. That limited truth gets generalized into a purchasing conclusion, and the generalization is where the trouble starts. Aluminum routing succeeds only when the entire cutting chain stays stable for the real job: frame rigidity, spindle behavior, workholding, toolpath strategy, cutter geometry, chip evacuation, and heat control.
The process rarely fails because every element is weak simultaneously. It fails because one weak link gets exposed first. The gantry flexes more than expected under cut forces. The spindle behaves poorly in the speed band the job requires. Thin sheet lifts between vacuum zones. Chips pack in the flutes and the cut drifts into rubbing. Heat builds faster than the shop planned for. Once that first weak link triggers, the entire cut deteriorates, and the machine looks worse than its specifications suggested.
This is why average machine specs mislead. Aluminum does not test the average. It tests the first component in the chain that cannot stay honest under load.
Rigidity Is the First Real Filter for Aluminum Work
Aluminum reveals structural weakness quickly. If the gantry, spindle mount, table, rail support, or material support stack deflects too much under cutting forces, the result is chatter, burrs, unstable finish, and dimensional drift. This is not a bonus-feature discussion. Rigidity is the first filter that separates routers capable of productive aluminum work from machines that will only frustrate the operators assigned to them.
Mass alone does not prove rigidity. A heavy machine with a poorly supported spindle mount or a flexing table can still deflect. The entire stiffness chain matters: frame construction, linear guide sizing, ball screw or rack-and-pinion behavior, spindle mounting interface, table flatness, and how well the material is supported through the cut. Aluminum is unforgiving when any single point in that chain gives way.
That said, a router does not need to behave like a heavy machining center to contribute productively on aluminum. It needs enough stiffness to hold the specific part family it will actually run. A machine that handles 3 mm sheet profiles confidently may struggle with 20 mm plate work. The evaluation should match the stiffness requirement to the real workload, not to a generic sense of what a “rigid” machine should weigh.
Spindle Power Matters Only in the Band Where the Cut Actually Runs
Buyers compare routers by maximum spindle rating, even though aluminum routing depends more on usable behavior in the real operating band. The relevant questions are whether the spindle maintains stable shearing at the required RPM, whether it holds torque discipline without rubbing, and whether it responds predictably with the actual cutter diameter, depth, and feed strategy the job demands.
A strong headline kilowatt number does not help if the spindle drifts into heat, vibration, or finish deterioration at the speeds and feeds the aluminum job requires. Conversely, a modest spindle that stays clean and predictable across the useful cutting band can outperform a larger unit that behaves erratically at the relevant operating point.
Practical buyers should ask about the spindle package as a system: motor characteristics, bearing quality, toolholder interface, and how the spindle behaves under sustained load at the RPM range the aluminum work requires. If the supplier cannot articulate that relationship clearly, the power number is doing rhetorical work instead of manufacturing work.
Workholding Usually Determines Whether the Router Looks Honest or Overrated
In aluminum routing, workholding is where optimistic buying decisions fail first. Thin sheets, narrow profiles, small retained islands, detailed cutouts, and long unsupported sections all create opportunities for part movement. Once the work lifts, chatters, or vibrates, finish quality drops and tool life follows.
Buyers sometimes assume a stronger spindle will compensate for weak fixturing. In aluminum, that logic backfires. More cutting energy exposes poor holding faster. If the material is not secure against the real forces in the cut, the router will appear less capable than it actually is, because the process was unstable before the spindle had a chance to help.
Aluminum routing should always be evaluated as a table-and-fixturing question, not just a spindle-and-frame question. Vacuum hold-down strategy, spoilboard condition, fixture design for small parts, and clamping methods for profiles all belong in the same conversation as machine rigidity. A router with excellent structural stiffness will still produce poor aluminum parts if the workholding plan cannot keep the material stationary.
Chip Evacuation and Heat Control Keep the Cut in a True Cutting State
Aluminum routing works only when the process remains in a true cutting state. That means the cutter is shearing material cleanly, chips are evacuating from the cut zone, and heat is not accumulating faster than the process can shed it. Once chips stop clearing, the cut drifts toward rubbing, recutting, heat buildup, burrs, smeared finish, and rapidly declining tool life.
This is why the purchase decision is never just about structure and spindle. Tool geometry, chip load, evacuation behavior, extraction performance, and the shop’s plan for heat control all belong in the same evaluation. Shops that treat these items as optional add-ons often end up blaming the machine for a process package that was incomplete from the start.
Aluminum also demands attention to cutter selection. Geometry designed for wood does not transfer directly to aluminum. Flute count, helix angle, coating, and chip-breaking characteristics all affect whether the cut stays clean or drifts into rubbing. The machine cannot compensate for a cutter that is fundamentally wrong for the material.
The Best Aluminum Jobs for Routers Still Look Like Routing Work
Routers become convincing on aluminum when the work still resembles routing: flatter parts, sheet-based profiles, lighter plate work, mixed-material production, and applications where the same large-format table already creates value in plastics, composite panels, or non-metal sheet processing.
In these environments, aluminum is often a secondary but commercially useful capability. The router does not need to become the plant’s primary metal-cutting identity to justify itself. It only needs to stay reliable on the defined family of aluminum work the shop expects to carry.
That distinction keeps the investment honest. A router can be a sensible bridge into aluminum work if the role is clear. It becomes a weak answer when buyers quietly expect it to behave like the center of a dedicated metal-cutting business. The machine class has limits, and those limits are not negotiable.
Warning Signs Appear Before the Router Completely Fails the Job
Shops often wait too long to admit the router is operating outside a healthy aluminum window. The early warning signs are usually visible before catastrophic failure:
- Operators keep reducing feed rates and depth of cut to protect finish quality.
- Tool life collapses faster than expected, with cutters dulling or chipping prematurely.
- Thin or detailed parts require excessive manual cleanup and deburring.
- Burrs and edge defects become normal rather than occasional.
- Repeatability depends too much on which operator is running the job.
- Setup teams spend more time stabilizing the process than producing through it.
When these signals become routine, the shop is not “learning aluminum.” It is discovering that the current machine-process package sits too close to the edge of its useful role. The honest response is to either adjust the part mix to fit the machine’s capability or evaluate a different machine class.
Representative Parts Matter More Than the Easy Demo Sample
Many routers can produce one acceptable aluminum sample. That does not prove production fit. The better test is whether the platform can hold the real part family: the deeper slot, the thinner wall, the smaller retained feature, the longer run, the less perfect sheet, or the mixed batch that actually appears after installation.
Router-for-aluminum evaluation should be tied to representative parts rather than to the safest demonstration geometry. A machine that survives only the easiest sample is not a fit. It is a delayed production problem. Factories should test what they expect to sell, not what flatters the equipment fastest.
This means bringing actual production files, actual material thicknesses, and actual tolerance requirements to the evaluation. If the supplier cannot run representative parts to acceptable quality, the machine is not suitable for the workload, regardless of how impressive the demo sample looks.
When Aluminum Becomes Core Work, the Router Decision Changes Completely
The router usually becomes a weaker answer once aluminum is no longer occasional or complementary work. If the growth plan depends on heavier material removal, tighter tolerance expectations, more demanding geometry, or a daily metal-cutting lane that leaves little room for process drift, the management question shifts from “which router?” to “why are we not evaluating a milling platform instead?”
That boundary matters. The shop does not need to wait until the router fails badly to recognize it. Once aluminum becomes central rather than adjacent, the economic logic changes. The machine is now being asked to carry a core production identity, not an extension capability. That is a different investment decision with different machine requirements.
The Most Honest Commercial Question Is Where Aluminum Sits in the Growth Plan
The strongest decisions come from one explicit answer: is aluminum an extension of a router-based business, or is it becoming a core lane that deserves its own machine logic? If it is an extension, a capable router may be the right bridge. If it is core, the buyer should be far tougher about whether the router is a productive asset or a compromise with a short commercial lifespan.
This is also where quotations become misleading. One supplier may assume light aluminum work inside a mixed-material environment. Another may assume a more ambitious production burden. If those assumptions are not visible, the price comparison becomes distorted. Buyers should compare machinery quotes line by line rather than treating every router as equivalent because the spindle rating looks similar.
A Router Is Good for Aluminum Only When the Whole Process Stays Honest Under Stress
Aluminum routing can work well, but only when the frame, spindle behavior, workholding, cutter strategy, and chip-control plan all stay inside the same stable operating window. Buyers who focus on spindle power alone usually miss that. Buyers who treat aluminum as a whole-process stress test usually make better decisions.
For occasional or mixed-material aluminum work, a well-chosen router can be a sensible production tool. For heavier or central aluminum work, the more disciplined answer is often to admit the router has reached the edge of its role before the shop spends too much time forcing it past that line. The machine class has a defined operating envelope, and the best purchasing decisions respect that envelope rather than testing it.