Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
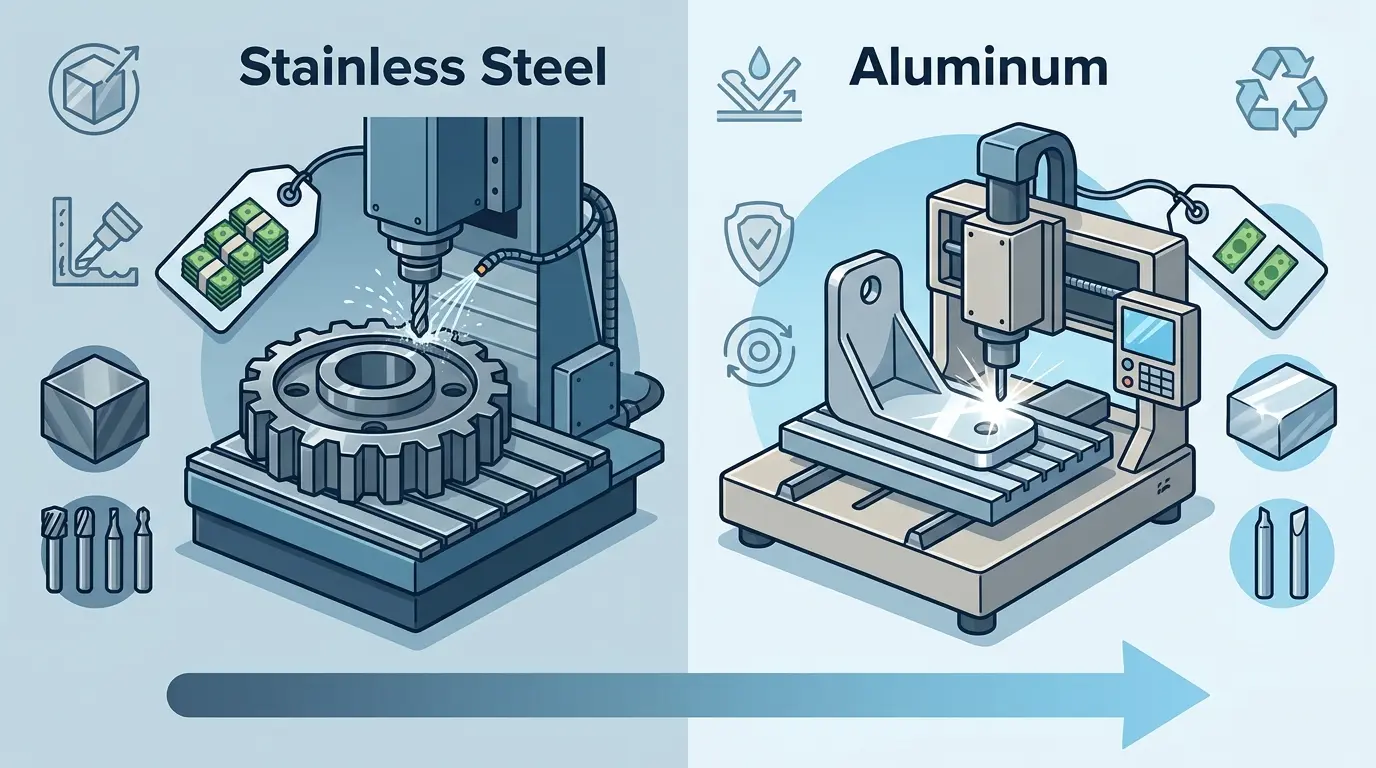
When the same part drawing is quoted in aluminum and stainless steel, the price gap often exceeds 40 percent—and raw material cost rarely explains the bulk of that difference. The real shift happens inside the machining route: cycle time, tooling stress, fixturing logic, finish stability, and the supplier’s risk allowance all change when the metal changes. Buyers who compare only material prices miss the actual cost driver. This article breaks down where that premium really accumulates, why geometry and tolerances magnify it, and how to decide whether your application genuinely needs stainless’s service burden or can run profitably in aluminum’s wider process window.
Why the Same Drawing Can Produce Two Very Different Quotes
Send an identical part drawing to a machine shop and ask for a quote in aluminum, then ask for the same part in stainless steel. In many cases, the second quote comes back 40 percent higher, sometimes more. The natural assumption is that raw material cost explains the gap. In practice, it often explains only a fraction of it.
The larger shift happens inside the machining route itself. Cycle time changes. Tooling stress changes. Finish stability changes. Fixturing logic changes. The supplier’s risk allowance changes. By the time the quote reaches your desk, the material change has effectively rebuilt the entire manufacturing plan.
That is why the useful comparison is not “Which metal is better?” The better question is: “What does the shop have to do differently once the metal changes, and does my application actually need that added burden?” Material selection only becomes intelligent when service requirements and manufacturing consequences are considered together.
Start With Service Need Before You Start With Cost
Material choice should begin with what the part must survive in service. Corrosion exposure, washdown conditions, weight targets, cosmetic expectations, mechanical duty, and downstream finishing requirements all shape whether aluminum or stainless is the better fit. If that decision is made clearly, the manufacturing conversation becomes easier because the shop is not being asked to solve the wrong problem with process heroics.
Trouble begins when material is chosen by instinct instead of by duty. Stainless may be selected because it sounds safer, even when the part does not genuinely need that level of service resistance. Aluminum may be selected because it looks cheaper, even when corrosion, washdown, or structural expectations make it the wrong long-term choice. In both cases, the purchasing decision leaks cost because the service requirement was not defined firmly enough first.
Consider a food-processing guard panel that will be washed down with caustic chemicals several times per shift. Aluminum might machine beautifully and quote low, but if the finish cannot survive the washdown environment without heavy anodizing or powder coating, the apparent savings disappear. Conversely, a mounting bracket inside a dry, climate-controlled enclosure does not need stainless just because the plant has a “stainless is stronger” policy. The service environment should drive the material, not the other way around.
A Practical Comparison of What Usually Changes
The table below is a starting point for buyers reviewing the same part in both materials. It reflects typical shop-floor behavior, not universal truth for every grade and geometry.
| Decision Area | Aluminum Tends To Offer | Stainless Tends To Demand |
|---|---|---|
| Process window | Broader and more forgiving on many sensible geometries | Narrower and less tolerant of weak setup or tooling |
| Cycle time | Often shorter when the part is designed cleanly | Often longer because the route needs more caution |
| Tooling burden | Usually lower overall risk if the route is stable | Usually higher pressure on tool condition and process discipline |
| Finish stability | Can be very good but still sensitive on thin or cosmetic parts | Often more difficult to hold cleanly when the geometry is demanding |
| Quote risk | Lower when the supplier sees a comfortable route | Higher because more things can go wrong if the route is pushed too hard |
| Application strength | Low weight, practical machinability, broad general use | Corrosion resistance, washdown durability, harsher service fit |
Aluminum Usually Opens the Process Window
In many shops, aluminum gives the supplier a wider comfort zone. Sensible geometries can often be machined faster, with lower tooling burden and a route that feels more forgiving overall. That does not mean aluminum is effortless. Thin walls, cosmetic faces, long unsupported features, and poor chip evacuation can still create problems. But in many common machining scenarios, aluminum gives the process more room to stay productive without becoming fragile.
That wider window matters because it changes how aggressively the shop can plan the route. More stable cycle times, less defensive quoting, and a lower probability of process drama often follow. The larger point is simple: aluminum often gives the shop more freedom before the route starts feeling tight.
On the shop floor, this shows up in practical ways. A shop cutting 6061 aluminum can typically run higher spindle speeds, take more aggressive depths of cut, and rely on standard carbide tooling with predictable tool life. Chip evacuation is straightforward because aluminum chips are light and break easily. The operator can walk away from the machine with confidence that the part will be within tolerance when the cycle finishes. That confidence is worth real money because it reduces inspection time, rework, and the need for constant process monitoring.
Stainless Usually Narrows the Route and Raises the Penalty for Weakness
Stainless steel often pushes the supplier toward a more conservative plan. The process may need slower material removal, tighter attention to tool condition, more disciplined heat and chip control, and greater caution around finish-sensitive geometry. A route that feels routine in aluminum can become much less tolerant in stainless if the setup, tooling, or programming discipline is weak.
That is why stainless quotes often rise for reasons that go well beyond the raw material line. The supplier is not only paying for the metal. The supplier is pricing a route with less forgiveness. In commercial terms, stainless narrows the margin for casual decision-making. If the application truly needs what stainless provides, that higher burden is justified. If it does not, the plant may be paying for manufacturing difficulty it never needed to buy.
Consider what happens with a 304 stainless part that has a deep pocket and a tight internal corner. The shop cannot simply push the tool harder. Work hardening becomes a real risk if the tool dwells or rubs instead of cutting cleanly. The programmer must plan entry angles, stepovers, and finishing passes with more care. The tool may need to be replaced more frequently because edge breakdown shows up immediately in surface finish. The operator must watch for built-up edge and adjust coolant delivery. Every one of these adjustments adds time to the cycle and risk to the quote.
The Biggest Price Shift Usually Lives in Time and Tooling
Raw stock gets attention because it is visible on the quote. Cycle time and tooling burden often explain more of the gap. Stainless may require more careful passes, more frequent tool changes, more cautious finish strategy, and more allowance for what can drift under real cutting conditions. Aluminum often allows a shorter, cleaner route when the part design supports it.
So when buyers see a meaningful quote gap, they should not assume the supplier is mainly marking up the material. Often the supplier is pricing a different risk profile. If one route is broader and more forgiving while the other is tighter and more failure-sensitive, the quote is reflecting that difference in manufacturing reality.
Tool life is a concrete example. A carbide end mill cutting aluminum might last for hundreds of parts before showing measurable wear. The same tool cutting stainless might need replacement after a fraction of that volume, especially if the geometry involves interrupted cuts or small-diameter tools. Tool cost per part multiplies quickly when the tooling budget is spread across a production run. Add in the time lost to tool changes and the operator attention required to catch wear before it ruins a finish, and the stainless route carries a burden that never appears on the material line of the quote.
Geometry Does Not Stay Equally Easy When the Material Changes
One of the most common buyer mistakes is assuming that the same shape carries the same difficulty in both materials. It does not. Deep pockets, thin ribs, long slender features, tight internal corners, narrow slots, and cosmetic surfaces all interact differently with the material. A feature that feels manageable in aluminum can become more expensive or less stable in stainless because the supplier expects a tighter process window, more cautious removal, or more tool management to keep the result under control.
The reverse is also true in selected cases. Thin aluminum geometry can need careful support because deformation, handling damage, or cosmetic marking becomes more likely. That is why the material comparison should always be made through the actual geometry, not through the material label alone. Same CAD does not mean same route.
Take a thin-walled housing, for example. In aluminum, the wall might flex during machining, causing chatter marks that require a secondary pass or a change in fixturing. In stainless, the same wall is stiffer, but the cutting forces are higher, so the shop must balance rigidity against the risk of work hardening. Neither material is automatically easier. The geometry determines which challenges dominate, and the supplier’s experience with that specific combination matters more than any general rule about the metal.
Fixturing and Part Behavior Shift in Different Ways
Material changes the demands placed on fixturing. Aluminum may allow faster machining in many cases, but thin or delicate geometry can still make the part feel vulnerable to movement or cosmetic damage if support is poor. Stainless often pushes the route toward more cautious clamping logic because the process is already working inside a tighter stability window and the cost of losing position or inducing trouble is higher.
This matters because many quote conversations focus on spindle and tooling first, while the real process confidence depends just as much on how the part is held. If the material change forces the supplier to rethink support, staging, or pass planning, the economics have already shifted before anyone reaches the finish section of the print.
Consider a flat plate with a large machined pocket. In aluminum, a simple vacuum fixture or a few toggle clamps might hold the part securely enough for aggressive cutting. In stainless, the higher cutting forces may require additional support points, a thicker fixture plate, or a different clamping arrangement to prevent vibration. The shop might need to add a second operation to machine the back side, which doubles setup time and introduces a new opportunity for misalignment. These fixture-related costs are invisible in the CAD model but very visible in the quote.
Finish and Burr Expectations Can Rebuild the Quote Again
Machining is only one stage of the story. Surface finish, burr behavior, edge expectations, and downstream treatment can change the economics again. Aluminum may cut efficiently but still require careful cosmetic handling or protective finishing depending on the application. Stainless may cost more to machine but align better with environments that need corrosion resistance and want to avoid relying on later protective treatment.
That is why buyers should compare total route logic, not only metal removal. If one material machines faster but needs more downstream protection, while the other machines slower but better suits the final environment, the honest comparison is broader than the first machining estimate.
Burr behavior is a practical example. Aluminum tends to produce soft, stringy burrs that can be removed with a quick hand deburr or a simple tumbling operation. Stainless burrs are harder and more tenacious, often requiring secondary machining or manual work with power tools. If the part has multiple edges that must be broken cleanly, the deburring cost per part can be substantially higher in stainless. Add inspection requirements for edge condition, and the gap widens further.
Tolerance Strategy Magnifies the Difference Very Quickly
Careless tolerancing raises cost in both materials, but it usually hurts faster in stainless because the route is already less forgiving. Blanket tight tolerances, vague cosmetic language, and unnecessarily difficult edges force the supplier to price defensively because the material has already reduced the comfort zone. What looked like ordinary drawing caution can become a strong cost multiplier.
The cleaner approach is to separate functional dimensions from noncritical ones and to make surface priorities explicit. When the drawing shows what genuinely matters, the material comparison becomes much more honest. Otherwise the quote is not really comparing aluminum and stainless. It is comparing how much defensive process burden the supplier has to assume in each route.
For example, a drawing that calls for ±0.05 mm on every dimension, including features that simply locate a cover plate, forces the shop to plan for inspection and potential rework on every feature. In aluminum, that might be manageable because the material is forgiving and the shop can correct small deviations quickly. In stainless, the same tolerance band requires more careful toolpath planning, more frequent in-process measurement, and a higher scrap allowance. The buyer pays for that caution whether or not the tight tolerance is actually needed.
Volume Changes Whether the Harder Material Premium Is Acceptable
Batch size matters because route efficiency and setup strategy change with volume. At small quantity, the pain of a tougher material can be amplified because setup, prove-out, and tooling caution are being spread across fewer parts. At higher repeat volume, the economics can still improve if the route stabilizes and the service requirement truly justifies the material.
This is why buyers should be careful when using one-off prototype pricing to make a long-run material decision. The same part may look punishing in stainless at launch volume and still make sense in repeat production if the application demands it. The opposite can also happen. A material can appear reasonable at small scale and become too expensive once recurring throughput, tool management, and inspection burden are modeled honestly.
Consider a production run of 500 parts. In aluminum, the shop might dial in the route after the first 20 parts and then run the remaining 480 with minimal intervention. In stainless, the shop might need to check tool wear every 50 parts, adjust feeds and speeds as the tool degrades, and inspect critical features more frequently. The labor burden per part stays higher throughout the run, not just during setup. That recurring cost is what makes stainless premiums persist at volume, even when the raw material price difference narrows.
Supplier Questions That Usually Expose the Real Difference
The most useful material-comparison questions are not abstract material questions. They are route questions:
- Which feature becomes the slowest or highest-risk feature when the material changes?
- Where does tooling burden increase most noticeably?
- Which tolerances or surfaces are driving the most defensive quoting?
- Does the supplier expect a broad or narrow process window here?
- What part of the route changes most: cycle time, finish control, fixturing, or tool life?
- Is the higher quote driven mainly by material cost or by route difficulty?
Questions like these move the conversation away from generic material preference and toward the specific manufacturing consequences of the choice. A supplier who can answer them clearly is showing you the real cost structure. A supplier who deflects with “stainless is just harder to machine” may not have analyzed the route carefully enough to give you an honest comparison.
How to Make the Final Decision Without Overpaying
Start by writing down the service requirements in plain language. What environment will the part live in? What loads will it carry? What finish does the customer expect? What is the weight target? What downstream processes, such as welding, anodizing, or passivation, will the part go through? Only after those answers are clear should you compare material options.
Then ask the supplier to quote both materials with the same drawing, and request a breakdown of where the cost difference comes from. If the supplier can show that the gap is mostly in cycle time and tooling, you know the stainless route is genuinely more demanding. If the gap is mostly in raw material, the manufacturing burden may be smaller than you feared. Either way, you are making the decision with real information instead of assumptions.
Finally, consider whether the part can be redesigned to reduce the burden in the harder material. A slightly larger internal radius, a shorter unsupported wall, or a relaxed tolerance on a cosmetic surface can bring the stainless route closer to the aluminum route in cost. Sometimes the material change is unavoidable, but the geometry is not fixed. A small design adjustment can save more money than any supplier negotiation.
Choose the Material That Solves the Application Without Buying Avoidable Difficulty
Aluminum often buys a wider process window, faster machining, and lower quote risk when the application allows it. Stainless often buys corrosion resistance, harsher-service durability, and better fit for demanding environments, but it usually does so at the cost of tighter process discipline, slower cutting, and greater quote caution. Neither material is automatically better. The better material is the one that satisfies real service demands without importing manufacturing difficulty the part never needed.
If buyers keep that standard, the quote comparison becomes much clearer. They are no longer deciding between a cheap metal and an expensive metal. They are deciding between two different manufacturing routes and two different service outcomes, then choosing the one that honestly fits both.
For shops and buyers working through these tradeoffs, the practical path is to bring the drawing, the service requirements, and the volume forecast to the table together. That combination, not the material name alone, determines whether the part is economical to produce and reliable in service. When the material decision is made that way, the quote stops being a surprise and starts being a plan.