Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
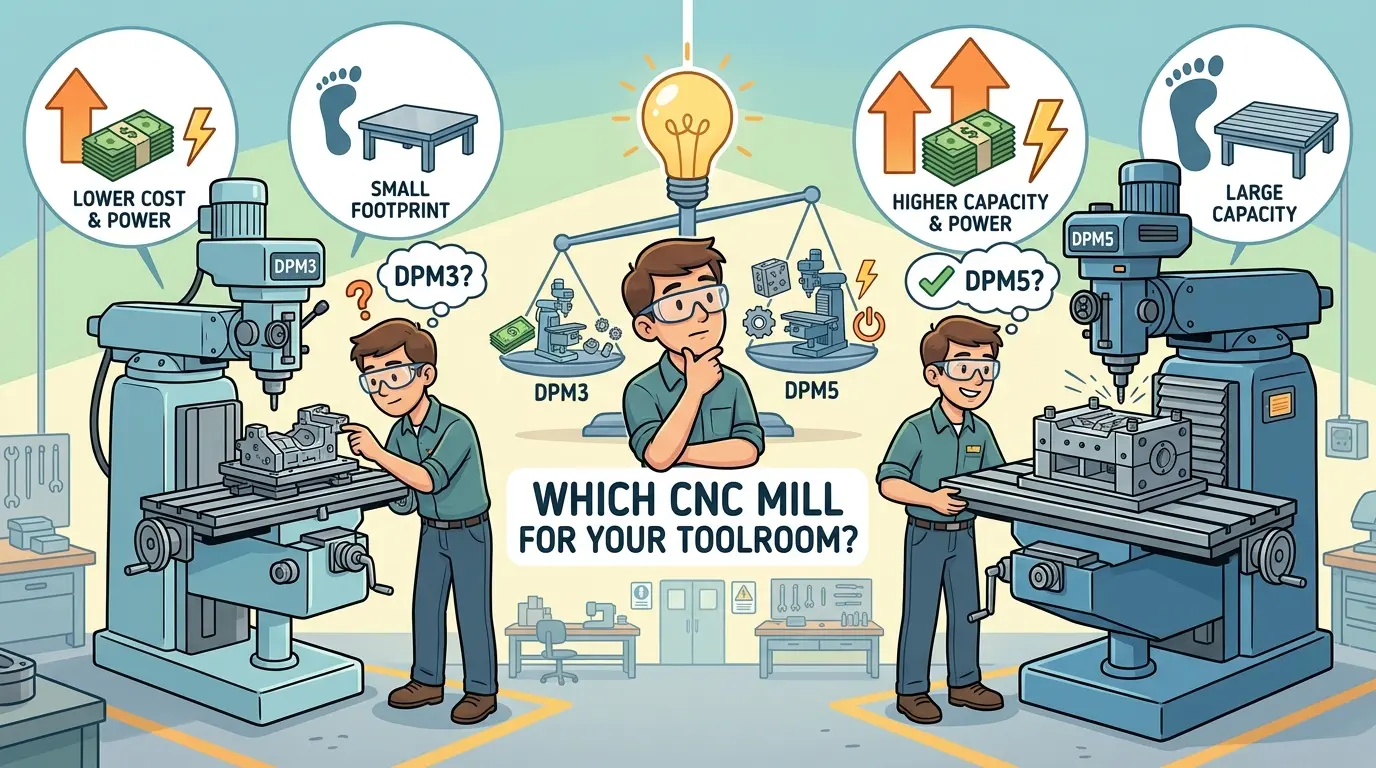
Toolrooms buy turnaround, not envelope size, yet many purchasing decisions default to the larger model without auditing the actual job mix. This comparison between the Trak DPM3 and DPM5 forces that audit: compact fixture work, urgent repair plates, and short-run utility parts reward a smaller, faster machine that keeps setup times low and floor space intact, while expanding fixture scale and repeated capacity pressure justify the bigger footprint. Before weighing spindle torque or axis travel, define which job families dominate your departmentâbecause the machine that protects rapid response, operator approachability, and existing tooling compatibility is the one that keeps the toolroom’s promise to the factory.
Toolrooms Buy Turnaround, Not Maximum Envelope
Production departments justify larger machines by measuring output and part coverage. Toolrooms operate on a different logic. Their value comes from compressing delay: making the repair part that stops a line from waiting another day, recovering a damaged fixture before the next shift, or running an urgent rework plate that production cannot absorb without losing scheduled time. In that environment, setup speed and operator comfort can outweigh raw capacity.
The wrong buying habit is assuming the larger model is automatically the better investment. Sometimes the bigger envelope simply brings more footprint, more idle capacity, and a worse fit into a department that survives by being fast and flexible. The right question is which machine protects the actual mix of repair, fixture, and short-run work without turning the toolroom into a miniature production floor that has lost its speed advantage.
This comparison is not about which machine is more impressive on paper. It is about which one keeps the toolroom’s promise to the factory: that urgent work gets done now, not eventually. Before looking at spindle power or axis travel, define the job families that actually arrive at the department door. That definition drives every other decision in this comparison.
The Smaller Machine Wins When Work Is Dense and Repetitive
Many toolrooms spend more time on compact utility work than on large dramatic parts. They machine fixture pieces, mounting plates, guards, repair blocks, brackets, jigs, and short-run components that are important but not huge. In those settings, the smaller machine often feels better because it is proportionate to the work. It is easier to keep active, quicker to load, and simpler to place inside a department that already contains benches, inspection space, storage, and manual equipment.
Consider a typical week in a mid-sized fabrication shop. The toolroom receives a damaged locating pin that must be remade before the afternoon shift, a set of four clamp blocks for a new fixture, and a replacement wear plate for a forming die. None of these parts exceed a 300 mm cube. None of them require a large envelope. What they require is quick access, fast setup, and the ability to move from one job to the next without hesitation.
Utilization is psychological as well as numerical. A machine that feels quick to use gets used. A machine that feels oversized for most tasks often gets reserved only for “serious jobs,” which quietly reduces the day-to-day value the toolroom extracts from it. For departments dominated by compact fixtures, repair parts, and fast-response jobs, the smaller format can be the stronger operational answer even if it loses the capacity contest on paper.
There is also a practical loading advantage. Smaller tables sit at a comfortable working height for manual setup. Operators can reach across the work area without stretching, and workholding can be arranged with less planning. When a job arrives at 2:00 PM and must be finished by 4:00 PM, these small ergonomic advantages compound into real time savings.
The Larger Machine Wins When Fixture Scale Keeps Expanding
The case for the larger model strengthens when the toolroom is repeatedly asked to support bigger plates, larger repair components, longer workpieces, or tooling assemblies that push the smaller machine too close to its practical limits. This usually happens in factories where product size, fixture scale, or internal tooling complexity has grown over time. The toolroom still thinks of itself as a flexible support department, but the physical size of the jobs has changed.
When that happens, a smaller machine may remain theoretically useful while becoming commercially awkward. Too many setups require compromise. Too many jobs need creative positioning or second operations. Too many urgent tasks arrive that “almost fit.” In that context, the larger machine stops being a prestige upgrade and becomes a way to prevent the toolroom from losing time to avoidable workarounds.
Imagine a toolroom that supports a line producing large agricultural equipment. The fixtures for that line have grown over several product generations. What used to be a 400 mm base plate is now a 700 mm weldment with machined pads. The smaller machine can still handle the job, but only by repositioning the part twice, indicating from a reference edge, and accepting a longer cycle time. Multiply that by a dozen fixtures per year, and the toolroom has quietly lost days of productive time to workarounds that the larger machine would eliminate entirely.
The right test is not whether the larger machine could do more. It is whether the current work is already pushing the smaller lane often enough to slow the department down. Track the last six months of jobs. How many required creative setup? How many needed a second operation because the first pass could not reach all features? How many were delayed while waiting for another machine to free up? If the answers point to a pattern, the larger machine is not a luxury. It is a correction.
Conversational Productivity Only Pays Off If the Machine Fits the Job Rhythm
Trak-style toolroom mills remain attractive because they match the way many toolrooms actually think. They support quick-turn work, conversational or operator-friendly programming logic, and a workflow that does not always look like formal CAM-driven production. That is a strength. But the programming advantage only pays off if the machine itself fits the rhythm of the jobs being programmed.
Conversational programming shines when the operator can stand at the control, answer a few prompts about hole patterns, pocket dimensions, or facing passes, and generate a program in minutes. That workflow suits repair work and simple fixtures perfectly. It loses its advantage when the part is too large to fit comfortably, because the operator then spends time on setup gymnastics instead of programming.
If the department mainly needs quick repair and utility responses, a smaller conversationally productive machine can be ideal. If the jobs are increasingly large, multi-setup, and approaching short-run production behavior, the programming ease may remain valuable while the smaller format stops being enough. In that case the larger machine is not replacing conversational productivity. It is extending the range of jobs that can benefit from it.
Buyers should evaluate programming style and physical capacity together. A toolroom machine is not only an iron decision. It is a response-style decision. Ask whether the conversational interface will be used on 80 percent of the jobs or only on the ones that fit. If a significant share of work requires CAM programming or manual code because the part exceeds the conversational envelope, part of the machine’s value proposition disappears.
Floor Space in Toolrooms Is More Expensive Than Buyers Admit
Production departments often plan space around big equipment. Toolrooms usually do not have that luxury. They need benches, manual work areas, storage, inspection access, incoming damaged components, and often several different repair or fabrication activities happening at once. That makes floor space unusually valuable.
A larger mill can therefore cost more than its price tag suggests if it forces the department to sacrifice useful support space. Buyers should be honest here. Will the bigger machine merely fit, or will it degrade the toolroom’s overall responsiveness by crowding everything else? Toolrooms lose value when the department starts moving slower because people, carts, and jobs cannot circulate comfortably.
Walk through the department before making a decision. Measure the aisle width. Look at where the incoming damaged parts are staged. Check whether the inspection bench can stay where it is. Consider the path from the machine to the manual work area where operators do fitting and finishing. If the larger machine forces any of these paths to narrow or disappear, the cost of the machine goes beyond its purchase price.
This is one reason smaller models sometimes outperform expectations in toolrooms. Their value comes not only from what they can machine, but from what they allow the rest of the room to keep doing. A toolroom that can keep its benches, its staging area, and its circulation paths intact is a toolroom that can keep responding quickly. A toolroom that has been compressed around a large machine may find that every job now takes longer because the surrounding workflow has been disrupted.
Operator Mix Often Decides the Better Model
Some toolrooms are run by deeply experienced machinists who are comfortable stretching setups and extracting value from whatever machine is available. Others have mixed-skill staffing, rotating coverage, or a blend of experienced and developing operators. That difference matters because the bigger-capacity machine is not always the easier machine to keep productive across multiple users.
Consider how the department actually assigns work. If a single senior machinist handles every job on the mill, that person’s preferences and experience level should drive the decision. If the mill is shared across shifts, or if apprentices and newer operators are expected to run urgent jobs when the senior person is busy, the machine needs to be approachable for a wider range of skill levels.
If the department needs a mill that several people can approach quickly for urgent jobs, the smaller and more immediately approachable option may generate better overall response. If the department has a narrower, highly skilled user base and repeatedly sees larger or more awkward work, the larger machine may be fully justified.
The best toolroom comparison includes operator coverage. The machine should fit not only the job but also the people who will need to run it under time pressure. A machine that only one person can use effectively is a bottleneck, regardless of its capacity. A machine that five people can approach confidently is an asset that multiplies the department’s responsiveness.
Maintenance and Uptime Questions Should Be Read Through Department Risk
Toolrooms do not always run the highest spindle hours in the factory, but the cost of downtime can still be severe because their work is often urgent by definition. A machine outage in the toolroom can mean a delayed repair, an extended production interruption, or a fixture that remains out of service longer than expected. That makes supportability and maintenance logic important.
The larger machine may bring broader capacity, but buyers should still ask whether it also brings a maintenance burden or space impact that the department does not really want. The smaller machine may be easier to keep integrated and active, but only if it covers enough of the department’s real tasks to avoid constant escalation to outside resources or other departments.
Think about the failure modes that actually occur in a toolroom environment. A machine that sits idle for two days and then runs a heavy interrupted cut on a repair part has different stress patterns than a machine that runs the same cycle continuously. Spindle bearings, way covers, and coolant systems all respond to that usage pattern differently. The maintenance plan should match the actual duty cycle, not the theoretical maximum.
Uptime risk in a toolroom is not just about machine reliability. It is about what happens to the factory when the toolroom cannot respond as quickly as expected. A repair part that takes three days instead of one because the mill is down can shut down a production line. That cost is far higher than any difference in machine price. Buyers should verify that the chosen model has a reasonable service network, available spare parts, and a maintenance routine that fits the department’s actual schedule.
A Toolroom Comparison Table Should Start With Job Families
| Toolroom Pattern | DPM3-Type Logic Usually Fits Better | DPM5-Type Logic Usually Fits Better |
|---|---|---|
| Dominant work | Compact fixtures, repairs, utility parts, urgent small jobs | Larger plates, broader fixture bases, longer repair components |
| Department layout | Dense room where floor space and access matter | Toolroom with enough space to support larger-machine use cleanly |
| Response priority | Fast setup and frequent small interventions | One-machine coverage for a wider size band |
| Operator mix | Multiple users need quick familiarity | Experienced users handling larger and more varied setups |
| Capacity pressure | Size is rarely the main bottleneck | Size limits are already causing delays or awkward workarounds |
| Typical cycle time | Short cycles, frequent job changes | Longer cycles, fewer but larger setups |
| Workholding approach | Simple vises, clamps, quick fixtures | Larger vises, sub-plates, dedicated fixture bases |
This table translates the purchase into department behavior. The better machine is the one that matches how the toolroom actually earns its value. Use it as a starting point for discussion with the team, not as a final answer. The real decision comes from walking through the job list and matching each family to the machine that handles it with the least friction.
Watch for the Sign That the Toolroom Is Becoming a Short-Run Production Cell
Some departments say they are toolrooms but behave more and more like small production cells. They run repeated internal batches, larger family-of-parts work, and extended machining sessions that go beyond repair and utility response. When that shift happens, the DPM3 versus DPM5 decision may be signaling a larger organizational change. The department may be asking for more capacity because its mission is expanding.
That matters because the correct answer might not be only “buy the larger toolroom mill.” The correct answer might be to revisit whether the department now needs a broader comparison against vertical machining center versus standard CNC mill choices. If the workload is evolving away from classic toolroom logic, forcing the decision to stay inside a narrower frame can hide the real need.
Look at the job history over the past year. How many jobs repeat? How many are one-off repairs? How many are small batches of five or ten identical parts? If the repeat work is growing, the department may need features that a toolroom mill does not emphasize: automatic tool changers, higher spindle speeds, or more rigid cutting capability. Those features belong to a different machine category entirely.
Toolrooms should read repeated capacity pressure as information, not just as justification for one larger model. The pressure may be telling you that the department’s role is changing. If that is the case, the right investment might be a different class of machine, not a larger version of the current one.
Legacy Toolroom Expectations Still Matter
Another useful lens is to compare the new choice against the older toolroom mindset the department may still carry. Many toolrooms are culturally shaped by versatile, operator-driven equipment where response speed mattered more than high-volume optimization. If that remains true, the smaller machine may fit the department’s DNA better. If the department has already moved beyond that mindset and now expects broader part coverage and more formal CNC behavior, the larger machine may be more aligned.
Some buyers still find it useful to think about the broader spectrum of legacy and specialist toolroom mill logic. The issue is not nostalgia. It is understanding whether the department still wins by being nimble or now wins by covering a wider size range.
That cultural fit often predicts satisfaction better than spec-sheet enthusiasm. A department that has always valued the ability to walk up to a machine, indicate a part, and start cutting will feel constrained by a machine that requires formal programming for every job. A department that has already adopted CAM workflows and expects consistent, repeatable cycles will feel frustrated by a machine that cannot hold tight tolerances across a large envelope.
Talk to the operators who will use the machine daily. Ask them what they value in the current setup and what frustrates them. Their answers will reveal whether the department’s culture aligns more with the smaller or larger model. The machine that matches the team’s working style will generate better results than the machine that merely has the right specifications.
Workholding and Setup Time: The Hidden Differentiator
Setup time is where the two machines diverge most in daily practice. The smaller machine encourages simple workholding: a precision vise, a few clamps, maybe a small sub-plate. These setups take minutes, not hours. The operator can mount a part, indicate it, and start cutting while the job is still fresh in mind.
The larger machine invites a different approach. With more table area, operators often build more elaborate setups: larger vises, dedicated fixture plates, multiple parts per setup. That can be efficient for repeat work, but it adds setup time for one-off repairs. A job that takes ten minutes to set up on the smaller machine might take forty minutes on the larger one, simply because the workholding system is heavier and more complex.
For a toolroom that lives on one-off and small-batch work, that setup time difference matters. It is not just the minutes spent mounting the part. It is the mental overhead of planning a larger setup, the physical effort of moving heavier workholding components, and the reduced flexibility to change jobs quickly when an urgent request arrives.
Consider also the chip handling and coolant management. A larger machine produces more chips in a given cycle, which means more frequent cleaning and more attention to coolant levels and filtration. In a busy toolroom, those maintenance tasks compete with the actual machining work. The smaller machine is simpler to keep clean and ready for the next job.
Cutting Capability and Material Realities
Toolroom work often involves materials that are not ideal for machining: worn steel with hard spots, welded assemblies with inconsistent hardness, castings with sand inclusions, or heat-treated components that need careful stock removal. The machine’s rigidity and spindle power determine how well it handles these variable conditions.
The larger machine typically offers more rigidity and more torque, which helps when cutting tough materials or taking heavier passes. That can be a real advantage when the toolroom regularly machines hardened steel or large weldments. The smaller machine may require lighter cuts and more passes, which extends cycle time but may still produce acceptable results.
However, most toolroom work does not demand maximum metal removal. It demands accuracy and surface finish on parts that are often small and detailed. For that work, the smaller machine’s lighter spindle can actually be an advantage, because it is easier to control and less likely to chatter on delicate features. The operator can take fine finishing passes with confidence, knowing that the machine will hold the tolerance.
The material reality of the department should drive this part of the decision. If the job list is dominated by aluminum, mild steel, and plastics, the smaller machine is likely sufficient. If the list includes hardened tool steel, stainless alloys, or large weldments, the larger machine’s rigidity becomes more valuable.
Inspection and Quality Control Integration
Toolroom parts often require verification before they are released to production. A repair part that fails inspection means the line stays down longer. A fixture that is out of tolerance creates scrap in the production process. The machine’s ability to support accurate machining directly affects the inspection workload.
The smaller machine, with its tighter work envelope, often holds tolerances more consistently because thermal growth and deflection are lower. The larger machine, with more mass, may take longer to reach thermal stability but can hold size across a larger part. Both are valid, but they suit different inspection strategies.
If the toolroom uses in-process inspection, with the operator checking features as they go, the smaller machine’s accessibility is an advantage. The operator can reach the part easily, measure, and make adjustments without breaking down the setup. If the toolroom relies on post-process inspection at a CMM or surface plate, the larger machine’s ability to complete more features in one setup reduces the number of inspection events.
Consider also how the machine’s accuracy interacts with the department’s quality system. If the toolroom is ISO-certified or works to customer-specific quality requirements, the machine’s repeatability and the operator’s ability to document the process matter. Both machines can support that, but the workflow around them differs.
Power and Utility Requirements
Before committing to either machine, verify the department’s electrical and compressed air capacity. The larger machine typically draws more power, may require a dedicated circuit, and might need higher-capacity air supply for the tool changer or coolant system. The smaller machine is often easier to integrate into existing utility infrastructure.
This is not a glamorous consideration, but it is a practical one. A machine that requires a new electrical panel or a larger air compressor adds cost and installation time. A machine that plugs into existing utilities can be running within days of delivery. For a toolroom that needs to maintain production while the new machine is installed, the smaller machine’s simpler utility requirements are a real advantage.
Check also the floor loading. A larger machine is heavier and may require a reinforced foundation or special leveling. The smaller machine can often sit on a standard shop floor with minimal preparation. That difference affects installation cost and timeline.
Tooling and Accessory Compatibility
The department’s existing tooling inventory should influence the decision. If the toolroom already owns a set of toolholders, vises, and cutting tools sized for a smaller machine, the smaller model will use them directly. The larger machine may require larger toolholders, bigger vises, or longer reach tools, which adds cost beyond the machine itself.
Consider also the spindle taper and tooling interface. If the department standardizes on a particular taper, the new machine should match that standard to avoid maintaining two separate tooling systems. The larger machine may use a different taper, which means new holders and potentially new tooling for every job.
Tooling compatibility also affects setup time. An operator who can reach for a familiar toolholder and know it will fit is faster than one who must search for the right adapter or modify an existing tool. The smaller machine’s compatibility with existing tooling reduces friction and keeps the department moving.
Training and Skill Development
The learning curve for each machine differs. The smaller machine, with its conversational interface and simpler setup, is easier for new operators to learn. The larger machine, with more capacity and potentially more complex controls, may require more formal training.
If the department has a steady flow of apprentices or cross-trained operators from other areas, the smaller machine’s approachability is a benefit. New operators can contribute sooner, and the senior staff can focus on the more complex jobs. If the department has a stable, experienced team, the training curve matters less.
Training also affects the department’s ability to cover shifts and vacations. A machine that several people can operate confidently is easier to schedule around. A machine that only one or two people can run creates scheduling constraints and increases the risk of downtime when those people are unavailable.
Resale Value and Future Flexibility
Toolroom machines are long-term investments, but departments change. Product lines shift, factory layouts evolve, and the mix of work can change dramatically over a few years. Consider how each machine holds its value and how easily it could be redeployed if the department’s needs change.
The smaller machine is often easier to sell or repurpose because it fits a wider range of shops. The larger machine may have a narrower market but can command a higher price if it is well-maintained. Neither is a bad investment, but the risk profile differs.
Think also about the department’s growth trajectory. If the factory is expanding and the toolroom is likely to take on more work, the larger machine provides headroom. If the factory is stable or contracting, the smaller machine may be the more prudent choice, avoiding idle capacity that ties up capital.
Choose the Machine That Best Protects the Toolroom’s Promise
The promise of a toolroom is not maximum capacity. It is dependable response. That is the standard the DPM3 versus DPM5 decision should serve. If the department mainly lives on compact urgent work, smaller fixtures, and quick-turn utility parts, the smaller machine may be the best investment because it protects speed, access, and room function. If the work has clearly grown into larger fixture and repair territory, the larger machine may be the only honest way to keep that promise without constant compromise.
The smartest buyers do not ask which model sounds more serious. They ask which one best protects the toolroom’s actual role inside the factory. Once that role is defined clearly, the right machine usually stops looking like a prestige choice and starts looking like the obvious fit.
Run the comparison through the department’s real job list. Measure the floor space. Talk to the operators. Check the utility infrastructure. Review the tooling inventory. Each of these practical checks will point toward one machine or the other. The machine that survives all the checks is the one to buy.
For toolrooms that need to see the options side by side, reviewing the current lineup of toolroom mills and related equipment can help clarify what fits the department’s workflow. The useful comparison is the fit between the mill and the toolroom’s work, not a universal ranking. It is about which machine serves this toolroom, this team, and this factory’s response requirements. That is the only standard that matters.