Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
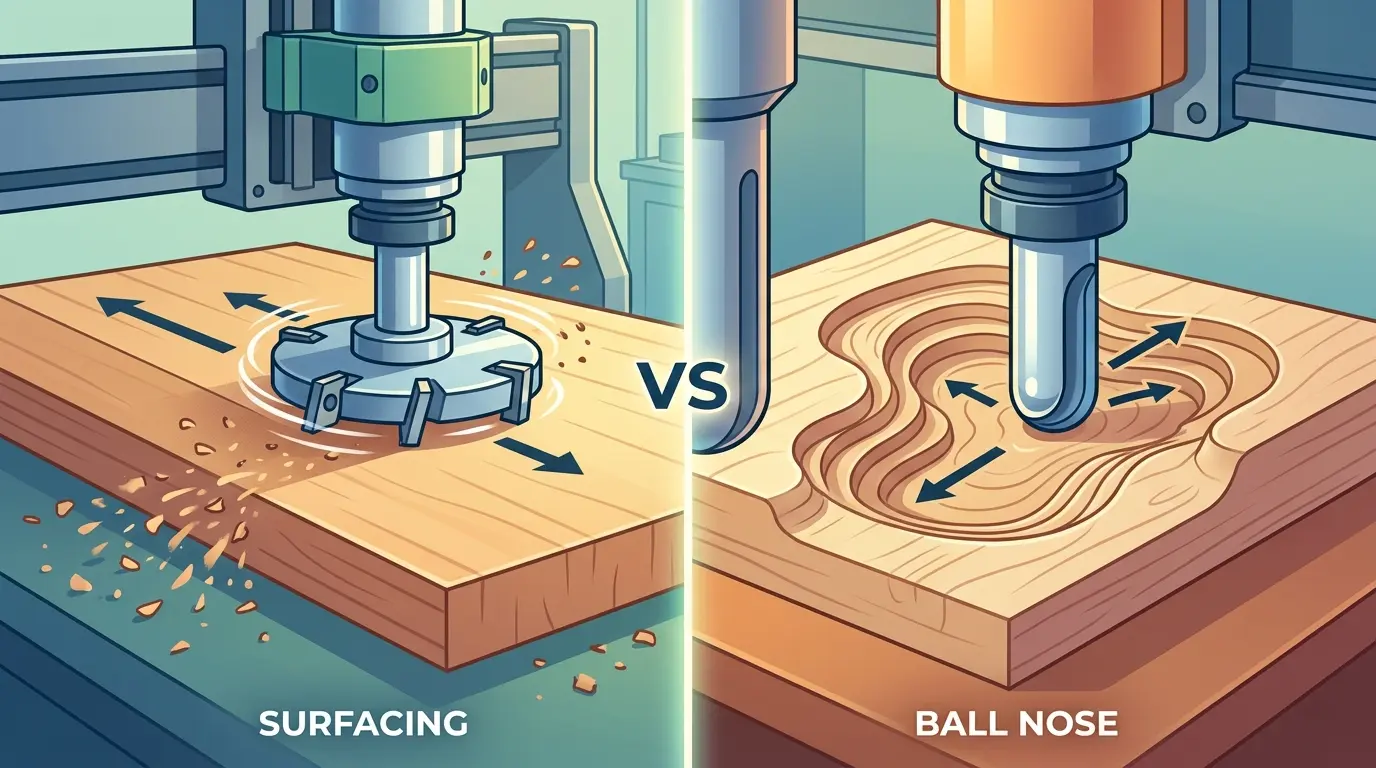
Every routing shop eventually faces the moment when a surfacing bit and a ball nose cutter are both loaded in the tool rack, and the CAM file is waiting for a decision. The temptation is to pick whichever tool is already in the spindle, but that shortcut usually transfers cost into sanding time, ugly cutter marks, and toolpaths that fight the cutter’s geometry. This article cuts through the versatility debate by anchoring the choice to the surface outcome each stage requires—planar coverage versus continuously changing contour—and explains why forcing one tool to own both jobs slows production and inflates finishing labor.
Start With The Surface, Not The Tool Debate
Surfacing bits and ball nose router bits get compared as if one is inherently better than the other. That framing misses the point. These cutters solve different problems at different stages of a routing job. A surfacing bit is built to create a plane. A ball nose tool is built to follow changing geometry. The right choice becomes obvious once you define what surface the next operation actually requires.
If the job calls for a broad, dependable flat face, a surfacing bit owns that stage. If the job involves curves, blended slopes, or three-dimensional contours, a ball nose tool owns that stage. The costly mistake is forcing one tool to handle both jobs poorly simply because it is already loaded in the spindle or already set up in CAM.
Define The Required Surface Outcome First
Before selecting a bit, determine what the workpiece must become after that operation. Are you establishing a reference plane on a slab, spoilboard, panel, or glued-up assembly? Are you preparing a flat surface before carving, cutting, or finishing? Or are you describing a contour where the surface direction changes continuously?
This distinction drives everything downstream. Shops that pick cutters from habit often write the wrong toolpath, take longer cuts than necessary, and push extra sanding or cleanup work into later stages. Shops that start from the required surface outcome make the tool choice quickly because the geometry tells them what stage they are programming.
Surfacing Bits Own Plane-Creation Work
Surfacing bits deliver value through coverage and planar material removal. They are the practical choice for flattening spoilboards, truing slabs, leveling large glued panels, cleaning broad faces, and preparing flat reference surfaces before subsequent routing operations. Their job is not to interpret subtle geometry. Their job is to remove material efficiently across an area and leave a surface the next step can trust.
That is why surfacing bits belong near the front of the workflow. They establish the plane that later operations assume already exists. When dealing with warped stock, inconsistent slab thickness, or a work surface that must become dependable before dimensional or decorative work begins, the surfacing bit is usually the correct owner of that first stage.
Ball Nose Tools Own Changing Geometry
Ball nose cutters create value where the surface changes direction continuously. Relief carving, sculpted shapes, contoured signwork, radiused blends, shallow 3D finishing, and shaped transitions all benefit from the rounded tool form because it traces changing geometry more naturally than a broad flat cutter. The rounded profile leaves a more manageable pattern on curves and lets the CAM strategy follow the part’s shape rather than trying to flatten it.
That is why the ball nose tool is typically a contouring or finishing tool, not a flattening shortcut. If the part’s value lies in changing surface shape, the rounded profile makes more practical sense than forcing a surfacing cutter to behave like a geometry-following tool.
The Penalty Shows Up In Time, Not Immediate Failure
One reason shops keep making the wrong comparison is that either tool can often still produce a part. The machine does not fail dramatically. Instead, the penalty appears in slower machine time, uglier cutter marks, more sanding, CAM frustration, and a surface that took too much effort to reach acceptable quality.
Flattening with a ball nose tool is a classic example. The tool may eventually get the stock level, but coverage is inefficient and the resulting pattern creates more cleanup burden than necessary. Trying to finish changing contours with a wide surfacing bit causes a different kind of waste. The tool does not follow the shape the way the part wants to be followed, so the route becomes awkward and the visible result reflects that mismatch.
Cutter Marks Create Different Cleanup Burdens
Think about the mark pattern each tool leaves behind. A surfacing bit is designed to cover area and leave a planar cut pattern that makes sense on wide flat work. Its strength is efficient overlap across broad faces. A ball nose cutter leaves a different visual and tactile pattern because it moves through changing geometry and depends on controlled step-over to manage scallop height on contours.
This matters because the wrong cutter choice often transfers its cost into sanding and finish preparation. If the routed face will be stained, painted, laminated, or used as a visible decorative surface, the character of the cutter marks matters almost as much as raw cycle time. Shops that ignore this often think they saved time in routing when they actually moved the cost into manual finishing.
Toolpath Strategy Must Follow Cutter Shape
The cutter and the toolpath are a pair. A surfacing bit expects wide overlap, planar coverage, and a route designed to clean an area efficiently. A ball nose tool expects a strategy built around contour quality, step-over discipline, and surface continuity. Even when both tools touch the same workpiece, they almost never want the same style of CAM logic.
This is where repeated inefficiency gets locked into production. A convenient path style gets reused because it already exists in software, not because it suits the cutter. The result is a route that technically runs but never feels elegant. Treat tool choice and toolpath choice as one decision. If one changes, the other usually needs to change with it.
Step-Over Means Different Things For These Two Tools
A broad surfacing cutter and a ball nose cutter react to step-over differently because they are trying to leave different kinds of surfaces. With surfacing, overlap is about efficient coverage and how cleanly the bit establishes a plane without visible ridges that create unnecessary cleanup. With ball nose finishing, step-over becomes closely tied to scallop pattern, contour smoothness, and the amount of secondary finishing the part will require.
Do not transfer step-over habits from one cutter family to the other. The same number does not mean the same thing. A choice that feels efficient on planar surfacing can leave an unacceptable contour texture with a ball nose tool, while a very fine contour-finishing approach can waste enormous time if misapplied to broad planar stock preparation.
Material Changes Sensitivity, Not The Core Decision
Wood, MDF, plywood, laminated board, acrylic, and composites do not respond the same way to heat, chip evacuation, edge quality, or finish expectations. That affects how carefully the route must be tuned and how expensive a poor cutter decision becomes. But material does not change the core rule. The first decision still comes from surface geometry.
Flat work points toward surfacing. Continuously changing form points toward ball nose finishing. Material mainly changes how forgiving the process will be if the setup, step-over, or cutter condition is less than ideal. In abrasive or finish-sensitive materials, the wrong cutter choice simply becomes more expensive faster.
Machine Stability Can Make A Good Tool Look Bad
Neither cutter should be judged in isolation from the machine and setup supporting it. Weak hold-down, spindle runout, excessive stick-out, poor spoilboard condition, or unstable stock can make either tool look worse than it is. A surfacing bit may leave ridges on a slab that is moving slightly. A ball nose tool may leave rough contour quality or ugly step lines because the assembly is vibrating, not because the cutter concept is wrong.
Tool performance has to be read together with spindle truth and workholding logic. Shops running larger routing cells or nesting machines already know that cutter choice and support strategy are closely linked. If the platform is not stable, the route will mislead the buyer about what the tool is actually capable of.
One Job Often Needs Both Tools In Sequence
Many real jobs are not a choice between one tool and the other. They are a staged workflow. A slab may need a surfacing pass before decorative carving. A sign blank may need one clean plane before relief detail begins. A shaped panel may need the reference face established first and the visible contour finished second. In these cases, forcing one tool to own the whole route usually adds time and cleanup instead of saving it.
The staged approach often performs better commercially because each cutter is allowed to do the work it was built to own. The surfacing bit establishes truth quickly. The ball nose tool follows geometry cleanly. That division usually produces a better finish path and less manual correction afterward.
Ask The Right Questions Instead Of Debating Versatility
Buyers and operators often ask, “Which bit is more versatile?” That sounds practical, but it pushes the decision in the wrong direction. Versatility often becomes a trap because one tool gets forced into stages it does not own well.
More useful questions are:
- Am I creating a flat reference or following a changing contour?
- Is this a preparation stage or a visible finishing stage?
- Where will the cost show up if the cutter marks are wrong: in machine time, sanding, or both?
- Does the machine setup support the cutter honestly?
- Will the workpiece benefit from a two-tool sequence instead of a one-tool compromise?
Those questions get closer to production truth than any general debate about which tool is supposedly better.
Quick Shop Scenarios Make The Decision Easier
If the shop is flattening a spoilboard, leveling a slab, or preparing a large glued panel, the surfacing bit is usually the obvious answer because the stage is about establishing a plane efficiently.
If the shop is finishing relief carving, 3D signwork, shallow sculpted forms, or radiused shape transitions, the ball nose tool is usually the better answer because the stage is about following geometry with a cleaner contour pattern.
If the job is a decorative panel that needs both a true base plane and later shaped detail, the practical answer is often both tools in sequence.
If the shop is trying to use one tool only because changing tools feels inconvenient, that is usually a warning sign that the workflow is being organized around convenience instead of surface outcome.
Tooling Discipline Still Matters After The Tool Family Is Chosen
Even once the correct cutter family is selected, basic tooling discipline still controls quality. Worn holders, poor clamping, too much projection, or neglected cutter condition will weaken the result no matter which tool is conceptually right. Shops that want to improve the larger picture should also pay attention to bits, holders, and wear factors that affect routing quality instead of treating bit selection as the whole story.
That matters especially in finish-sensitive work where a correct tool family can still underperform if the rotating chain is not stable. The right bit cannot rescue a careless setup.
Choose the cutter by the surface the stage needs to create. If the route needs a broad, dependable plane, let the surfacing bit own it. If the route needs changing geometry to be described cleanly, let the ball nose tool own it. When both surfaces appear in the same job, let both tools do their proper work instead of forcing one compromise cutter through the whole part.