Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
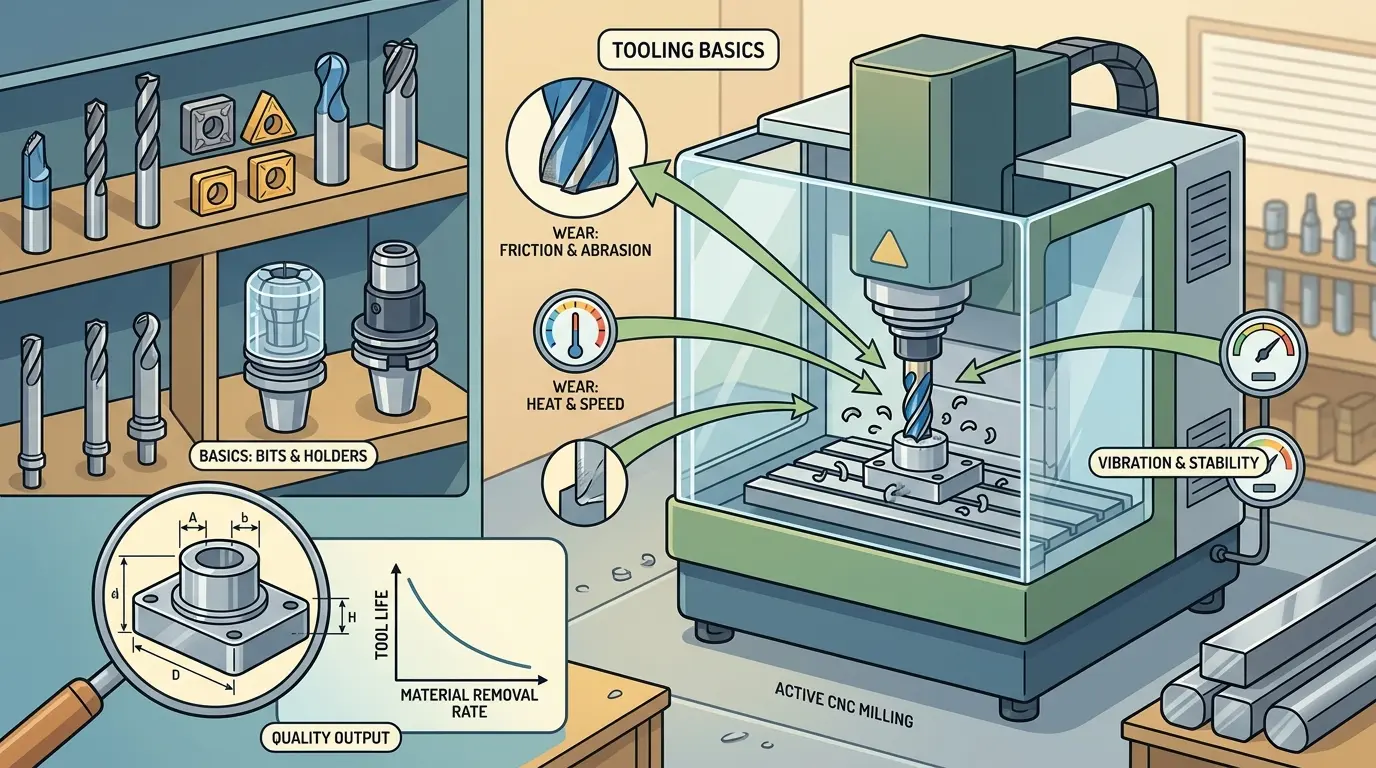
When a CNC router starts producing rough edges, drifting dimensions, or premature tool failure, the instinct is often to blame the program or the machine frame. Yet in most shops, the real loss of control happens much closer to the workpiece: in the rotating assembly of cutter, holder, collet, and clamping interface. This article walks production teams through the practical decisions that determine whether that assembly holds or breaks down. From matching tool geometry to specific operations, controlling stick-out and runout, to standardizing tool libraries, the guidance explains why tooling discipline—not just brand selection—is the first place to troubleshoot quality problems and protect repeatability across shifts.
Why Quality Problems Often Start at the Tool, Not the Machine
When a CNC router starts producing rough edges, inconsistent finishes, or premature tool failure, the first instinct is often to blame the program, the feed rate, or the machine itself. But in many shops, the actual source of the problem is much closer to the workpiece: the rotating assembly that carries the cutter. The spindle may be perfectly healthy, the servo drives may be accurate, and the machine frame may be rigid, but if the tool, holder, collet, and clamping interface are not in good condition, the cut will be unstable from the first pass.
This is why tooling deserves more attention than it typically gets. Tooling is not just a consumable cost center. It is the first point where process control either holds or breaks down. Shops that treat tooling as part of their quality system troubleshoot faster, repeat jobs more reliably, and get more value from the machine platform they already own.
The Rotating Assembly Is What the Part Actually Sees
From the workpiece’s perspective, the machine is filtered entirely through the tool assembly. The spindle may be true, the structure may be rigid, and the control may be precise, but the cut will still be compromised if the rotating chain is weak. A cutting edge that starts work with runout, poor clamping, excessive projection, contamination, or hidden wear is already at a disadvantage before it touches the material.
This is why tool-side problems often show up as symptoms that seem unrelated at first: shorter tool life, uneven surface finish, fragile small-diameter performance, noisy edges, or dimensions that drift. The machine looks innocent because it is moving exactly where it was told. The real loss of control is happening at the interface between the spindle and the material.
Match Tool Selection to the Operation, Not Just the Material
Material selection matters, but the operation matters just as much. A cutter that performs well in roughing is not automatically right for finishing. A tool that leaves a clean edge on one type of cut may struggle in a slot, pocket, contour, or long run of abrasive material. In routing environments, this becomes obvious when shops force a single cutter to handle flattening, edge finishing, contouring, and cleanup simply because it seems close enough.
The better question is not “What can this tool cut?” but “What job is this tool being asked to own?” If the answer is long-run panel processing, clean laminate edges, broad surfacing, contour finishing, tight drilling, or abrasive survival, the tool geometry should be selected for that task specifically. Compromise cutters can keep production moving, but they usually do so by forcing slower programs, more sanding, or more frequent correction later.
Roughing and Finishing Should Not Share the Same Tool Logic
One of the easiest ways to raise tooling cost quietly is to let roughing and finishing share one tool strategy out of habit. Roughing wants reliable material removal and a process window that stays productive. Finishing wants predictable surface quality, clean geometry, and a stable assembly that does not introduce avoidable marks or chatter. These are different priorities even when the material is the same.
Shops that scale well usually separate tooling by operation ownership rather than by vague general category. They define which cutter roughs, which cutter finishes, which one handles surface-sensitive work, and which one is only acceptable for broad stock removal. Once that distinction becomes part of the tool library, repeated jobs stop relying so heavily on individual operator judgment.
Holders and Collets Decide Whether Accuracy Survives Setup
A good cutter in a bad holder is still a weak production setup. Many shops learn this only after a problem becomes visible, yet holder and collet condition often decide whether the tool runs truthfully at all. They affect repeatability, rigidity, balance, and how much runout reaches the cutting edge. If that chain is weak, the machine will still move exactly as commanded while the cut itself becomes less predictable.
This matters especially in small-diameter work, finish-sensitive routing, drilling, and any operation where edge cleanliness is being watched closely. But it matters in heavier work too. Premature tool wear, odd chatter, drifting slot width, and uneven surface quality often trace back to worn collets, dirty contact surfaces, or inconsistent holder condition long before buyers admit that the clamping side deserves as much attention as the cutter brand.
Cleanliness at the Clamping Interface Is a Quality Variable
Contamination at the clamping interface is one of the least glamorous and most expensive tooling problems in production. A tool loaded into a dirty holder or clamped into an interface that is not maintained consistently does not start from a neutral condition. It begins work with hidden instability. The resulting symptoms can look like random wear, unreliable finish, or a cutter that inexplicably underperforms compared with the previous batch.
Disciplined shops standardize how tools are loaded, how holders are cleaned, how collets are inspected, and when those components are replaced. Cleanliness at the spindle end is not about appearance. It is about whether the tool begins its job in a repeatable mechanical state.
Tool Stick-Out Is One of the Fastest Ways to Lose Stability
Excess projection is common because it feels convenient. More stick-out makes the tool easier to load, easier to reach with, and easier to leave alone across several jobs. It also increases leverage on the assembly and reduces the margin against vibration, poor finish, and shortened tool life. In many shops, too much projection is one of the most consistent hidden causes of preventable instability.
The machine may still complete the part, which is why the mistake survives. But the route becomes weaker than it needs to be. Shops should treat tool projection as a controlled variable tied to the feature, not as a convenience choice that drifts by habit. If the feature does not need the extra reach, the process probably should not carry the extra risk.
Runout Damages the Process Before It Creates a Dramatic Measurement Problem
Runout is often discussed like a metrology topic, but on the floor it behaves more like a quality tax. The tool does not share load evenly. One flute works harder. Finish consistency drops. Small features become more fragile. Tool life shortens. Operators may keep adjusting feeds and speeds when the real issue is that the cutting edge is not rotating as truthfully as the setup assumes.
This is one reason small-diameter tools reveal problems earlier than larger ones. They have less margin for mechanical error. A process that appears acceptable with larger tools can fail quickly once smaller tools expose the weakness in the rotating chain. Shops that understand this usually diagnose fine-detail problems faster because they do not assume every symptom comes from the program.
Wear Starts Long Before the Defect Becomes Visible
Tool wear is often treated as a purchasing question, but on the machine it appears first as a process-stability question. Finish changes. Edge quality shifts. Burr behavior gets worse. Load rises. Heat rises. Tolerances become harder to trust. If the shop waits until a visible defect appears, then some portion of the batch has already paid for that delay.
The smarter question is not how long the tool can survive physically. It is how long it can perform without pushing the route into risk. That threshold changes by material, operation, and feature importance. A finish-critical pass should not inherit the same replacement rule as a roughing stage just because the tool family looks similar.
Tool Life Problems Usually Mean the Process Is Hurting the Tool
When tool life collapses, buyers often blame the cutter brand first. Sometimes that is fair. Often it is incomplete. Recutting chips hurts tools. Excess stick-out hurts tools. Runout hurts tools. Weak workholding hurts tools. A mismatched toolpath hurts tools. Poor evacuation and heat control hurt tools. In other words, the process often damages the tool long before the catalog gets a real chance to prove itself.
Mature suppliers and disciplined plants explain wear in process terms. They identify whether the root cause lives in clamping, heat, chip evacuation, tool selection, projection, or cutter loading strategy. That diagnosis is usually more valuable than any generic statement about premium tooling grades because it tells the shop where the next loss will come from if nothing changes.
Heat and Chip Evacuation Are Tooling Issues Too
Some tooling conversations become too narrow because they focus only on diameter, coating, or brand. But chip evacuation and heat behavior are tooling issues as well. A theoretically correct cutter can still underperform if chips are being recut or heat is building in a way the route does not manage well. When that happens, the tool seems weaker than it really is because the process is feeding it bad conditions.
Tooling has to be read together with path strategy and machine stability. The tool is not only a piece of geometry. It is part of a complete cutting system. Shops that treat it that way tend to get more value from ordinary tooling than shops that keep buying better cutters without fixing the conditions surrounding them.
Standardized Tool Libraries Convert Tooling From Habit Into Process
The strongest tooling environments are standardized. They do not rely on one operator remembering which cutter usually works or how much stick-out was used last time. They define which tool belongs to which operation, what holder it should use, how it should be loaded, what projection is allowed, and what replacement logic applies. That makes programming cleaner, setup more repeatable, and troubleshooting much faster.
Without that structure, repeated jobs drift. A similar cutter gets substituted. A holder with slightly different projection gets used. A tool stays in service too long because the last batch happened to survive. The part may still get produced, but the cell becomes harder to stabilize and harder to scale across operators or shifts.
This matters in high-throughput routing and panel work especially, where nesting machines depend on stable tool libraries if they are going to repeat cleanly over time. The machine platform can be capable, but the tooling system has to be equally organized.
Presetting and Tracking Matter Once Volume Increases
Low-volume expert shops can sometimes run on experience and close observation alone. As soon as volume rises, shift coverage widens, or repeat jobs multiply, presetting and wear tracking become more important. The plant needs a reliable way to know which tool was loaded, how much life it has consumed, and whether the current setup matches the approved production condition.
That does not require unnecessary bureaucracy. It requires enough structure to stop tooling decisions from becoming tribal knowledge. Part counts, processed area, run time, or scheduled replacement intervals can all work if they are applied consistently. The point is to prevent wear and substitution from drifting invisibly into the process.
Tooling Problems Often Masquerade as Machine Problems
One of the most expensive diagnostic mistakes in CNC work is blaming the machine too early. Finish gets rough, tools wear quickly, dimensions drift, or contour quality becomes inconsistent, and the first reaction is to suspect the spindle, the frame, or the control system. Sometimes the machine really is part of the issue. Just as often, the first problem lives in the tooling chain.
Tooling review should come early in troubleshooting. Check holder condition, clamping cleanliness, runout, projection, wear history, and cutter-task fit before assuming the machine platform itself is failing. Shops that do this save time because they examine the most exposed failure point first.
The Best Tooling Question Is Usually Not “Which Brand?”
Brand matters, but it should come after clearer operational questions:
- Which operation is consuming the most tool life?
- Where does finish begin to drift before tools are replaced?
- Which critical features depend on the cleanest holder condition?
- Is wear tracked deliberately or only noticed after defects appear?
- Are tools being selected by task, or by habit?
- Is the current process damaging the tool before the tool has a fair chance to perform?
Those questions reveal whether the plant is treating tooling as a controlled production input or as a pile of consumables stored near the machine.
Spend Tooling Budget Where It Protects Repeatability
Not every tooling dollar has equal impact. Shops sometimes spend aggressively on premium cutter brands while neglecting holder condition, collet replacement, loading discipline, or standardized projection rules. That usually creates a distorted tooling budget where the visible cutting edge is upgraded but the support chain stays weak.
The better spending pattern protects repeatability first. Buy cutter quality appropriate to the operation, but do not neglect the clamping and process discipline that let the cutter perform honestly. In broader production planning, including the Pandaxis machinery lineup, machine quality and tooling discipline should support each other rather than compensating for one another.
Treat bits, holders, collets, projection, cleanliness, and wear control as one quality system. When those basics are controlled well, the machine has a fair chance to deliver the finish, accuracy, and output the route was designed for. When they are controlled poorly, the machine gets blamed for problems that started much closer to the spindle. Tooling basics matter because that is where machining reality begins.