Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
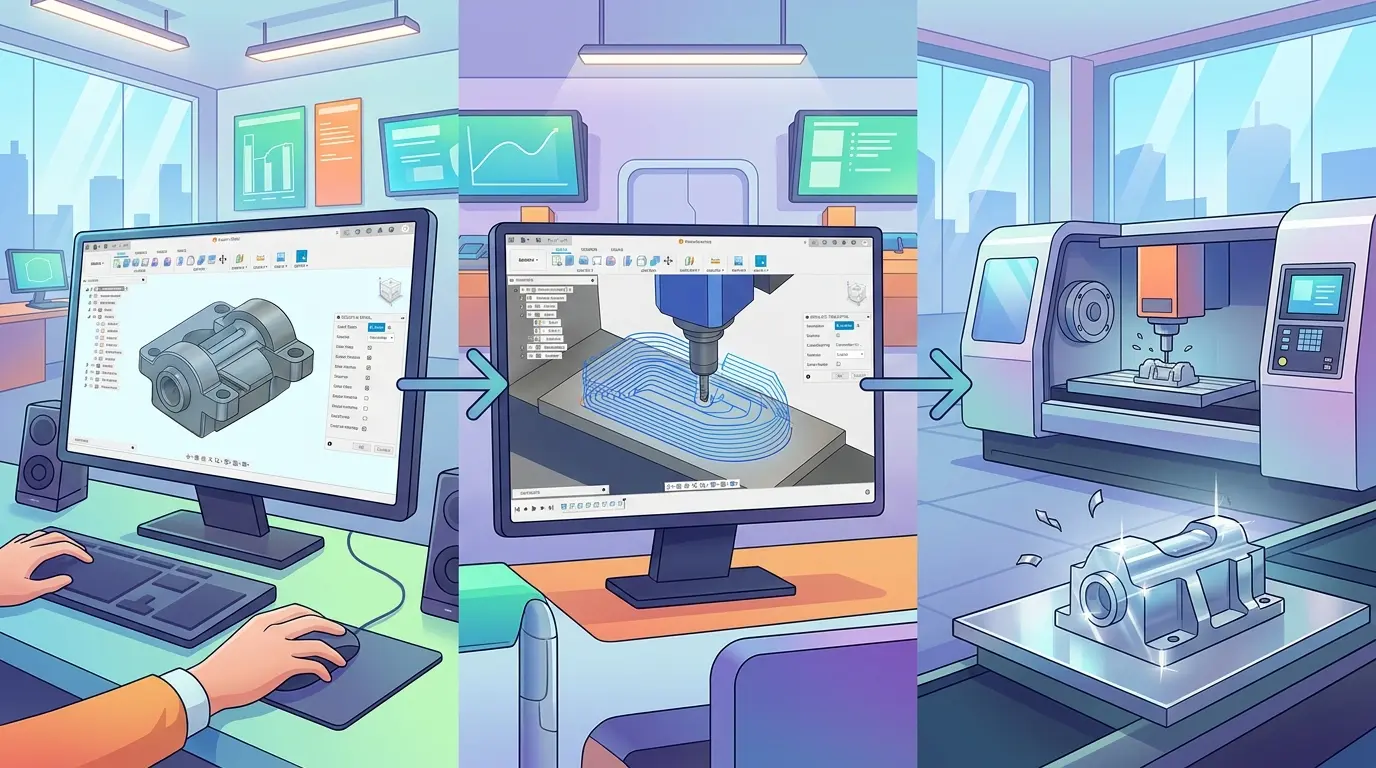
Most CNC programming failures are not born at the machine but in the gap between a finished CAD model and a ready-to-run toolpath. A part can be dimensionally perfect on screen yet awkward to hold, inefficient to cut, or dependent on tooling the shop never runs. This article walks production teams through a disciplined CAD-to-toolpath workflow that tests manufacturability before material is committed, aligns setups with real table conditions, and keeps tool libraries honest. The payoff is fewer scrapped parts, less rework, and calmer spindle time.
Why the CAD-to-Toolpath Gap Creates Real Shop-Floor Problems
Most CNC programming mistakes are not made at the machine. They are made earlier, in the space between a finished CAD model and a ready-to-run toolpath. A part can be dimensionally perfect on screen and still be a problem on the floor: awkward to hold, inefficient to cut, poorly sequenced, or dependent on tooling the shop does not actually run. That gap between design intent and machine reality is where rework, scrapped material, and lost spindle time come from.
The job is not to move from drawing to G-code as quickly as possible. The job is to move from design intent to a machine-ready route with fewer surprises. A disciplined CAD-to-toolpath workflow helps you test manufacturability before you commit material, choose setups that match how the part will actually sit on the table, align tooling with real shop conditions, and catch design changes before they become floor problems.
For engineers, programmers, and growing shops, the useful mindset is simple: CAD and CAM should not be treated as two separate worlds linked only by a file export. The stronger the connection between them, the easier it becomes to judge what the machine will actually experience when the spindle turns on.
| Workflow Stage | What Happens | Why It Matters In Production |
|---|---|---|
| CAD Modeling | Geometry and design intent are created | Features that look acceptable in CAD may still be difficult to hold or cut |
| Manufacturability Review | The part is checked against tooling, access, and setup logic | Cheap changes are still possible at this stage |
| Manufacturing Setup | Stock, work origin, orientation, and fixture assumptions are defined | This is where the digital part first meets physical reality |
| Toolpath Planning | Operations, tools, sequencing, and cut behavior are chosen | Cycle time, tool load, and finish quality begin taking shape |
| Simulation And Verification | The route is checked before material is at risk | Many avoidable mistakes become visible here |
| Post And Handoff | The strategy becomes machine-specific output | The route becomes production data rather than design data |
The CAD Model Is Design Intent, Not Yet a Manufacturing Plan
A common mistake among new CNC users is to treat the finished CAD model as if the hard part is already over. In practice, the finished model is the beginning of manufacturing judgment. The part may be fully defined in CAD and still be difficult to clamp, awkward to access with real tools, or inefficient to produce in the order it was designed.
This is exactly why a connected CAD/CAM environment is useful. It keeps manufacturing questions close to the model while the geometry is still easy to change. If a wall is too thin for stable machining, if a pocket is too deep for the shop’s preferred tooling, or if the chosen orientation creates unnecessary setups, the team can see those consequences much earlier.
That early visibility matters because late design fixes are expensive. Once drawings are released, fixtures are prepared, or material is already staged, even a small design oversight can slow the route down. So the real value of Fusion 360 in CNC is not just that it produces toolpaths. It is that it encourages manufacturability thinking before the machine is committed.
Manufacturability Review Should Happen Before the First Toolpath Is Built
Many inefficient CNC workflows fail before toolpath planning even begins. The part reaches CAM with unresolved questions around stock size, tool access, support faces, wall strength, or operation order. The programmer then has to rescue the design indirectly through awkward setups and compromises.
That is why a good Fusion 360 workflow includes a deliberate manufacturability review before any serious CAM work starts. Ask simple but production-relevant questions. Can the part be held without heroic fixturing? Do internal corners, slot widths, or pocket depths match real tools? Will the first operation leave the part stable for the next one? Is the model designed around the machine’s actual strengths, or only around geometry convenience?
This review is not bureaucracy. It is one of the cheapest ways to save machine time later. A part that is slightly revised in CAD may become much easier to cut, inspect, and repeat. That kind of improvement is exactly what a connected CAD/CAM workflow is supposed to make easier.
Setup Is Where the Digital Part Signs a Contract With the Real Machine
Once the model exists, manufacturing setup becomes the first truly physical decision. This is the moment where abstract geometry is assigned a stock definition, a work coordinate, a machine orientation, and an implicit workholding plan. That may sound administrative, but in real production it is one of the highest-value stages in the whole workflow.
Stock size, part orientation, zero location, tool access direction, and operation order all shape whether the route will be efficient or frustrating. A weak setup can ruin otherwise strong toolpaths because the machine is being asked to execute them under poor physical assumptions. A strong setup can make the rest of the route calmer, faster, and easier to verify.
This is why experienced programmers think about setup as process design, not as a screen that must be filled out. The better the setup reflects how the part will actually sit on the machine, the more useful the rest of the CAM work becomes.
Tool Libraries Only Help When They Match Real Shop Conditions
Software training often emphasizes what operations can do. In production, what matters just as much is whether the digital assumptions about tooling match the real tools, holders, stick-outs, and spindle behavior in the shop. A polished digital plan built around imaginary tooling discipline is not a strong plan. It is only a neat-looking one.
That is why tool libraries deserve much more seriousness than many small teams give them. If the programmer builds strategies around tool lengths that are not practical, holders that are not actually used, or cutter choices that are poorly controlled on the floor, then the link between CAD/CAM and production weakens immediately.
Fusion 360 can help standardize that knowledge, but only if the shop keeps the library honest. A real tool library should reflect what the machine can run predictably, what the shop can measure confidently, and what the operators will actually load. When that connection is strong, CAM planning becomes much more repeatable.
Toolpath Strategy Is Where Productivity and Risk Start Moving in Different Directions
Toolpaths are not merely lines that tell the cutter where to go. They are decisions about how the machine removes material, in what order, with what engagement, and with what tradeoff between cycle time, finish, and tool life. That is why CAM strategy matters so much. A part can be technically machinable in several ways, but those routes are not equally safe, fast, or repeatable.
In Fusion 360, choosing between roughing, finishing, drilling, contouring, adaptive clearing, rest machining, and different stepdown or stepover patterns is really choosing process behavior. The programmer is deciding how aggressively the machine should work, how much stock should be left for the next stage, and whether the route protects quality or only chases nominal speed.
This is where software skill and manufacturing judgment have to meet. A visually clean toolpath is not enough. The real question is whether the route helps the machine behave well in the real world, with the real stock, fixture, and cutter condition the shop will actually have.
Operation Sequence Decides Whether the Machine Works Calmly or Fights the Part
One of the most underestimated parts of the CAD-to-toolpath flow is operation order. The issue is not only which operations exist, but when they happen. If too much material is removed too early, the part may lose stability. If a finishing surface is left until after a destabilizing cut, quality may drift. If drilling happens after the geometry becomes less supported, position confidence can suffer.
This is why sequencing is not cosmetic. It is structural. Good programmers do not just choose operations. They decide which features should be created while the stock is still strongest, which surfaces should be finished while support is highest, and which cuts are safest to leave for later.
Fusion 360 is valuable here because the CAD model and CAM workflow sit close enough together that these decisions can be reviewed against the actual part shape. The software does not make the sequencing decision for you, but it makes it easier to evaluate before material is wasted.
Simulation Is Most Valuable As a Decision Filter, Not As a Magic Guarantee
Simulation is one of the strongest parts of a CAD-to-toolpath workflow because it moves some troubleshooting into the planning stage, where correction is cheaper. Collision risk, obvious inefficiencies, wasted air cutting, bad operation order, and questionable tool engagement can often be seen before stock is loaded.
But simulation should not be romanticized. It is only as good as the setup assumptions, tool definitions, and model conditions behind it. If the fixture is imaginary, the tool length is wrong, or the stock condition is unrealistic, the simulation can still give a false sense of security.
The best use of simulation is therefore disciplined rather than theatrical. It should answer practical questions. Does the route clear the part the way we think it does? Does the holder remain safe? Are we spending too much time in air? Are we leaving the part stable enough for the next stage? Used this way, simulation becomes a decision filter rather than a checkbox.
Post-Processing Is Where CAM Strategy Finally Becomes Production Data
Even when the toolpaths are sound, the job is not really ready until the strategy has been translated into machine-specific output. This is where post-processing matters. A CAM environment may describe the route clearly, but the control only sees its own syntax, machine behavior, and output conventions. If the post is poorly matched, confusion can begin right where the route is supposed to become real.
That is why the CAD-to-toolpath story is incomplete until the post and handoff process are stable. Good shops do not treat posting as an afterthought. They treat it as part of the route. The goal is not simply to create code. The goal is to create code that matches the setup, the controller, the expected tool calls, and the way the machine is actually run.
This becomes even more important in mixed environments where routers, mills, drilling centers, or different control families coexist. The more varied the machine base, the more disciplined the digital handoff has to be.
Revision Control Matters Because Design Changes Rarely Stay Small in CAM
One of the commercial advantages of a connected Fusion 360 workflow is that design changes can be checked against machining consequences before they ripple through production. A pocket gets deeper. A radius changes. A wall is reduced. A slot moves. On paper these can look minor. In CAM they may change tool reach, operation order, stock condition, or fixturing logic significantly.
That is why revision management matters so much. Shops that handle CAD and CAM as loosely connected steps often discover too late that a “small drawing update” has created a much different manufacturing route. When CAD and CAM stay closer together, those effects become easier to review, and the cost of change falls.
This matters in prototype work, low-volume custom production, and internal development equally. The closer the workflow stays to the model, the easier it becomes to keep design change from turning into shop-floor confusion.
Shop-Floor Handoff Is Strongest When the Programmer Thinks Like the Operator
Many CAM problems are not technical failures. They are communication failures. The toolpath may be valid, but the operator receives too little context around zero location, stock condition, fixture intent, tool substitutions, or the order in which the job is meant to run. In small teams, this may be handled verbally. In growing operations, that quickly becomes unreliable.
That is why the CAD-to-toolpath workflow should include clear handoff habits. Setup sheets, fixture notes, tool expectations, origin logic, and revision clarity all reduce the chance that the operator has to reinterpret the route alone at the machine. Fusion 360 does not eliminate the need for that discipline, but it supports it well when the team treats handoff as part of the workflow rather than as something the operator is expected to infer.
The real goal is simple: the machine should receive a route that is not only technically correct, but operationally legible.
The Same CAD-to-CAM Discipline Matters in Routing, Drilling, and Panel Work Too
Although conversations around Fusion 360 often lean toward machined parts, the same workflow logic matters in routing, drilling, and broader non-metal production. In those environments, the move from digital geometry to machine path still determines whether the output is smooth, efficient, and repeatable. A panel may be drawn correctly and still be awkward to nest. A router part may be modeled correctly and still be poorly sequenced for hold-down. A drilling route may be dimensionally correct and still be inefficient to run.
That is why the underlying lesson travels well beyond metal machining. Digital geometry only becomes production value when it is translated into a route the machine can carry predictably. Shops planning to build a more connected production line or align software planning with the Pandaxis machinery lineup still benefit from the same discipline: bring machine reality into the design conversation early, not late.
What Makes the Workflow Strong Is Not the Software Alone But the Thinking Around It
It is important not to overstate the tool. Fusion 360 can organize CAD and CAM effectively, but it does not replace fixture planning, tooling knowledge, control familiarity, or operator discipline. A poor strategy inside a polished interface is still a poor strategy. A part that is hard to hold remains hard to hold even if the toolpath looks elegant on screen.
The software should therefore be treated as a process amplifier. It makes good decisions easier to preserve, and weak decisions easier to encode consistently. That is precisely why the thinking around the software matters so much. The better the shop understands manufacturability, setup logic, tool control, and handoff discipline, the more useful the CAD-to-toolpath bridge becomes.
From Model Approval to Spindle Time
Fusion 360 for CNC matters because it helps connect geometry, manufacturing setup, tooling, strategy, simulation, and machine handoff into one workflow instead of several disconnected steps. The real value is not that it can generate operations. The real value is that it helps shops discover process problems while those problems are still cheap to fix.
That is why the path from CAD model to toolpath should be treated as a controlled manufacturing sequence, not as a file export. When the workflow is strong, design changes are easier to assess, setups are cleaner, operators receive clearer intent, and the machine sees a calmer route. That is what turns a digital model into production value.