Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
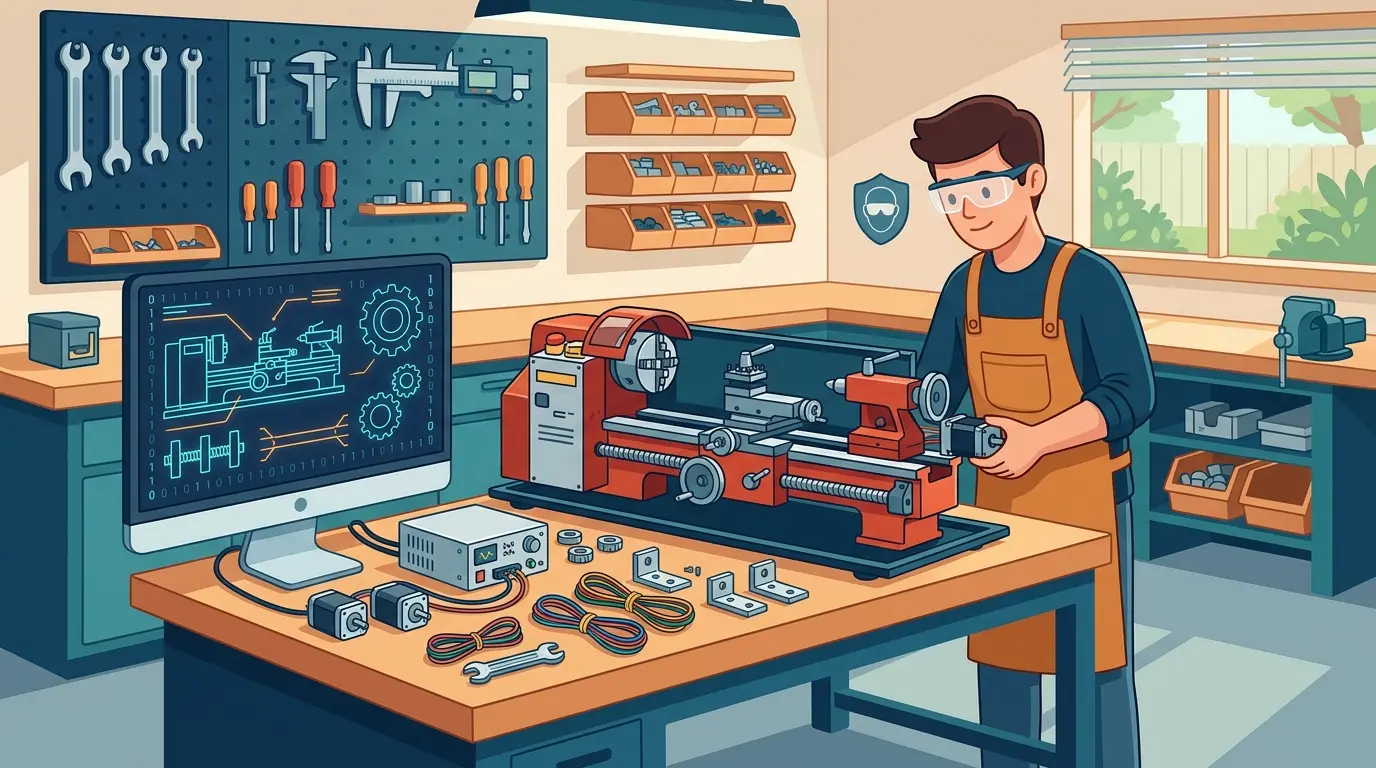
Before you price a single stepper motor or controller board, a mini lathe CNC conversion demands a mechanical audit, not an electronics shopping spree. Backlash, bed wear, spindle stability, and slide rigidity determine whether the retrofit will produce repeatable parts or simply automate inconsistency. This article walks through the critical checkpoints—defining the machine’s duty, testing against real threading and finish work, matching motion hardware to actual loads, and planning for commissioning, safety, and serviceability—so you can decide whether the base machine justifies the investment or whether a purpose-built CNC lathe is the more honest production answer.
Define the Machine’s Job Before You Price a Single Component
The appeal of a mini lathe CNC conversion is straightforward: it promises a low-cost path into programmable turning without the floor-space commitment of an industrial machine. In the right setting, that promise holds. A converted mini lathe can serve as a capable educational platform, a short-run tool for simple parts, or a way to automate repetitive second-operation work in a compact shop.
But retrofit projects fail for a predictable reason. Buyers commit to motors, controllers, and software before confirming the underlying lathe is worth converting. A weak mechanical base does not become strong because it receives modern electronics. Backlash, bed wear, spindle inconsistency, and poor rigidity will still define the result. Treat a mini lathe CNC retrofit as a mechanical evaluation first and an electronics project second.
Before choosing any hardware, define the role the converted machine must play. Is the goal education? Repeatable simple turning? Faster second-operation work? Small-batch prototype support? A platform for threading practice? A way to reduce handwheel time on recurring parts?
Different answers justify very different spending levels. Without a clear job definition, projects drift. One week the goal is learning; the next week the owner prices the project as if it must support commercial output. That mismatch is how you overspend on electronics while underinvesting in the base machine. Size the project to the duty. Until the role is clear, parts selection is guesswork wearing technical language.
Mechanical Health Is the Gate, Not a Detail
Inspect the lathe’s actual condition before ordering anything electrical. Bed wear, spindle play, cross-slide stiffness, gib condition, tailstock alignment, carriage feel, and leadscrew condition all determine whether the retrofit will ever deliver acceptable results. If the lathe already struggles to turn parts manually with confidence, CNC conversion will not rescue it. It will simply automate the inconsistency.
This is the most important checkpoint because it prevents you from investing heavily in the visible parts of the project while ignoring the condition that dominates the outcome. A lathe that cannot hold calm manual behavior is not a strong candidate merely because conversion hardware exists for machines of its size.
A conversion only makes sense when the base lathe is mechanically respectable enough to justify the effort. That does not mean perfect. It means good enough that the added control layer is refining a usable machine instead of decorating a weak one.
Threading, Shoulders, and Finish Reveal the Truth Faster Than Demo Cuts
Turning projects sound manageable until the work includes meaningful threading, repeat shoulder positions, or finish expectations that must survive inspection. These operations expose backlash, looseness, speed inconsistency, and rigidity limitations quickly. Test your retrofit plan against the hardest real work the machine will face, not the easiest simple-diameter demonstration cut.
If the intended parts involve threading, repeat diameters, controlled shoulder stops, or cosmetic finish requirements, the machine mechanics must support that before any controller choice becomes interesting. Otherwise the project becomes an electronics success and a manufacturing disappointment.
In retrofit work, glamorous controls often arrive before mechanical truth. Reverse that order.
Spindle Behavior Matters as Much as Axis Motion
Most retrofit conversations focus on axis conversion while treating the spindle as a background detail. That is a mistake. Turning quality depends heavily on spindle consistency, bearing condition, speed stability, and how predictably the machine behaves across the operating range your work actually needs.
If the spindle already feels unstable, noisy, or inconsistent, no amount of motion improvement will make the finished machine feel dependable. The spindle is not just another subsystem. It is central to whether the converted lathe can produce repeatable finish, threading behavior, and part confidence.
Assess the spindle early in the project, not after the motion hardware has been ordered.
Control Strategy Should Follow Part Mix, Not Internet Popularity
Some buyers assume they need a highly flexible CAM-driven workflow. Others assume canned cycles and simple conversational control will cover everything. The right answer depends on the actual part mix. Simple repeat turning may not need the same software and integration burden as more varied geometry, heavier threading use, or frequent program changes.
Let the control decision follow the work. What parts will you run? How often will setups change? Will threading be common? Does manual fallback matter? Is the machine for one operator who likes to tune and troubleshoot, or for a broader group that needs clearer standard behavior?
The answers determine whether the retrofit should emphasize simplicity, programmability, or a balance of both. Define the machine’s job before collecting the most popular electronics parts from other people’s builds.
Motion Hardware Must Match the Real Load and the Real Friction
Motor sizing on a mini lathe is easy to misjudge. Small machines still face real cutting loads, acceleration demands, axis friction, and low-speed torque needs. If the drive choices do not match the actual axes and intended cuts, the retrofit becomes noisy, temperamental, or difficult to tune even if it looks modern on paper.
The mechanics come first for this reason. The condition of the slides, the resistance in motion, the size of the parts, and the expected duty all influence what the motion system really needs. Overly optimistic drive choices make the project unreliable. Overly ambitious performance targets force the retrofit into instability the base machine was never built to support.
The motion package should respect the lathe. It should not pretend the lathe has become a different class of machine simply because the axes are now commanded differently.
Commissioning Work Is Usually Larger Than New Builders Expect
Many conversion plans assume the electronics will be the hard part and the mechanical adaptation will be straightforward. In reality, mounting, alignment, backlash control, clearances, limit behavior, spindle integration, and machine-condition surprises consume far more time than expected. Commissioning adds its own layer: tuning motion, confirming direction logic, validating safe startup, testing repeatability, and proving that normal work can run without constant intervention.
Plan for that openly. A retrofit schedule built on best-case assumptions becomes frustrating quickly. Projects that go well start with a realistic view of alignment work, adjustment time, and how much proving-out is needed before the machine is honestly usable.
The retrofit is finished only when the machine behaves predictably during ordinary work, not when it first moves under program control.
Safety Needs to Be Designed In From the First Revision
Safety planning is not a later polish step. Guards, emergency stop logic, spindle behavior, safe start routines, operator position, chip containment, and sensible recovery procedures belong in the earliest design thinking. A converted machine creates new risks because the lathe now moves under program control rather than only under direct operator motion.
This is especially important on compact equipment where users may treat the machine informally. A retrofit that works electrically but behaves unsafely is not a finished success. The fact that the machine is small does not make unintended movement harmless. Compactness encourages a false sense of familiarity that makes procedural discipline even more important.
Good retrofits behave safely during normal operation, abnormal stops, and awkward recovery moments, not only when everything goes according to plan.
Manual Serviceability and Fallback Use Still Matter
Many mini lathe retrofits benefit from retaining sensible manual serviceability for setup, troubleshooting, lubrication, inspection, or limited fallback use. Think carefully about how the conversion affects access to slides, adjustments, guards, wiring, and routine maintenance points.
A retrofit that makes the machine harder to inspect or service creates new frustration even if the motion control works well. Good conversions respect the machine as a machine, not only as an electronics platform. Leave enough clarity in the physical layout that someone can still diagnose wear, check alignment, and maintain the machine without reverse-engineering the conversion every time something changes.
This matters most when the machine is meant to stay useful beyond the enthusiasm of the original build phase.
Documentation and Recovery Separate a Tool From a Temporary Project
Even compact conversions need clear wiring documentation, settings backups, a restore path, and a way to recover after faults or configuration mistakes. Without that, the project depends on the memory of the person who built it. That may be acceptable for a personal experiment. It is much less acceptable once the machine becomes part of recurring work.
The more the retrofit is expected to behave like a dependable tool, the more important documentation and recovery become. If the control is changed, if a component fails, or if someone must revisit the machine after several months, the project should not have to start from confusion.
Many retrofit efforts lose momentum after the first successful demonstration because too much knowledge remains informal. Spare components, wiring notes, parameter copies, and maintenance references keep the machine usable after the novelty of the build is gone.
Tolerance Ambition Has to Stay Aligned With the Base Machine
One of the easiest ways to overestimate a retrofit is to let the control upgrade quietly inflate quality expectations. Once a machine has programmable motion, it is tempting to expect a different class of turning result. But if the castings, spindle, slides, and overall rigidity still belong to a modest mini lathe, the achievable tolerance and finish expectations must remain honest.
This does not mean the retrofit has little value. It means the value comes from better repeatability, better convenience, and more controlled motion within the real physical limit of the machine. Projects go wrong when owners expect the new control layer to turn a compact lathe into something closer to a purpose-built production platform.
The healthiest retrofit plans define quality targets the base machine can plausibly support before the control upgrade is added. Then the electronics improve consistency inside that boundary rather than deny the boundary exists.
Ownership Risk Rises Fast When Only One Person Understands the Build
Many conversions work well while the original builder is constantly present, then become fragile when the machine must survive handoff, staff change, or even a few months of inactivity. That is not only a documentation problem. It is an ownership-model problem. If the machine is meant to support recurring work, more than one person should be able to understand how it starts, stops, recovers, and gets serviced.
This is why some technically successful retrofits still fail as shop tools. The machine runs, but the usable knowledge never became transferable. In a one-person experimental environment, that may be acceptable. In a shared workspace or commercial setting, it is usually a sign that the project has not really matured into equipment.
Retrofits become durable assets only when the knowledge around them becomes durable too.
A Practical Retrofit Check Table
| Checkpoint | Why It Matters |
|---|---|
| Bed, spindle, and slide condition | Determines whether the base machine is worth converting |
| Backlash and rigidity | Directly affect turning quality |
| Intended part mix defined clearly | Guides control and software choices |
| Motion hardware sized for real loads | Supports usable and stable behavior |
| Threading expectations reviewed early | Exposes mechanical weakness quickly |
| Safety and recovery planned from the start | Prevents a fragile or risky retrofit |
| Documentation strategy defined | Keeps the machine supportable later |
This table is basic by design. It keeps the project grounded in turning reality rather than retrofit enthusiasm.
Know When Buying a CNC Lathe Is the Better Answer
Some retrofit ideas are worthwhile. Others are really signals that the buyer needs an actual CNC lathe. If the expected workload is commercial, repeatable, and dependent on reliable threading, faster setup, predictable finish, or more than one operator, the economics may favor buying rather than converting.
Retrofits are strongest when the goal includes learning, experimentation, compact short-run support, or modest automation of simple turning work. They are weaker when the business expects industrial dependability from a lightly converted base machine.
That is not an argument against retrofits. It is an argument for honest role definition. A retrofit should not be expected to absorb production expectations that the base machine and the support plan were never meant to carry.
How This Connects to Broader Turning Planning
Pandaxis does not sell mini lathe conversion kits, but the buying discipline is the same. If the project is drifting from retrofit curiosity toward real turning capacity, the Pandaxis CNC lathe buying guide is the more relevant planning frame. For buyers who need clearer turning vocabulary before making the comparison, understanding what CNC lathes do best in real manufacturing helps define what proper turning capacity should actually deliver. And when retrofit realism needs a parallel lesson from milling, knee mill retrofit planning reinforces the same principle: start with the machine, not the electronics.
The Best Retrofit Plans Feel Narrow in a Good Way
Before any major parts are ordered, define what success means in a way the actual lathe can plausibly support. Is the goal learning? Repeatable simple turning? Better threading on limited parts? Reduced manual effort on recurring short runs? A platform for experimentation? The narrower and more honest the answer, the better the project usually goes.
Retrofits succeed when expectations, mechanics, controls, safety, and maintenance planning all point in the same direction. When those pieces are misaligned, the project usually becomes more educational than productive. That is useful only when education was the goal in the first place. Otherwise, the smarter move is usually a more honest machine strategy.