Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
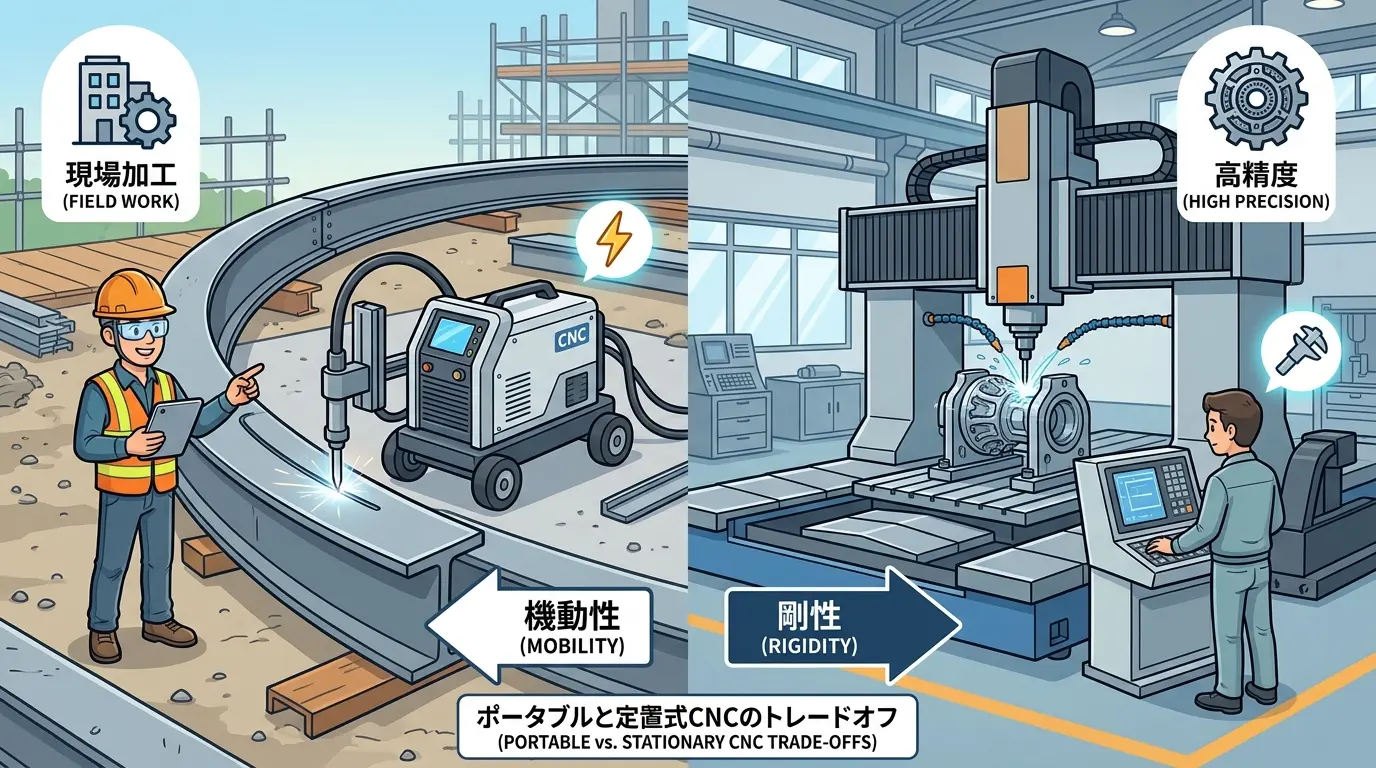
Portable CNC machines solve a genuine production problem only when the workpiece cannot reasonably come to the machine—installed panels, seated countertops, or oversized assembled structures that make transport costly, risky, or impractical. But buyers frequently mistake portability for general-purpose versatility, overlooking the real trade-offs in rigidity, reference control, setup repeatability, and environmental exposure. The decision must start with the workpiece location, not the machine’s folding mechanism. If moving the machine is cheaper, safer, and more accurate than moving the part, portability earns its place; otherwise, it simply removes the stability that daily production depends on.
Portable CNC Is a Location Strategy, Not a Lighter Shop Machine
Portable CNC machines attract attention for a straightforward reason: some workpieces simply cannot come to the machine. A panel built into an architectural installation, a countertop already seated on cabinetry, a large assembled structure that would require disassembly and reinstallation—these jobs create a genuine production problem. Moving the part is expensive, risky, or physically impractical. Bringing the machine to the part looks like the obvious answer.
That logic holds in specific workflows. But it fails when buyers treat portability as a general-purpose feature rather than a location-specific solution. A portable CNC is not a compact version of a fixed industrial machine. It is a different process with a different risk balance, and the trade-offs show up in places that product brochures rarely mention.
The Decision Starts With the Workpiece, Not the Machine
Buyers often begin by asking whether a portable CNC can be transported, folded, lifted, or carried between job sites. Those questions matter, but they skip the central issue. The real question is whether moving the machine is cheaper, safer, and more accurate than moving the workpiece.
That comparison forces an operational view. A portable machine creates value only when the cost of transporting, supporting, or reworking the part exceeds the cost of setting up the machine at the point of work. Mobility is valuable when location is the problem.
That condition appears more often than some buyers expect. Typical situations include:
- The workpiece is already installed and cannot be removed without significant labor.
- The workpiece is too large to move efficiently or safely.
- Repeated handling would create damage risk to finished surfaces or assembled components.
- Measurement and cutting must happen in one continuous step because the installed condition differs from the drawing.
- The job site changes faster than a fixed shop workflow can respond.
If none of those conditions apply, the case for portability weakens quickly. A machine that travels well but solves no location problem is simply a less rigid version of equipment you already need.
Where Mobility Creates Real Economic Value
Portable CNC wins when it removes logistics that would otherwise dominate the job. That is why the category makes sense in installation work, fit-out operations, large assembled structures, exhibit fabrication, contractor workflows, and specialty trimming tasks. In these cases, the part is not waiting on a flat reference table inside a climate-controlled shop. It may be attached to a wall, built into a space, too large to reload safely, or too context-sensitive to measure in one place and cut in another.
In those conditions, a portable CNC creates value in three practical ways.
First, it reduces the handling burden. Moving a large part back to the shop requires labor, packaging, transport risk, and then another installation pass. Bringing the machine to the part can be more efficient overall, even if the cutting itself takes longer.
Second, it shortens the gap between measurement and execution. On-site dimensions frequently differ from CAD files. When the part must be matched to a real-world condition, cutting in place eliminates the translation error that occurs when you measure on site, return to the shop, and hope the numbers still hold.
Third, it reduces rework caused by context loss. Some jobs are difficult precisely because the final cutting decision depends on the installed environment. Portable CNC is not just mobile cutting; it is a way to keep the reference context alive while the cut is made.
That is the strongest case for portable CNC: the machine solves a location problem that a fixed shop process solves poorly.
What Portability Takes Away From a Stable Shop Process
Every portable machine pays for mobility with some degree of process compromise. A fixed machine benefits from stable mounting, known utilities, controlled reference surfaces, predictable hold-down, and a repeatable setup environment. Portable systems operate with fewer of those advantages.
Cut quality is not created by spindle speed alone. It depends on how consistently the machine is referenced, how stable the work surface is, how well the material is supported, and how repeatable the setup becomes from one task to the next. When buyers ignore that point, they compare a portable CNC to a fixed machine as if the only difference were transportation. In reality, the entire process stack changes.
The machine may still cut accurately enough for the job, but the path to that result depends much more heavily on setup discipline. A better description of portable CNC is not “shop capability anywhere.” It is “controlled compromise where mobility solves a bigger problem than stability would.”
Reference Control Is Usually the Hardest Part, Not the Cutting
Portable CNC conversations often focus on spindle power, frame size, or travel range. Those factors matter, but many real-world problems come from reference control instead.
A fixed machine starts from known geometry. The bed, the hold-down method, and the machine structure create a stable reference environment. Portable CNC often has to build that reference environment at the job site, sometimes on imperfect surfaces, awkward material supports, or temporary staging.
That is where strong operators separate from weak ones. If the machine sits on an uneven base, if the part is not fully supported, if clamps force distortion, or if the operator cannot re-establish datum points reliably, the portability advantage disappears into inconsistency. The machine is not necessarily failing. The workflow is asking a mobile system to recreate shop-like conditions in a place that may not allow them.
Buyers should examine portable CNC through a reference question first: how will this machine find, hold, and repeat a trustworthy starting condition in the actual environment where it will work? If that answer is vague, the portability decision is still immature.
Environmental Variables Matter More Than Product Pages Suggest
Portable machining is more exposed to uneven support surfaces, limited clamping options, power inconsistency, temperature shifts, debris, operator positioning issues, and incomplete extraction. None of these automatically makes the process unusable, but each one raises the burden on setup and execution.
A shop machine benefits from a controlled home. Portable CNC often works in borrowed conditions. That has practical consequences:
- Material support may change from job to job.
- Dust or chips may be harder to capture consistently.
- Power quality may be less predictable.
- Operator body position may be worse for accurate setup.
- Surface flatness and part stability may need to be created instead of assumed.
This is why portable CNC workflows depend heavily on operator discipline. The machine may be mobile, but the process still needs structure. Without strong habits, the convenience of portability gets consumed by setup drift, slower cycles, or rework. For experienced teams, that may still be acceptable. For inexperienced buyers, it is one of the easiest places to underestimate the true cost of mobility.
Portable CNC Is Strongest in Narrow, High-Relevance Use Cases
Portable CNC machines are usually strongest when the work location itself is part of the job difficulty. That includes on-site operations, large-format adjustments, installation fitting, custom trimming in place, and limited machining tasks on structures that are impractical to load and unload repeatedly.
The best use cases tend to share several traits:
- The job cannot be fully standardized before arrival.
- The part or structure is hard to move.
- The operation is important but not high-volume production.
- The value of in-place accuracy exceeds the value of shop-level throughput.
That last point matters. Portable CNC is often strongest when precision must be delivered in context, not when maximum daily throughput is the priority. This is why the category often makes more sense for contractors, fit-out teams, specialty installers, and some one-off or semi-custom work than for factories trying to build repeatable daily output.
The Wrong Reason to Buy Portable CNC Is “It Seems More Versatile”
Portable CNC becomes a weak choice when the work is actually stable shop work that would benefit more from proper fixturing, cleaner extraction, better hold-down, and a fixed reference environment. If most jobs happen in the same workshop, a portable platform may add theoretical flexibility while removing the very stability that daily production depends on.
This is where many buyers talk themselves into the wrong purchase. They imagine that portability means broader capability. But versatility is useful only if it solves the right constraint. If the constraint is not mobility, then the machine may simply become harder to control without creating real operational benefit.
That is especially true when “portable” becomes a substitute for deciding what the workflow really is. A buyer may not want to commit floor space yet, may not want to choose between routing and sawing processes, or may simply want one machine that feels universally adaptable. Those are understandable instincts, but they do not change the underlying production logic. If most of the work is fixed-location panel processing, repeated part programs, and predictable shop throughput, then portability is rarely the strongest answer.
Compare Portable CNC to the Best Fixed Process, Not to an Abstract Ideal
The most useful comparison is not portable versus non-portable in the abstract. It is portable versus the best fixed process for the same work.
If the job is mainly sheet-based production inside a workshop, a fixed workflow built around nesting machines usually delivers stronger repeatability, better material handling, and higher daily throughput. If the work is precision sizing, straight cutting, and controlled panel processing inside a shop, fixed sliding table saws may be a cleaner process match than a mobile CNC platform.
That is the key buying discipline: compare portable CNC to the real alternative you would actually run, not to a generic fantasy of stationary shop equipment. When buyers make that comparison honestly, the answer becomes clearer:
- Portable machines win when location drives the job.
- Fixed machines win when stability drives the job.
- Portable machines help when handling the part is the bigger cost.
- Fixed machines help when repetition, referencing, and throughput matter more.
That framing prevents a lot of expensive confusion.
Throughput Usually Falls Faster Than Buyers Expect
Portable CNC can be productive, but buyers should be careful not to confuse productive with production-oriented. A mobile workflow often includes transport, unpacking, surface assessment, temporary support setup, reference establishment, dust strategy, cut execution, cleanup, and repacking. Each step may be reasonable on its own. Together, they can make the real cycle much longer than the cutting time suggests.
That is why portable CNC should be evaluated using full-job cycle time, not just feed rate or spindle specifications. A buyer may compare a portable system to a fixed shop machine and think the mobile option is acceptable because the cut itself only takes slightly longer. But if the surrounding workflow adds substantial setup and recovery time, the process economics change.
Portable CNC can still win when the alternative involves moving a large part twice and reinstalling it, but the comparison has to be made honestly. In other words, portable CNC may be faster than moving the job. It is not automatically fast in absolute terms.
Safety, Extraction, and Power Do Not Shrink Just Because the Machine Folds
One of the most misleading assumptions around portable equipment is that mobility somehow reduces the seriousness of setup requirements. In reality, a machine that travels still needs disciplined stopping logic, clear operating rules, power planning, and debris management. Portable workflows often make these issues harder, not easier.
There may be no permanent enclosure. Extraction may be improvised rather than fixed. Power availability may vary. Cable routing may be temporary. The work area may be shared with installation crews or other site activity. All of that means the operator has to think more like a process manager and less like someone simply using a compact tool.
This is another reason portable CNC is not a general-purpose shortcut to industrial output. It is a specialty process that demands clear discipline around setup, operation, and cleanup.
Portable CNC Is Often Best Treated as a Specialty Lane, Not a Production Backbone
The cleanest way to avoid disappointment is to classify portable CNC correctly inside the business. In many cases, it works best as a specialty lane rather than the center of all machining activity. That means the machine has a defined mission. It might handle in-place adjustments, site-specific cuts, large installed structures, or limited operations where bringing the job back to the shop would be inefficient. It is not expected to replace a stable production bay.
When buyers make that distinction early, they usually make better decisions. The portable machine is judged by how well it solves a location problem, not by whether it can imitate every strength of a fixed machine.
That framing also helps when a company is growing. Portable CNC may remain useful long-term, but often as a complementary capability while the main production burden shifts toward fixed equipment and more controlled process cells. If the business is moving toward daily duty, recurring parts, and standardized throughput, it helps to look beyond mobility and toward the broader equipment mix in the Pandaxis shop, where machine choice is tied to stable production roles rather than transport convenience alone.
Buy Portable CNC Only When the Workpiece Location Is the Real Constraint
Portable CNC machines help when the workpiece location is the real production problem. They are useful for on-site fitting, oversized work, installed structures, and location-specific fabrication tasks where moving the part is less practical than moving the machine.
They also create real trade-offs in rigidity, setup repeatability, environmental control, extraction planning, and operator dependence. Buyers who choose portability for the right reason can get real value from it. Buyers who choose it because it sounds more adaptable often discover that the mobility they gained came directly out of the process stability they needed.
That is the right final test. If the machine must travel because the job cannot reasonably come back to a fixed process, portability can be a smart and disciplined choice. If the job already lives in a repeatable shop environment, a fixed machine is usually the cleaner answer. Portable CNC is at its best when moving the machine is cheaper than moving the work, and when the expected quality level matches a process that depends on careful field setup rather than permanent industrial stability.