Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
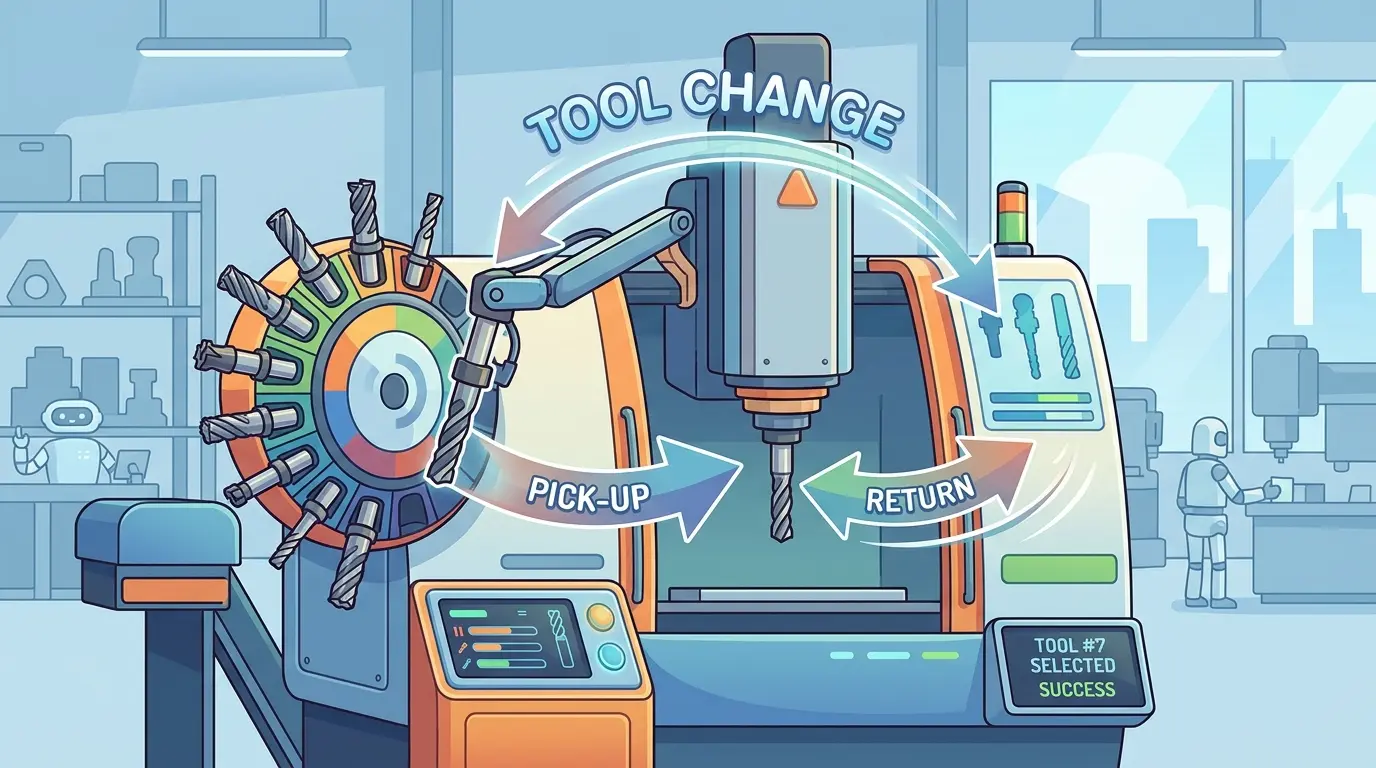
In production terms, ATC in CNC stands for automatic tool changer: the mechanical system and control logic that let a machine swap tools under program control. Instead of stopping the spindle, waiting for an operator to loosen a holder, load a new tool, confirm offsets, and restart the cycle, the machine handles the exchange itself. The purpose is straightforward—protect spindle continuity. ATC earns its keep when the machine keeps losing productive minutes to repeated tool-change interruptions.
That is why ATC is often misread. Buyers sometimes treat it as a prestige feature or a default sign of an advanced machine. The more useful reading is simpler: ATC is a response to a measurable bottleneck. If stopped spindle time is repeatedly getting in the way of throughput, consistency, or operator efficiency, automatic tool change deserves serious attention. If not, it may add cost and complexity faster than it adds value.
Frame the Decision Around Interruption, Not Features
The real question is not “Do you want ATC?” but “How often is manual tool change interrupting the work that actually pays the bills?” That shift matters because many shops buy around appearance instead of interruption pattern. They imagine future flexibility, but they do not measure how often parts truly need multiple tools, how long operators are tied up at the spindle, or how much of the day is spent on repeat manual changes rather than productive cutting.
Once you frame the decision that way, ATC becomes easier to judge. It is not an upgrade for pride. It is an upgrade for cycles that repeatedly lose time at the same point.
What an Automatic Tool Changer Actually Includes
An ATC system is more than a row of tool pockets. It is a coordinated system involving tool storage, transfer motion, spindle release and retention behavior, tool identity tracking, and control logic that keeps the right tool in the right place at the right time. If any part of that chain becomes unreliable, the benefit of automation disappears quickly.
That is why ATC should be treated as a machine system, not as a decorative option. A machine with ATC is asking the shop to manage holders, offsets, pocket assignments, and recovery behavior with much more discipline than a manual-change workflow usually requires.
Where the Payback Usually Comes From
The payback rarely comes from one dramatic moment. It comes from repeated small interruptions disappearing. The machine stops less often. The operator is pulled away less often. Multi-tool parts flow with fewer pauses. The process becomes easier to standardize because the same tool sequence can be called again and again without relying on a person to rebuild it manually.
One manual change may look trivial. Fifty of them per shift are not trivial. That is the economic center of ATC.
When ATC Makes Immediate Sense
ATC usually makes strong sense when the shop sees some combination of these conditions:
- Parts routinely need several tools in one cycle.
- The same multi-tool sequence repeats often enough to justify automation.
- Operators lose too much time standing at the machine for tool swaps.
- The machine is expected to run longer with less direct attention.
- The shop can manage holders, offsets, and magazine discipline consistently.
When those conditions are present, ATC is not a luxury. It is often a practical answer to a bottleneck the shop can already see.
When Manual Tool Changes Still Win
Manual changes still make sense when the part mix is simple, tool count is low, and the machine spends most of its day on short jobs or single-tool work. In that environment, ATC may improve the brochure more than the factory result. The machine becomes more expensive, the tooling system becomes more demanding, and the maintenance burden rises even though the workflow did not truly need the automation.
This is especially common in smaller shops that want versatility and assume ATC automatically belongs in that picture. Sometimes it does. Sometimes it only adds complexity to work that would have run acceptably with manual discipline.
ATC Changes Shop Behavior, Not Just Machine Hardware
Once a machine has ATC, tool management becomes a daily operating system. Holders must stay organized. Pocket assignments must remain trustworthy. Tool lengths and offsets must be handled consistently. Recovery after a tool issue must be understood by the people actually running the machine.
That means ATC rewards disciplined shops and exposes casual habits quickly. A shop that cannot keep tooling information under control may discover that automation creates a different category of error rather than removing interruption cleanly.
The Hidden Cost Is Usually Tooling Discipline
Buyers often focus on the machine price and pocket count, but the more expensive reality may be tooling discipline. Holders cost money. Spare tools cost money. Incorrect pocket loading can cost parts, fixtures, or worse. Setup routines need to be cleaner. People need to understand how to recover from tool faults without turning a simple interruption into a collision or scrap event.
That does not mean ATC is risky by nature. It means the return depends on whether the shop is ready to manage the support system that makes the automation dependable.
Router and Woodworking Workflows Show the Logic Clearly
In woodworking and panel processing, ATC becomes easy to justify when the machine keeps switching between routing, grooving, drilling, boring, trimming, or other repeated tool-specific steps on the same part family. If the machine spends the day alternating between those operations, ATC protects continuity and reduces operator interruption in a way the floor can feel immediately.
If the jobs are much simpler, the case gets weaker. A machine that mostly runs one cutter on uncomplicated work may not need ATC nearly as badly as buyers expect. The decision belongs to workflow structure, not to whether the machine looks industrial in the catalog.
A Strong Internal Justification Starts With Lost Minutes
The best way to justify ATC internally is not with aspiration. It is with lost minutes. Count how often operators stop the spindle to change tools. Count how often multi-tool cycles repeat. Count how much time goes into manual handling that does not actually create value on the part. Once those minutes are visible, the ATC decision becomes much cleaner.
This is one reason strong ATC purchases usually come from shops that already know their bottleneck. Weak purchases come from shops that want future-proofing but have not proved that tool-change interruption is really where the day is leaking capacity.
Why Some Shops Overbuy ATC
ATC gets overbought when buyers imagine complexity that never arrives. They picture future jobs with many tools, long unattended cycles, and highly standardized production, but the machine ends up spending most of its life on straightforward work. The result is a more expensive machine with more components to maintain and more tooling organization to manage, but without enough repeated multi-tool activity to pay the feature back.
That is why honest workload review matters. ATC should be bought because it solves a repeated production pattern, not because it flatters the machine specification.
What to Compare in Quotes Beyond Pocket Count
When suppliers quote machines with ATC, buyers should compare more than how many tools the magazine holds. The more useful questions are:
- How many tool positions are realistically usable for the actual work?
- What holder system and tooling inventory will the shop need?
- How easy is the machine to set up, recover, and maintain after a tool issue?
- What happens when the magazine logic, pocket assignment, or tool mapping goes wrong?
- Does the machine solve a real cycle bottleneck or simply offer a more advanced-looking feature list?
These are stronger buying questions because they connect the changer to production behavior rather than to feature marketing.
Magazine Size and Usable Capacity Are Not the Same Thing
Another point buyers miss is that advertised pocket count does not automatically equal practical day-to-day flexibility. Some shops run a narrow stable tool set and use most of the magazine efficiently. Others find that duplicate tools, wear backups, specialty cutters, probing tools, or job-specific holders consume space faster than expected. A large magazine can still feel tight if the work mix changes constantly.
That is why buyers should think in terms of usable capacity for their real parts, not maximum capacity in a brochure. The right question is not only how many pockets exist. It is how many of those pockets remain useful once the shop’s real tooling habits are loaded into the machine.
Recovery Discipline Matters Almost as Much as Change Speed
ATC discussions often focus on speed, but recovery behavior matters almost as much. Sooner or later a tool will wear unexpectedly, a pocket assignment will need correction, or a setup change will force the operator to intervene. When that happens, the shop needs a clear method for recovering without creating confusion in offsets, pocket mapping, or part status.
This is where good ATC ownership separates itself from superficial ATC ownership. A shop that can recover cleanly after a tool event turns the changer into a dependable production asset. A shop that panics every time the sequence is interrupted may own the hardware without fully owning the workflow.
Where ATC in CNC? Automatic Tool Changer Basics Fits in the Production Route
Pandaxis is directly relevant here because automatic tool changing often affects real throughput in industrial woodworking CNC, especially when one machine is expected to run several operations without repeated manual intervention. If the buyer is trying to decide whether a more advanced machine feature actually deserves the extra capital, it helps to review how Pandaxis frames the investment logic behind industrial CNC equipment when the workflow truly benefits from the upgrade. If the buyer is already comparing quotations and wants to know how ATC should be judged alongside the rest of the machine scope, it also helps to read how to compare CNC machinery quotes without letting one attractive feature hide more important integration details. Those links matter because ATC is rarely the only machine decision in the quote.
The Cleanest Rule for Deciding
If a machine repeatedly needs several tools in one uninterrupted cycle and manual changes are clearly interrupting throughput, ATC deserves serious consideration. If the job mix is simple, the tool count is low, and the operator is not losing meaningful time at the spindle, ATC may still be desirable, but it should be treated as optional rather than essential.
That rule is not flashy, but it is dependable. ATC pays back when the workflow gives it repeated chances to remove interruption. Without those chances, the machine may become more sophisticated without becoming more productive.
Buy It to Remove a Specific Bottleneck
ATC in CNC means automatic tool changing under machine control so multi-tool work can continue with less manual interruption. Its value is real when repeated tool changes are sitting directly on the critical path of production. Its value is weaker when the machine rarely needs more than one tool at a time or when the shop is not ready to manage tooling systematically.
That is the most useful way to think about the feature. Buy it to remove a specific bottleneck you can already see, not because automatic tool change sounds like the adult version of the machine. When the interruption is real, the payback is usually real too. When the interruption is imaginary, the feature often becomes a more expensive way to own the same cycle.