Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
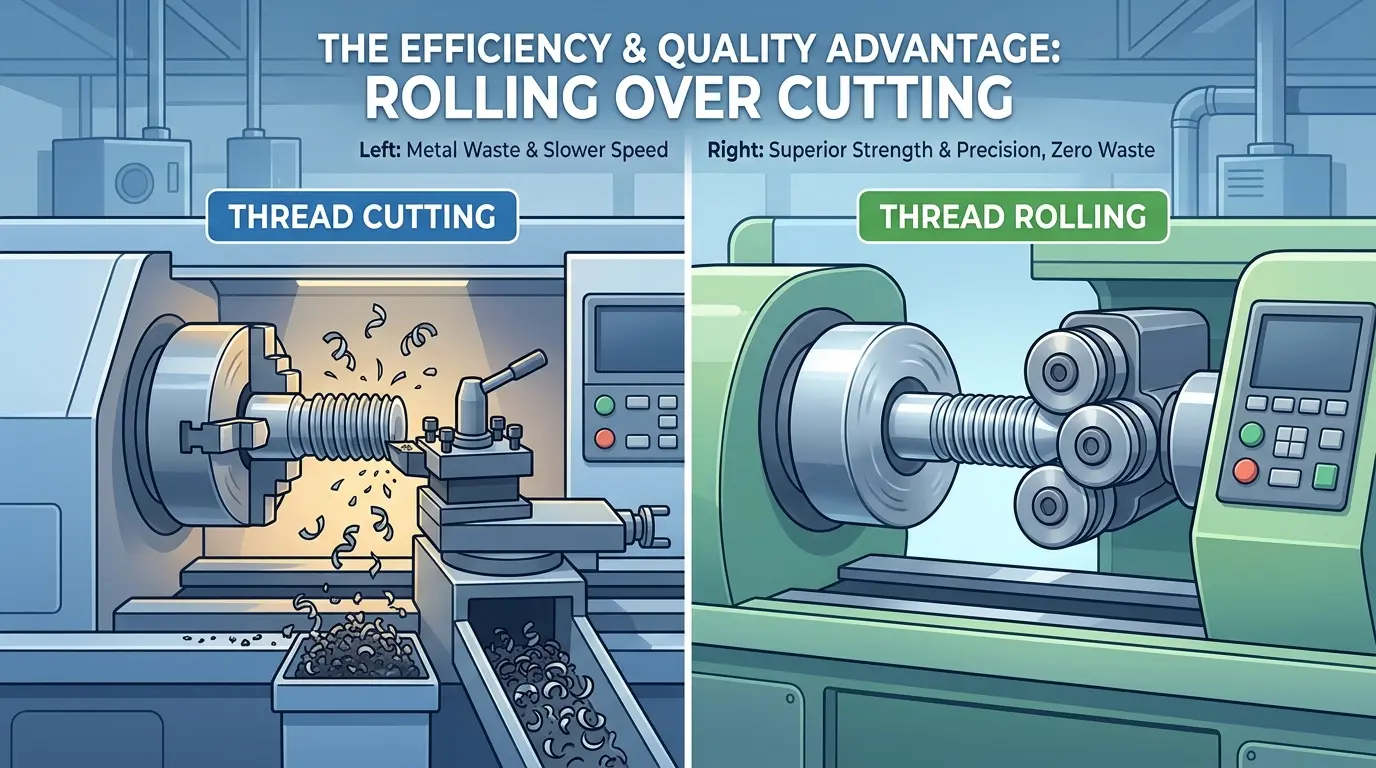
When the same external thread appears on a part family week after week, the question shifts from whether you can cut it to whether you should still be cutting it. Thread rolling attachments replace chip removal with plastic displacement, but the payoff is conditional: ductile material, stable blank diameter control, repeatable volume, and geometry that allows proper tool access. This article walks production teams through the real comparison—not rolling versus cutting in theory, but which method holds up inside your actual job mix, where setup burden and upstream turning discipline often decide the outcome.
When Threading Stops Being a One-Off Feature
On many CNC lathe jobs, cutting a thread is just another operation in the cycle. The tool paths in, the machine makes a few passes, and the part moves on. That works fine when threads are occasional features. But there comes a point in many shops where threading stops being an exception and becomes a recurring production event. The same external thread appears on the same part family week after week. Cycle time on that operation starts to matter. Consistency becomes a measurable issue. Inspection keeps flagging the same small variations.
At that point, the question changes from “can we cut this thread?” to “should we still be cutting it?” That is where thread rolling attachments start to make sense.
Forming a thread instead of cutting it can reduce cycle time, improve surface finish, and produce a more consistent thread form on suitable materials. The process can also improve the surface characteristics of the thread root and flanks. But those benefits are conditional. Thread rolling is not a universal upgrade. It wins only when the part family, material behavior, blank preparation, and production volume align well enough for the forming process to stay stable. When those conditions are weak, a rolling attachment adds complexity without delivering proportionate payback.
This is a production economics decision, not a process preference. The right route is the one that gives the shop the better combination of speed, repeatability, and practical control for the threads it makes most often.
What a Thread Rolling Attachment Actually Changes
A thread rolling attachment changes the threading event from a material removal process into a material displacement process. Instead of cutting chips away to generate the flank geometry, the attachment plastically displaces ductile material into the required thread form. That single change ripples through the entire operation.
Cycle time can drop because forming typically requires fewer passes than cutting. Surface finish can improve because the forming action burnishes the thread surface rather than leaving tool marks. Tool life behavior changes because there is no cutting edge to wear in the conventional sense. Blank diameter preparation becomes more critical because the process starts from a specific starting diameter rather than removing material down to a finished size. And material suitability stops being a secondary consideration—it becomes a gate that determines whether the process can work at all.
Shops sometimes underestimate the scope of this change. They see a faster threading method and assume it is simply a productivity add-on for any lathe that already cuts threads. In reality, the attachment shifts the constraints of the operation. Some problems get easier. Others move upstream. If the team is not ready for those upstream demands, the theoretical advantage never fully appears in production.
Rolling Usually Wins When the Part Family Is Stable
The strongest commercial case for thread rolling appears when the shop is making the same external threads repeatedly enough for setup refinement to matter. That could be a contract part, a family of shafts or studs, a fluid fitting, or any repeat work where the thread is not unusual and the shop expects the program to keep coming back.
In that environment, rolling pays back because the machine no longer treats threading as a flexible one-off feature. The operation becomes standardized. The blank size is controlled. Tooling choice stabilizes. Inspection criteria become familiar. Once those pieces settle, the rolling route can outperform cutting in both time and consistency.
This is also why shops that do mostly prototypes or constantly changing custom work often stay with cutting. Their threading workload is too mixed for the forming route to reach its best rhythm. The volume is not just lower—the process memory is weaker. Every job brings a new set of variables, and the rolling process does not get the repetition it needs to stabilize.
Material Ductility Is Not a Minor Detail
Thread rolling only makes sense when the material will form cooperatively. That sounds obvious, but it is one of the most common reasons buyers overestimate the attachment. They focus on the speed of rolling and forget that the process depends on material behavior. Ductile materials are usually where thread rolling shows its advantages most clearly. Materials that resist plastic deformation or behave unpredictably under forming load can turn the same setup into a frustrating experiment.
This is why material should be treated as a go or no-go factor, not as a tuning variable the operator can work around later. If the shop runs a wide mix of materials, some of which do not consistently support formed threads, the attachment may be less useful than the headline productivity claims suggest. If the shop runs a narrower, cooperative material family repeatedly, the case gets much stronger.
That material discipline is part of the economics. Shops that think of rolling as a universal attachment often discover that it is really a specialist advantage within a controlled material lane.
Blank Diameter Control Becomes More Important Than Many Shops Expect
When threads are cut, the machine removes material to create the form. When threads are rolled, the blank is pushed into the thread shape. That means the preparation diameter matters a great deal. If it drifts, the thread result drifts. Shops that are casual about blank control often struggle here because the rolling process exposes upstream inconsistency more brutally than cutting does.
This is not a reason to avoid rolling. It is a reason to understand what the attachment is asking from the rest of the turning route. The lathe must present the thread area in a controlled state before the attachment enters. If upstream turning is already stable, the demand is manageable. If upstream turning is inconsistent, the attachment becomes the place where the inconsistency gets noticed.
That is why rolling is often best in shops that already run disciplined turned-part processes. If the team is still cleaning up fundamental turning consistency, review the broader turning workflow first, not just the attachment choice.
Geometry and Clearance Can Make or Break the Choice
Even when material and volume are favorable, part geometry can still keep cutting in the lead. Thread rolling attachments need physical space and approach logic that fit the part. Shoulders, relief limitations, nearby features, and awkward access can all make the rolling route less attractive. A thread that looks ordinary on a drawing may be easy to cut and inconvenient to form.
This is why the best decisions happen when the buyer evaluates the entire threaded region, not only the thread callout. Is there enough room to run the tool properly? Does the part design support the operation cleanly? Are there undercuts or runouts where needed? If those details are weak, the attachment may not be the right answer even in an otherwise strong production program.
Part design discipline matters here. Shops that want smoother thread production should connect the attachment decision to the same thinking used in turned-part design for lower cost and better accuracy, because design details often determine whether a forming process feels natural or forced.
The Real Comparison Is Not Rolling Versus Cutting in Theory
The useful comparison is not which method is “better” in abstract terms. It is which method behaves better inside your actual job mix. Rolling may give faster cycles and more repeatable results on stable programs. Cutting may still be the smarter choice when the shop needs thread flexibility, mixed pitches, varied materials, and fast adaptation to changing drawings.
This is why shops get into trouble when they evaluate rolling through the lens of isolated technical advantages. A faster thread on the right part is valuable. A faster thread on the wrong part is irrelevant if the setup burden, geometry limitations, or material restrictions make the route fragile.
The best comparison method is to line up the parts that generate the most threading hours in a month and ask whether they belong to a stable rolling lane. If they do, the attachment deserves serious analysis. If they do not, cutting may remain the higher-value choice even if it is slower per thread.
A Practical Decision Table
| Condition | Thread Rolling Usually Leads | Cutting Usually Leads |
|---|---|---|
| Material | Cooperative, ductile, stable production material | Mixed or marginal material behavior |
| Volume | Repeating jobs or part families | Prototypes, sporadic jobs, mixed batches |
| Thread type | Common external thread work with repeatable prep | Special, changing, or low-frequency threads |
| Geometry | Good access and suitable relief/runout conditions | Tight shoulders, awkward access, constrained form zone |
| Upstream turning control | Strong blank diameter discipline | Variable prep and inconsistent pre-thread turning |
This table is intentionally simple, but it captures the commercial logic. Rolling wins when the rest of the process is ready for it. Cutting wins when flexibility is still the higher-value capability.
Rolling Can Improve More Than Cycle Time
Cycle time is the most visible benefit, but it is not the only one. On the right work, rolling can improve process rhythm because it reduces the amount of threading drama in production. The operation becomes easier to standardize. The shop may see less tool-change disruption around threading. Inspection can become more predictable because the same material, same geometry, and same preparation are coming through repeatedly.
That matters in high-mix environments that have small islands of stable repeat work. A rolling attachment can be valuable not because every threaded part should be rolled, but because the attachment quietly stabilizes the subset of jobs that return often enough to justify it. This is a more realistic benefit than generic claims that rolling is simply stronger or faster in all circumstances.
The strongest shops treat it as a specialist productivity tool, not as a symbolic upgrade.
Cutting Still Dominates When Flexibility Pays the Bills
Many small and mid-sized shops continue cutting threads because flexibility is what their business model sells. They need to move between sizes, pitches, quantities, and materials without turning every route into a dedicated production cell. In that environment, the slightly slower but more adaptable process can still be the right one.
This is especially true when the thread program changes often or when the shop is still deciding whether certain thread work should even stay in-house. If that broader in-house turning decision is unresolved, the attachment question may be premature. The bigger issue is still whether the part family belongs on your lathe at all, not whether it should be rolled once it gets there.
That is why buyers should not treat cutting as the outdated option. In mixed work, cutting is often the method that preserves the agility the business actually needs.
Attachments Should Be Evaluated as a Cell Decision, Not a Tool Purchase
One mistake buyers make is evaluating the attachment as though it were only another toolholder decision. It is not. It changes prep requirements, inspection behavior, and process discipline. That makes it closer to a small cell-level decision than to a casual tooling add-on.
Before buying, ask who will own the standards around prep diameter, thread inspection, material selection, and program selection. Ask whether the machine is already stable enough in its turning work to expose the rolling advantage. Ask whether operators will know when to choose rolling and when to stay with cutting. Without those answers, the attachment is more likely to become an occasionally used option than a real production improvement.
This is why shops that succeed with rolling tend to integrate it into a clear process lane rather than leaving it as a vaguely available capability.
Buy It When the Thread Work Has Stopped Being Flexible
Thread rolling attachments beat cutting threads when the threaded work has stopped being mostly flexible and started being mostly repeatable. That is the cleanest way to frame the decision. If the shop is repeatedly making common external threads in suitable materials, with disciplined prep and enough volume to stabilize the route, rolling can outperform cutting in both efficiency and consistency. If the work is varied, low-frequency, or geometry-constrained, cutting still deserves the lead position.
The smartest buyers do not ask whether rolling is better in principle. They ask whether their thread workload has matured enough to reward a forming process. When the answer is yes, the attachment can create real production value. When the answer is no, cutting remains the more honest and more profitable route.