Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
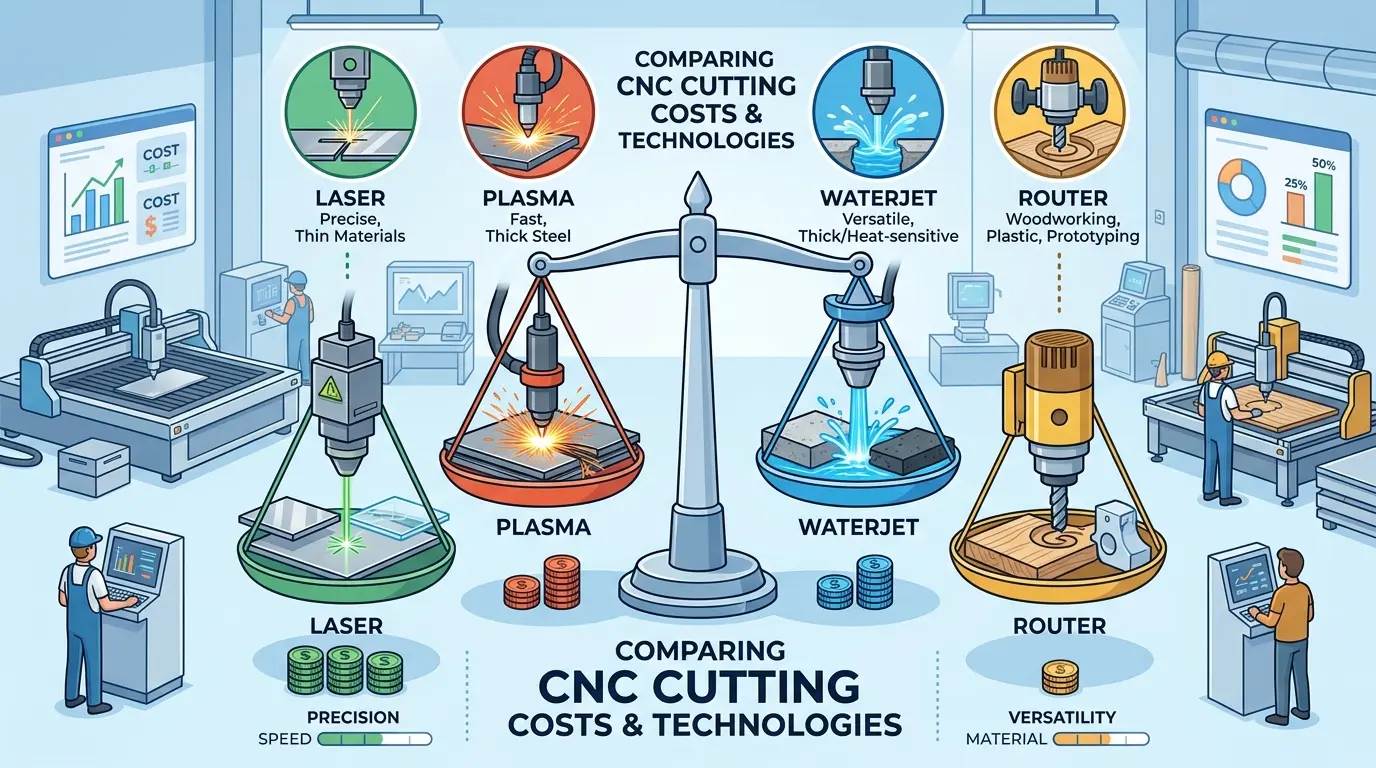
Sticker prices mislead because they ignore the infrastructure, consumables, and labor each cutting process demands once it hits the production floor. A router’s tooling and spoilboard burden, a laser’s ventilation and material-fit dependency, a plasma system’s fume handling and edge cleanup, and a waterjet’s abrasive and slurry management all shift the true cost picture dramatically. Before comparing quotations, buyers must build a first-year budget that captures facility readiness, operator discipline, and secondary finishing. The winning technology is the one whose ownership model matches the shop’s dominant weekly workload, not the cheapest machine on paper.
Why the Sticker Price Is Not the Real Cost of a CNC Cutting Machine
Most CNC cutting machine purchases go wrong not because a buyer misread the quotation, but because the quotation was treated as the complete economic picture. It never is. A router can look financially safe until tooling, spoilboards, hold-down discipline, dust extraction, and setup labor are priced honestly. A laser can look expensive until the material mix makes non-contact detail work and reduced cleanup commercially valuable. A plasma system can appear efficient until fume control, consumables, and downstream edge work are added. A waterjet can seem too costly until heat-sensitive material or mixed-material flexibility makes the alternatives weaker.
The useful comparison is not “Which machine is cheaper?” It is “Which ownership model fits our materials, output plan, and facility burden with the fewest expensive surprises?”
Price Starts With Process Fit, Not With the Machine Body
Router, laser, plasma, and waterjet systems are not four versions of the same business case. They solve different production problems and move cost into different places. Buyers should begin with five questions:
- What materials make up most of weekly output?
- Is the shop paying more for shape complexity, cut speed, or edge condition?
- Which downstream steps absorb cleanup—or fail because of it?
- What support systems can the facility add calmly?
- How much operator attention can the process demand every week?
Without that framing, a cost comparison becomes sticker-price theater. A shop that mostly cuts 18 mm plywood panels for cabinet boxes has a different economic problem than a shop cutting 3 mm acrylic signage, and both are different from a fabrication shop processing 6 mm steel plate. The machine that wins in one context can be a financial drag in another.
The First-Year Budget Is Usually More Honest Than the Purchase Order
The purchase order is not the best comparison window. The first year is. That is where the machine, the infrastructure, and the operating rhythm finally show up in one place. A first-year budget usually has three layers:
- Machine acquisition, freight, and delivery.
- Site preparation, installation, commissioning, and startup support.
- Normal running cost once the machine enters real production.
This matters because a router, a non-metal laser, a plasma system, and a waterjet do not ask the building, the operators, or the maintenance team for the same things. A router needs a dust collection system sized to the spindle and table configuration, plus a stable vacuum source if the hold-down strategy depends on it. A laser needs ventilation and extraction appropriate to the materials being processed, and the electrical supply must match the machine’s actual draw. A plasma system needs compressed air, fume extraction, and often a water table or downdraft table to manage the thermal process. A waterjet needs a high-pressure pump, abrasive storage and handling, a water supply with appropriate filtration, and a plan for spent abrasive and slurry disposal.
Each of these support requirements carries a capital cost and an ongoing operating cost. The first-year budget is where those costs become visible. A machine that arrives at a facility without the supporting infrastructure will not reach its rated throughput, and the delay itself becomes a cost.
Three Questions Expose a Weak Quote Very Quickly
Before comparing technologies one by one, ask:
- What is included in the quoted machine scope?
- What must the facility still add before the system is genuinely productive?
- What will ordinary running weeks demand in consumables, utilities, maintenance, and labor?
If a proposal cannot answer those three layers clearly, it is not ready for serious comparison. the full startup scope in the quote. A quote that assumes the facility already has adequate extraction, compressed air, or water handling may be hiding the largest part of the real investment.
Router Economics Usually Hide Cost in Tooling and Workflow Discipline
Routers often look approachable from a capital standpoint, especially in woodworking, sign-making, plastics, foam, and other non-metal workflows. But the real cost picture often lives outside the frame and spindle. Router ownership commonly pulls money into:
- Tooling consumption.
- Spoilboard management.
- Dust extraction.
- Hold-down strategy and vacuum stability.
- Operator setup time.
- Material handling and re-zero discipline.
Router pricing should not be reduced to table size plus spindle power. A router pays back well when the business genuinely needs shaped parts, pockets, grooves, bores, nesting, or flexible geometry in non-metal materials. It becomes less economical when it is forced into work that mostly needs straight repetitive separation.
Consider a cabinet shop that runs a nesting router for most of its panel processing. The machine itself may carry a moderate price tag, but the real cost structure includes tooling that wears and needs replacement, spoilboard surfaces that must be refaced periodically, vacuum pumps that consume electricity and require maintenance, and dust collection that must be sized for the volume of chips and fines generated. The operator must manage tool offsets, monitor vacuum zones, and verify that the spoilboard is flat enough for consistent cut depth. Each of these tasks takes time, and time is a cost.
On the other hand, a shop that produces custom furniture pieces with varied geometry, pockets, and joinery will find that the router’s flexibility directly replaces multiple dedicated machines and manual operations. The same tooling and workflow costs that burden a high-volume straight-cut operation become acceptable overhead when the machine is doing work that would otherwise require several setups and skilled handwork.
For buyers working mainly in panel and non-metal sheet processing, it makes sense to compare router economics alongside CNC nesting machines designed for flexible panel workflows and decide whether the shop needs that flexibility badly enough to justify the operating burden around it.
Laser Cost Logic Depends on Material Value and Cleanup Savings
Laser pricing is easy to misunderstand because buyers reduce it to one shallow question: is the machine expensive or not? The more useful question is whether the process creates value elsewhere. In non-metal laser work, that value often comes from:
- Fine detail capability.
- Non-contact processing.
- Efficient handling of decorative or intricate work.
- Reduced mechanical cutting load.
- Less secondary cleanup on the right materials.
Laser does not win automatically on cost. It wins when those strengths reduce enough burden elsewhere to justify the ownership model. For buyers evaluating wood, acrylic, and similar non-metal materials, it helps to frame cost against laser cutters and engravers used in those non-metal applications, not against vague assumptions borrowed from unrelated metal-laser discussions.
A sign shop cutting acrylic letters and detailed plywood decorations will find that the laser eliminates the need for secondary sanding or deburring on many parts. The cut edge is clean, and intricate shapes that would require careful router toolpath planning and possibly multiple passes are produced in a single operation. The laser also removes mechanical cutting forces from the equation, which means thin or delicate materials can be processed without the risk of breakage or deformation.
The cost side of the laser includes the machine itself, which can be moderate to high depending on the work area and power, plus ventilation and extraction that must handle the fumes and particulates generated by the materials being processed. Laser tubes or sources have a service life, and the optics require periodic cleaning and alignment. The operator must understand focus distance, power and speed settings for different materials, and the safe operating envelope of the machine.
The economic case for a laser strengthens when the shop’s material mix includes acrylic, thin wood veneers, fabrics, paper products, or other materials where the laser’s edge quality and detail capability directly reduce downstream labor. It weakens when the shop mostly processes thick materials where the laser’s cutting speed drops and the edge quality advantage becomes less relevant.
Plasma Shifts Cost Toward Facility Burden and Edge Management
Plasma often enters the conversation when conductive metal cutting needs practical throughput at a cost level that feels commercially reachable. But plasma economics do not stop at the machine body. The ownership model often includes meaningful cost exposure in:
- Fume handling.
- Consumable wear.
- Power demand.
- Table maintenance.
- Edge cleanup or downstream finishing.
- Operator practices that affect consistency.
Plasma should be priced as a fabrication system, not just as a cutting table. If the part mix tolerates the thermal footprint well, plasma can still be the strongest commercial answer. If the downstream process is sensitive to edge condition or cleanup labor, the budget case can weaken quickly.
A fabrication shop cutting mild steel plate for structural components, brackets, and frames will find that plasma offers a productive balance of speed and cost. The machine cuts through thick material quickly, and the capital investment is often lower than a laser or waterjet of similar capability. But the shop must manage the thermal process carefully. The cut edge has a heat-affected zone, and depending on the material thickness and cutting parameters, there may be dross on the bottom edge that requires grinding or chipping. The consumables—nozzles, electrodes, and shields—wear and must be replaced on a schedule that depends on the amperage and duty cycle of the work.
The facility burden is also real. Plasma cutting generates fumes and fine particulate that must be extracted and filtered. The power draw of a plasma system can be significant, and the compressed air supply must be clean and dry to protect consumable life. The table itself, whether water table or downdraft, requires maintenance to keep the cutting environment stable.
Plasma becomes the right economic choice when the shop’s parts tolerate the thermal edge condition and the throughput advantage outweighs the consumable and facility costs. It becomes a poor choice when the parts require tight tolerances, clean edges, or minimal heat input, because the downstream correction work will consume the savings from the cutting process itself.
Waterjet Usually Carries the Highest Burden When Flexibility Is Not Needed
Waterjet systems often look expensive because buyers compare them from the wrong angle. They compare them against a single-machine price expectation instead of comparing them against the conditions where waterjet becomes commercially rational. Waterjet economics become easier to defend when one or more of these conditions are true:
- Heat must be minimized.
- Material flexibility is commercially valuable.
- The shop handles mixed materials that complicate other cutting routes.
- Edge quality and downstream material condition matter enough to justify the burden.
If those conditions are not important, waterjet can look like a premium process carrying too much cost. If they are important, the more expensive ownership model may still be the least risky route.
A shop that cuts stainless steel, aluminum, glass, stone, and composites in the same week has a material mix that defeats most single-process solutions. A laser struggles with reflective materials and thick non-metal sheets. A plasma introduces heat that can distort thin aluminum or compromise the properties of certain alloys. A router lacks the ability to cut hard, brittle, or abrasive materials without excessive tool wear. The waterjet cuts all of these materials with the same abrasive water stream, producing a cut with no heat-affected zone and a reasonably clean edge.
The cost structure of a waterjet includes the high-pressure pump, which consumes significant electrical power and requires regular maintenance on seals and plungers. The abrasive garnet is a consumable that adds to the per-part cost, and the spent abrasive and slurry must be collected and disposed of properly. The machine requires a water supply with appropriate filtration, and the cutting table and catch system must be maintained to prevent wear from the abrasive-laden water.
The waterjet’s economic case rests on the value of its flexibility and the absence of thermal effects. A shop that regularly processes heat-sensitive materials, or that must maintain material properties in the cut zone, will find that the waterjet’s higher operating cost is justified by the elimination of rejected parts and rework. A shop that mostly cuts one material with forgiving thermal characteristics will find the waterjet’s burden hard to justify.
Hidden Cost Drivers Usually Decide the Winner
Most cutting-system comparisons are lost in hidden cost drivers rather than obvious ones. The most common hidden drivers include:
- Utilities and facility readiness.
- Ventilation, extraction, or fluid-handling support.
- Tooling or consumable replacement.
- Operator training and setup discipline.
- Secondary cleanup and finishing burden.
- Maintenance intervals and service access.
- Material-handling time outside the cut itself.
These are the items that turn a good-looking quote into an expensive surprise. A router that requires a new spoilboard every few weeks, a laser that needs its optics cleaned weekly, a plasma system that goes through consumables faster than the supplier estimated, or a waterjet that needs pump service more often than planned—each of these shifts the monthly cost picture in ways that the initial quote never revealed.
The facility itself is often the largest hidden cost. A shop with inadequate electrical service will need a transformer upgrade. A shop without compressed air will need a compressor sized for the cutting process. A shop without proper ventilation will need an extraction system that may cost as much as a small machine. These infrastructure costs are not optional, and they must be included in the comparison.
A Cost-Exposure Matrix Is Better Than a Fake Price Ranking
| Cost Area | Router | Non-Metal Laser | Plasma | Waterjet |
|---|---|---|---|---|
| Base machine burden | Often moderate relative to flexible capability | Often moderate to high depending on scope | Often moderate | Often high |
| Facility support burden | Extraction and hold-down matter | Ventilation and safe operating setup matter | Fume handling and power burden matter | Water handling and system support matter |
| Consumables or tooling | Tooling and spoilboard costs stay active | Process-specific consumables and service items apply | Consumables are a meaningful budget line | Abrasive and wear-related costs can be significant |
| Cleanup or secondary work | Depends on material and tooling fit | Often lower on suitable non-metal jobs | Edge cleanup may be meaningful | Depends on part standard and material |
| Best economic case | Flexible non-metal shaping and nested work | Detailed non-metal processing where finish and detail matter | Productive conductive-metal cutting where the tradeoff fits | Heat-sensitive or mixed-material work where flexibility pays |
This kind of matrix does not tell the buyer what to purchase automatically. It tells the buyer where the budget pressure will probably show up. A shop that has limited tolerance for ongoing consumable costs should weight that row heavily. A shop that has ample floor space and utility capacity but tight labor availability should weight the operator-attention row differently. The matrix is a starting point for honest comparison, not a substitute for it.
Buyers Should Budget for the Workload They Actually Run
The same technology behaves very differently financially depending on job mix. A router in high-mix custom panel work lives inside one business model. A router used mostly for straight breakdown lives inside another. A laser serving decorative acrylic and detailed non-metal parts is not the same financial case as a laser bought for vague future flexibility. A plasma system running suitable metal fabrication work is different from a plasma purchase made without honest edge-condition expectations.
Ask:
- What percentage of our work really benefits from this process?
- Which costs grow when the weekly mix changes?
- Where does labor still sit outside the machine?
- What support systems are mandatory rather than optional?
- Which burdens only become visible after normal production begins?
The budget should be built around the dominant weekly reality, not around the most impressive sample job. A shop that runs 80 percent straight panel cuts and 20 percent shaped parts should not buy a nesting router based on the 20 percent. A shop that runs 70 percent acrylic signage and 30 percent plywood should not buy a laser based on the plywood work. The dominant workload defines the economic case, and the minority workload should be handled by the process that serves it best without compromising the main line.
Consider a shop that produces custom cabinetry with a mix of standard boxes and one-off pieces. The nesting router handles the shaped parts, the dados, and the joinery, but the straight panel cuts might be faster and cheaper on a dedicated panel saw. The shop that recognizes this split can buy a smaller nesting router and a panel saw, rather than forcing all work through one machine. The total investment may be similar, but the operating cost structure is more efficient because each machine works in its economic sweet spot.
How Pandaxis Fits the Non-Metal Cutting Side of the Discussion
For non-metal processing, panel work, and broader woodworking-related cutting decisions, the practical next step is to review the Pandaxis machinery catalog as a grouped buying reference and compare the process lane first: straight panel breakdown, flexible nesting, or non-metal laser detail work. The catalog groups machines by function, which makes it easier to see the range of options within each process category before comparing across categories.
Compare Ownership Models, Not Just Machines
That is the practical answer to the title. Routers usually hide more cost in tooling, hold-down, and operator workflow. Lasers depend heavily on material fit, extraction, and process intent. Plasma has to be priced with its fabrication burden, not just its cutting speed. Waterjet must be judged with its full support structure, not just its machine cost.
Each cutting technology is really an economic system around a process, not just a machine with a price. Once buyers compare the systems instead of only the shells, the budget becomes much more honest and the risk of an attractive but short-lived decision drops sharply.
The machine that wins the comparison is the one whose cost structure matches the shop’s actual workload, facility capabilities, and tolerance for ongoing operating burden. That machine may not be the cheapest on the quotation, and it may not be the most impressive in a demonstration. But it will be the one that produces parts at a predictable cost per part, week after week, without surprises that erode the margin.
Before signing a purchase order, build the first-year budget for each candidate technology. Include the machine, the infrastructure, the consumables, the labor, and the secondary work. If the numbers are close, the decision can rest on softer factors like service access, operator familiarity, and supplier support. If the numbers are not close, the decision is already made—the technology that fits the workload and the facility will win on cost per good part, which is the only number that matters in production.