Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
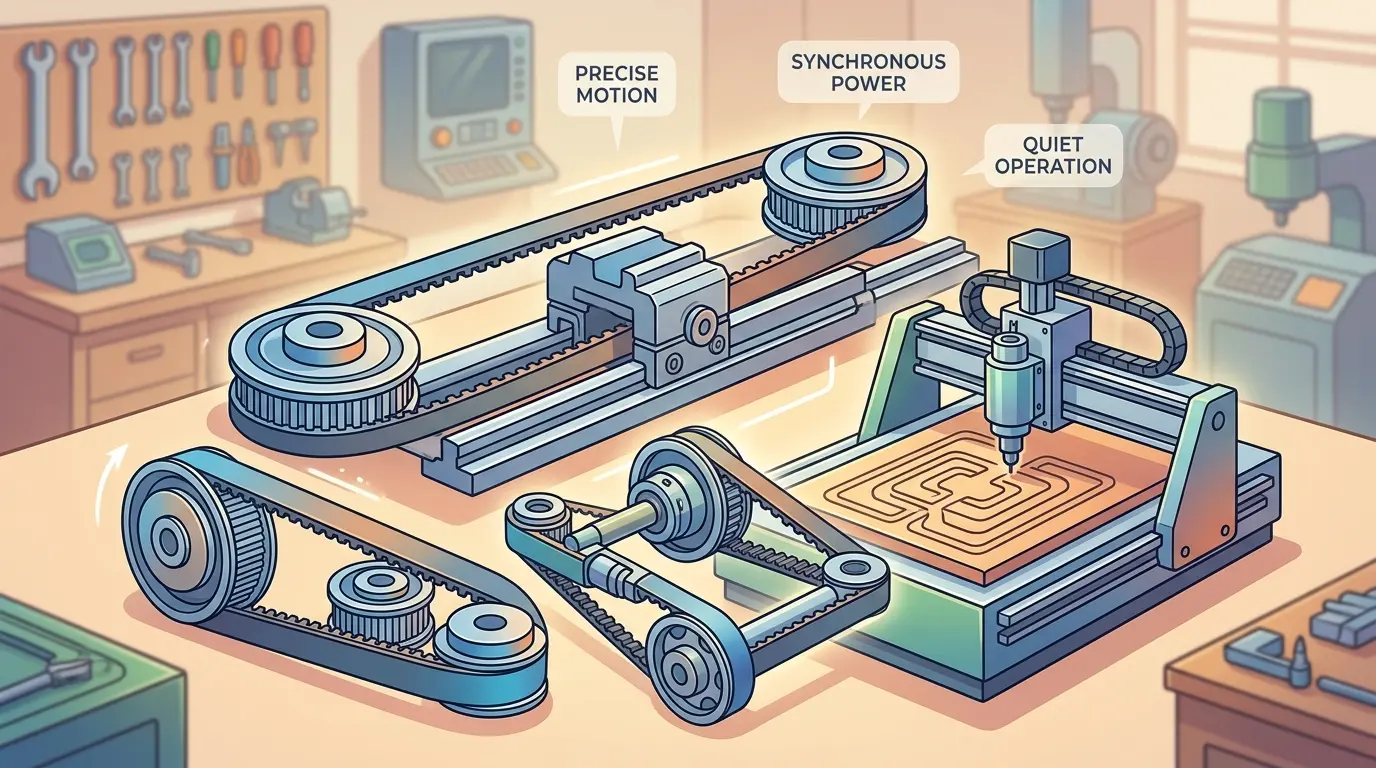
Timing belts and pulleys rarely get the scrutiny they deserve until a machine starts drifting from its original motion character—repeatability fades, acceleration feels different, or a gantry sounds uneasy at a familiar feed rate. Buyers often default to lazy extremes: belt drive is either cheap and imprecise or fast and automatically superior. Both miss the real question. This article forces the conversation back to workload fit, explaining why belt-driven motion is a transmission choice with a defined operating window, not a status symbol. For production teams evaluating routers, gantries, or auxiliary axes, the decision hinges on force demand, travel length, and service access—not ideology.
Why Belt-Driven Motion Gets Misjudged
Timing belts and pulleys rarely get attention until motion quality starts to drift. A machine accelerates differently than it used to. Position repeatability fades over long travel. A gantry sounds composed at one feed rate and uneasy at another. Or a buyer hears “belt-driven” and reaches for one of two lazy conclusions: either belt drive is cheap and imprecise, or belt drive is fast and therefore automatically superior. Both shortcuts miss the point.
Timing belts and pulleys transmit synchronized motion between rotating elements without the slip inherent to friction belts. In the right machine class, they are practical, fast, straightforward to service, and commercially sensible. In the wrong machine class or workload, they become the component everyone blames after the design has been asked to do more than it should. The useful question is not whether belts are good or bad. It is what job they are being asked to carry.
Belt Drives Exist Because Not Every Axis Needs Screw-Level Rigidity
Many buyers compare drive systems as though every axis performs identical work. That is the first mistake. Some machine designs prioritize high rigidity under cutting load. Others prioritize longer travel, lighter moving mass, faster rapid movement, simpler service, or a lower-cost structure that still makes sense for routing, panel work, lighter machining, or auxiliary movement.
Timing belts belong in that second conversation. They are not there because engineers overlooked ballscrews or heavier transmission systems. They are there because not every axis needs screw-level stiffness to produce commercially acceptable results. On lighter routers, gantry systems, or machine subsystems with moderate force demand, belts can be a rational choice precisely because they reduce weight and complexity while keeping motion synchronized.
The problem starts when shops stop thinking about job type and start thinking only about hierarchy. Belts are not a prestige feature, and they are not automatically a flaw. They are a transmission choice. Like any transmission choice, they have a suitable workload and an obvious breaking point.
What The Belt-And-Pulley Pair Actually Does
The belt and pulley set transfers rotary motion from the motor or driven shaft to another rotating element in a tooth-matched way. Because the teeth engage, the system avoids the deliberate slip associated with general-purpose belt drive. In CNC use, that matters because synchronized motion is the whole point. If the motor turns, the axis or subsystem needs to respond predictably.
That sounds simple, but several practical details sit underneath it. Pulley diameter changes how motion is translated. Belt width and tooth profile influence how much load the system can handle and how it behaves dynamically. Tension determines whether the belt tracks correctly and responds cleanly. Alignment determines whether the belt lives a healthy life or wears itself into trouble.
In other words, timing belts and pulleys are not one part. They are a relationship. Shops that replace one element without checking the relationship often fix symptoms briefly while keeping the real cause alive.
Pulley Ratio Is A Motion-Character Decision, Not Just A Speed Decision
Buyers often notice pulley size because it changes visible travel behavior, but the effect goes beyond top speed. Pulley ratio influences how motor rotation becomes axis movement, which then shapes resolution feel, responsiveness, acceleration character, and how the machine behaves under changing load. A ratio that makes a light machine feel quick may also make it less forgiving if the workload becomes heavier than expected.
This is why pulley choice should be read as part of machine intent. Designers are not only choosing speed. They are choosing how the machine trades motion character against force demand. For the buyer, that means a belt-driven machine should be evaluated in motion, not just on a spec sheet. Does it move in a way that fits the real work? Does it stay composed under the accelerations and direction changes that matter in the actual program?
Those questions matter because two belt-driven machines can look similar in principle and feel very different in practice. Ratio choice is one reason why.
Where Timing Belts Usually Make Sense
Timing belts typically make the most sense where travel is significant, moving mass should stay moderate, and the cutting or positioning load fits the machine’s intended class. That often includes compact routers, light gantry systems, faster non-metal routing platforms, some feeder or auxiliary mechanisms, and subsystems where synchronized motion matters more than heavy-force resistance.
They also make sense where service access matters. Belts are easier to inspect than many internal transmission arrangements, and replacement can be simpler if the machine is designed intelligently. On the right machine, that can reduce downtime and lower maintenance complexity.
This is one reason belt drive shows up so often in lighter routing families and format-driven machines. When the real job is sheet processing, contour routing, signage, templates, plastics, or similar workloads, the machine may benefit more from travel behavior and manageable maintenance than from the absolute stiffness expected in heavier metal-cutting contexts. The drive choice follows the work, not the other way around.
Where Belts Stop Being An Honest Answer
Belts stop being convincing when the job demands higher sustained cutting force, stronger resistance to deflection, or a motion profile the belt system was never intended to carry. This is where generalizations become dangerous. A belt drive that performs well in panel routing can become a weak link in a more demanding cutting environment if the machine is pushed into heavier work, tighter expectations, or longer-term load that exceeds the original design logic.
That does not mean belt-driven motion is inaccurate by identity. It means the transmission has a window. When the shop pushes outside that window, problems usually show up first in repeatability, dynamic response, or maintenance frequency. Buyers who refuse to name the real workload end up arguing about ideology instead of motion physics.
The practical standard is simple. Ask what force, travel, acceleration, and positioning burden the axis is expected to manage every day. If the answer is modest and repetitive, belts may be entirely appropriate. If the answer points toward heavier rigidity demand, a different transmission strategy may be the more honest choice.
Belt-Driven Does Not Automatically Mean Loose Or Cheap
Another bad shortcut in the market is to hear “belt-driven” and translate it into “sloppy.” That is not an engineering conclusion. It is a prejudice. A belt-driven system can hold acceptable repeatability very well inside its intended machine class when tension, alignment, frame behavior, and load expectations are sensible.
The real issue is not looseness by identity. The real issue is whether the machine around the belt system was designed coherently. A weak frame, poorly managed gantry squareness, bad pulley fastening, or unrealistic cutting demand can all make a belt-driven axis look worse than the belt alone deserves. Buyers should therefore resist both extremes: assuming belt drive is automatically weak, or assuming it can be pushed into any job if maintenance is frequent enough.
That balanced view helps avoid false decisions. The transmission should be judged as part of a machine system, not as an isolated phrase on the quote.
Travel Length, Speed, And Load Decide The Economics
One reason timing belts remain attractive is that they can support fast travel on longer axes without the same mass and cost pattern as heavier alternatives. That matters on format-driven equipment. But speed alone is not the win. The win is speed that still fits the cut quality and repeatability the shop actually needs.
This is why the real economic conversation should include travel length, acceleration demand, duty cycle, and the material/process mix. A machine that spends its day moving quickly between light cuts may benefit from belt-driven motion. A machine that spends its day pushing harder into the work will expose the transmission sooner. The belt system is therefore part of the machine’s business model, not only part of its mechanics.
Buyers who understand that usually make better comparisons. They stop asking which drive is superior in theory and start asking which drive supports the part mix with the least expensive compromise over time.
Tension And Alignment Decide More Than Buyers Expect
When belt-driven motion becomes unstable, the problem is often not the belt concept itself. It is tension, alignment, or fastening quality. Incorrect tension can make the axis feel lazy, noisy, or inconsistent. Poor pulley alignment shortens belt life and can introduce uneven wear that confuses diagnosis. Loose pulley attachment can mimic much larger machine problems.
This is why routine inspection matters. Belt condition is not only about whether the belt is visibly damaged. It is about whether the full relationship remains healthy. A machine can still move and still be outside its best operating range. That is the dangerous middle ground where production keeps going while finish, repeatability, or confidence slowly declines.
Maintenance teams should therefore watch for early signs rather than waiting for breakage. A cheap belt is not really cheap if the shop uses the whole machine as a fault detector instead of checking the transmission proactively.
What Early Wear Usually Looks Like
Belts rarely begin with dramatic failure. More often, they start by changing how the machine sounds or feels. Axis behavior may become harsher during acceleration. Positioning may seem slightly less settled after quick moves. The machine may leave a finish pattern that appears process-related but is really motion-related. Recurring need for tension adjustment, unusual belt dust, visible tooth wear, edge fraying, or inconsistent tracking can all be early warnings.
The important lesson is that timing belts fail as part of a system. Debris, misalignment, mounting issues, weak pulley fastening, or an overloaded axis can shorten their life significantly. If the shop treats every belt replacement as isolated wear, the same failure pattern often returns.
This is especially true where contamination is normal. Dust, fines, and neglected covers do not always destroy a belt immediately, but they can accelerate wear and distort maintenance intervals enough that the drive begins to feel unreliable long before it looks catastrophic.
Gantry Accuracy Still Depends On More Than The Belt
When belt-driven motion is used on a gantry system, some shops put too much diagnostic weight on the belt itself and too little on the larger moving structure. Gantry squareness, rail condition, mounting stiffness, side-to-side synchronization, and axis geometry all shape the result. If one side of the system behaves badly, the belt may receive the blame even though the machine is really suffering from broader alignment trouble.
This matters in practical service because replacing the belt may restore tension while leaving the structural cause alive. The same symptoms then reappear, and the belt drive concept gets blamed unfairly. Better troubleshooting asks whether the transmission is unhealthy or whether the surrounding geometry is forcing the transmission to live badly.
That question is especially important in long-travel machines where frame behavior and synchronization discipline can matter as much as the belt condition itself.
Belt Problems Are Often Misdiagnosed As Electrical Or Tuning Problems
A useful diagnostic habit is to avoid blaming the control first. When motion quality changes, teams often jump toward servo tuning, parameter trouble, or control instability. Those are real possibilities, but they are not the only ones. Mechanical transmission issues can create symptoms that resemble electrical or software problems when the axis response no longer matches what the control expects.
That is why belt-driven machines should be diagnosed across both sides of the system. If axis behavior seems suspicious, check the transmission before rewriting the control narrative. In some cases, what looks like unstable servo response actually starts with belt tension, pulley movement, or related transmission looseness. In other cases, nearby parts such as couplers can create similar confusion.
Good diagnosis means refusing to let one symptom automatically choose one cause.
Replace The Belt, But Review The Workload And The Environment Too
When a belt is worn, replacement may be necessary. But the more useful question is what made it wear that way. Was the axis overloaded? Was alignment poor? Was contamination unmanaged? Was the maintenance interval too loose? Did someone chase speed or acceleration settings beyond what the machine was really meant to carry? If the answer to any of those is yes, belt replacement alone is only a temporary reset.
This matters because transmission problems often hide larger design or usage mismatch. A belt drive can live a healthy life in one shop and fail repeatedly in another because the second shop is using the machine for work it was never intended to run or maintaining it as if belt condition should never matter. Both errors are costly.
The better approach is to treat replacement as a review point. Replace the part, yes. But also inspect the axis logic around it and decide whether the transmission is healthy in context, not only in isolation.
How Belt-Driven Motion Fits Real Shop Workflows
For shops running lighter routing, sheet handling, and similar format-driven work, timing belts are easiest to understand when they are tied to machine class and workflow. Belt-driven motion can be completely sensible if the machine is matched to the workload. That is especially true where long travel, responsive movement, and maintainable service burden matter more than heavy-force metal-cutting rigidity.
That broader fit is easier to judge when looking at routing-oriented categories such as CNC nesting machines or the wider Pandaxis machinery lineup through the lens of actual daily work. The right question is not whether a drive type sounds premium. The right question is whether the machine can hold its expected output window with sane maintenance and without constant excuses.
Buyers who keep the discussion there usually make better decisions than buyers who compare transmission types like status symbols.
Judge Timing Belts By The Job, Not By Bias
CNC timing belts and pulleys are used because synchronized belt transmission can be fast, practical, and serviceable in the right kind of machine. They are not universal, and they are not automatically inadequate. They are a fit question.
If the workload, travel length, speed demand, and load pattern match the design, belt-driven motion can perform honestly and economically. If the workload exceeds that design logic, the belt becomes the first place the mismatch shows up. That is the real takeaway. Do not judge timing belts by prejudice. Judge them by whether the machine, the axis, and the production job are asking the same thing from one another.