Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
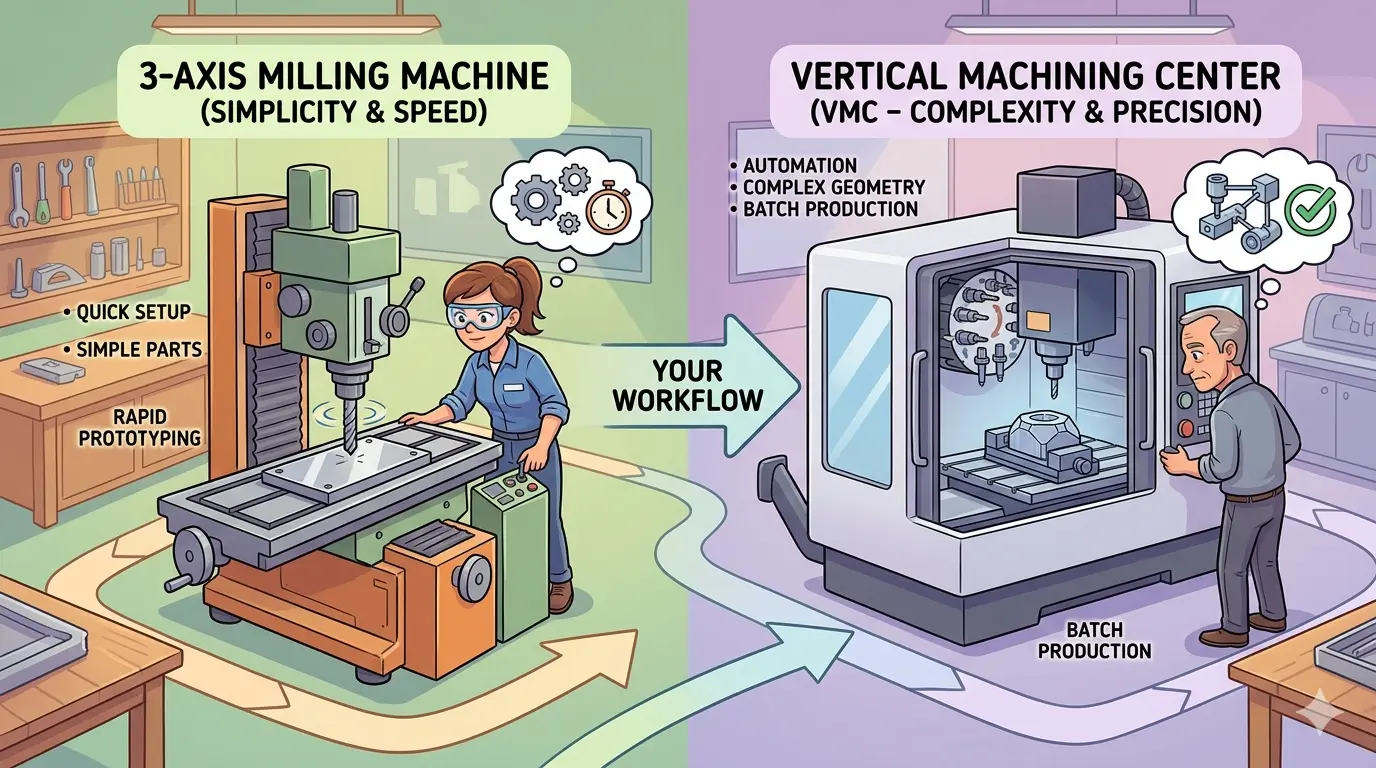
Before comparing axis counts or spindle specs, the real decision hinges on where your shop loses money between the cuts. A conventional 3-axis mill and a VMC can both hold tolerance on identical geometry, but they diverge sharply on setup recovery, manual tool changes, restart discipline, and operator dependence. If your part families return irregularly and adaptation drives value, the simpler mill wins. If recurring brackets, longer tool lists, or shift handoffs are leaking hours into re-indicating vises and re-entering offsets, the VMC’s stored process knowledge changes the economics. Start with the Monday-morning test: how many things must go right before the first good part?
Start With The Workflow, Not The Label
A conventional 3-axis milling machine and a vertical machining center (VMC) can often cut the same part to the same print. The geometry is rarely the deciding factor. The real difference is how much of the surrounding process—tool changes, setup recovery, operator intervention, restart discipline—each machine package removes or leaves behind.
That distinction matters because the purchase decision should begin with workflow, not with a machine category. If the shop lives on prototypes, repair work, fixtures, and irregular jobs, a simpler 3-axis mill is often the more disciplined purchase. If the same part families keep returning and too much time is disappearing into setup recovery, manual tool handling, and repeated intervention, a VMC usually becomes the stronger operating model.
Use The Monday-Morning Test
The fastest practical filter is to think about the first good part after a break in production. Not a demo part. The first good part after a weekend, a tooling change, a shift handoff, or a repeat order that comes back three weeks later.
Ask one blunt question: how many things must go right outside the program before the spindle can start with confidence?
If the answer includes a lot of manual touching off, fixture rechecking, tool loading, cleanup, and operator memory, the process is still depending heavily on flexibility and attention. That often points toward a conventional 3-axis milling route.
If the business needs the route to restart cleanly with fewer manual decisions and fewer hidden minutes before the first good part, the logic usually starts leaning toward a VMC.
Where A 3-Axis Milling Machine Still Fits Better
A simpler 3-axis mill is often the right answer when operator involvement is part of the value model rather than a cost to be removed.
That usually includes shops where:
- Part families change constantly.
- Jobs return irregularly or not at all.
- One-off fixtures, repairs, and engineering changes are common.
- Tool lists stay manageable.
- The business values fast adaptation more than low-intervention repetition.
In that environment, direct operator access is not a weakness. It is the operating method. The machine stays open, adaptable, and easy to justify because the work itself is unstable. A machinist who can read a print, build a quick fixture, and cut a one-off part in an afternoon is worth more than an automated toolchanger in that setting.
Consider a job shop that takes in a steady stream of repair work for aging production equipment. A hydraulic manifold cracks, a gearbox housing wears out of spec, a fixture plate gets damaged. Each job is different. The operator needs to see the part, measure the damage, decide on a repair strategy, and often machine a replacement from a solid block. There is no repeat order coming next week. There is no tooling package to standardize. The value in that shop comes from the machinist’s ability to adapt quickly, and a manual 3-axis mill gives them the direct feel and visibility they need. Adding a toolchanger to that workflow would not remove meaningful labor—it would just add a mechanism that rarely gets used.
The same logic applies to prototype work. When a design engineer hands over a new part drawing every few days, the shop is constantly proving out new programs, testing new workholding, and adjusting feeds and speeds. The first article is the only article. A VMC’s automation does not help when every job is a fresh start. What helps is a machine that is easy to set up, easy to adjust, and easy to read.
When A VMC Changes The Economics
A VMC usually starts paying back when the biggest losses no longer come from material removal. They come from everything around the cut.
That often shows up as:
- Repeated tool changes that interrupt the day.
- Setup drift between repeat runs.
- Messy restarts after a stop.
- Too much dependence on one operator’s memory.
- Shift handoffs that feel risky or slow.
The recurring part may still be a plate, housing, bracket, manifold, or fixture block. Geometry does not have to become exotic for VMC logic to make sense. The real shift is that repetition has become important enough that manual habits are now leaking margin. Every time an operator walks to the tool crib, re-indicates a vise, or re-enters an offset from a notebook, the shop is paying for the machine’s lack of structure.
Think about a typical production day in a shop that runs the same three bracket families every week. Each bracket needs six tools: a face mill, two end mills, a drill, a tap, and a chamfer tool. On a manual 3-axis mill, the operator changes tools by hand six times per part. With a run of fifty parts, that is three hundred manual tool changes. At two minutes each, that is ten hours of non-cutting time just for tool handling. Add in the risk of a wrong offset after each change, and the process is bleeding money in ways that do not show up on a simple cost-per-part calculation.
A VMC with a 20-tool magazine changes those tools automatically in seconds. The operator loads the tools once, sets the offsets once, and lets the machine cycle. The same fifty-part run now requires maybe thirty minutes of tool-related labor instead of ten hours. That is the kind of difference that changes the economics of the entire shop.
A Practical Comparison Table
| What The Shop Looks Like | Better Starting Fit | Why |
|---|---|---|
| Jobs change constantly and return unpredictably | 3-axis milling machine | Flexibility is still worth more than deeper process packaging |
| The same part families keep returning with longer tool lists | VMC | Repeated manual intervention is now shaping cost |
| One skilled machinist owns most jobs start to finish | 3-axis milling machine | Direct judgment is already built into the operating model |
| Multiple operators or shifts must run the same work | VMC | Standardized setup and cleaner handoff matter more |
| Fixturing changes frequently and prove-out is part of the day | 3-axis milling machine | Adaptive setup work still outweighs automation around it |
| Chip cleanup, restart hesitation, and repeated interruptions are routine | VMC | The route needs more structure around the cut |
This table is more useful than comparing travel numbers in isolation because it ties the decision to actual production stress. A machine with generous axis travel but no toolchanger will not solve a tool-change bottleneck.
Setup Recovery Usually Decides The Long-Term Cost
Many buying conversations treat accuracy as if it lives only in the iron. In real production, accuracy is also preserved or lost during recovery. A machine that holds tight tolerances on a fresh setup but drifts when the job returns three weeks later is not delivering repeatability—it is delivering a gamble.
The better questions are:
- How often does this job come back?
- Can a different operator restart it with confidence?
- How much time is spent rechecking fixture location, tool state, and offsets before the first good part?
- Is the approved setup stored in a repeatable method or mostly in one person’s notes?
If setup recovery remains personality-driven, the lower-priced machine may become the more expensive route because it keeps consuming skilled labor outside the actual cut. A VMC with tool length measurement, fixture offsets, and stored tool data removes much of that recovery burden. The operator loads the program, verifies the setup against the stored values, and starts cutting.
Let us walk through a concrete example. A shop machines a valve body that comes back as a repeat order every six weeks. On a manual 3-axis mill, the setup procedure looks like this: the operator finds the previous job notes, which may or may not be complete. They locate the vise, indicate it square, and tram it in. They load the tools one by one and touch each one off against a known surface. They re-verify the fixture location against the program zero. They cut a test part, measure it, and adjust offsets. The whole process takes three to four hours, and it relies on the operator remembering details that may not be written down.
On a VMC with stored offsets and tool data, the same setup takes thirty minutes. The operator calls up the saved program, verifies that the tools in the magazine match the tool table, checks the fixture against the stored work offset, and runs a quick dry cycle. The machine holds the process knowledge. The operator does not have to remember anything that is not already in the control.
That difference matters more than the purchase price in most shops. If the job returns ten times a year, the manual route consumes thirty to forty hours of skilled labor just in setup recovery. At shop rates, that is thousands of dollars per year—often enough to justify the VMC price premium on its own.
Tool Count And Intervention Tell The Truth Quickly
Another useful filter is to stop asking how many axes the spindle can move in and start asking how many interventions the route requires to finish an ordinary job.
If recurring parts need only a short tool list and the work changes constantly, manual handling may still be perfectly rational. The operator can load three tools, touch them off, and cut the part without losing meaningful time.
If the same recurring parts depend on longer tool sequences every time, interruptions begin carrying both time cost and concentration cost. Every manual tool change is a chance for a crash, a wrong offset, or a broken edge finder. Every interruption breaks the operator’s focus on the actual cutting process.
That is where many shops start feeling the need for a VMC before they can explain it cleanly in technical terms. They are not always chasing harder parts. They are trying to remove routine interruption from familiar work.
Consider the difference in operator attention. On a manual mill, the operator is constantly switching between cutting, measuring, changing tools, and re-establishing references. Each switch is a chance for error. A wrong tool loaded, an offset entered incorrectly, a part moved in the vise—all of these are more likely when the operator is juggling multiple responsibilities. On a VMC, the operator’s role shifts to monitoring and verification. They load the program, check the setup, and let the machine cycle. The concentration cost drops dramatically, and so does the error rate.
Staffing Pressure Changes The Decision Fast
Some machines look economical only because the business quietly assumes the same highly capable operator will always be standing there.
That assumption weakens as soon as the shop:
- Adds a shift.
- Rotates staff.
- Grows output.
- Tries to reduce dependence on one person’s judgment.
This is one of the strongest reasons shops move toward a VMC even when the part family itself has not changed very much. The issue is not that the 3-axis mill can no longer cut the part. The issue is that the business needs the process to survive normal staffing conditions. A VMC with a toolchanger, standardized offsets, and stored programs lets a less experienced operator run the same work with less risk. The machine carries more of the process knowledge.
Think about what happens when a shop adds a second shift. The day-shift operator has been running a particular job for months. They know the quirks of the setup, the way the material behaves, the exact offsets that work. When the night-shift operator comes in, they have to learn all of that from scratch. On a manual mill, that learning curve is steep and risky. The night operator might not know that the vise needs to be re-indicated, or that the tool offsets drift after a certain number of parts. The result is scrap, rework, and frustration.
On a VMC, the night operator has a much simpler job. The program is stored. The tool offsets are in the control. The fixture is located and verified. The operator’s main responsibility is to load material, start the cycle, and check the first part. The machine does the rest. That is a much safer handoff, and it is one of the main reasons shops invest in VMCs as they grow.
Base Price Is Only One Line
The bottom-line number matters, but it does not finish the decision. Tooling, workholding, startup support, control familiarity, service clarity, commissioning, and daily process discipline all shape the real cost of ownership.
A 3-axis mill with a low base price can become expensive quickly if it requires custom fixturing for every job, frequent spindle maintenance, or a control that nobody on the floor understands. A VMC with a higher base price can become economical if it standardizes setups, reduces tooling inventory, and lets the shop run more work with the same headcount.
Buyers should compare machinery quotes line by line instead of reducing the decision to travel and base price. They should also verify factory-direct support and recovery assumptions before deciding that the lower quote is automatically safer. A machine that sits idle waiting for a service visit is not a bargain at any price.
Let us look at the cost structure more carefully. A manual 3-axis mill might have a base price that is forty percent lower than a comparable VMC. But the manual machine requires a more skilled operator, which means a higher hourly rate. It requires more time per part, which means lower throughput. It requires more setup time, which means less productive spindle time. It requires more tooling inventory, because the operator has to have the right tools on hand for every job. When you add all of those costs together, the manual machine can easily become the more expensive option within the first year of operation.
The VMC, by contrast, has a higher upfront cost but lower operating costs. The operator can be less experienced, because the machine handles more of the process. The throughput is higher, because tool changes are automatic and setup times are shorter. The tooling inventory is smaller, because the toolchanger holds a standard set of tools that covers most jobs. The result is a lower cost per part, even though the machine itself costs more.
Spindle Time And Throughput: The Hidden Math
One of the most overlooked differences between a manual 3-axis mill and a VMC is the ratio of cutting time to total job time. On a manual machine, the spindle is actually cutting for maybe thirty to forty percent of the total job time. The rest is spent on tool changes, measurements, setup adjustments, and operator decisions. On a VMC, that ratio often climbs to seventy or eighty percent, because the machine handles the interruptions automatically.
That difference has a direct impact on throughput. A shop that runs a VMC can often produce the same number of parts in half the time it takes on a manual mill. That means the VMC can handle more work without adding headcount. It also means the shop can take on more jobs without expanding the floor space.
Consider a shop that runs a mix of production and prototype work. The production jobs are recurring brackets and housings that need six to eight tools each. The prototype jobs are one-off parts that need only two or three tools. On a manual mill, the production jobs consume most of the operator’s time, leaving little room for prototypes. On a VMC, the production jobs run mostly unattended, freeing the operator to set up prototype work on a second machine. The shop gets the best of both worlds: high throughput on production and flexibility on prototypes.
Workholding And Fixturing: The Often-Forgotten Variable
The choice between a 3-axis mill and a VMC also affects how the shop approaches workholding. A manual mill is often paired with simple vises and clamps, because the operator is always present to adjust and verify. A VMC, by contrast, encourages more sophisticated workholding, because the machine can run unattended for longer periods.
That shift has practical consequences. A shop that moves to a VMC often invests in modular fixturing systems, hydraulic vises, or tombstone setups that allow multiple parts to be machined in a single cycle. These systems cost more upfront, but they reduce setup time and increase throughput. They also make the process more repeatable, because the fixture location is fixed and verified once, rather than re-established every time.
The workholding decision also affects the machine’s flexibility. A manual mill with a simple vise can handle almost any part that fits in the envelope. A VMC with a dedicated fixture is faster on the parts it is set up for, but slower to change over to something new. Shops that run a wide variety of parts need to balance that tradeoff carefully.
Control Familiarity And Operator Training
Another factor that often gets overlooked is the control system. A manual 3-axis mill typically has a simpler control that is easy to learn and intuitive to use. A VMC has a more complex control with more features, which requires more training to use effectively.
That difference matters for shops with a less experienced workforce. A shop that hires entry-level operators may find that a manual mill is easier for them to learn, because the control is straightforward and the operator is always in the loop. A VMC, by contrast, requires the operator to understand tool offsets, work coordinates, and program management before they can run the machine safely.
However, the training investment in a VMC often pays off in the long run. Once the operator learns the control, they can run the machine more efficiently and handle a wider range of jobs. The VMC also reduces the risk of operator error, because the machine handles more of the process automatically.
Maintenance And Reliability: Planning For Downtime
Both machine types require regular maintenance, but the nature of that maintenance differs. A manual 3-axis mill has fewer moving parts and simpler systems, which means fewer things can go wrong. A VMC has a toolchanger, a more complex control, and additional servos and drives, which means more potential failure points.
That does not mean a VMC is less reliable. It means the shop needs to plan for maintenance differently. A VMC requires regular checks of the toolchanger, the spindle, and the lubrication system. The shop also needs to keep spare parts on hand, such as toolchanger arms, sensors, and limit switches.
The key is to build maintenance into the production schedule rather than waiting for a breakdown. A shop that runs a VMC should have a preventive maintenance plan that includes daily checks, weekly inspections, and monthly service. That plan should be documented and followed consistently.
The Most Honest Way To Decide
Take one real part family and run the full route on paper.
Map:
- Setup time when the job returns.
- Number of tools that must be loaded or verified.
- Manual intervention before the first good part.
- Restart confidence after a stop.
- Cleanup and housekeeping burden around the cycle.
If the route still depends mainly on adaptation, short tool lists, and operator-led judgment, a 3-axis milling machine may still be the better business fit. If the route is now suffering from recurring parts, longer tool sequences, staffing handoffs, and repeated restart friction, the VMC is usually the stronger long-term choice.
Choose the machine whose capacity matches the route the factory must actually run. It is about which machine removes the costs that are actually hurting the shop today. For shops that need to compare options across a broader equipment range, reviewing available machining and fabrication equipment can help clarify what fits the workflow before committing to a purchase.