Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
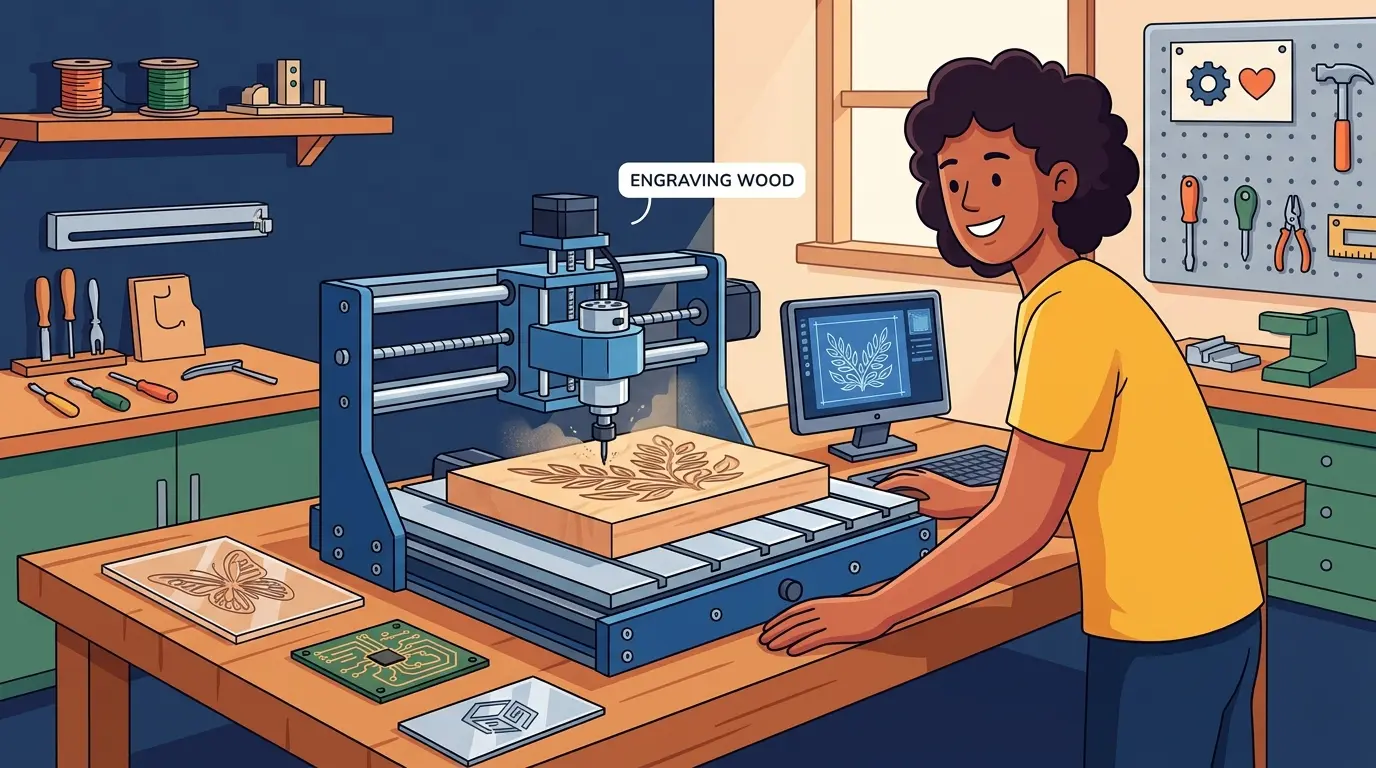
Before you spec a 3018 Pro into any workflow, separate the marketing label from the machine’s actual structural envelope. This guide forces that distinction by grading the router on repeatable, calm production rather than one-off demo cuts. You will see exactly where engraving, light plastics, and PCB work fit, and where aluminum or recurring routed parts expose rigidity limits. The article also walks through setup truth, tooling choices, feeds and speeds, and workholding—so you can decide whether this is a bench instrument for supervised jobs or a delay before moving to a production-class platform.
What the 3018 Pro Actually Is
The 3018 Pro is best understood as a refined desktop router, not a scaled-down production machine. That distinction matters more than the name suggests. The “Pro” suffix implies a category change, but the machine still behaves like a close-attention bench tool. Buyers who expect calm, repeatable throughput from a machine in this class are usually disappointed; buyers who treat it as a capable, hands-on workshop instrument tend to get real value from it.
The practical question is not “what can it cut once?” It is “what can it cut or engrave repeatedly, with acceptable effort and without turning every job into a recovery exercise?”
Where the 3018 Pro Fits Naturally
This machine performs best when the work is small, the cutting load is modest, and the operator stays involved. Typical good-fit applications include:
- Small wood engraving and light profile work
- Simple plastics or acrylic jobs run conservatively
- PCB-style experiments and tiny technical parts
- Prototype geometry checks
- Small internal fixtures, templates, and bench accessories
These jobs work because they do not demand structural reserve the machine does not have. The 3018 Pro rewards patience and setup discipline, and it punishes operators who try to push it beyond its intended envelope.
A Capability Table That Reflects Reality
A generic material list overstates what this machine can do. A more honest reading is a fit assessment by operation type:
| Operation or Material | Typical Fit | Why It Can Work | What Usually Sets the Limit |
|---|---|---|---|
| Shallow engraving in wood or MDF | Good | Low cutting force and clear visual feedback | Zeroing, spoilboard truth, and tool sharpness |
| Light plastic or acrylic work | Fair | Small parts and careful paths can be manageable | Heat, chip clearing, and edge quality |
| PCB-style or small technical work | Good | Small format rewards bench control and patience | Flatness and restart discipline |
| Small internal fixtures and templates | Fair to good | Useful when cycle time is not the main value | Setup time can overtake part value |
| Aluminum or harder materials | Narrow and weak | Possible in limited cases | Rigidity, finish stability, and supervision burden |
This table reflects the machine’s true character. It handles a narrow slice of many materials, not a broad range of them. The difference matters when you are planning production work rather than one-off experiments.
Engraving Is the Machine’s Strongest Role
For most owners, engraving is where the 3018 Pro stays useful longest. Text, logos, outline details, nameplates, coordinate marks, and decorative V-bit work place less sustained demand on the machine than heavier routing. The spindle and frame can maintain acceptable accuracy at shallow depths without being pushed toward their structural limits.
That does not mean engraving is effortless. It still depends on:
- Clean zeroing
- Trustworthy surface flatness
- Stable tool presentation
- Careful depth control
But it does mean the machine can deliver genuine bench value without being forced into heavier removal work where its limitations appear quickly. Operators who respect this boundary tend to get years of useful service from the machine.
It is also worth remembering that router engraving and laser engraving are different workflows. If the real need is non-contact graphic marking rather than carved detail, it helps to compare router and laser workflow fit directly instead of trying to force one machine to represent both processes equally well.
Read “Can Cut” as “Can Repeat Calmly”
This is the most important filter when evaluating a 3018 Pro. A material is not a good fit just because the cutter can enter it. A material becomes a good fit when the machine can produce acceptable results without turning every run into a closely watched recovery exercise.
Two owners can discuss the same material and sound like they own different machines. One is judging a single careful sample. The other is judging repeated work after tool changes, cleanup, and setup drift. Both may be telling the truth. They are simply using different standards.
For buying decisions, repeatable calm is the better standard. A machine that can produce one good part under ideal conditions is not the same as a machine that can produce fifty good parts under normal shop conditions.
Upgrades That Usually Improve the Experience
The most useful upgrades are the ones that make the machine’s current role more stable, not the ones that try to turn it into a different class of machine. Common worthwhile upgrades include:
- Better workholding and a more trustworthy spoilboard
- Homing, limit, or probing improvements that reduce restart uncertainty
- Cleaner toolholding or spindle smoothness when runout is the proven problem
- Better cable management, dust handling, or enclosure discipline
These upgrades improve machine truthfulness. They help the machine start more repeatably, hold the part more honestly, or present the tool more consistently. Each one reduces the variables that cause scrap, rework, or operator frustration.
Upgrades That Usually Waste Time or Hope
Owners often get into trouble when upgrades stop refining the machine’s role and start arguing with it. The warning signs are familiar:
- The upgrade story depends on the machine becoming comfortable in work it previously only survived
- The buyer is chasing production calm rather than bench improvement
- Every new accessory is really delaying a machine-class decision
A 3018 Pro can be improved. It is much harder to transform. Buyers should keep asking one blunt question: does this upgrade improve the work I already know belongs here, or does it mainly support a fantasy about what the machine might become?
When the Machine Has Already Taught Its Lesson
There is a normal point where a 3018 Pro stops being a smart compact solution and starts becoming a delay between the buyer and a better-matched machine class. That point usually appears when the work shifts toward:
- Recurring routed parts
- Tighter customer-facing expectations
- Larger job volume
- Lower tolerance for supervision and retesting
At that stage, it is often more useful to compare the workload against a broader desktop CNC capability discussion or the wider Pandaxis machinery lineup than to keep searching for the next accessory bundle. The machine has taught its lesson: it is a capable bench tool, not a production platform.
The Right Way to Judge It
Judge a 3018 Pro by the cleanest repeat part it can make under normal conditions, not by the boldest demo it can produce once. If your real work is engraving, small prototypes, PCB-style experimentation, and modest bench routing with close operator attention, this machine can be a very good fit. If your real need is low-intervention production, “Pro” is not enough to erase the limits of the desktop category.
Setting Up for Success: The First Hour Matters
The difference between a frustrating 3018 Pro experience and a productive one often comes down to how the machine is set up before the first job. A machine that arrives with loose eccentric nuts, a bowed spoilboard, or a spindle that is not square to the table will produce confusing results that look like machine failure but are actually setup failure.
Start by checking the frame for squareness. The 3018 Pro uses a combination of aluminum extrusions and threaded rods. If the gantry is not square to the base, every cut will be slightly skewed, and the error will compound as the tool moves across the work area. A simple machinist’s square and a feeler gauge can confirm whether the gantry sits true. If it does not, loosen the gantry mounting bolts, square it, and retighten.
Next, flatten the spoilboard. Many 3018 Pro units ship with a thin MDF or acrylic spoilboard that is not perfectly flat. Run a surfacing pass with a straight bit across the entire spoilboard to establish a true reference plane. This single step eliminates more engraving depth problems than any other adjustment. If the spoilboard is too thin to surface, replace it with a thicker piece of MDF before doing anything else.
Finally, check the spindle for runout. A collet that is dirty, worn, or not seated properly will cause the tool to wobble, producing rough edges and inconsistent engraving depth. Clean the collet, seat the tool fully, and use a dial indicator to check runout at the tool tip. If runout exceeds a few thousandths of an inch, replace the collet before running any real work.
Tooling Choices That Make or Break the Job
The 3018 Pro is sensitive to tool selection in ways that larger machines are not. Because the frame is light and the spindle is modest, the tool must do the work of maintaining finish quality. A poor tool choice will produce chatter, burning, or broken bits long before the machine’s structural limits are reached.
For engraving in wood and MDF, a V-bit with a 30- to 60-degree included angle is the standard choice. The sharper angle produces finer detail but requires shallower passes. A 60-degree bit is more forgiving and works well for text and logos. For deeper profile cuts, a single-flute straight bit with a small diameter, typically 1/8 inch or 3 mm, clears chips more effectively than a multi-flute bit and reduces heat buildup.
For plastics and acrylic, the rules change. These materials melt rather than cut cleanly, and heat is the enemy. A single-flute bit with a polished flute surface reduces friction and helps evacuate chips. Run the spindle at a moderate speed and take shallow passes, typically no more than 0.5 mm per pass for acrylic. If the material starts to melt or smear, reduce spindle speed, increase feed rate slightly, or both. The goal is to cut chips, not to rub the material into a molten mess.
For PCB work, a dedicated carbide end mill with a 0.8 mm or 1 mm diameter is the standard tool. These bits are brittle and break easily if the depth is set too aggressively. Use a depth of 0.05 to 0.1 mm per pass for copper removal, and always verify the board is flat before starting. A slightly warped PCB will cause the tool to cut deeper in some areas and shallower in others, producing short circuits or broken traces.
Feeds and Speeds: The Practical Numbers
The 3018 Pro does not have the rigidity to run aggressive feeds and speeds, but it also does not need to. The machine’s value is in precision, not speed. Running the machine too fast is the most common cause of broken bits, burned material, and poor finish quality.
For wood engraving with a V-bit, a spindle speed of 8,000 to 10,000 RPM and a feed rate of 300 to 500 mm/min is a reasonable starting point. Adjust from there based on the material and the depth of cut. If the bit chatters, reduce feed rate or increase spindle speed. If the wood burns, increase feed rate or reduce spindle speed.
For plastic and acrylic, spindle speed should be lower, typically 6,000 to 8,000 RPM, with a feed rate of 200 to 400 mm/min. The slower spindle speed reduces heat generation, and the moderate feed rate keeps the tool cutting rather than rubbing. If the material melts, reduce spindle speed and increase feed rate slightly.
For PCB work, spindle speed can be higher, around 10,000 to 12,000 RPM, with a feed rate of 100 to 200 mm/min. The high spindle speed helps the small bit cut cleanly, and the slow feed rate prevents the bit from deflecting or breaking. Always use a depth of no more than 0.1 mm per pass for copper removal.
These numbers are starting points, not fixed values. Every machine has slight variations in rigidity, spindle quality, and alignment. The operator’s job is to start conservative, observe the results, and adjust incrementally. A machine that is cutting cleanly should produce consistent chips, not dust, and the tool should not make a high-pitched squeal or a dull thud.
Workholding: The Hidden Variable
The 3018 Pro’s small work area makes workholding seem simple, but it is often the source of the most frustrating failures. A part that moves even a fraction of a millimeter during a cut will ruin the job, and the operator may not notice until the cut is complete.
Double-sided tape is the most common workholding method for small parts. It works well for flat, lightweight materials like PCB blanks, thin acrylic, and small wood pieces. The key is to use enough tape to hold the part firmly without creating a gap between the part and the spoilboard. Press the part down firmly and check for any rocking or movement before starting.
Mechanical clamps are better for larger or heavier parts, but they take up space and can interfere with the tool path. If using clamps, position them so they do not collide with the spindle or the tool. It is also worth checking that the clamp pressure does not distort the part. A thin piece of acrylic can bow under clamp pressure, causing the tool to cut unevenly.
For repeated jobs, a dedicated fixture plate is the best investment. A simple plate with threaded inserts or T-slots allows the operator to mount parts in the same position every time, reducing setup time and improving consistency. This is especially valuable for small production runs where the same part is made repeatedly.
Dust and Chip Management
The 3018 Pro is a small machine, but it can still generate a surprising amount of dust and chips. Without proper management, debris accumulates on the spoilboard, clogs the tool, and obscures the work area. It also gets into the lead screws and linear bearings, accelerating wear and reducing accuracy over time.
A simple shop vacuum with a small nozzle is often sufficient for light work. Position the nozzle near the cutting area to capture chips as they are produced. For heavier work, a dust shoe that surrounds the spindle and connects to a vacuum is a worthwhile upgrade. It keeps the cutting area clear and reduces the amount of debris that settles on the machine.
Chip clearing is especially important for plastics and acrylic. If chips are not evacuated, they can melt and weld themselves to the tool or the workpiece, ruining the finish. A blast of compressed air directed at the cutting area can help, but it also blows debris around the shop. A vacuum is the cleaner solution.
Software and Workflow: From CAD to Finished Part
The 3018 Pro is typically controlled by open-source software like GRBL, and the workflow from design to finished part is straightforward but requires attention to detail. The operator must move the design through three stages: CAD, CAM, and control.
In the CAD stage, the part geometry is created. For engraving, this usually means importing a vector file like an SVG or DXF. For routing, it means drawing the part outline and any internal features. The key is to ensure the design is clean, with no duplicate lines, open paths, or overlapping geometry that will confuse the CAM software.
In the CAM stage, the tool paths are generated. The operator selects the tool, sets the depth of cut, and defines the cutting strategy. For engraving, a single pass at a fixed depth is usually sufficient. For routing, multiple passes may be needed to reach the final depth without overloading the tool. The CAM software also generates the G-code that the machine will execute.
In the control stage, the G-code is loaded into the GRBL controller, and the machine is zeroed. Zeroing is the most critical step. The operator must set the X, Y, and Z axes to the correct reference point, usually the bottom-left corner of the work area and the top surface of the material. A mistake here will shift the entire job or cause the tool to plunge too deep.
A touch probe is a worthwhile upgrade for zeroing. It automates the Z-axis zeroing process, reducing the risk of a crash and improving repeatability. Without a probe, the operator must use a piece of paper or a feeler gauge to set the Z zero, which is less accurate and more time-consuming.
Common Failure Modes and How to Diagnose Them
Even with careful setup, the 3018 Pro will occasionally produce bad parts. The key is to diagnose the cause quickly and correct it before running another job. The most common failure modes are:
- Inconsistent engraving depth: This is almost always caused by an uneven spoilboard or a part that is not flat. Surface the spoilboard and check the part for flatness before running the job.
- Rough edges or chatter: This is usually caused by a dull tool, excessive feed rate, or insufficient spindle speed. Replace the tool and adjust the feeds and speeds.
- Broken bits: This is typically caused by too aggressive a depth of cut, a feed rate that is too high, or a tool that is too small for the job. Reduce the depth of cut and feed rate.
- Burned material: This is caused by too much heat, usually from a spindle speed that is too high or a feed rate that is too slow. Reduce spindle speed or increase feed rate.
- Lost steps or skipped motion: This is caused by a mechanical binding or a controller issue. Check the lead screws and linear bearings for debris or damage, and verify the GRBL settings are correct.
Comparing the 3018 Pro to Other Desktop CNC Options
The 3018 Pro is not the only desktop CNC machine on the market, and it is worth understanding how it compares to other options before making a purchase decision. The main alternatives are larger desktop routers, laser engravers, and entry-level production machines.
Larger desktop routers, such as those with a 500 by 500 mm work area or more, offer more rigidity and a larger cutting envelope. They can handle heavier cuts and larger parts, but they also cost more and take up more bench space. If the work is primarily small engraving and light routing, the 3018 Pro is often sufficient. If the work involves larger parts or heavier cuts, a larger machine is worth the investment.
Laser engravers are a different tool entirely. They use a focused beam of light to mark or cut materials, and they excel at graphic marking, fine detail, and non-contact work. They cannot produce the carved depth of a router, and they are limited to materials that absorb the laser wavelength. If the work is primarily graphic marking, a laser engraver may be a better fit. If the work involves carved detail or cutting through material, a router is the right choice.
Entry-level production machines, such as a small nesting machine or a compact CNC router from a commercial manufacturer, offer the rigidity and repeatability needed for low-volume production. They cost significantly more than a 3018 Pro, but they can run for hours without supervision and produce consistent parts. If the work has moved past the prototype stage and into recurring production, this is the category to consider.
Use the Upgrade Budget Where It Changes the Workflow
The useful upgrades are the ones that improve work the 3018 Pro already handles: a square frame, a flat spoilboard, clean tooling, and repeatable workholding. Once the workload becomes recurring production or requires less supervision, compare the cost of accessories with the cost of moving to a stiffer machine class.
That comparison keeps the budget tied to the next production problem. Spend on setup quality when the machine is still a good fit; move up when the work itself has outgrown the desktop envelope.