Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
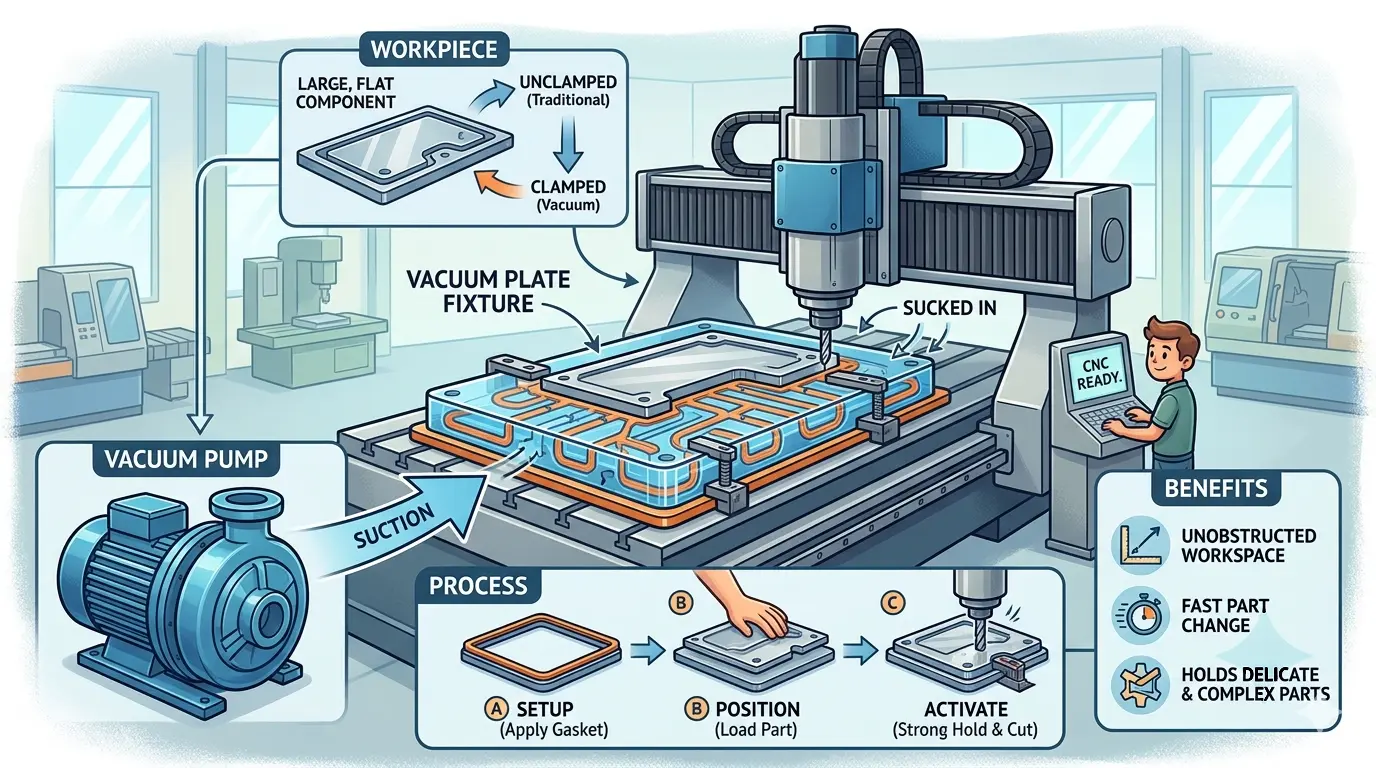
Mechanical clamps quietly tax every cycle through placement, adjustment, and verification, while their presence inside the machining envelope forces programmers to leave no-cut zones that restrict tool access. A CNC vacuum plate fixture replaces that handling friction with a sealed-zone system that holds parts by atmospheric pressure, but the real decision hinges on whether your part family maintains enough sealed area after cutouts break through and profiles lighten mid-cycle. Before you compare pump sizes or plate thicknesses, evaluate leakage behavior, material porosity, and toolpath sequencing together—because a fixture that feels solid at startup can lose its holding margin exactly when the spindle needs it most.
Why Shops Move Away From Clamps
Mechanical clamps get the job done, but they come with a cost that shows up in every cycle. Each clamp has to be placed, adjusted, and verified before the spindle can run. On a busy nesting or panel-processing schedule, that handling time adds up across dozens of parts per shift. Clamps also sit inside the machining envelope, which means the programmer either works around them or leaves no-cut zones that reduce tool access and slow down the cycle.
A CNC vacuum plate fixture removes much of that friction. Instead of positioning hardware around each blank, the operator places the workpiece on the plate, activates the vacuum zone, and starts the cycle. The top surface stays open to the cutter, setup time drops, and repeat jobs become noticeably more consistent. That is the practical appeal: faster workholding and better tool access, not a theoretical improvement in holding force.
How a Vacuum Plate Fixture Actually Works
The operating principle is straightforward. The fixture plate connects to a vacuum pump or central vacuum source through internal ports and channels. When the workpiece covers a sealed or gasketed area, the pump evacuates the air between the part and the plate. Atmospheric pressure then presses the workpiece down against the fixture surface. The holding force is the difference between atmospheric pressure and the reduced pressure inside the sealed zone, multiplied by the effective sealed area.
That description makes the system sound simple, and in principle it is. In practice, every vacuum fixture is managing two competing factors at the same time:
- The holding force available at the part surface.
- The air leakage the pump must overcome while the job is running.
When the sealed area is solid and leakage stays low, the fixture feels fast and dependable. When leakage climbs or the contact condition weakens, the same plate can become unstable at the worst possible moment. A useful way to think about it: a vacuum fixture does not succeed because it has suction. It succeeds because it maintains enough sealed area for the entire toolpath to finish safely.
Which Parts Favor Vacuum Workholding
Vacuum plate fixtures perform best on parts that offer broad, reasonably flat contact area and where the shop benefits from faster loading than clamp-based setups allow. That description covers a large share of woodworking production: sheet goods, flat panel routing, nested cabinet parts, and recurring part families where a dedicated fixture design can pay for itself quickly.
The method is especially valuable when clamps would obstruct the cutter path or when changeover speed directly affects throughput. In those situations, vacuum fixturing improves access while cutting handling time.
But vacuum is not a universal solution. Parts that are very small, highly porous, noticeably warped, or aggressively opened by the cut may require different zoning, additional support, pods, tabs, onion-skin strategies, or hybrid workholding. Vacuum is a workholding method with clear strengths and clear boundaries, not a guarantee for every geometry.
The Holding Picture Changes Mid-Cycle
One of the most common mistakes buyers make is judging a vacuum fixture by its starting condition. At the beginning of a job, the raw blank covers the fixture well, the sealed area is large, and hold-down feels strong. That initial test can be misleading.
As the toolpath progresses, the situation changes. Internal cutouts break through and open air paths. Outer profiles get lighter as material is removed. Scrap areas release and lift away from the plate. Each of these events alters the leakage picture and reduces the effective sealed area. The fixture that felt rock-solid with the blank in place may lose its holding margin halfway through the cycle.
This is why vacuum fixtures should be evaluated dynamically rather than statically. The real question is not whether the part holds before cutting starts. It is whether the part stays held after the first pocket breaks through, after the profile gets lighter, and after multiple parts are nearly separated from the sheet. Shops that skip this evaluation often blame the pump or the plate for a problem that was actually a fixture-design or toolpath-sequencing issue.
Dedicated Plates, General Tables, and Pods Solve Different Problems
Not every vacuum-based workholding setup addresses the same production challenge. Buyers often ask about vacuum fixturing as if it were one product category, but the design direction depends heavily on the job mix.
| Vacuum Workholding Direction | What It Usually Fits Best | What It Usually Gives Up |
|---|---|---|
| Dedicated vacuum plate fixture | Repeat work on one part family or a stable pattern | Flexibility across changing job mixes |
| General vacuum table | Broader sheet handling and more flexible routing | Specialization for one exact part geometry |
| Vacuum pods or smaller zones | Localized hold-down on shaped or partially supported work | More setup complexity and slower loading |
| Hybrid vacuum plus mechanical support | Jobs that need both open access and a security margin | More fixture planning and operator discipline |
A dedicated plate is not simply a stronger version of a generic table. It is a specialized decision built around repeatability and loading speed on a narrower range of work. General tables trade that specialization for flexibility across changing jobs. Understanding which direction fits your production mix matters more than comparing pump sizes or plate thicknesses.
Material Behavior Often Decides the Outcome
The fixture does not create hold-down in isolation. The workpiece material plays a major role in whether vacuum fixturing is realistic at all. Risk rises when the job includes any of the following conditions:
- Porous material that leaks air through the body of the part.
- Thin or warped parts that do not sit flat on the fixture surface.
- Very small parts with limited contact area for vacuum force.
- Narrow parts with low resistance to side load from the cutter.
- Geometries that open air paths early in the machining cycle.
This is why two jobs on the same fixture can behave completely differently. The plate did not change. The part family changed. A vacuum fixture that works beautifully on one panel geometry may be marginal on another because the effective holding area and leakage path are no longer comparable. Vacuum fixturing always starts as a part-behavior question, not just a pump-sizing question.
Zoning and Sealing Strategy Determine Reliability
Many vacuum problems that get blamed on weak pumps are actually zoning or sealing problems. If the fixture does not isolate the active vacuum area properly, the pump spends too much of its capacity fighting leakage outside the part instead of holding the part itself.
Good fixture design pays close attention to several details:
- How the active vacuum area is defined for each part placement.
- How zones are separated from unused regions of the plate.
- Where ports are located relative to the part geometry.
- How gasket or sealing paths are maintained over time.
- How quickly air pathways open when cutouts break through.
A vacuum fixture is not a solid object with magical holding ability. It is a controlled leak-management system. When the sealing logic is sound, the fixture feels stable and repeatable. When the sealing logic is weak, the fixture feels unpredictable even if the plate looks beautifully machined.
Programming and Fixture Design Belong in the Same Conversation
Vacuum fixturing works best when the CAM program respects the fixture logic. Cut order, tab strategy, onion-skin depth, and the timing of through-cuts all affect how well the part stays held during the cycle.
If the program opens leakage paths too early or creates side load on a part whose holding margin is already shrinking, the fixture gets blamed for a problem that actually started in the toolpath strategy. Shops that succeed with vacuum fixtures review programming and workholding together rather than treating them as separate concerns.
This is also why vacuum plate fixtures are stronger in repeat work than in completely unpredictable one-off jobs. Once the fixture and the program are built around each other, the method becomes fast and stable. Without that coordination, the shop may have suction but not reliable process control.
Hybrid Workholding Is Often the Right Answer
Some buyers assume that if vacuum alone does not hold every part securely, then vacuum fixturing itself must be the wrong approach. That conclusion is too simplistic for real production conditions.
In practice, hybrid workholding frequently delivers the best result. Vacuum provides most of the speed and accessibility benefit, while small locating features, backup supports, tabs, onion skins, or limited mechanical restraints protect the few parts or moments in the cycle that need extra security. This combination is not a compromise. It is a recognition that the goal is stable production, not ideological purity about workholding methods.
If vacuum handles most of the job well but one risky geometry or final profile needs additional help, that does not disqualify the method. It simply means the workholding strategy needs to match the actual part behavior rather than the shop’s preferred theory.
Maintenance Requirements Are Easy to Underestimate
Because vacuum plate fixtures are often machined from solid material and look substantial, buyers can underestimate how much sealing condition matters. The plate may be beautifully made and still perform poorly if channels are damaged, ports are blocked, the top surface is no longer flat enough for the job, or gasketed areas are worn.
Vacuum fixturing should not be treated as a one-time capital investment that never needs attention. The fixture surface, sealing paths, and connected plumbing all need to stay honest if the hold-down strategy is expected to remain honest. This is especially true on high-repeat work where the same zones carry the same loading pattern continuously. Wear tends to localize in those areas. Once that happens, the fixture may keep running while its real holding margin falls quietly in the background.
Economics Depend on Repeatability, Not Hardware Cost
Dedicated vacuum plate fixtures can look expensive if judged only as pieces of machined hardware. The more useful question is how much time and variability they remove from the process. They tend to pay off fastest when:
- The same or similar parts repeat frequently.
- Setup speed matters more than maximum flexibility.
- Clamp placement is slowing the process.
- Tool access is constrained by conventional workholding.
- Part quality improves when the work area stays cleaner and more repeatable.
They tend to be weaker investments when jobs change constantly, part families vary too widely, or the process still depends heavily on programming and operator improvisation that a dedicated fixture cannot stabilize. The economic test is not whether the plate is expensive. It is whether the fixture removes enough setup time, handling, and inconsistency to justify its specialization.
Evaluating Used Vacuum Fixtures
Used vacuum plates and legacy fixtures deserve closer inspection than many buyers give them. Surface flatness, channel condition, sealing wear, blocked ports, rough repairs, and unknown prior part families can all reduce performance sharply. A fixture that held one product well under one operator does not automatically translate into reliable hold-down for a different mix of parts in another shop.
Useful checks before purchasing used vacuum fixturing include:
- Surface flatness at the real contact zones.
- Condition of channels, ports, and connection points.
- Signs of repeated rework or makeshift sealing fixes.
- Evidence that the fixture was built around one narrow historical part family.
- Whether the current part mix really matches the old fixture logic.
Leakage behavior and actual part compatibility matter more than how substantial the plate looks at first glance.
Questions to Answer Before Approving a Fixture Concept
| Question | Why It Matters |
|---|---|
| What material is being held? | Porosity and flatness directly affect usable vacuum force |
| Does the part remain sealed through the critical parts of the cut? | Determines whether hold-down stays stable mid-cycle |
| Is this a repeat fixture for one part family or a more flexible setup? | Changes the economics and design direction |
| Is programming being developed alongside fixture logic? | Prevents toolpath decisions from undermining hold-down |
| What backup plan exists for marginal parts? | Avoids preventable scrap when vacuum alone is not enough |
These questions separate vacuum as a production advantage from vacuum as an ongoing troubleshooting topic.
Where Vacuum Fixturing Fits in a Woodworking Workflow
Vacuum strategy sits close to many woodworking CNC and nesting workflows. A vacuum plate fixture is one expression of the broader workholding goal: hold the part securely, keep the toolpath open, and reduce setup handling without turning the cutting area into a clamp-management problem. For shops weighing the process impact of nesting-style production, the same hold-down logic applies whether the machine is a general router or a dedicated nesting center. The fixture, the material, and the program all need to agree for the method to deliver its full benefit.
Judging Vacuum Fixturing as a Process System
A CNC vacuum plate fixture is a vacuum-based workholding system that uses ports, channels, and often sealing zones to hold parts against a fixture plate or table. Its biggest strengths are faster setup, cleaner tool access, and stronger repeatability on suitable jobs. Its biggest limits are leakage sensitivity, part-geometry sensitivity, and the way through-cuts change hold-down conditions while the cycle is running.
That is why vacuum fixturing should be judged as a process system rather than as a piece of hardware. The fixture design, the material, the sealing condition, the programming sequence, and the backup strategy all decide whether the method works well in production. When those pieces match, a vacuum plate fixture can be one of the most efficient workholding methods on the shop floor. When they do not, the same fixture becomes an ongoing source of instability. Buyers who evaluate the whole process instead of expecting the pump alone to make the system work make better decisions and avoid costly trial-and-error on the production floor.