Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
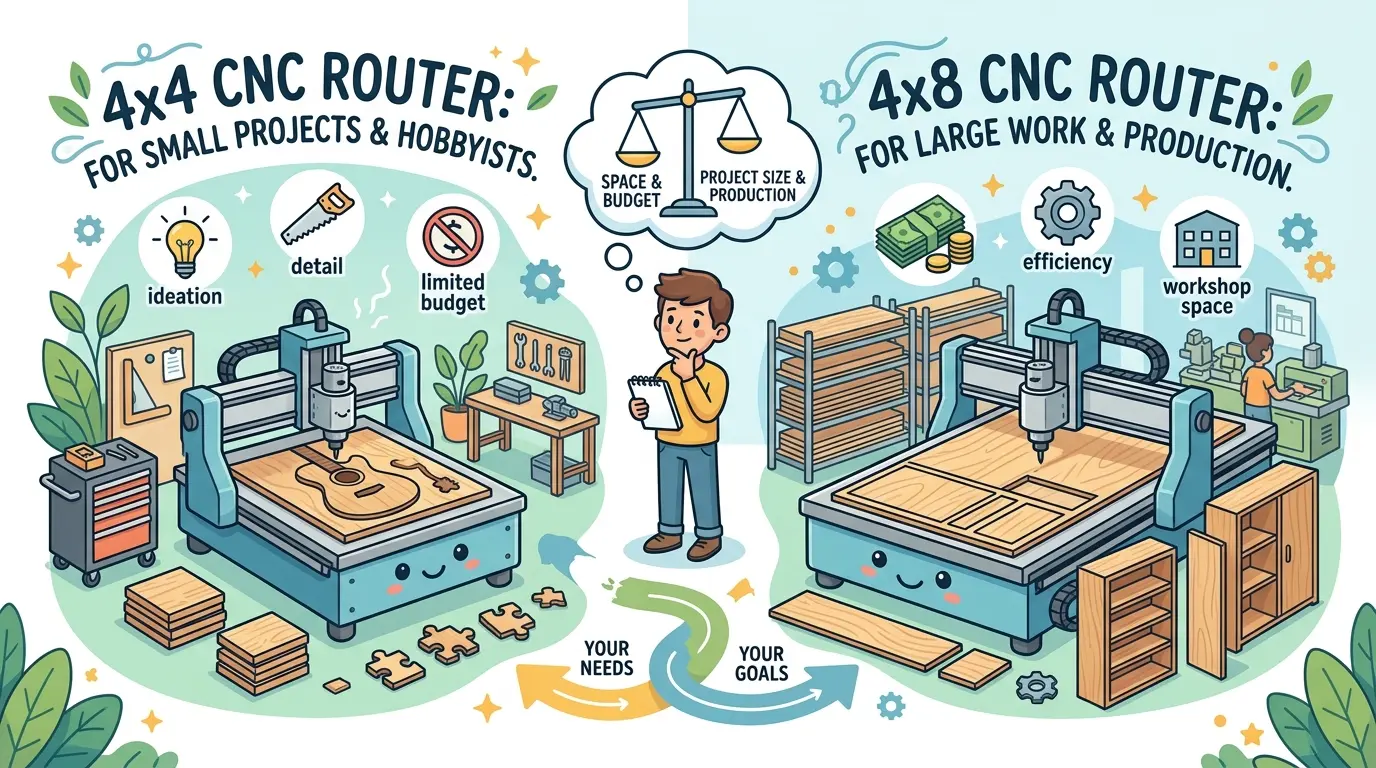
Choosing between a 4×4 and a 4×8 CNC router is not a table-dimension question; it is a material-flow decision that determines how many times an operator touches each panel before the spindle cuts. Buyers who start by measuring finished parts instead of raw stock risk paying for unused capacity or absorbing weekly breakdown labor that a larger bed would eliminate. This article walks through the real variables—sheet entry patterns, nesting density, handling equipment, ergonomics, and downstream part flow—so you can score both formats against your actual production history before committing capital.
Bed Size Is a Material-Flow Decision, Not a Capability Decision
Choosing between a 4×4 and a 4×8 CNC router looks like a simple question of table dimensions. In practice, it is a decision about how material moves through your shop, how many times an operator touches each panel, and where labor gets spent before the spindle ever starts cutting.
The real question is not which machine sounds more capable on paper. It is which bed size removes more recurring labor from the workflow your shop already runs. Getting this wrong means paying for capacity you do not use, or spending hours every week breaking down sheets to fit a table that is too small.
Start With Raw Stock, Not Finished Part Size
Most buyers begin by measuring their largest finished part. That is the wrong starting point. The more revealing variable is how material enters the cell.
If your profitable jobs begin as full 4×8 sheets, a 4×8 bed usually matches the route more naturally. If your shop already works from smaller blanks, cut-to-size stock, prototypes, templates, or compact custom pieces, a 4×4 bed may fit better even when some finished parts are not small.
Before comparing machine specifications, answer these five questions:
- How often does the shop start from full-sheet stock?
- How often is stock pre-cut before it reaches the router?
- How much operator time is spent on breakdown before routing?
- How often do recurring jobs actually use the full nesting area?
- Does the work mix stay sheet-driven and repetitive, or does it change constantly?
Those answers will reveal the correct bed size faster than any generic planning about future growth. If you cannot answer them from production history, spend a week tracking material flow before you commit to a purchase.
What a 4×4 Router Usually Does Better
A 4×4 router typically wins on control, access, and compact cell management. That matters in specific production conditions:
- One operator manages the whole cell. A smaller table means shorter reach, easier part retrieval, and less walking per cycle.
- The shop wins work through fast changeovers and mixed orders. Smaller blanks load faster, and the operator can stage the next job without a forklift.
- Material often arrives already broken down or naturally compact. If your supplier delivers cut-to-size blanks, a 4×8 table is mostly unused surface.
- Floor space is tight. The machine footprint is only part of the story, but a 4×4 cell demands less surrounding room for staging and access.
- The work mix includes prototypes, signs, displays, fixtures, and short-run custom parts. These jobs change constantly, and a smaller bed makes each changeover faster and less physically demanding.
In those conditions, a 4×4 is not simply the cheaper version of a bigger machine. It is often the bed that fits the operator and the actual work more honestly. The machine is easier to load, easier to supervise, and easier to keep productive through a day of mixed orders.
What a 4×8 Router Usually Removes
A 4×8 router earns its place by removing avoidable handling from sheet-based work. That matters most when:
- Standard panels arrive as the natural raw format. If you buy 4×8 sheets and your router cannot accept them whole, someone is cutting them down before every job.
- The shop repeatedly loses time cutting sheets down before routing. That pre-cutting step adds labor, creates an extra material handling stage, and introduces dimensional error that carries into the routed parts.
- Routing is part of a structured cabinet, wardrobe, or furniture workflow. In a connected line, the router should accept what the upstream process delivers, not force a format change.
- Keeping sheet registration intact longer helps the next steps. A full sheet holds its reference edge. Once you break it down, every smaller blank needs its own setup and alignment.
- The shop can support the larger cell without congestion. A 4×8 machine needs staging space, unload space, and clear access for sheet handling equipment.
In these cases, the bigger bed is not mainly about cutting bigger parts. It is about touching the material fewer times before the cut. Every time a panel is handled without cutting, you are paying labor that adds no value.
Touches Matter More Than Travel Numbers
The shop-floor result is usually decided by touches, not by headline travel speeds or spindle power. A touch is any time an operator handles material: unloading a sheet from a truck, moving it to a breakdown saw, cutting it to size, stacking the blanks, moving them to the router, loading the table, and repositioning parts.
If a smaller bed forces extra breakdown, extra repositioning, or extra sorting, those touches can quietly outweigh the savings of the lower machine price. A shop that runs 20 sheets per day through a 4×4 router may spend 30 to 45 extra minutes per day on breakdown and staging compared to running the same sheets whole on a 4×8. Over a 250-day production year, that is 125 to 190 hours of labor spent on handling that a larger bed would eliminate.
Conversely, if a larger bed forces awkward loading, longer walking, and more surrounding floor pressure for work that rarely needs full-sheet handling, then the bigger bed is carrying overhead the shop never converts into value. A 4×8 machine running mostly small blanks still requires the operator to reach across a large table, manage a bigger dust collection footprint, and keep more surface clear.
How Nesting Density Changes the Math
Nesting software changes how you should evaluate bed size because it changes how much material fits on a single load. A 4×8 sheet can hold roughly twice the surface area of a 4×4 sheet, but the practical gain depends on part geometry and how tightly the software packs parts together.
For cabinet parts, the difference is often substantial. A typical cabinet job produces a mix of large panels, narrow stretchers, and small gussets. On a 4×8 bed, the nesting software can arrange those parts across the full sheet, placing small parts in the gaps between large ones. On a 4×4 bed, the same job may require two or more loads, and the software cannot always preserve the same nesting efficiency because the smaller area limits how parts can be rotated and interlocked.
For sign shops and display fabricators, the math is different. Many jobs are one-off pieces with irregular shapes. A 4×4 bed can handle most of those pieces individually, and the operator can load a new blank for each job without worrying about sheet optimization. The nesting efficiency gain from a 4×8 bed matters less when every job is unique and the operator is already changing tools and programs frequently.
For shops that do both sheet-based cabinet work and custom one-offs, the decision becomes a question of which work pays the bills. If 70 percent of revenue comes from cabinet jobs that start as full sheets, the 4×8 bed pays for itself through nesting efficiency and reduced handling. If 70 percent comes from custom pieces that arrive as individual blanks, the 4×4 bed may be the more honest fit.
Material Handling Equipment Changes the Equation
The bed size decision also depends on what material handling equipment you already own or are willing to buy. A shop with a panel saw and a forklift can break down sheets efficiently before routing. A shop without that equipment will spend more labor forcing full sheets through a smaller bed.
Consider the workflow for a 4×4 router in a shop that receives full 4×8 sheets. The operator must move each sheet to a saw, cut it into quarters or custom blanks, stack the blanks, and move them to the router. That process adds at least one extra material handling stage per sheet. If the shop runs 20 sheets per day, that is 20 extra handling events, each requiring physical labor and floor space for staging.
A shop with a 4×8 router can skip the breakdown step entirely. The operator moves the full sheet directly from the delivery truck or storage rack to the router table, clamps it down, and starts the program. The sheet stays intact through the entire routing process, and the nested parts come off the table already cut. The labor savings are not theoretical; they are measured in minutes per sheet, which compound over a production day.
However, a 4×8 router requires more surrounding infrastructure. The machine needs a clear path for sheet movement, a staging area for incoming and outgoing material, and enough room for the operator to walk around the table. A shop with tight floor space may find that a 4×4 router fits the available area better, even if it means accepting the breakdown labor.
Operator Ergonomics and Fatigue
The physical demands of loading and unloading a CNC router are easy to underestimate until you have watched an operator work through a full shift. A 4×4 table allows the operator to reach most of the surface without stretching or walking around the machine. Parts can be lifted off the table with minimal bending, and the operator can inspect the cut quality from a comfortable position.
A 4×8 table changes the ergonomics significantly. The operator must walk around the machine to reach parts on the far side, bend across the table to retrieve small pieces, and manage a larger working area. Over an eight-hour shift, those extra movements add up. Fatigue reduces attention to detail, which increases the risk of missed defects, misaligned parts, or safety incidents.
For shops with a single operator running the router all day, the ergonomic difference can be decisive. A 4×4 bed keeps the operator closer to the work and reduces the physical strain of each cycle. For shops with two operators or a dedicated material handler, the 4×8 bed becomes more practical because the loading and unloading work can be shared.
The material weight also matters. A full 4×8 sheet of 3/4-inch MDF weighs roughly 70 to 80 pounds, depending on density. Lifting and positioning that sheet on a 4×8 table requires either a second person, a vacuum lifter, or a roller table. A 4×4 blank of the same material weighs roughly half as much, which makes manual loading more feasible for a single operator.
Downstream Operations and Part Flow
The router does not end the process. Parts still have to move to drilling, edging, sanding, assembly, finishing, or packing. Bed size affects how smoothly those downstream steps run.
In some shops, a 4×4 supports a compact one-operator cell where parts are easy to inspect, sort, and transfer to the next station. The operator can reach every part without moving around the machine, which makes quality checks faster and reduces the chance of mixed parts in a batch.
In others, a 4×8 supports cleaner panel flow because routing is only one stage inside a broader line. The real goal is to avoid extra handling before downstream work begins. A full sheet that comes off the router with all its parts nested keeps the relationship between parts intact. That makes sorting, labeling, and kit assembly more straightforward.
Consider a cabinet shop that routes all its parts on a 4×8 bed. When the program finishes, the operator can see the entire sheet layout at once. Parts for the upper cabinets are on one side, parts for the lower cabinets on the other. The operator can label and sort them into kits before moving them to the edgebander. That visual organization is harder to achieve on a 4×4 bed, where parts come off in smaller batches and the operator must track which load belongs to which job.
For a sign shop, the downstream flow is different. Routed letters and shapes are often individual pieces that go straight to finishing or installation. A 4×4 bed produces those pieces in manageable batches, and the operator can inspect each piece as it comes off the table. The smaller bed actually supports the one-piece-at-a-time workflow better than a larger bed would.
Floor Space Must Be Judged As Working Space
Many buyers know the machine footprint from the spec sheet. Fewer know the real cell footprint, which is what actually matters on the shop floor.
The router also needs:
- Material staging room. Sheets or blanks need a place to sit before loading, and finished parts need a place to go after unloading.
- Approach and unload space. The operator needs room to move around the table, reach the far side, and handle parts without straining.
- Tool-change access. The spindle and tool magazine need clearance for maintenance and tool changes.
- Dust collection routing. Ductwork takes space and may need to run overhead or along walls.
- Safe walking lanes. Material handling equipment and foot traffic need clear paths that do not cross the machine’s operating zone.
A 4×8 can easily need far more practical operating space than the machine dimensions alone suggest. That does not make it wrong. It means the shop must judge working space, not just table size. Measure the actual area you can dedicate to the cell, including staging and access, before you decide.
Dust Collection and Airflow Considerations
Bed size also affects dust collection requirements. A 4×8 router has a larger cutting area, which means more surface area generating chips and dust during routing. The dust collection system must handle a higher volume of airborne particles, and the ductwork must be sized accordingly.
A 4×4 router generates less dust per cycle, but the dust is concentrated in a smaller area. The collection hood and vacuum system can be more compact, which simplifies installation and reduces the load on the shop’s central dust collection system.
For shops with an existing dust collection system, the bed size decision should include a check of whether the current system can handle the additional load. A 4×8 router may require a larger collector, additional duct runs, or a more powerful vacuum table. Those costs should be included in the total ownership calculation.
Tooling and Spindle Load Patterns
The bed size also influences how the spindle is loaded during cutting. A 4×8 router can cut a full sheet with many parts nested together, which means the spindle may be cutting continuously for longer periods. That sustained load affects tool wear, spindle temperature, and the need for automatic tool changers.
A 4×4 router typically cuts smaller batches, which means more frequent starts and stops. The spindle cycles more often, and the operator has more opportunities to change tools between jobs. For shops that use a variety of tooling for different materials, the 4×4 bed can actually be easier to manage because tool changes happen naturally between loads.
However, a 4×8 router with an automatic tool changer can handle the sustained cutting load more efficiently. The machine can switch between roughing and finishing tools without operator intervention, which keeps the spindle cutting and reduces cycle time. For high-volume sheet work, that automation advantage can offset the larger bed’s ergonomic drawbacks.
Software and Programming Differences
The bed size also affects how you program and nest parts. Nesting software for a 4×8 bed can optimize the full sheet, arranging parts to minimize waste and reduce cutting time. The software can also account for grain direction, edge banding requirements, and part orientation.
For a 4×4 bed, the nesting software must work with a smaller area. That often means splitting a job into multiple nests, which can reduce nesting efficiency and increase the number of tool changes. The software may also need to handle more complex part placement to fit everything into the smaller area.
Shops that already use nesting software should test both bed sizes with their actual job files. The software can generate a report showing material utilization and estimated cutting time for each bed size. That data is more reliable than guessing based on part dimensions alone.
Failure Modes to Screen Before Buying 4×4 CNC Router vs 4×8 CNC Router
The most common mistakes in this decision are straightforward and avoidable:
- Buying 4×8 because it feels safer even when the current work rarely uses the full table. A larger bed that sits half-empty still costs more, takes more floor space, and demands more effort to load.
- Buying 4×4 because the entry price is easier to approve while ignoring the weekly labor cost of panel breakdown. The price difference can disappear in a few months of extra handling labor.
- Comparing ideal sample nests instead of real production history. A perfectly nested 4×8 sheet looks impressive, but if your jobs rarely fill the table, that efficiency is theoretical.
- Assuming growth always means a bigger bed, when the real need may be cleaner upstream sizing or a more connected line. Sometimes the answer is better breakdown equipment, not a larger router.
- Ignoring the cost of auxiliary equipment. A 4×8 router may require a vacuum pump with higher flow, a larger dust collector, or a sheet feeder to reach its full potential. Those costs add up quickly.
- Forgetting about maintenance access. A larger machine needs more clearance for servicing the spindle, linear guides, and drive systems. If the machine is wedged into a tight corner, routine maintenance becomes a major project.
In some shops, even upstream equipment such as panel saws can be part of the better answer if the actual problem is where breakdown should happen. If your material flow is inefficient, the fix may be at the receiving end, not at the router.
Cost of Ownership Beyond the Purchase Price
The purchase price is only the first number in a long equation. A 4×8 router costs more upfront, but it may also cost more to operate. The larger table requires more vacuum pressure to hold sheets in place, which means a larger vacuum pump and higher energy consumption. The dust collection system must handle more airflow, which increases filter maintenance and replacement costs.
The floor space for a 4×8 cell is also more expensive. In a crowded shop, every square foot has a value. A 4×8 router plus its staging and access areas can easily occupy 200 to 300 square feet. A 4×4 cell might need half that. If your shop is paying rent or mortgage on that space, the larger machine carries a monthly cost that never appears on the invoice.
On the other hand, a 4×4 router that forces daily breakdown labor carries a recurring cost that is easy to ignore. If an operator spends 30 minutes per day cutting sheets down to fit the smaller bed, that is 125 hours per year of labor that adds no value. At a loaded labor rate of $40 per hour, that is $5,000 per year spent on handling that a 4×8 bed would eliminate.
The correct comparison is not machine price versus machine price. It is total annual cost of the 4×4 cell versus total annual cost of the 4×8 cell, including labor, floor space, energy, maintenance, and consumables.
Growth Planning Without Overbuying
Many buyers justify a 4×8 router by saying they expect to grow into it. That logic works only if the growth is real and measurable. If your shop has been running the same volume for two years and the sales pipeline does not show a step change, the bigger bed is likely an overbuy.
A more disciplined approach is to plan for the next 12 to 18 months of confirmed work, not speculative growth. If a major customer has signed a contract that will double your sheet volume, the 4×8 bed makes sense. If you are hoping to win more work but have not secured it, the 4×4 bed keeps your capital exposure lower and your cell more flexible.
Some shops solve the growth problem by starting with a 4×4 and adding a second machine later. Two 4×4 routers can run different jobs simultaneously, which improves throughput for mixed work. That approach also spreads risk: if one machine is down for maintenance, the other keeps producing. A single 4×8 router is a single point of failure.
Use a Short Scorecard Before You Commit
Score both formats against the same real questions before you make a decision:
- Which bed matches how stock enters the shop today?
- Which one removes more non-cutting touches per order?
- Which one fits the actual staffing model, not the ideal future one?
- Which one leaves the cleaner path to the next operation?
- Which one would still feel right if the next six months looked exactly like the last six?
- Which one fits the available floor space including staging and access?
- Which one matches the dust collection and vacuum capacity you already have?
- Which one supports the nesting software you use without forcing inefficient splits?
Choose 4×4 when compact handling, direct access, and high-mix flexibility create more value than full-sheet flow. Choose 4×8 when the shop keeps paying too much labor every week to force standard panels through a smaller format.
The right answer comes from your material entry pattern, your operator model, and your downstream flow. Measure those honestly, and the bed size decision becomes clear.