Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
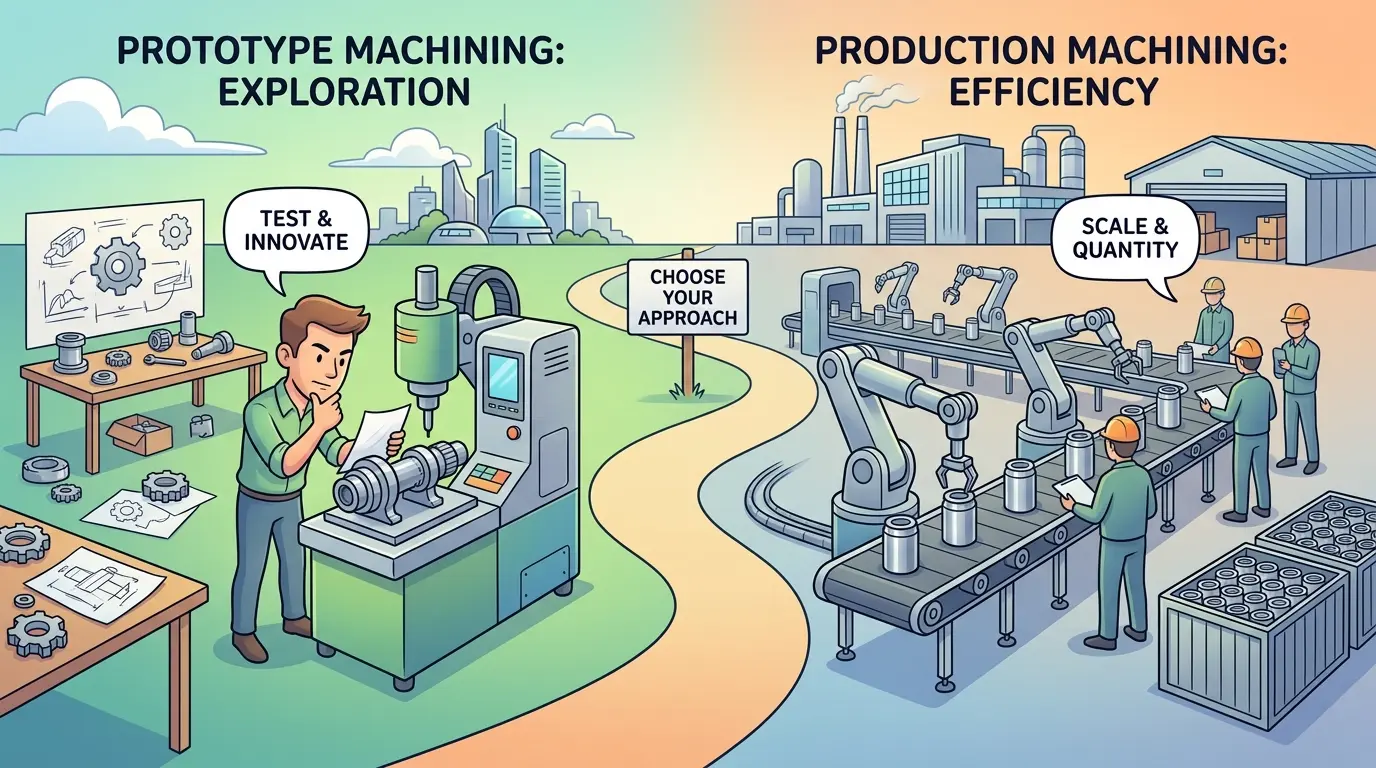
Prototype machining and production machining are not two speeds of the same job; they are two different contracts with opposing priorities. When a part is still changing weekly, you are buying learning velocity, not unit economics. When the design stabilizes, you must shift to process stability, fixture logic, and inspection rhythm. The costly failure occurs when teams demand prototype flexibility at production prices or expect production consistency from a moving design. Before you compare quotes or select a supplier, identify which question your current order must answer: does the design work, or can it repeat economically?
Prototype Machining Buys Answers, Not Perfect Economics
Prototype machining exists to shorten the learning cycle. The goal is rarely perfect unit economics. The goal is to answer questions quickly. Does the part fit? Does the geometry interfere with adjacent components? Is the wall too thin, the radius too sharp, the feature too difficult to reach, or the assembly harder than expected?
In that environment, flexibility is valuable. Engineers may revise the CAD repeatedly. Suppliers may need to make reasonable process accommodations to get a part in hand quickly. A prototype part can be successful even if it is not the cheapest possible route, because its real value lies in what it teaches before larger commitments are made.
That is why prototype machining often carries a higher per-part cost. Buyers are not paying only for metal removal. They are paying for responsiveness, setup agility, and the ability to iterate without freezing the design too early.
This point matters because many commercial arguments go wrong right here. Teams start criticizing prototype pricing as if it were failed production pricing, when in fact the quote is reflecting the cost of uncertainty, revision risk, and low-volume agility.
Production Work Buys Predictability, Not Experimental Freedom
Production machining changes the center of gravity. Once the design is stable enough to repeat, the process must shift toward consistency, throughput, fixture logic, tool life, inspection rhythm, and predictable delivery. At that point, the question is no longer “Can we make this part today?” It becomes “Can we keep making this part reliably and economically over time?”
That means features that were acceptable in a prototype context may need revision for production. A feature that can be machined once with careful attention may be a weak choice if it slows cycle time, complicates fixturing, or creates variation risk across hundreds or thousands of parts.
Production thinking is not less precise than prototype thinking. It is more systemic. It asks how the whole process behaves, not just whether one part can be achieved. It also forces the team to care about issues that barely matter during prototypes: setup repeatability, lot traceability, packaging discipline, operator instructions, and how quickly a problem can be detected before it spreads across a batch.
Compare the Decision Logic Before Comparing Speed
Prototype machining prioritizes learning speed and design freedom. Production machining prioritizes process stability and cost discipline. Those priorities affect nearly every decision.
In prototyping, buyers may tolerate slower manual setups, special handling, or less optimized process paths if it gets a usable part quickly. In production, those same accommodations become expensive. They add variability, consume labor, and make output less predictable.
This is why prototype-friendly designs are not automatically production-friendly designs. A part that works as a prototype may still need simplification, fixture-aware changes, or tolerance cleanup before it becomes a good production part.
The problem is not that one phase is better than the other. The problem is that teams often demand the wrong behavior from the phase they are in. They want prototype flexibility at production prices, or production consistency from a design that is still moving every week.
How Buyers Should Know Which Phase They Are Actually In
Ask what question the current order is supposed to answer.
If the main question is whether the design works at all, you are in prototype mode. If the main question is whether the design can be repeated consistently at acceptable cost, you are already moving into production thinking.
Another practical test is revision frequency. If drawings are still changing quickly, prototype logic probably still dominates. If drawings are stabilizing and the team is now focused on cycle time, yield, and supply continuity, the process is shifting toward production.
Pilot lots, bridge quantities, and “pre-production” labels do not change this logic. A program is not in true production simply because the quantity is larger than a prototype batch. If the team is still learning essential things about the part or the process, the program is still carrying prototype risk.
What Must Change Between Prototype And Production
Several things should change during the transition.
Design intent should become clearer. Critical features should be identified. Tolerances should be rationalized instead of inherited casually from the first model. Features that complicate fixturing or add cost without adding value should be reconsidered.
Process planning should become more deliberate. Workholding strategy, setup sequence, tool access, inspection method, packaging logic, and revision control all matter more in production than they do in an early prototype sprint.
Supplier communication needs to change as well. In prototype work, the supplier may help interpret incomplete decisions. In production, ambiguity becomes a liability. Drawings, assumptions, acceptance criteria, and delivery expectations should all become more explicit.
If these elements do not mature, the team may think it is entering production while still behaving like an extended prototype program.
The Dangerous Middle Is Usually The Pilot Stage
The most confusing stage is often the middle one. The design is more stable than it was during early prototyping, but the process is not yet reliable enough to behave like full production. Many teams describe this as a pilot, trial batch, launch lot, or bridge order.
This stage matters because it reveals whether the design can survive contact with repetitive manufacturing logic. A part that worked in prototype may start showing hidden issues once multiple setups, longer runs, broader operator involvement, and real delivery pressure enter the picture.
That is why pilot machining should not be treated as discounted production. It is a risk-reduction phase. The team is buying confidence that fixtures, sequence, tooling, inspection, packaging, and documentation behave under more realistic conditions than the prototype stage ever demanded.
Cost Misunderstandings Happen In Both Directions
Buyers often complain that prototypes cost too much per part. That complaint misses the point. Prototype pricing reflects uncertainty, engineering interaction, and low-volume setup economics. It is not supposed to look like steady-state production.
On the other hand, buyers sometimes launch production thinking the prototype price should scale directly. That assumption also fails, because production demands different controls and different process commitments. Cost may fall per part, but only if the design and workflow actually support efficient repetition.
This is where structured quote comparison matters. Teams moving from design validation into volume should compare CNC quotes carefully so they understand what is changing in scope, assumptions, inspection logic, and production responsibility.
The commercial mistake on the supplier side is similar. If a supplier quotes prototype work as if it were clean production, the buyer may receive an attractive number that only survives by hiding the real engineering effort somewhere else.
Revision Control Separates Serious Production From Controlled Chaos
Prototype programs often survive with loose revision handling because everyone knows change is coming. Production programs usually do not. Once output must repeat predictably, revision ambiguity becomes one of the fastest ways to create scrap, rework, and supplier conflict.
That means phase transition should include a real decision about when the design is frozen enough to justify fixture investment, standardized programs, controlled work instructions, or formal launch commitments. If revisions continue to drift informally through email or meeting notes, production discipline will stay weak no matter how often the order is called a production order.
One of the most useful transition habits is setting clear phase gates. Prototype freeze, pilot release, production release, and engineering change control should not be ceremonial labels. They should change how the organization behaves.
Inspection Strategy Must Mature With The Program
Inspection in prototype work is often targeted and pragmatic. The team may focus on learning-critical dimensions, functional fit, or confirming that a few high-risk features behave as expected. Full documentation may be light because the goal is speed of learning.
Production cannot depend on that same informal logic. Once the part is repeating, the inspection plan must match the cost of failure and the realities of lot behavior. Critical features need defined measurement paths. Incoming and outgoing expectations must align. The team should know whether the process is being controlled tightly at launch or monitored through a more mature sampling rhythm later.
This does not mean every part needs the most elaborate quality regime available. It means inspection has to fit the phase honestly. Over-building inspection too early slows learning. Under-building it too late destabilizes production.
The Best Supplier For Prototypes Is Not Always The Best Supplier For Production
Some suppliers are very strong at prototype response and less compelling for long-run production. Others are optimized for repeat manufacturing and less flexible during early development. Buyers should not assume the same partner is automatically the best fit for both phases.
The useful question is whether the supplier understands the current purpose of the order. If the supplier is set up for learning speed, they may be excellent in early development. If the program is stabilizing and output risk is rising, buyers should reassess whether the process support remains sufficient.
That is not a criticism of either model. It is simply good manufacturing planning. If a new supplier enters at the production stage, however, the handoff should be treated carefully. Matching a print is not always enough to match the real functional behavior that earlier iterations uncovered.
For broader supplier evaluation, it helps to think in the same structured way used when comparing machining companies on capability, quality, and lead time.
A Transition Checklist That Prevents Expensive Phase Confusion
Before moving a part from prototype logic into production logic, teams should be able to answer these questions clearly.
- Has the design stabilized enough that fixture and tooling decisions will not be invalidated immediately?
- Are critical features identified and separated from dimensions that were tolerated loosely during learning?
- Has the inspection method been upgraded to match repeat-order risk?
- Are revision controls strong enough that suppliers and internal teams are working from the same release?
- Has the supplier fit been re-evaluated for repeatability rather than only responsiveness?
- Do commercial assumptions reflect production responsibility instead of prototype flexibility?
If several of these answers are still uncertain, the program is probably not ready to be judged as true production.
How Pandaxis Fits This Decision
Pandaxis focuses on industrial machine categories where throughput, repeatability, and workflow fit are central buying criteria. That broader perspective is useful because it shows how manufacturing decisions evolve once the conversation shifts from proving an idea to sustaining a process.
If a team is moving from experimental development toward more stable manufacturing logic, it helps to think less like a prototype buyer and more like a process owner. Reviewing the wider Pandaxis product catalog can help frame that shift, because industrial equipment decisions are built around repeatability, workflow integration, and capacity alignment rather than one-off part success.
The article on when the difference between precision CNC machining and general machining actually matters is also useful here, because many prototype-to-production problems start when the team has not yet decided what level of process control the finished part truly justifies.
Choose The Phase Honestly, And The Process Gets Much Easier
Prototype machining and production machining serve different goals and should be managed differently. Prototypes are for learning, validating, and revising quickly. Production is for repeating reliably, protecting quality, and controlling cost across time. The more clearly a team understands which phase it is in, the better its drawings, supplier expectations, and sourcing decisions become.
The most expensive mistake is trying to force one phase to behave like the other. Treat the transition deliberately, and the manufacturing path becomes much easier to scale with confidence. Teams do not need to eliminate uncertainty instantly. They do need to stop pretending that uncertainty and repeatable production can be managed by the same rules.
Prototype runs should generate actionable DFM notes: corner radii that reduce chatter, hole accessibility that enables true position achievability, and material alternatives if supply tightens. Production benefits when those notes become tracked action items with owners—otherwise prototypes become a museum of good intentions.
Cost Accounting: Where Learning Expense Should Land
Be honest internally about which budget funds prototype learning. Hiding NRE inside production piece price distorts product margin and causes teams to under-invest in early learning. Conversely, walling off prototypes as “unlimited R&D” removes discipline. A defined learning budget is usually healthier than both traps.
Summary
Choose prototype machining when learning and iteration dominate; choose production machining when repeatability, unit cost, and schedule certainty dominate. Separate the phases explicitly—revision control, inspection depth, tooling strategy, and named freeze gates—and plan supplier transitions deliberately. Mixing the two without discipline ships neither speed nor economy; it ships confusion onto the shop floor, invoices without accountability, and documentation debt your future teams inherit.
Prototype machining buys learning velocity; production machining buys predictable replication. Treat them as different products with different contracts, different inspection plans, and different supplier strengths—or pay both invoices twice for the same lesson. Name your phase out loud in meetings; unnamed phases become expensive misunderstandings between teams that each believe they already agreed.