Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
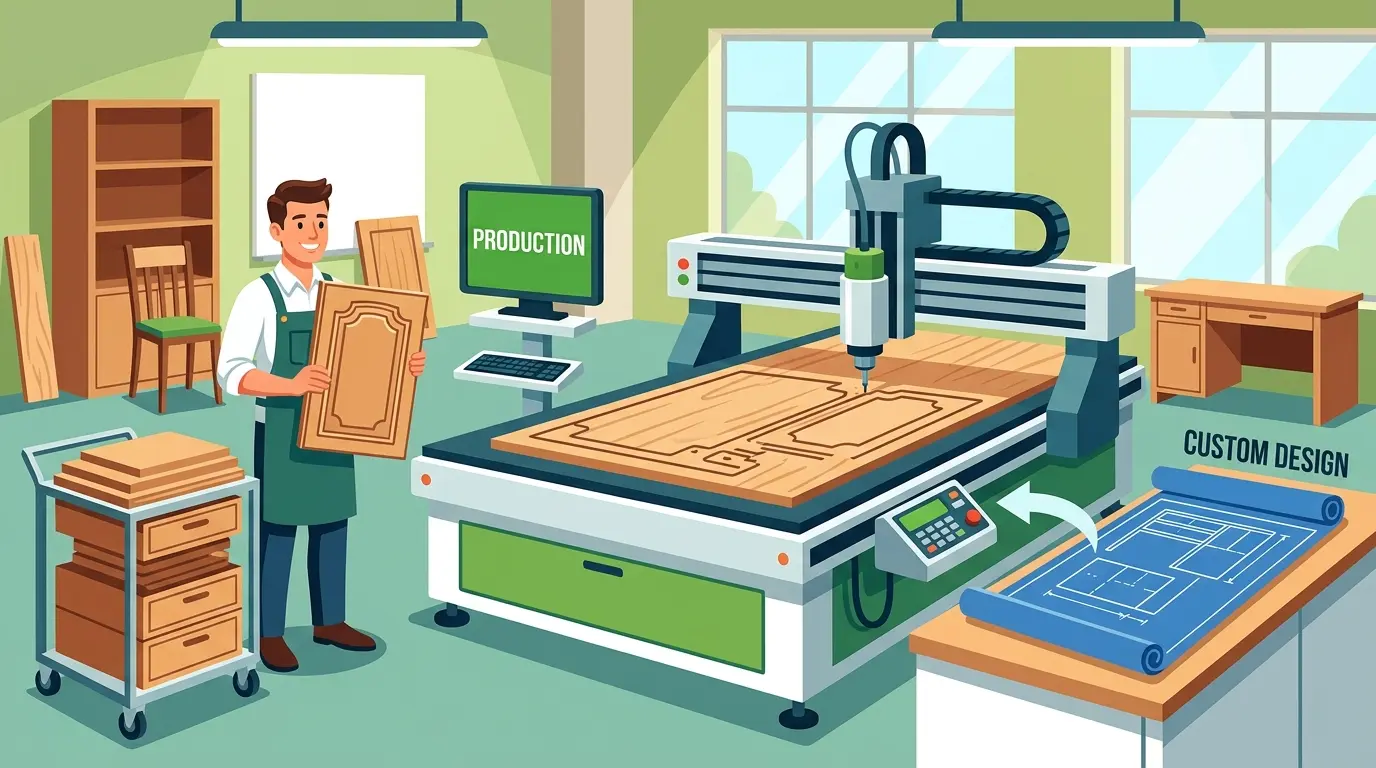
Before you commit capital to a 4×8 CNC router, the decisive question is not whether the bed matches your sheet stock but whether the machine will organize full-sheet flow into clean, traceable part groups for drilling, edging, and assembly. This guide forces buyers to audit the entire routing cell—vacuum hold-down for small parts, toolpath sequencing, labeling, dust collection, and downstream absorption—before comparing spindles or demo cuts. If your line loses part identity or shifts labor downstream, the router amplifies the problem rather than solving it.
Start With the Sheet, Not the Spindle
A 4×8 CNC router looks like the obvious choice for cabinet and furniture production because the bed matches standard panel stock. That part is easy. The harder question is whether the machine will shorten the route from sheet to assembly-ready parts, or simply turn one cutting problem into a sorting problem.
The strongest buying case is not “we use sheet goods, so we need a 4×8.” It is “this machine will reduce handling, preserve part identity, and feed the next stations cleanly.” In cabinet and furniture work, the router is rarely the last meaningful step. Parts still need drilling, edging, stacking, inspection, and assembly preparation. That means the machine has to do more than cut profiles. It has to help the factory keep full sheets intact long enough to avoid unnecessary breakdown, cut slots, pockets, openings, and profiles in one controlled stage, and release output in a form the next department can understand quickly. When that happens, the 4×8 creates value far beyond spindle time.
Part Identity Is the Hidden Buying Variable
Many buyers focus on spindle power, speed, or cut quality. In cabinet and furniture production, part identity often matters more. If the line loses track of what each part is, where it belongs, or what the next step should be, the routing cell starts creating downstream cost immediately. That usually shows up as resorting after unload, lost orientation before drilling or edge work, small parts getting mixed into the wrong job group, and assembly delays caused by confused release flow. A router that cuts fast but releases parts into confusion is not yet producing clean value.
Where a 4×8 Usually Fits Best
This bed size is usually strongest when the factory already has a repeatable sheet-based workflow but still needs routing flexibility. Typical strong-fit settings include growing cabinet shops processing standard boards daily, wardrobe and shelving lines with repeated parts plus order variation, furniture factories combining recurring panels with shaped components, and fixture and retail producers still built around sheet material. The common thread is not just bed size. It is the need to keep full-sheet flow under control while still allowing part variation.
Watch the Handoff More Than the Demo Cut
The cleanest buying test is not whether the sample cuts well. It is whether the handoff after the cut looks calm. In live cabinet production, four warning signs matter quickly:
- Parts leave the bed as a mixed pile instead of a usable job group.
- Small parts become unstable late in the nest and force operator intervention.
- Labels, orientation, or next-step sequence are lost during unload.
- The next process cannot absorb output at the rate the router releases it.
Those issues usually cost more than a modest difference in cut speed ever will.
A Router Is Not Always the First Problem to Solve
A 4×8 router is often the wrong first investment when the real bottleneck is somewhere else. That is often true when the work is still dominated by straight rectangular sizing, software and release discipline are loose, one operator is already overloaded with loading, unloading, sorting, and rework, or downstream stations are too disorganized to absorb more routed output. If the real problem is straight panel sizing, stronger upstream equipment such as panel saws may remove more daily friction first.
Router Versus Nesting Is Often the Real Question
Many factories say they need a 4×8 router when they are really deciding whether a standalone routing step is still enough. A straightforward 4×8 router can work well when the main gain is flexible profiling and shaped panel work. Once the business needs tighter grouping, cleaner sheet use, and less manual handling between processes, the conversation often becomes broader than routing. That is when it helps to step back and compare what changes when the shop moves toward nesting-driven furniture production, or to review whether CNC nesting machines are now the more honest fit.
Downstream Capacity Decides Whether the Router Earns Its Place
The routing cell only succeeds if the next stations can absorb the output without confusion. Two downstream pressure points usually matter first. Boring and drilling machines require parts to arrive with orientation and grouping intact. Edgebanders require parts to move forward without resorting, relabeling, or fresh edge damage. If the router only shifts labor downstream instead of removing it, the buying case is weak even if the cutting performance looks good.
Audit the Whole Cell Before the Machine
Before choosing a model, map the entire routing cell as if it were already installed. Check how full sheets will arrive and be loaded, how nests will be grouped by order, cabinet, or next operation, how small parts and remnants will stay stable, how finished parts will be sorted, labeled, and transferred, and how offcuts and skeletons will leave the area. If those answers are weak, the machine will expose process problems faster than it solves them.
Questions Buyers Should Force Into the Quote Stage
Suppliers should be answering the factory’s actual routing problem, not just presenting a machine story. Ask how your common materials and nest patterns would move from load to unload on the machine, what stays manual after installation, and what really changes. Ask how part identity is preserved once the nest is cut, what habits keep small parts stable late in the sheet, and what labor model the recommendation assumes. Then compare what is included and what is quietly left to the buyer.
The Most Honest Buying Rule
Buy a 4×8 router for cabinet and furniture production when it helps the factory process full sheets with less handling, cleaner grouping, and stronger handoff into drilling, edging, and assembly. Do not buy one just because the bed matches the stock size if the rest of the line is still too loose to turn cut parts into usable production flow. The machine is a means to organize the sheet, not a substitute for organizing the line around it.
Material Handling and Sheet Flow: The Real Cost Drivers
The physical movement of panels into and out of the router is where most hidden costs accumulate. A 4×8 bed accepts a full sheet, but the operator still has to lift, position, and secure that sheet before the cycle starts. If the shop uses 18mm melamine-faced MDF or 16mm plywood, a full 4×8 sheet can weigh anywhere from 25 to 40 kilograms depending on core density and coating. That weight matters when the operator handles twenty or thirty sheets per shift. Manual loading quickly becomes a fatigue issue, and fatigue shows up as misaligned sheets, skipped vacuum zones, or damaged edges before the router even starts.
Consider how the sheet arrives at the machine. If it comes from a panel saw or a storage rack, the router cell needs a clear staging area. A roller table or an air-float table in front of the machine reduces the physical effort of positioning the sheet. Without that, the operator is dragging panels across the floor, which risks scratching the faces and skewing the sheet on the bed. A skewed sheet means the nest is not aligned to the material, and the first cut can be off by a few millimeters. That error propagates through the entire part, and the part either gets scrapped or requires rework at the edgebander or drilling station.
The unload side deserves equal attention. After the cycle finishes, the operator has to remove the cut parts, the remnant, and the skeleton. If the nest is dense, the skeleton may be a fragile lattice that collapses when lifted. That collapse can damage the edges of the parts still attached to the skeleton. A better approach is to plan the nest so that the skeleton remains rigid enough to lift in one piece, or to use tabbing and micro-tabs that hold small parts in place until the operator breaks them free. Some shops use a vacuum table with multiple zones so that the operator can release only the finished parts while keeping the remnant and skeleton held down. That reduces the risk of parts shifting during unload.
Vacuum Hold-Down and Small Part Stability
The vacuum system is the backbone of a 4×8 router, and it is often under-specified in the quote. A standard 4×8 bed with a single vacuum pump may hold a full sheet of plywood or MDF without issue, but the real test comes when the nest includes small parts. A part that is only 150mm by 200mm has a small surface area, and the vacuum force on that area may not be enough to keep it stationary during high-speed cutting. If the part shifts, the cutter can push it out of the nest, and the tool may break or the part may be ruined.
The solution is usually a combination of a stronger vacuum pump, a segmented vacuum table, and a porous spoilboard. A segmented table allows the operator to isolate vacuum zones so that the pump does not waste suction on areas where there are no parts. A spoilboard with a fine grid of holes distributes the vacuum evenly across the sheet. For very small parts, some shops add a thin layer of sacrificial material, such as a 3mm MDF sheet, and cut through the part into the sacrificial layer. That creates a seal around the part and increases the effective vacuum area.
Another option is to use mechanical hold-downs, such as toggle clamps or spring-loaded pins, for parts that are too small for reliable vacuum retention. These are slower to set up, but they are reliable for high-value parts where a shift would be costly. The tradeoff is setup time. If the shop runs many small-batch jobs with different part geometries, mechanical hold-downs may add minutes to every changeover. That is acceptable for a job shop but not for a high-volume production line.
Tooling Selection and Spindle Speed
The spindle and the tooling determine the surface quality and the cycle time. A 4×8 router for cabinet work typically uses a spindle in the 6kW to 9kW range, with variable speed control from 9,000 to 24,000 RPM. That range covers most woodworking operations, from roughing passes on plywood to fine finishing passes on hardwood veneers. The spindle power matters most when cutting dense materials or when using large-diameter tools. A 12mm compression bit cutting through 18mm MDF at 18,000 RPM requires a certain amount of torque, and a spindle that is underpowered will stall or produce a rough finish.
Tool selection is where many shops save money on the quote but lose money on the floor. A cheap 8mm single-flute bit may cut fine for a few sheets, but it dulls quickly and leaves burn marks on the edges. A high-quality carbide compression bit with a proper chip-breaker geometry will last much longer and produce a cleaner cut. The tradeoff is the upfront cost, but the per-part cost is usually lower with a better bit because it requires fewer changeovers and less sanding after the cut.
For cabinet work, the most common tools are compression bits for cutting panels, spiral bits for profiling and edge finishing, and drill bits for through-holes and pocket holes. Some shops also use a scoring tool or a separate scoring pass to prevent tear-out on melamine-faced boards. Tear-out on the top face is a common problem when the cutter exits the material, and a scoring pass or a down-cut spiral bit can eliminate it. The downside is that a scoring pass adds cycle time, so the shop has to decide whether the extra seconds are worth the reduction in rework.
Nesting Software and Toolpath Strategy
The software that generates the nest and the toolpath is as important as the machine itself. A good nesting program will arrange parts on the sheet to minimize waste, but it also has to consider the cutting order. Cutting the perimeter of a part before cutting the interior features can leave the part unstable. The software should sequence the cuts so that small parts are cut last, or so that the toolpath leaves tabs that hold the part in place until the final pass.
Toolpath strategy also affects cycle time. A common mistake is to use a single pass for all cuts, regardless of the material thickness. For 18mm material, a single pass with a 12mm compression bit may be possible, but it will put a heavy load on the spindle and may cause deflection. A better approach is to use a roughing pass that removes most of the material, followed by a finishing pass that cleans up the edge. That adds time but improves the surface quality and reduces the risk of tool breakage.
The software should also generate a label or a barcode for each part, and that label should be printed and applied to the part before it leaves the bed. Some routers have an integrated labeling system that prints and applies the label automatically. That is a significant advantage because it removes the manual step of sorting and labeling after unload. If the router does not have an integrated labeler, the shop needs a clear procedure for labeling parts as they are removed from the bed. Without that, part identity is lost, and the downstream stations have to guess which part goes where.
Dust Collection and Air Quality
A 4×8 router generates a lot of dust and chips, especially when cutting MDF or particleboard. The dust collection system has to be sized to the machine’s chip load. A typical router with a 6kW spindle can produce several cubic meters of air per minute of dust-laden air. The collection hood around the spindle has to capture that dust at the source, and the ducting has to carry it to a cyclone or a baghouse. If the dust collection is inadequate, the dust settles on the bed, the spoilboard, and the machine frame. That dust can interfere with the vacuum hold-down, and it can also be a fire hazard if it accumulates near the spindle.
The shop should also consider the air quality in the work area. Fine dust from MDF and particleboard is a health hazard, and the shop may need to meet local occupational safety standards for airborne particulate. A good dust collection system with a HEPA filter on the return air will keep the shop within those limits. The cost of the dust collection system is often a separate line item in the quote, and it is worth spending more on a system that is oversized rather than undersized. An undersized system will struggle to keep up with the router, and the operator will spend time cleaning the machine instead of running parts.
Changeover and Batch Size Considerations
The 4×8 router is a flexible machine, but flexibility comes at the cost of changeover time. Every time the shop switches from one job to another, the operator has to load a new sheet, possibly change the tool, and update the nest in the software. For a job shop that runs many small batches, the changeover time can dominate the cycle time. A shop that runs a hundred different cabinet fronts per week will spend more time on changeovers than a shop that runs a thousand identical panels.
To reduce changeover time, the shop should standardize the tooling as much as possible. If most jobs use the same compression bit for cutting and the same spiral bit for profiling, the operator does not have to change tools between jobs. The software should also store the nest and toolpath for each job, so the operator can recall it quickly. Some shops use a tool library in the software that automatically selects the correct tool for each operation, which reduces the risk of using the wrong tool.
Batch size also affects the choice between a 4×8 router and a nesting machine. A nesting machine with an automatic tool changer and a larger bed can handle larger batches more efficiently, but it costs more. For a shop that runs batches of ten to fifty sheets, a 4×8 router with a manual tool change may be sufficient. For a shop that runs batches of a hundred or more sheets, the nesting machine will pay for itself in reduced changeover time and higher throughput.
Operator Skill and Training
The best 4×8 router in the world will not produce good parts if the operator does not know how to use it. The operator has to understand the software, the tooling, the vacuum system, and the material. That knowledge comes from training and experience. A new operator will make mistakes, and those mistakes will cost money in scrapped parts and damaged tools. The shop should budget for training time, and it should have a senior operator who can mentor the new person.
The software interface matters for operator efficiency. A graphical interface that shows the nest and the toolpath is easier to understand than a text-based interface. The operator should be able to see the progress of the cut on the screen, and the software should alert the operator to any issues, such as a tool that is about to break or a vacuum zone that is not holding. Some software packages also include a simulation mode that lets the operator run the toolpath virtually before cutting the sheet. That is a valuable tool for catching errors before they cost material.
Maintenance and Spare Parts
A 4×8 router is a mechanical machine, and it will wear out over time. The spindle bearings, the linear guides, the ball screws, and the vacuum pump all have a finite lifespan. The shop should have a maintenance schedule that includes regular lubrication, belt tension checks, and spindle temperature monitoring. The maintenance schedule should be based on the manufacturer’s recommendations, but the shop should also track the actual usage and adjust the schedule accordingly.
Spare parts are another consideration. The shop should stock the most common consumables, such as vacuum gaskets, spoilboard material, and tool holders. It should also have a plan for getting replacement parts quickly if a major component fails. A spindle failure can take the machine down for days, and the shop should have a spare spindle or a rental option available. The cost of downtime is usually much higher than the cost of the spare part, so it is worth investing in a small inventory of critical components.
Comparing the 4×8 Router to Other Equipment
The 4×8 router is not the only machine that can cut panels. A panel saw is faster for straight cuts, and a nesting machine is more efficient for high-volume production. The choice depends on the shop’s product mix and volume. A shop that makes mostly rectangular panels with occasional shaped parts may be better served by a panel saw and a smaller router for the shaped parts. A shop that makes mostly shaped parts with a high degree of variation may be better served by a 4×8 router. A shop that makes a high volume of standard parts may be better served by a nesting machine.
The comparison should also include the cost of the ancillary equipment. A 4×8 router needs a dust collection system, a vacuum pump, and a computer with the nesting software. A panel saw needs a dust collection system and a computer with the cutting optimization software. The total cost of ownership includes the purchase price, the installation cost, the training cost, the maintenance cost, and the cost of consumables. The shop should calculate the total cost per part for each option, not just the purchase price.
Make the 4×8 CNC Router Buying Guide for Cabinet and Furniture Production Decision
The decision to buy a 4×8 router should be based on a clear understanding of the shop’s production needs. The shop should map its current workflow, identify the bottlenecks, and determine whether the router will remove those bottlenecks or simply move them downstream. The shop should also consider the long-term direction of the business. If the shop expects to grow its volume and add more shaped parts, the router is a good investment. If the shop expects to stay with a simple rectangular product line, a panel saw may be a better use of capital.
The quote stage is the time to ask the supplier hard questions. The supplier should be able to demonstrate the machine on the shop’s own material, with the shop’s own nest. The supplier should also provide a clear breakdown of the costs, including the machine, the installation, the training, and the ancillary equipment. The shop should not be afraid to negotiate on the price, but it should also be willing to pay for quality. A cheap machine that breaks down frequently will cost more in the long run than a well-built machine that runs reliably.
The Bottom Line for Cabinet and Furniture Shops
A 4×8 CNC router is a powerful tool for cabinet and furniture production, but it is not a magic solution. It works best when the shop has a clear process for handling sheets, cutting parts, and moving parts to the next station. The machine will amplify the strengths of a well-organized shop, and it will expose the weaknesses of a disorganized one. The buying decision should be based on the shop’s actual production needs, not on the appeal of a new machine. If the shop is ready to organize its workflow around the router, the investment will pay off. If not, the money is better spent on improving the process first.