Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
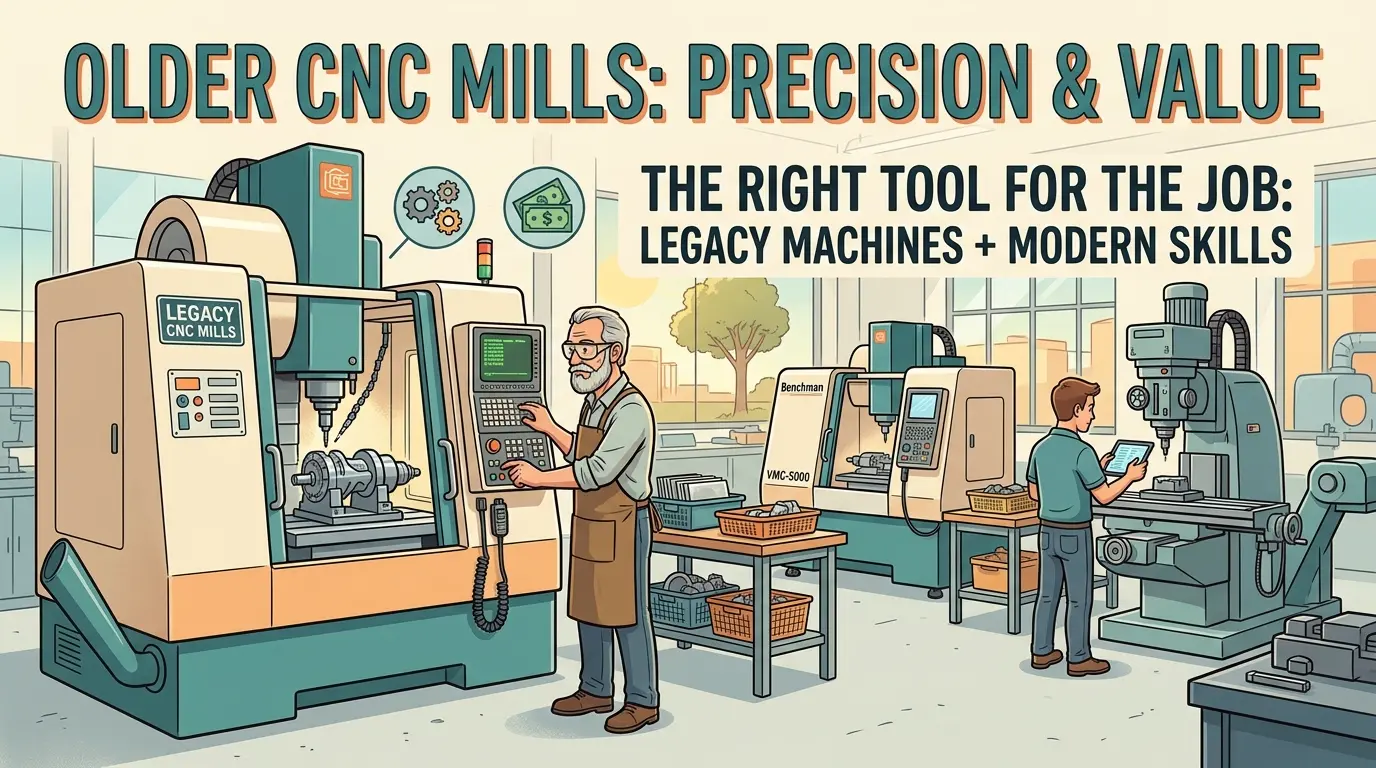
Older CNC mills like the Benchman VMC 5000, Maho 600, and Devlieg 2B 36 attract buyers with low listing prices, but that number never reflects the true cost of ownership. Rigging, electrical prep, control cleanup, repairs, and verification cuts quickly reshape the economics, and the real decision hinges on whether your shop can sustain the support burden. Before you commit to legacy iron, you must separate mechanical condition from control practicality, define a narrow job scope, and price retrofit as a full project—otherwise a bargain becomes a production-stopping distraction.
Where Legacy-Machine Costs Appear After Purchase
The listing price on an older CNC mill is only the opening number. After that comes rigging, transport, electrical preparation, access planning, tooling, coolant, repairs, control cleanup, verification cuts, and the time needed to make the machine trustworthy. On larger legacy equipment, even placement and power compatibility can change the economics materially.
That is why older machines like the Benchman VMC 5000, Maho 600, Devlieg 2B 36, and similar platforms create such divided opinions. Both sides usually have a point. An older machine can still be a very smart asset, but only when the machine, the job, and the support model match. Without that alignment, a bargain purchase can turn into a slow restoration project with a production schedule attached to it.
The right way to judge older mills is therefore not old versus new in the abstract. It is productive ownership versus expensive distraction.
The First Real Question Is Not About Iron, But About Ownership
Many legacy-machine discussions start with spindle taper, travel, table size, casting mass, or brand reputation. Those all matter. But the first practical question is simpler: who in the company will actually keep the machine productive?
If the answer is clear, the purchase becomes more plausible.
- The shop already understands older controls or similar platforms.
- Someone on staff can handle electrical and mechanical diagnosis.
- The machine will live in a toolroom, maintenance area, or lower-pressure workflow.
- The business can tolerate a stabilization period.
If the answer is vague, the risk rises fast.
- One experienced person knows older machines, but is already overloaded.
- The shop assumes outside help will always be available quickly.
- Nobody has priced what happens when a control issue stops the machine for a week.
This is why ownership matters more than the romance of older iron. A legacy mill is never just a casting and a spindle. It is a support commitment.
Model Reputation Matters Less Than The Specific Machine Sitting On The Floor
Older models build reputations over decades, but the individual unit in front of you matters much more than the badge. Two machines with the same name can behave very differently depending on maintenance history, crash history, retrofit quality, storage conditions, and undocumented changes made by previous owners.
Buyers should therefore treat model reputation as background, not proof. The inspection still has to answer what this exact machine looks like now.
Useful inspection points include:
- Axis smoothness across full travel.
- Signs of backlash, stick-slip, or inconsistent movement.
- Spindle noise and behavior at speed.
- Table wear, crash repair, or obvious abuse.
- Lubrication-system condition.
- Electrical-cabinet cleanliness and evidence of improvised wiring.
- Quality of manuals, parameters, and machine records.
Older machines rarely fail as one dramatic event during the buying stage. More often they arrive with several medium-sized issues that combine into one expensive reality. That is why serious buyers inspect the individual unit, not the reputation story.
The Control Usually Decides Whether The Iron Is Practical Or Academic
Buyers love older machines because heavy castings, rigid frames, and old industrial build quality still have real value. But if the control situation is poor, the iron can become academic. A mechanically attractive machine may still be impractical if the control is unreliable, undocumented, unsupported locally, or mismatched to the shop’s staffing model.
That is why every legacy-mill purchase should separate two judgments clearly:
- Is the machine mechanically worth owning?
- Is the control situation worth living with?
Sometimes the answer is yes to both. That is when an older machine can be very smart. Sometimes the mechanical side is appealing but the control side quietly turns the purchase into a retrofit candidate, a chronic support dependency, or a machine that nobody wants to touch when it goes down. That is not automatically a reason to walk away, but it is absolutely a reason to stop pretending the deal is simple.
A Legacy Mill Needs A Narrow And Honest Job Description
Older CNC mills are strongest when the shop can define exactly what work they are expected to do. Good fits often include toolroom tasks, repair parts, internal fixtures, maintenance components, lower-pressure prototypes, or recurring in-house jobs where rigidity and useful travel matter more than turnkey convenience.
That is the kind of work where older equipment can still shine. The shop values mechanical capability, can live with some setup and support complexity, and does not need the machine to behave like a new production-ready asset on the first morning.
Risk rises when the machine is expected to carry urgent customer-facing production with little tolerance for troubleshooting. In that environment every weak link becomes more expensive:
- Slow fault recovery.
- Sparse parts support.
- Limited control familiarity.
- Missing documentation.
- Dependence on one experienced person.
Legacy equipment works best when the job scope is honest enough to absorb those realities.
Retrofit Must Be Priced As A Project, Not As Comforting Language
One of the most dangerous sentences in legacy-machine buying is, “We can always retrofit it later.” That is sometimes true, but it changes the purchase from machine acquisition into machine redevelopment. Once retrofit enters the plan, the buyer is no longer simply pricing equipment. The buyer is pricing engineering time, control integration, commissioning effort, electrical work, debugging, and the internal focus needed to return the machine to stable service.
That does not make retrofit wrong. Some older machines earn a strong second life through it. But it does mean the buyer should answer retrofit questions before purchase, not after frustration begins.
- Who will specify the retrofit path?
- Is the mechanical platform worth that effort?
- What output will be lost during the project?
- Will the new control reduce long-term risk, or just replace one uncertainty with another?
- Does the shop need production now, or does it genuinely have time for a rebuild cycle?
If those answers do not exist yet, retrofit should not be used as emotional reassurance during the deal.
The Cheap Purchase Price Usually Hides Expensive Commissioning
The listing price on an older mill is only the opening number. After that come rigging, transport, electrical preparation, access planning, tooling, coolant, repairs, control cleanup, verification cuts, and the time needed to make the machine trustworthy. For a large older machine, power connection and placement constraints can determine whether the purchase remains practical.
This is where many good-looking deals begin to weaken. The iron may be inexpensive, but the shop still has to convert it into a reliable asset. That conversion cost can be completely rational if the machine truly fits the work. It becomes painful only when the buyer acted as if the listing price was the whole decision.
This is also why used-equipment discipline matters so much. A serious used CNC inspection checklist before payment is more valuable than general enthusiasm about any older machine family.
Parts, Documentation, And Local Support Belong In The Approval Decision
Newer machines usually win on clarity. Parts channels are clearer, documentation is fresher, and support paths are easier to identify. Older machines can still be workable, but the buyer has to build that clarity proactively.
Before approval, the shop should know:
- Which wear items and consumables remain easy to source.
- Which control failures could create long downtime.
- Whether local technicians can support the platform.
- Whether diagrams, parameters, and electrical records are complete enough to matter.
- Whether the business can tolerate a longer recovery window when something uncommon fails.
These are not theoretical questions. They decide whether the machine is a manageable asset or a risky dependency. Buyers who skip them are usually buying hope more than equipment.
Legacy Mills Fit Toolrooms Better Than Fragile Delivery Models
One reason older mills still survive productively is that some environments are naturally suited to them. Toolrooms, maintenance departments, repair operations, lower-pressure internal machining, and certain cost-sensitive job shops can often absorb the service burden if the mechanical platform is still worthwhile.
That is not usually true in fragile delivery models where customer deadlines leave no room for uncertainty. In those businesses the machine is judged less by how much iron it offers per dollar and more by how predictably it starts, runs, recovers, and returns to service after trouble. Older mills can still pass that test, but only if the shop has a much stronger support situation than many buyers assume.
This is why legacy mills usually succeed when the team sees them as maintained assets and fail when the team sees them as cheap shortcuts to modern uptime.
Buying Old Iron Is Rational Only When The Tradeoff Is Deliberate
There are strong reasons to buy an older CNC mill.
- The machine offers real rigidity and useful travel for the money.
- The shop has maintenance depth and control familiarity.
- The work is defined and can tolerate support complexity.
- The machine has been inspected honestly.
- The buyer knows whether it is a production tool, toolroom asset, or retrofit candidate.
There are weak reasons too.
- The machine looks impressive for the listing price.
- The castings seem heavier than anything new at the same number.
- Someone assumes old industrial iron is always better than newer lighter equipment.
- The shop wants future capability without defining present work.
The first group leads to rational ownership. The second usually leads to regret, delay, or endless postponement of the real capital decision.
When Newer Equipment Is The Smarter Answer
Older iron is not automatically noble just because it is substantial. If the business needs predictable uptime, fast fault recovery, operator simplicity, and lower internal troubleshooting burden, newer equipment is often the smarter answer even if the casting looks less romantic. There is nothing inefficient about buying clarity when clarity protects delivery.
This is especially important for shops that are already moving from toolroom-style work toward more formal production discipline. In those cases, the budget question is no longer only about how much machine mass can be bought for the money. It is about whether the process needs a more supportable and serviceable asset. For some buyers that means browsing the Pandaxis machinery lineup or reconsidering the production requirement entirely instead of trying to force an old platform into a modern uptime role.
Buy The Support Model Or Do Not Buy The Machine
Older CNC mills still make sense when the shop is buying with open eyes: mechanical condition verified, control reality accepted, job scope defined, and internal ownership planned. In those conditions, legacy machines can still provide serious value, especially where rigidity and lower capital entry matter more than modern convenience.
They stop making sense when the purchase relies on optimism instead of support planning. If the business needs modern predictability, fast recovery, and low troubleshooting burden, then a legacy mill is usually the wrong center of gravity no matter how good the iron looks.
The useful rule is simple: buy old iron only when you are also ready to buy its support model. Without that, the machine is not a bargain. It is a project pretending to be an asset.