Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
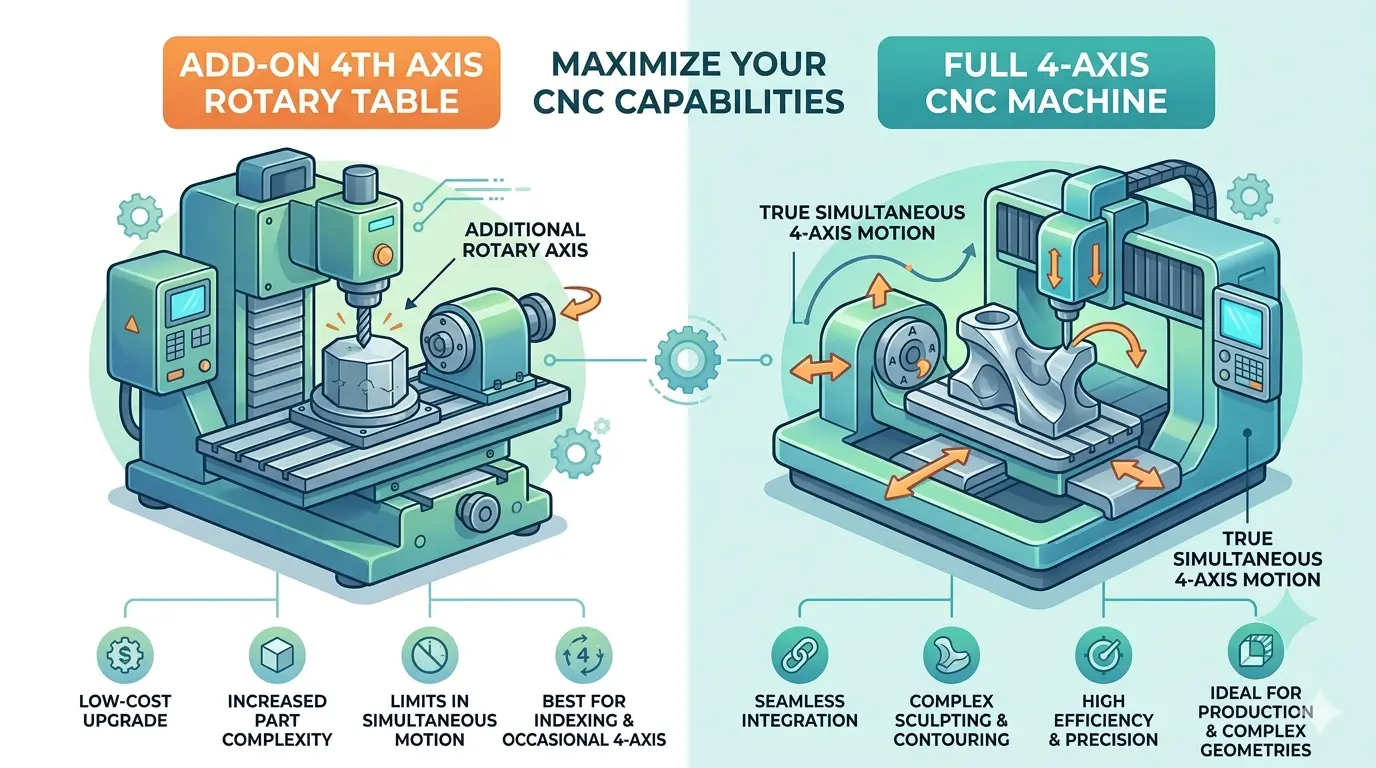
Start with the job, then compare rotary tables against integrated four-axis machining centers, stop counting axes and start counting hours. The real decision hinges on how often cylindrical parts, wrapped details, or indexed drilling actually appear in your weekly schedule. A retrofit indexer makes sense when rotary jobs are occasional and your existing three-axis machine still earns its keep on flat panels or nested parts. But when rotary families show up every week, the true cost shifts from hardware to changeover disruption, clearance compromises, and postprocessor debugging that quietly erode schedule integrity. This article forces that frequency-based evaluation before you commit capital.
Start With The Real Question: How Often Does Rotary Work Appear?
Before comparing hardware, compare schedules. The first question is blunt: how often do rotary jobs actually matter in a normal month? If indexed drilling, wrapped details, or cylindrical parts show up only occasionally, a rotary table or indexer may be the disciplined answer. It lets the team validate demand and build programming habits without replacing a machine that still earns money on flat work.
If the same rotary part families now appear every week, the question changes. At that point, the cost is no longer just hardware. It is repeated changeover, clearance compromise, capacity interruption, and support complexity on a machine that was not originally built around rotary work.
The mistake most shops make is treating this as a capability question. It is not. A retrofit fourth axis and a full four-axis machine can often machine the same geometry. The difference is how that geometry fits into the rest of the production week. A shop running 80 percent flat panels and 20 percent wrapped edges has a different problem than a shop running 60 percent cylindrical components. The first shop needs occasional rotary access without losing panel throughput. The second shop needs a machine whose motion envelope, workholding strategy, and programming workflow were designed around rotation from day one.
What The Add-On Route Usually Does Well
An add-on rotary unit is usually the right bridge when:
- Rotary jobs are real but not dominant in the production mix.
- The current three-axis machine still carries valuable flat work.
- Capital needs to stay controlled while demand is proven.
- The team wants to learn rotary workflow gradually.
The biggest advantage is lower commitment. You keep the machine you know, add a rotary axis, and start cutting cylindrical features without a full machine replacement. For a shop that is testing whether rotary work will become a regular part of the mix, this is a reasonable way to find out.
The biggest warning is that the base machine still defines the compromise. Table area may shrink, Z clearance may tighten, setup access may worsen, and flat-work rhythm may be interrupted whenever rotary hardware enters the schedule. A shop that runs a steady stream of panel processing or nested parts will feel that interruption quickly.
Consider a typical cabinet shop. The CNC router spends its week nesting cabinet parts, drilling shelf pin holes, and cutting dados. Once a week, a customer orders a cylindrical leg or a curved rail that needs rotary machining. The add-on route lets that shop take the job without buying a second machine. But every time the rotary table is mounted, the shop loses table area for nesting, spends 30 to 60 minutes on changeover, and must re-zero the machine before returning to panel work. If that happens once a week, the disruption is manageable. If it happens three times a week, the shop is effectively running two production systems on one machine, and neither runs at full efficiency.
What A Full Four-Axis Machine Usually Removes
An integrated four-axis machine becomes easier to justify when rotary work is no longer occasional. Its value is not only that it can rotate. It is that the rotary system, controls, structure, clearances, and support logic were planned together.
That usually gives the shop:
- Better repeatability on frequent rotary jobs.
- Fewer clearance and reach compromises.
- Clearer ownership of commissioning and support.
- Less engineering friction once rotary work becomes routine.
The difference is not raw capability. A well-integrated rotary axis on a dedicated machine behaves predictably because the machine builder accounted for the rotary system when designing the motion envelope, the control logic, and the safety interlocks. On a retrofit, those considerations are layered on top of a machine that was never intended to carry them.
Think about what happens during a typical rotary job on a retrofit. The operator mounts the rotary table, which reduces the usable X and Y travel. The workpiece is now held between centers or in a chuck, which changes the Z-axis approach. The toolpath must be generated with a postprocessor that understands the rotary axis, and the retract moves must be checked against the new collision envelope. Every one of these steps is a place where the process can fail. On a dedicated four-axis machine, the builder has already resolved those issues. The rotary axis is part of the machine’s native coordinate system, the postprocessor is tested, and the collision envelope is defined by the machine’s actual geometry.
A Practical Comparison Table
| Buying Question | Add-On Rotary Usually Fits Better | Full Four-Axis Usually Fits Better |
|---|---|---|
| Do we need rotary access before demand is fully proven? | Yes | Rarely |
| Do we still need the machine to spend most of its week on flat work? | Often yes | Less naturally |
| Do we need rotary to be routine, repeatable production? | Not usually | Yes |
| Do we want one supplier responsible for the full motion package? | Less often | Yes |
| Can the team tolerate more integration burden and support boundaries? | Sometimes, while demand is still developing | Less necessary once demand is established |
| Is the rotary part family visible in weekly scheduling? | Not yet | Yes |
| Does the current machine lose too much flat-work time to rotary changeovers? | Not yet | Yes |
| Does programming stability matter more than low entry cost? | Not yet | Yes |
This is the real trade. The retrofit path keeps commitment smaller. The integrated path reduces the number of moving parts the team must keep managing manually.
Capacity Sharing Is The Main Add-On Risk
One of the most common mistakes is ignoring what the base machine already does for the plant. If the existing router or mill is already revenue-critical for flat work, every rotary setup interrupts that revenue stream. The add-on route can look efficient until one platform is asked to support two different production rhythms. That is where the real cost often appears: not in spindle time, but in queue disruption.
Imagine a shop that runs a single CNC router for all its flat work. The router is scheduled for the full week: panels on Monday through Wednesday, nested parts on Thursday, and a mix of small jobs on Friday. Adding a rotary table means one of those days is now partially dedicated to rotary setup and machining. The flat work that would have run that day is pushed to the next day, which pushes the next job, and so on. The shop does not lose spindle time; it loses schedule integrity. Jobs that used to ship on time now ship late because the router is doing double duty.
In woodworking and furniture settings, that wider production logic matters even more. If the plant still depends on routing, drilling, and organized part flow, the better investment may sometimes sit elsewhere, such as boring and drilling capacity, rather than in forcing more jobs through one shared machine. A dedicated boring machine can take drilling work off the router entirely, freeing it for the flat work it does best while a rotary setup runs elsewhere.
This is a point that gets lost in most rotary table comparisons. The alternative to a retrofit fourth axis is not always a full four-axis machine. Sometimes it is a different machine altogether, one that removes a different bottleneck and leaves the router free to do what it already does well. A shop that is drowning in shelf pin holes does not need a rotary axis; it needs a dedicated drilling machine. A shop that is struggling with edge banding does not need a fourth axis; it needs a better edgebander. The rotary question should only be asked after the rest of the production line is balanced.
Retrofit Satisfaction Is Usually Decided By Boundaries
An add-on rotary is not just a piece of hardware. It adds offsets, fixture rules, post assumptions, collision zones, and support boundaries onto a machine that already has an established job pattern. Buyers should pin down these questions early:
- Who owns the postprocessor?
- Who proves retract strategy and collision assumptions?
- Who troubleshoots rotary-specific faults after installation?
- Who decides whether a problem belongs to the base machine, the add-on supplier, or the programming workflow?
If those boundaries stay vague, the cheaper option often becomes the noisier operational choice. A retrofit that requires constant engineering attention to keep running is not saving money; it is spending engineering hours that could go toward new part programming or process improvement.
Consider a typical failure mode. A shop installs a rotary table on its three-axis router. The first job runs well because the application engineer who sold the table also wrote the postprocessor and set up the toolpaths. The second job is different: the part is longer, the fixture is different, and the retract moves collide with the chuck. The shop calls the rotary table supplier, who says the problem is in the postprocessor. The shop calls the router manufacturer, who says the problem is in the fixture. The shop calls the CAM reseller, who says the problem is in the toolpath strategy. Three weeks later, the job still does not run reliably, and the shop has spent more in engineering time than it saved on the purchase price.
That is the real cost of a retrofit. It is not the hardware. It is the boundary management. Every time a rotary job fails, the shop has to figure out which of the three or four parties is responsible. On a full four-axis machine, that question does not arise. The machine builder owns the entire motion package, and one phone call resolves the issue.
A Good Add-On Decision Needs An Exit Condition
The retrofit path works best when it is treated as a bridge, not as an indefinite compromise. The business should define in advance:
- What level of recurring demand would justify a dedicated rotary cell.
- How much flat-work disruption is still acceptable.
- How much engineering time the shop is willing to keep spending on a mixed-purpose platform.
Without an exit condition, the add-on can drift from “disciplined test” into “permanent workaround.” That is a common failure mode in smaller shops: the rotary table gets installed, the first few jobs go well, and then the team discovers that every rotary job requires a different fixture setup, a different post tweak, or a different collision check. The machine still runs, but it runs less predictably.
A better approach is to set a threshold before the retrofit is purchased. For example, the shop might decide that if rotary jobs represent more than 25 percent of weekly spindle time for three consecutive months, it will move to a dedicated four-axis machine. That threshold gives the team a clear signal for when the retrofit has outlived its usefulness. It also prevents the slow drift toward a machine that is perpetually being reconfigured.
The exit condition should also include a time limit. A shop that installs a rotary table and still has not developed a repeatable rotary process after six months has a process problem, not a hardware problem. Continuing to invest engineering time in the retrofit is unlikely to fix it. The shop should either commit to a dedicated machine or stop taking rotary jobs.
Fixture Repeatability Exposes Weak Buying Logic Fast
A rotary setup that works once is not the same as a rotary process the normal team can repeat. The best pre-purchase question is simple: can the intended setup be repeated by the normal team on a normal day, or does it only work when one experienced person makes it work by feel? If the answer is the second, the buying decision is not mature yet.
This is especially relevant in woodworking and stone fabrication, where material variation already adds enough process noise. A rotary setup that depends on one operator’s judgment about clamping pressure or toolpath retract height will not survive a shift change. The process has to be documented and repeatable before it becomes a production asset.
Consider a stone fabrication shop that wants to machine curved profiles on a rotary axis. The material is natural stone, which varies in hardness, density, and internal stress from slab to slab. A rotary setup that works on one piece may fail on the next because the stone behaves differently. The operator has to adjust feed rates, spindle speed, and clamping pressure on the fly. That is not a production process; it is a craft. The shop can either invest in the process development needed to make it repeatable, or it can accept that rotary work will always be a special project rather than a production line.
The same logic applies to wood. A rotary setup for a cylindrical table leg works fine when the wood is straight-grained and dry. It fails when the wood is twisted, wet, or contains knots. The operator has to compensate for material variation, which means the process is not repeatable. A shop that wants rotary work to be a regular part of its mix has to design fixtures and toolpaths that tolerate material variation, not just one perfect piece.
Programming And Postprocessor Realities
The programming side of a rotary axis is often underestimated. A three-axis machine uses a straightforward Cartesian coordinate system. A rotary axis adds a fourth dimension, and the CAM software has to manage the relationship between linear motion and rotational motion. That relationship is handled by the postprocessor, which translates the CAM toolpath into machine code.
On a retrofit, the postprocessor is often the weak link. The rotary table supplier may provide a generic postprocessor that works for simple jobs but fails on complex ones. The CAM reseller may not have experience with the specific combination of machine and rotary table. The shop ends up debugging postprocessor issues on every new job, which is exactly the kind of engineering friction that a full four-axis machine eliminates.
On a dedicated four-axis machine, the postprocessor is part of the machine package. The builder has tested it against the machine’s actual motion envelope, and the CAM reseller has verified that it produces reliable code. The shop does not have to worry about whether the postprocessor understands the rotary axis; it does, because it was written for that machine.
The programming workflow also differs. On a retrofit, the shop has to manage two coordinate systems: the machine’s native system and the rotary table’s system. On a full four-axis machine, the rotary axis is integrated into the machine’s coordinate system, so the programmer works in one consistent framework. That reduces programming time and, more importantly, reduces the chance of errors.
When The Full Machine Becomes The More Honest Choice
A dedicated four-axis machine usually becomes the more honest answer when:
- The rotary part family is visible in weekly scheduling.
- The current machine loses too much flat-work time to rotary changeovers.
- Fixture and clearance compromises keep costing time.
- Programming stability matters more than low entry cost.
- Management wants one responsible motion package instead of a combined stack.
At that point, the cheaper route may no longer be the cheaper answer. The decision framework is not about which option is more advanced. It is about whether rotary work is occasional enough to extend an existing machine, or frequent enough that the machine should be built around rotary motion from the start. An add-on fourth axis buys access. A full four-axis machine buys a steadier production home.
The cost comparison also changes when the full machine is considered. A retrofit rotary table might cost a fraction of a new machine, but the total cost of ownership includes the engineering hours spent on postprocessor debugging, fixture development, and collision checking. If those hours add up to more than the difference in purchase price, the retrofit is not actually cheaper. It is just cheaper on paper.
There is also the question of resale value. A full four-axis machine is a coherent piece of equipment that can be sold or repurposed if the shop’s needs change. A retrofit rotary table is a collection of parts that may not fit the next machine the shop buys. The retrofit has value only as long as it stays attached to the current machine.
Practical Guidance For The Decision
For shops that are still evaluating whether rotary work will become a regular part of the mix, the add-on route is a reasonable way to test demand without committing to a new machine. For shops that already know rotary jobs are on the weekly schedule, the integrated machine will usually pay for itself in reduced changeover time, fewer clearance headaches, and simpler support. The key is to make the decision based on production frequency, not on the appeal of adding a new capability.
Start by tracking rotary work for a full month. Count the number of rotary jobs, the hours they consume, and the changeover time they require. If rotary work is less than 10 percent of spindle time, the add-on route is probably sufficient. If it is more than 25 percent, the full machine is likely the better investment. Between those numbers, the decision depends on how much flat-work disruption the shop can tolerate and how much engineering time it is willing to spend on a mixed-purpose platform.
Also consider the downstream effects. Rotary work often requires different fixtures, different tooling, and different inspection methods than flat work. A shop that is already stretched thin on fixture design will struggle to support a retrofit. A shop with a dedicated tooling engineer may be able to manage the additional complexity. The decision is not just about the machine; it is about the entire support system around it.
Finally, talk to other shops that have made the same decision. Ask them how often they use the rotary axis, how much time they spend on setup, and whether they would make the same choice again. The answers will be more useful than any specification sheet. The rotary axis is a production tool, and its value is determined by how well it fits into the shop’s actual workflow, not by its technical capabilities on paper.