Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
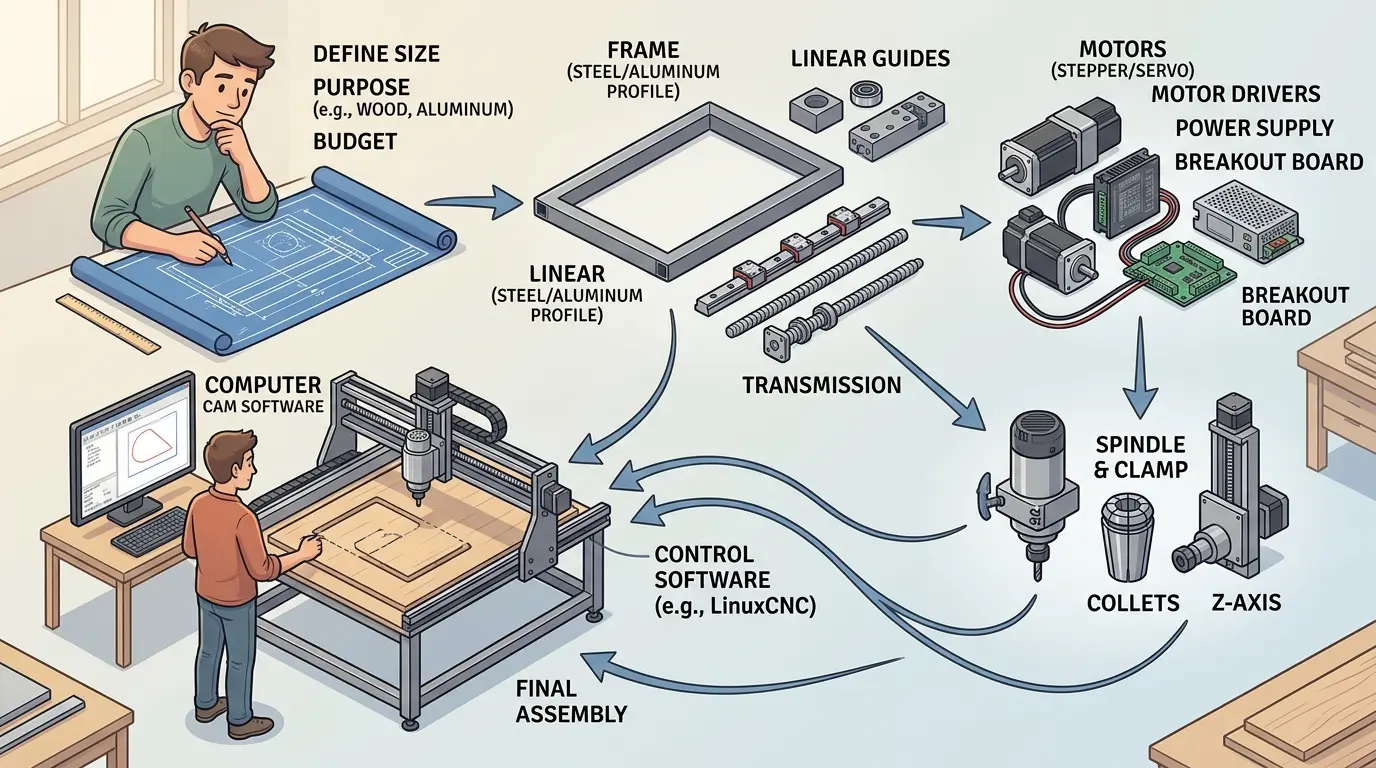
Before you order a single extrusion or spindle, the success of a DIY CNC router build hinges on planning decisions that have nothing to do with the parts list. The article forces builders to confront the real production problem: defining the first three jobs, freezing the machine envelope, and honestly weighing build-versus-buy before committing to a design. This matters because a machine that moves is not a dependable tool. Without early gates on structural stiffness, motion-system maintenance, workholding strategy, and software flow, your build risks becoming a permanent troubleshooting exercise instead of a repeatable production asset.
Start With the Jobs, Not the Parts List
A DIY CNC router project looks straightforward on paper. Frame, rails, drive system, spindle, controller, table, software. The parts list assembles quickly. The hard part comes later, when those components need to behave like one machine with predictable cutting behavior, a reasonable maintenance burden, and a workflow that does not collapse into permanent troubleshooting.
That is why the most important stage of a DIY router build happens before any metal is cut or any extrusion is ordered. Good builds start with design limits, performance gates, and a clear decision about whether the project is meant to teach, to solve a specific format problem, or to replace a purchased machine. When those answers stay vague, the build usually drifts into a machine that can move, maybe cut, but never becomes a dependable tool.
If You Cannot Name the First Three Jobs, Stop Before Ordering Parts
The first planning checkpoint is simple: what will the machine actually be asked to do first?
Not eventually. Not after future upgrades. Not after version two.
What are the first three real jobs the router must complete successfully?
Examples might include:
- Cutting plywood sign blanks,
- Routing plastic templates,
- Surfacing small fixture boards,
- Or producing repeated wood panels in modest quantities.
This question matters because it forces the build away from fantasy and toward performance requirements. If the part family is still vague, then the frame size, spindle logic, motion choice, and hold-down strategy are all at risk of drifting in different directions.
The best DIY routers are rarely the ones designed for every possible future task. They are the ones designed around a narrow set of real early jobs.
Decide Whether You Are Building a Machine or Running a Technical Learning Project
This is the most honest filter in the whole process. DIY CNC can be rewarding for several good reasons:
- Deep technical learning,
- Custom size or layout that off-the-shelf machines do not fit well,
- Staged spending,
- Or simple enjoyment of the build itself.
Those are solid reasons. Weaker reasons usually sound like this:
- DIY Must be cheaper than buying.
- I Need production reliability quickly, but I will build it myself anyway.
- I Can skip hard buying decisions by becoming the builder instead.
The distinction matters because a learning project can absorb slower progress, rework, and redesign. A machine needed for dependable output soon cannot absorb those things as easily. If the real goal is fast, stable production, then the build-versus-buy question needs to be answered early and honestly.
Freeze the Machine Envelope Before You Start Comparing Components
Many builders start shopping components before they freeze the working envelope and material range. That usually creates a mismatched design. A large-format ambition with light structural commitment, or a high-speed expectation with little thought about spindle and workholding interaction, is a common early mistake.
So before comparing rails, screws, belts, or gantry styles, define:
- Maximum practical part size,
- Dominant material types,
- Whether visible finish matters,
- And whether the machine will cut lightly and occasionally or more routinely.
Those answers should define the machine envelope. Once the envelope is fixed, component decisions become much clearer. Without that discipline, the builder often ends up paying for complexity in one area while quietly under-designing another.
Frame Planning Should Begin With Deflection Anxiety, Not Appearance
Frame design is where many first builds go wrong because visual confidence is mistaken for structural honesty. A router frame is not successful because it looks substantial. It is successful because it carries the intended travel and cutting load without constant chatter, flex, or alignment frustration.
That means builders should think first about behavior:
- How Far will the gantry span?
- How Much stiffness is needed for the actual material and cutter strategy?
- How Much mass can the design carry without turning the motion system into a different problem?
- How Will the table and gantry interact over the full working range?
Large unsupported ambition is one of the fastest ways to build a router that looks capable but argues with the operator on real parts.
Motion-System Choices Should Be Made Around Maintenance and Tuning Reality
DIY builders often compare motion components by reputation instead of by the behavior the machine needs over its actual travel. That is risky. Motion design should reflect machine length, expected cut load, acceptable maintenance burden, and the builder’s willingness to align and tune the system properly.
The right question is not which motion option sounds most advanced. It is which one gives the planned machine the best chance of staying predictable after assembly. A slightly less glamorous system that is easier to align, easier to maintain, and easier to recover can create a much better router in practice than a more impressive choice that keeps the build unstable.
Controller Planning Should Happen Before the Mechanical Stack Is Locked
Many DIY builders leave controller and electrical planning too late. That is usually a mistake because the electrical philosophy shapes the whole build. A mechanically promising router can still become a long-term headache if the control path, power planning, grounding, and wiring serviceability were never designed together.
Before the frame is finalized, decide:
- How much wiring complexity you are willing to own,
- Whether the controller should favor learning flexibility or faster stability,
- How serviceable the wiring will be after installation,
- And whether future upgrade ideas are real or just decorative planning.
The machine does not need infinite future flexibility. It needs a control system that matches the first working version honestly. Builders who want a deeper comparison point here should keep in mind the same ownership question that appears in controller buying generally: do you want the electrical layer to disappear quickly, or do you want it to remain part of the experiment?
Plan Dust Control, Safety, and Cleanup Like Core Design Inputs
Dust and safety are often treated like add-ons. That is backwards. A router that creates dust without a real control plan quickly becomes harder to maintain, harder to trust, and less likely to be used consistently. The same applies to emergency-stop logic, enclosure decisions where relevant, cable routing, and basic electrical safety.
This matters even more if the build is supposed to support any commercial work. The machine does not become useful because it can cut once. It becomes useful when it can be run repeatedly without turning cleanup and risk management into separate projects every day.
Workholding Strategy Should Be Designed Before the Table Is Built
DIY builders sometimes treat the table like a passive surface. It is not. The table and hold-down plan decide whether stock loads cleanly, whether parts stay stable, and whether repeat work will be practical or awkward.
Before building the table, decide what hold-down logic the router is really for:
- Clamps,
- Spoilboard-based screw-down work,
- Fixture plates,
- Vacuum ideas,
- Or some deliberate combination.
If that remains vague, the router may still move accurately and still feel slow and frustrating in daily use. That is because workholding problems are often what make a home-built machine feel unfinished long after the mechanics are assembled.
Software Flow Must Be Planned Before You Call the Build Finished
A DIY router is not close to complete just because the axes move under power. The real machine includes the design-to-toolpath workflow, the postprocessor behavior, the tool library logic, the zeroing routine, and the operator steps needed to run a job without confusion.
Builders should define early:
- What CAD/CAM path they will use,
- How work offsets and zeroing will be handled,
- How tools will be named and managed,
- How the first test jobs will be validated,
- And who will maintain process discipline if the machine is shared.
Without that layer, many builds reach mechanical completion and then stall in software uncertainty.
Build-Versus-Buy Needs a Real Decision Gate, Not a Last-Minute Panic
One of the smartest things a builder can do is set a pre-build gate for the build-versus-buy question. If the machine is supposed to support revenue soon, if tuning time is limited, or if support and recoverability matter more than customization, then buying may be the more disciplined move.
That is especially true once time and delayed productivity are priced honestly. Teams at this point should compare the hidden responsibilities of building against the visible cost of buying. It often helps to compare CNC machinery quotes line by line so the purchased alternative is judged fairly.
And if the intended workload is already drifting toward broader sheet processing or more industrial routing expectations, the better answer may be to review the Pandaxis machinery lineup rather than force a DIY design to carry a production role it was never meant to absorb.
The Strongest DIY Builds Usually Have Narrow Success Criteria
The best home-built routers usually succeed because the builder defined success tightly. They are not trying to do everything. They are trying to do one family of work well enough to justify the machine.
That is the real planning lesson. Narrow success criteria protect the design. They tell the builder what matters first, what upgrades can wait, and what compromises are acceptable. A router meant to cut signs cleanly is a different project from a router meant to process moderate sheet goods, and both are different from a router meant mainly to teach CNC integration.
When the success definition is narrow, the machine has a chance to become coherent. When the success definition is broad, the machine often becomes a permanent version-one prototype.
Plan the Whole Stack Before You Order the First Structural Part
The safest build sequence is to plan the mechanical, electrical, and operating stack together. That means deciding on target materials, acceptable chatter and finish, motion strategy, spindle logic, table concept, controller philosophy, safety approach, dust handling, and basic software flow before hardware buying starts.
That discipline does not make the build simple. It makes the problems appear in planning instead of appearing later during expensive rework. And that is usually the difference between a router that reaches stable use and one that reaches motion, then lives in endless refinement.
What to Plan Before You Start
That is the practical answer to the title.
Before building your own CNC router, plan:
- The first real jobs,
- The real reason for building,
- The exact machine envelope,
- The structural behavior you need,
- The motion and controller philosophy you can maintain,
- The hold-down method,
- The dust and safety strategy,
- The software workflow,
- And the point at which buying becomes the smarter path.
When those decisions are made early, a DIY router can become a focused, satisfying project with a real chance of stable use. When they are postponed, the machine usually becomes a long troubleshooting exercise disguised as progress.
Match the Spindle and Tooling to the Material, Not to the Motor Spec
The spindle selection is one of the most common places where DIY builds drift toward disappointment. Builders often compare horsepower ratings or maximum RPM figures without thinking about what those numbers mean for the actual cuts they plan to make. A spindle that spins fast but lacks torque at cutting speed will struggle through dense materials, while a low-speed spindle with high torque may be overkill for light engraving work.
Before choosing a spindle, define the cutting conditions the machine will actually see:
- The hardest material you will cut regularly, not occasionally,
- The typical depth of cut per pass,
- The cutter diameters you expect to use most often,
- And the acceptable surface finish for the parts that leave the shop.
These answers determine whether a trim router, a brushless spindle, or a larger air-cooled unit makes sense. They also determine collet sizing, tool change frequency, and whether you need variable speed control or can live with fixed RPM. Builders who skip this step often end up with a spindle that either bogs down on real jobs or runs so hot that duty cycle becomes a daily constraint.
Plan for the First Test Cuts Before the Machine Is Assembled
A surprising number of DIY builds reach mechanical completion and then stall because the builder has no clear idea how to validate the machine. The first test cuts should be planned in advance, with specific acceptance criteria that match the intended work.
A sensible test sequence looks something like this:
- Cut A simple rectangular pocket in soft material to verify axis squareness and backlash behavior.
- Cut A circle to check for ovality, which reveals axis scaling or calibration issues.
- Run A repeated shallow pass over the same path to confirm dimensional stability across multiple cycles.
- Cut A part from the actual target material at reduced feed rates, then gradually increase speed while monitoring finish quality.
Each of these tests tells you something specific about the machine. The pocket test reveals mechanical alignment. The circle test exposes calibration drift. The repeated pass test shows whether the machine holds position over time. The material test confirms whether the spindle and feed strategy work together. Without these gates, builders often discover problems only when they cut a real part and cannot tell which subsystem caused the defect.
Understand the Failure Modes That Will Actually Bother You
Every DIY router has predictable failure modes, and knowing them in advance changes how you design the build. The most common ones are not dramatic mechanical failures. They are slow, frustrating behaviors that erode confidence in the machine.
Chatter and vibration are the first failure mode most builders meet. They usually trace back to insufficient frame stiffness, loose connections, or aggressive cutting parameters. The fix is rarely a single component change. It is usually a combination of structural stiffening, feed rate adjustment, and spindle speed matching.
The second failure mode is lost steps or position drift. This often appears as parts that are slightly wrong in one axis, or as a machine that slowly walks out of alignment during long jobs. The causes range from inadequate motor sizing to loose couplings to acceleration settings that exceed what the mechanics can handle.
The third failure mode is the one builders least expect: inconsistent surface finish that changes from one part to the next. This usually points to workholding movement, tool wear, or thermal drift in the spindle. It is hard to diagnose because the machine appears to work correctly, but the parts tell a different story.
Planning for these failure modes means designing the build so that each one is diagnosable. That means accessible connections, visible indicators on the motion system, and a table design that makes workholding problems obvious rather than hidden.
Budget for Consumables and Maintenance, Not Just the Build
DIY builders often plan the purchase budget carefully and then ignore the operating budget. That is a mistake because the ongoing costs of a router are real and predictable. Bits wear out, spoilboards need surfacing, dust filters need replacing, and alignment checks take time.
A practical operating budget includes:
- Replacement cutter costs based on the materials you cut most often,
- Spoilboard material and surfacing time,
- Dust collection filter maintenance,
- Lubrication and cleaning supplies for the motion system,
- And a reasonable allowance for the occasional replacement part.
Builders who ignore these costs often find that the machine sits idle because running it feels expensive. The router becomes a tool that is technically functional but practically unused. Planning the operating budget before the build keeps the machine in service after the excitement of assembly fades.
Decide How Much Tuning You Are Willing to Own
Every CNC router needs tuning, but DIY machines need more of it than purchased ones. The builder owns the alignment process, the acceleration tuning, the backlash compensation, and the ongoing adjustments that keep the machine cutting accurately.
This is not a one-time effort. Temperature changes, material variations, and normal wear all shift the machine’s behavior over time. A builder who enjoys this process will find the machine rewarding. A builder who wants to cut parts will find it exhausting.
The honest question is not whether you can tune the machine once. It is whether you will still be willing to tune it six months from now, when the novelty has worn off and the machine needs attention before a deadline. If the answer is no, that is a strong signal that a purchased machine with factory support may be the better path.
Keep the Upgrade Path Honest and Limited
DIY builders often plan for upgrades that never happen. The machine will get a bigger spindle later. The motion system will be upgraded to a different drive type. The table will be replaced with a vacuum system. These plans feel productive, but they usually just add complexity to the initial design.
A better approach is to design for the first working version and only accommodate upgrades that are genuinely likely. That means asking which upgrades are realistic within the next year, which ones the machine structure can actually support, and which ones would require rebuilding the machine anyway.
Most upgrades that require structural changes are not upgrades at all. They are new machines. Planning for them during the initial build usually means compromising the first version to accommodate a future that may never arrive. Build the machine you need now, and let the next machine be a separate decision.