Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
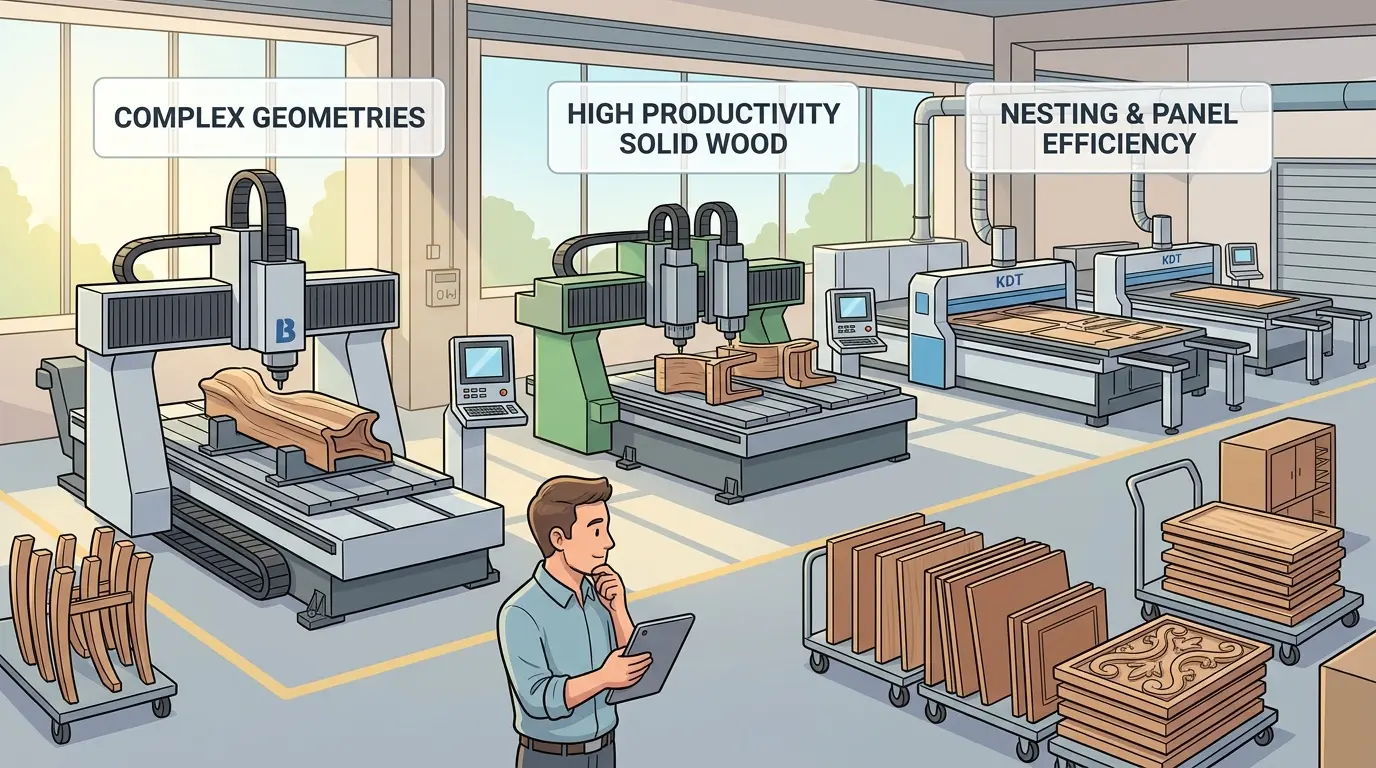
Comparing Busellato, Bacci, and KDT as interchangeable prestige options is a costly mistake for any woodworking plant. These machine families embody distinct production philosophies, and the real decision hinges on your factory’s bottleneck, workflow logic, and three-to-five-year direction. Before evaluating specifications, your buying team must define whether you run a panel-furniture line, a shaped-component shop, a high-mix custom operation, or an expanding system. That classification determines whether you judge line handoffs, geometry and fixturing, changeover discipline, or integration path—and it prevents a respected brand from becoming a poor fit for your actual production reality.
Three Brands, Three Different Production Philosophies
When Busellato, Bacci, and KDT appear on the same shortlist, it is tempting to treat them as interchangeable options differentiated mainly by price and prestige. That approach leads to expensive mismatches. These three names represent distinct machine families with different design priorities, and each one aligns with a different kind of woodworking operation.
The practical question is not which brand has the stronger reputation. It is which machine family matches the production logic of your plant, the bottleneck you are trying to eliminate, and the direction your factory is heading over the next three to five years.
Define the Factory Type Before Comparing Machines
A CNC machining center is not a universal tool. It is a production station that either fits your workflow or fights it. Before evaluating any of these brands, the buying team needs to agree on what kind of plant they are actually running.
- A panel-furniture plant processes sheet goods through sizing, nesting, drilling, edging, and assembly. The CNC center is one link in a chain, and its value depends on how well it coordinates with the stations around it.
- A shaped-component or solid-wood factory produces curved parts, chair components, stair parts, doors, frames, and joinery-heavy work. The CNC center carries more of the production burden, and its value depends on geometry capability and fixture practicality.
- A high-mix custom shop handles short runs, frequent changeovers, and constantly shifting part dimensions. The CNC center must be forgiving of variability and quick to reconfigure.
- An expanding factory is buying more than a machine. It is funding a production system, and the equipment decision must support future integration rather than just immediate output.
When the buying team skips this step, the shortlist becomes a source of confusion. One manager compares routing speeds. Another compares drilling accuracy. Another is thinking about line automation. The same brand name means different things to different people, and the decision process gets noisier than it needs to be.
Panel-Furniture Plants: Judge the Handoffs, Not Just the Machine
For cabinet, wardrobe, office furniture, and other panel-based production, the CNC machining center is rarely the actual constraint. The constraint is usually the handoff between stations. Panels move from the panel saw to the nesting machine, then to drilling and boring, then to the edgebander, and finally to assembly. If any of those handoffs is unstable, the CNC center cannot compensate for it.
Panel-furniture buyers should ask line-level questions before brand-level questions:
- Where does material queue up during a typical production day?
- Which station creates rework that downstream stations inherit?
- Is routing the real problem, or is drilling alignment the problem?
- Is the plant trying to reduce labor at one station while leaving another bottleneck untouched?
- Will the new machine improve flow across the chain, or will it simply create a faster local island?
For a panel plant, the right brand fit is the one that strengthens the weakest handoff. A respected name cannot fix a line that still delivers unstable parts to the next station. The machine may be excellent in isolation, but if it does not coordinate with the surrounding process, the factory will not capture the expected gain.
Shaped-Component and Solid-Wood Plants: Evaluate Geometry and Fixturing
Factories that produce shaped components, curved panels, chair parts, stair stringers, door frames, and other non-rectangular work should not evaluate this shortlist through a panel-furniture lens. Their decision criteria are different.
These plants need to ask:
- How well does the machine family handle the geometry the shop actually sells?
- How manageable are the fixturing demands for typical parts?
- Can the programming workflow stay practical when part geometry varies significantly?
- Will operators spend their time machining parts or interpreting complex setups?
This is where the same three brands can mean very different things to different factories. A panel-focused team sees the shortlist as a throughput conversation. A shaped-part plant sees it as a complexity-management conversation. Both perspectives are rational, but they are not comparing the same thing.
The evaluation should stay tied to the part family. If the work depends on shaped geometry and varied setups, the brand fit should be judged by process suitability. A machine that excels at high-speed panel processing may be the wrong choice for a shop that needs flexible fixturing and adaptable programming for irregular parts.
High-Mix Factories: Price the Cost of Changeover
Some woodworking plants win through flexibility rather than long repeated runs. They handle mixed dimensions, project-by-project batches, irregular schedules, and product variation that keeps operators switching context throughout the day. In these environments, automation only pays when it removes the right kind of friction.
High-mix buyers should ask whether the machine family helps the plant:
- Transition between jobs cleanly without excessive setup time
- Keep setups understandable for multiple operators, not just one specialist
- Reduce the penalty of part variation
- Stay productive when batch sizes are small
This is one of the easiest places to overspend. Buyers see more automation and assume it must represent a better answer. But if the factory changes jobs frequently, some forms of automation do not pay back the way they do in longer repeated runs. In a high-mix shop, the better brand fit may be the one that supports disciplined flexibility rather than the one that assumes stable, repetitive flow.
The wrong purchase in this environment often looks impressive during a factory visit and frustrating after installation. The machine may be technically capable, but the daily routine becomes too heavy for the variation the shop actually handles.
Factory Stage Changes the Evaluation Criteria
Woodworking factories at different stages of development need different things from the same shortlist.
| Factory Situation | Best Comparison Lens | Buying Mistake To Avoid |
|---|---|---|
| Growing Panel Shop | Line balance, drilling coordination, edging and routing handoff | Comparing only the flagship machining center without considering surrounding stations |
| Shaped-Part Producer | Geometry fit, fixture logic, and programming practicality | Judging the shortlist with sheet-processing assumptions |
| Mixed Custom Plant | Changeover discipline, operator clarity, and flexibility | Buying automation that only pays in long repeated runs |
| Expanding Factory | Integration path, support model, and future workflow coherence | Treating the decision as a one-machine beauty contest |
This framework separates a close shortlist more effectively than prestige language alone. It forces the buying team to state clearly what stage of plant development the investment is actually funding.
It also helps with internal alignment. Production managers, owners, engineers, and operators often attach different hopes to the same brand names. Once the plant agrees whether the project is mainly about throughput, complexity handling, flexibility, or system-building, those preferences become easier to test against reality.
Service Geography and Training Reality Break Ties
When the machine directions look close on paper, service reality often decides the outcome. Buyers should compare not only the equipment but the support conditions around it:
- Who commissions the machine, and how much production time is lost during installation?
- How is operator training delivered, and does it cover the specific part families the shop runs?
- How quickly can routine faults be clarified without waiting for remote diagnosis?
- How are spare parts accessed, and what is the realistic lead time?
- How much of the recovery burden stays inside the factory?
This matters because factories rarely lose output through one dramatic failure alone. They lose it through repeated small delays, weak training carryover, unclear troubleshooting ownership, and slow recovery from problems that should have been routine.
A famous name can still be the wrong choice if the support reality in the buyer’s region is thin. Better paper fit can be overwhelmed by weak commissioning, shallow training, or too much dependence on remote guesswork after installation. Brand fit is local as much as it is technical.
Replacement Purchase or System Decision?
Some woodworking purchases are simple replacements. Others are really production-logic decisions. The shortlist should not be judged the same way in both cases.
If the plant is replacing one machine in a stable surrounding process, stand-alone fit may be enough. The question can stay close to the station: which option covers the same job better, more reliably, or with better labor economics?
If the factory is moving toward cleaner line flow, more connected production, reduced handling, tighter traceability, or more disciplined handoffs between stations, the brand decision should be judged as part of a broader system move. In that case, the badge matters less than whether the equipment direction supports the next stage of factory organization.
This is where many brand debates drift. The team discusses features as if the project were a replacement when the real goal is process redesign. Or it discusses grand factory transformation when the current need is only a reliable station upgrade. The more honestly buyers separate those two project types, the faster the shortlist clarifies.
Adjacent Equipment Affects the CNC Decision
A woodworking CNC purchase almost never lives alone in the production story. The stations around it determine whether the machine delivers its full value. A strong machining or routing center can still underperform in business terms if the next station remains slow, inconsistent, or difficult to balance.
That is why adjacent equipment still matters in the brand discussion. A plant may need to think alongside the shortlist about wide belt sanders or other nearby stages if finish quality, calibration, or downstream readiness remain weak. In panel and batch environments, the biggest output gain may come not from the flashiest CNC purchase but from the combination of better upstream and downstream coordination.
This is also why many buyers benefit from stepping back and reviewing the Pandaxis machinery lineup when the project is really about plant balance, not just one machine class. The question becomes less about who wins the brochure comparison and more about which direction makes the entire cell easier to manage.
Five Questions Every Buying Meeting Should Answer
Before a woodworking factory lets brand preference harden into a purchase, the team should be able to answer five practical questions clearly:
- What exact bottleneck is this investment supposed to remove?
- What factory type are we really optimizing for: panel throughput, shaped-part capability, high-mix flexibility, or system expansion?
- Which surrounding stations will limit the value of the upgrade if they remain unchanged?
- What support, training, and recovery conditions actually exist in our region?
- Are we buying a stronger stand-alone machine or funding a new production logic?
If those answers remain vague, the shortlist is not ready no matter how well the vendor conversations are going. Clear brand comparison depends on clear plant intent.
The Brand That Removes Your Actual Bottleneck
Busellato, Bacci, KDT, and similar names become much easier to evaluate once reputation is pushed into the background and workflow is pushed into the foreground.
Panel-furniture plants should judge line handoffs. Shaped-component plants should judge geometry fit and fixture logic. High-mix factories should judge changeover discipline. Expanding factories should judge integration path and support reality. Once the plant defines its type, its bottleneck, and its real support conditions, the shortlist usually separates much faster.
The right brand is not the one that sounds best in a general woodworking conversation. It is the one that removes the bottleneck your factory actually has and still makes sense to own where you operate.