Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
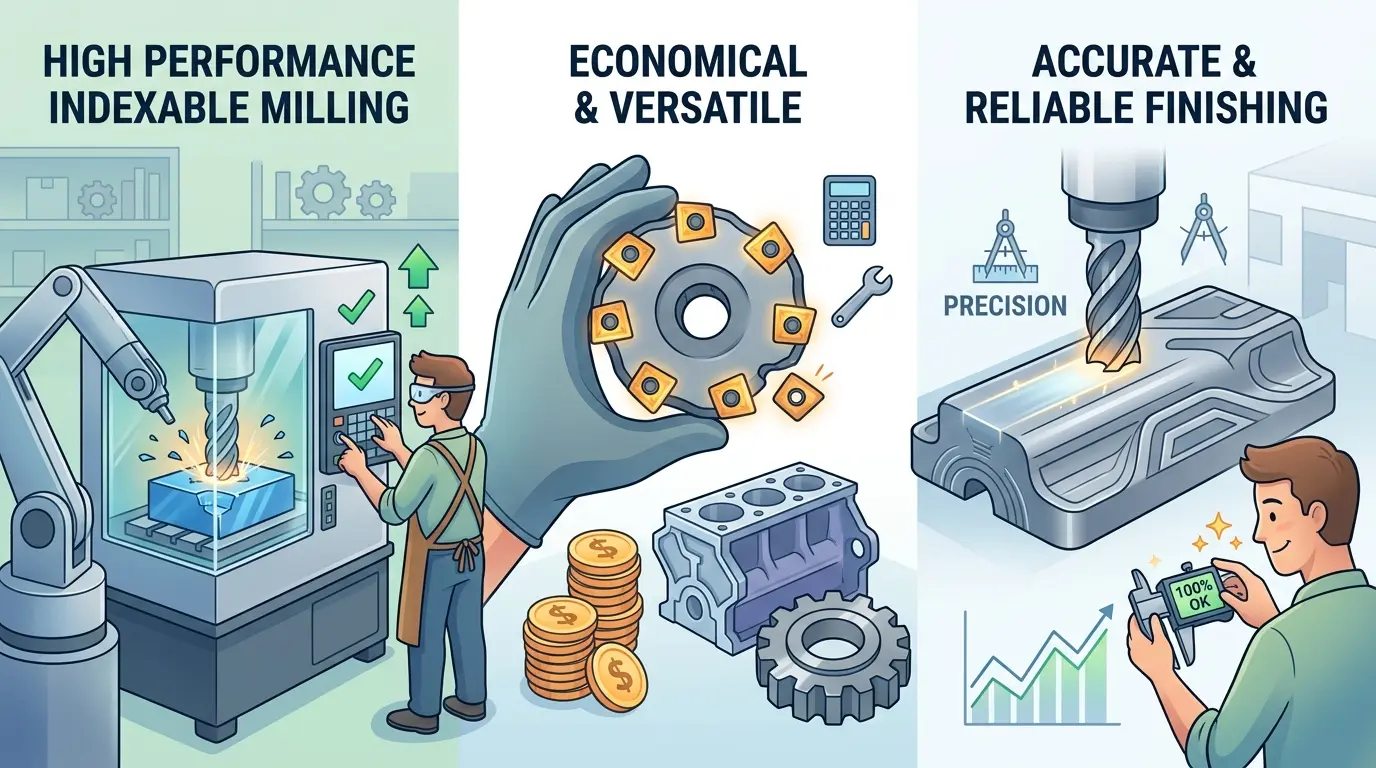
An indexable face mill like the CoroMill 200 gets recommended when a shop needs to clear broad surfaces efficiently, but the name alone tells you nothing about whether your spindle, holder, and workholding can actually carry the load. Too many shops commit to a cutter diameter and insert geometry before verifying that the machine-tool-fixture stack stays stable under that depth of cut and feed rate. The decision that matters is application fit: matching cutter size, insert grade, and stock-removal strategy to your actual machine rigidity, material condition, and batch economics. Evaluate the system on representative work, not catalog reputation, or you will trade predictable production for chatter, chipped inserts, and a washboard finish.
Why the CoroMill 200 Name Keeps Appearing in Milling Discussions
The CoroMill 200 name surfaces in a very specific conversation: face milling with indexable inserts. A programmer mentions it when a large flat surface needs material removed efficiently. A tooling representative recommends it when a job demands consistent edge management across repeated production runs. But the name alone does not tell you whether the cutter will work on your machine, with your material, or against your finish requirements.
Treat the name as a starting point for evaluation, not as a verdict on suitability. The real question is whether an indexable face-milling system fits the production situation you actually have on the floor. That question requires looking at machine capability, insert geometry, workholding, and the economic model behind the tooling decision.
What an Indexable Face Mill Is Designed to Deliver
An indexable face mill uses a cutter body with replaceable inserts rather than a solid tool that gets discarded when the edge wears. Shops choose this approach when they need one or more of the following:
- Controlled metal removal across a broad surface area
- Predictable edge replacement instead of full tool replacement
- Lower per-part tooling cost over repeated production
- Better economics than consuming large solid cutters in the same role
- Consistent behavior across recurring surfacing operations
Those benefits are real, but they only materialize when the machine and the job support them. The cutter does not create stability on its own. It is a component in a system that includes the spindle, the holder, the workpiece, and the operator’s ability to manage the process.
The Machine Has to Carry the Cutter Honestly
Many poor tooling decisions start when a shop hears a respected cutter name and forgets that the machine still has to handle the load. Cutter diameter, spindle power, rigidity, holder condition, setup stability, and the actual cutting envelope all determine whether the tooling family behaves as intended.
On a rigid machine with a stable setup and a sensible insert strategy, an indexable face mill becomes a reliable production tool. On a lighter machine or a weak setup, the same approach can turn into a vibration source, a finish problem, or a story about inserts disappearing faster than expected.
Consider a common scenario: a 40-taper vertical machining center with a 15-horsepower spindle and a worn drawbar. The shop wants to face a 12-inch square plate of 4140 pre-hard. The programmer selects a 4-inch indexable face mill because that is what the tooling catalog recommends for the material. The first pass sounds fine. The second pass starts to chatter. By the third part, the inserts are chipped and the surface finish looks like a washboard.
The cutter did not fail. The machine could not support the cutter’s demands at that diameter, depth of cut, and feed rate. A smaller cutter, a lighter depth of cut, or a different insert geometry might have worked. But the shop committed to the name before checking the machine’s actual behavior under load.
The cutter does not adapt to the machine. The machine has to support the cutter.
Name Recognition Is Not Application Proof
Recognized tooling names give shops a shared reference point. They become dangerous when they are treated as evidence of fitness. A cutter family may be widely trusted across the industry, but the question remains local: what is happening on this machine, on this material, on this part, at this depth of cut, with this finish expectation?
Experienced programmers treat the name as an entry point, not a conclusion. They still verify the application details before committing to a tooling strategy. They ask about the machine’s spindle taper, the holder condition, the workholding method, and the actual stock condition on the incoming material.
The Production Questions That Sit Under the Cutter
Before deciding that a CoroMill 200 style solution makes sense, clarify the following:
- Is the work mainly broad face milling, step surfacing, or general-purpose milling where another cutter style might compete?
- Is stock removal the primary priority, or is surface finish the primary priority?
- How rigid is the machine-tool-fixture stack?
- How often will inserts be consumed, changed, stocked, and tracked into the workflow?
- Does the batch size justify the discipline required to manage an insert system?
These questions matter more than the name because they reveal whether the cutter actually addresses the production bottleneck. A shop that runs 500 identical castings a month has a different relationship with tooling than a job shop that faces a different material every week.
Tooling Economics Are About the Whole System
Indexable cutters attract attention for economic reasons. Replaceable inserts protect the cutter body and make edge changes faster than replacing a solid tool. But tooling economics are never only about the price of an insert. They include setup time, cutter stability, surface consistency, operator confidence, spare insert availability, stock management, and the cost of troubleshooting when the machine does not really suit the cutter.
A tooling choice that looks efficient in a catalog can still be inefficient on the floor. The catalog shows the insert price. The floor shows the total cost.
Let’s walk through a realistic comparison. A shop faces a 10-inch square block of aluminum on a 3-axis mill. They have two options: a 3-inch indexable face mill with four inserts per body, or a 2-inch solid carbide end mill with a wiper flat. The indexable cutter removes material faster per pass, but each insert costs a certain amount and the cutter body requires a specific holder. The solid end mill costs more upfront but can be re-ground or used for profiling after the facing operation.
The decision is not simply “indexable is cheaper per edge.” It is about how many parts the shop runs, how much setup time each tool change costs, and whether the solid end mill can serve double duty. A shop that runs 20 parts a month may never recover the cost of the indexable cutter body. A shop that runs 2,000 parts a month will likely see the indexable system pay for itself quickly.
A Fit Table to Keep the Discussion Honest
| Situation | Likely Value of an Indexable Face-Milling System | Common Risk |
|---|---|---|
| Repeated facing on stable machines | Good insert economy and predictable edge management | Shops may over-size the cutter |
| Broad surfacing with decent spindle stability | Strong production logic if the insert strategy is right | Finish issues if vibration is ignored |
| Light machines or long overhang setups | Limited benefit unless cuts stay conservative | Chatter and wasted inserts |
| Mixed low-volume work | Value depends on setup frequency and insert control discipline | Name recognition replaces real evaluation |
The table does not prescribe one answer. It forces application fit back into the conversation. A shop with a light-duty benchtop mill should not expect the same results as a shop with a 50-taper horizontal machining center. The cutter family may be identical, but the production reality is completely different.
Insert Strategy Matters Almost as Much as Cutter Choice
Even when the cutter family is appropriate, the shop still has to manage insert selection intelligently. Different materials, interruption levels, finish expectations, and production goals do not all want the same edge behavior. A stable cutter body cannot rescue a poor insert choice, just as a good insert cannot rescue a badly matched machine.
Consider the difference between facing a continuous block of mild steel and facing a casting with sand inclusions or interrupted cuts from cored holes. The continuous cut allows a sharper, more positive insert geometry that produces a better finish. The interrupted cut demands a tougher edge geometry that can withstand impact without chipping. Using the same insert for both applications will produce mediocre results in at least one of them.
The same logic applies to material families. Aluminum wants a high-positive rake angle and a polished flute surface to prevent built-up edge. Stainless steel wants a tougher substrate and a stronger edge hone to resist work hardening. Cast iron wants a different grade entirely, often with a coating designed for abrasive wear. A shop that stocks one insert grade for everything will spend more time troubleshooting than cutting.
Strong tooling decisions are written in application language, not merely in product names. The team should know why that insert strategy exists, not only what the catalog code says.
Face Milling Success Depends on Entry Conditions and Support
A face-milling tool lives inside the rest of the setup. Entry conditions, workpiece support, stock condition, workholding strength, and machine response all affect whether the cutter works cleanly. Shops sometimes blame a tooling family for inconsistent results when the bigger issue is unsupported plate stock, poor clamping, or a machine that does not stay calm under the chosen cut.
Take a typical example: a shop faces a 1/2-inch thick aluminum plate that is clamped only at the edges. The center of the plate flexes under the cutter’s downward force. The surface finish looks acceptable near the clamps but shows vibration marks in the middle. The operator blames the inserts. The real problem is that the plate needs a sacrificial backing plate or a vacuum fixture to support the center.
Tooling evaluation should happen with setup evaluation at the same time. They are not separate problems. A cutter that performs poorly on a flimsy setup may perform perfectly once the workholding is corrected. Conversely, a cutter that works well on a rigid setup will chatter immediately on a weak one.
Prototype Work and Production Work Judge the Same Cutter Differently
In prototype work, the shop may care more about flexibility and getting the surface generated safely than about perfect insert economy. In production work, priorities shift toward repeatability, predictable insert life, surface consistency, and operator-friendly changeover. A cutter choice that feels acceptable in prototype mode may become weak in production if insert handling or machine stability proves too sensitive.
A cutter that shines in production may feel excessive for occasional one-off work if the shop rarely uses it enough to justify disciplined insert management. The prototype shop might be better served by a solid carbide end mill that can be used for multiple operations. The production shop needs the indexable system because it runs the same facing operation hundreds of times per month.
Why Buyers and Managers Often Misread Tooling Conversations
Managers sometimes hear a recognized tooling name and assume it means the process is technically mature. Not necessarily. Sometimes it only means the shop has adopted familiar tooling language. The mature process is the one that can explain cutter choice in terms of machine fit, insert strategy, process stability, and measured results.
That distinction matters when management reviews cycle time claims or tooling cost proposals. The name should never become a substitute for application evidence. A manager who asks “why this cutter and not another?” is doing the right thing. A manager who accepts “because it is a CoroMill 200” without further explanation is not.
The Best Test Is a Real Representative Trial
The honest way to evaluate a cutter family is not on a showroom demo or an unusually easy material sample. It is on representative work. The trial should examine insert life, vibration, surface finish, spindle behavior, operator ease of use, and whether the result remains stable after several edges rather than only the first one. If the tool behaves well only under ideal conditions, the shop has learned something important.
A real trial also exposes whether the cutter is solving the job or merely making the job sound more sophisticated. Run the cutter on the actual material, at the actual depth of cut, with the actual workholding. Measure the surface finish with a profilometer. Track insert wear after each edge. Compare the results against the current tooling method. Only then does the shop have data to make a decision.
Insert Inventory Discipline Often Decides the Economics
Indexable tooling promises are frequently won or lost in inventory behavior rather than at the spindle. If inserts are poorly tracked, mixed across applications casually, or replaced only after quality has already drifted, the shop may never realize the economic benefit that justified the tooling system in the first place. By contrast, a shop that tracks usable edges, change intervals, and application-specific insert behavior usually gets a much clearer picture of whether the cutter family is earning its place.
Many tooling conversations focus only on catalog efficiency. Real production efficiency includes whether operators can identify the right insert quickly, whether replacements are stocked intelligently, and whether the team can tell the difference between predictable wear and a setup problem.
A practical approach is to assign each insert grade a specific location in the tooling cabinet, label it clearly, and record which applications use which grade. When an operator reaches for an insert, they should know exactly what they are getting and why. If the shop runs multiple materials, the insert selection should be part of the setup sheet, not left to operator memory.
A Famous Cutter Still Loses If the Machine Wants Something Simpler
A respected indexable face mill can still be the wrong answer on a lighter or less stable machine. In some shops, a more conservative cutter size or even a different cutter concept may deliver calmer results, better finish, and less frustration. That is not a failure of the famous tool family. It is a reminder that tooling should fit machine behavior instead of demanding that the machine imitate a stronger platform than it really is.
The smartest shops are comfortable reaching that conclusion because they care more about stable output than about using the most recognizable name in the tooling cabinet. They would rather run a smaller cutter at a consistent depth of cut than fight chatter with a larger cutter that the machine cannot handle.
Documentation Prevents Tool Names from Becoming Shop Lore
When a cutter family proves itself, the logic should be documented. What material was it used on? What machine class? What finish target? What kind of stability? What insert behavior was acceptable? Without that documentation, the shop can easily turn one successful use into fuzzy folklore and start applying the same tool where it no longer belongs.
This is a common problem in growing CNC operations. A respected tool becomes a default answer instead of a justified answer. The solution is a simple tooling database or even a spreadsheet that records application parameters, insert grades, and measured results. When a new job comes in, the programmer can search for a similar application and start from a proven baseline instead of guessing.
What Machine Buyers Should Learn from Tooling Names
Tooling names often reveal the type of machine workload a shop is trying to support. If buyers keep hearing strong face-milling language in discussions about process capability, they should translate that into machine questions about rigidity, spindle stability, table support, and how production value is actually being created.
That is also why it helps to think about industrial CNC equipment in terms of what production gains are truly worth paying for instead of treating every recognized tooling reference as automatic proof of process strength. A machine that cannot hold a stable cut will undermine even the best tooling. A machine with adequate rigidity and spindle power will make the tooling decision much easier.
Read the Name as a Tooling Clue, Not a Final Answer
CoroMill 200 is useful because it gives shops a reference point for indexable face-milling logic. But the right purchasing and process decision still lives one level deeper, in application fit. Machine stiffness, insert economics, workload type, surface demands, and setup honesty decide whether a named cutter family delivers real value.
The product name can open the conversation, but the job, the machine, and the economics still have to close it. Start with the production problem, evaluate the machine’s real capability, test on representative work, and document the results. That process will tell you whether an indexable face mill belongs in your tooling strategy, regardless of which name is on the cutter body.