Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
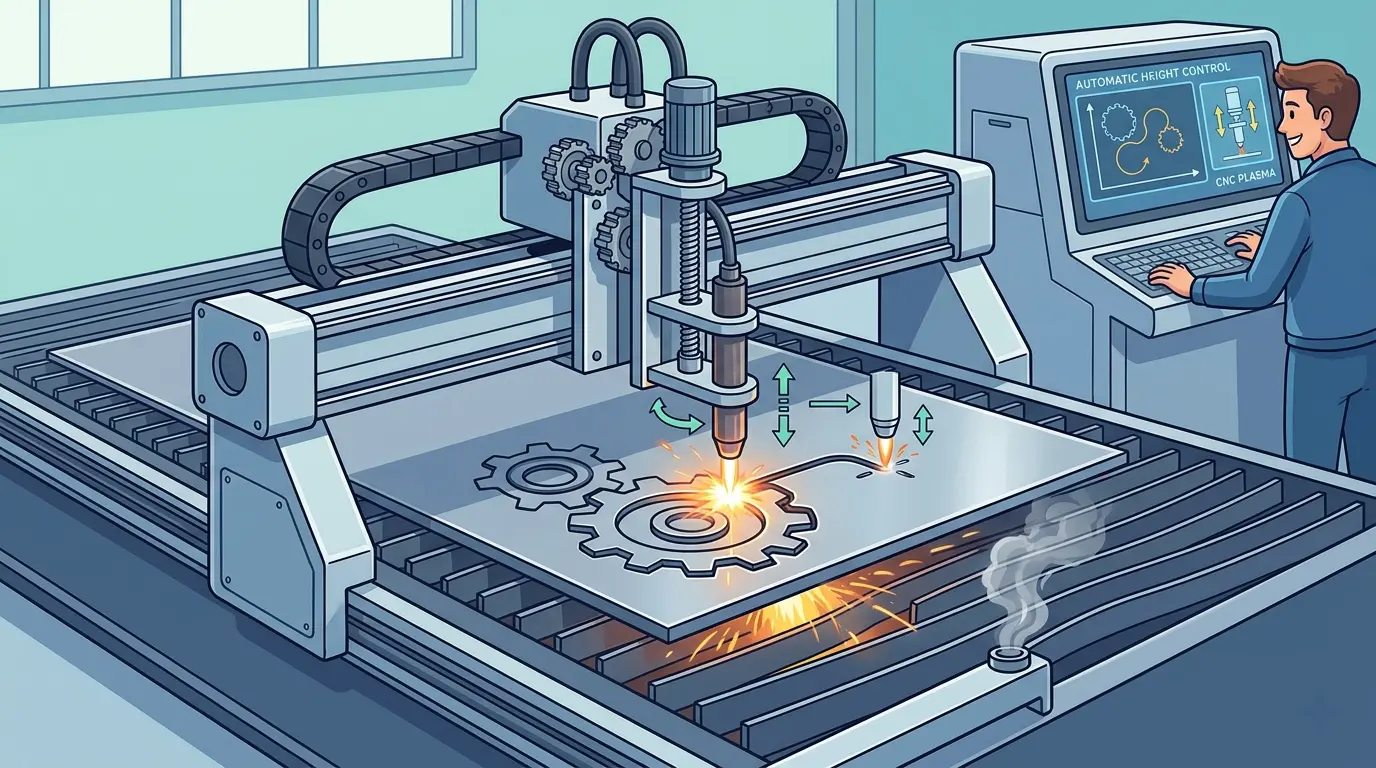
Plasma tables can position the torch precisely across X and Y axes yet still deliver inconsistent cuts when the torch-to-work distance drifts or is never properly established. That vertical positioning falls to the torch lifter, a subsystem buyers often dismiss as a minor accessory until underspecification shows up as poor cut quality, shortened consumable life, and operators babysitting the machine instead of running production. This article examines how torch height control works across piercing, edge starts, and steady-state cutting, and why evaluating this mechanism as part of process stability—not an isolated feature—determines whether a table earns its keep on real shop-floor material.
Why Torch Height Control Decides Whether a Plasma Table Earns Its Keep
A CNC plasma table can position the torch perfectly across X and Y axes and still produce inconsistent cuts. The reason is usually the same: the torch-to-work distance was wrong, drifted during the cut, or was never properly established in the first place.
That vertical positioning is the job of the torch lifter. On a CNC plasma table, the torch lifter is the mechanism that raises and lowers the torch so the cutting height can be set and corrected during operation. Buyers will often see the terms torch lifter and torch height control used together, and while they are related, they are not strictly the same thing. The practical distinction matters less than what the system actually does on the shop floor.
If torch height is unstable, cut quality degrades, consumable life shortens, and the operator ends up babysitting the machine instead of running production. Understanding how this subsystem works—and what happens when it is underspecified—can save a shop from buying a table that looks good in a quotation but struggles in daily use.
The Torch Lifter Manages Distance, Not Just Motion
It is easy to dismiss the torch lifter as a minor accessory because it only adds vertical motion to the gantry. In practice, it controls one of the most sensitive variables in plasma cutting: the gap between the nozzle and the material.
Plasma cutting is not tolerant of sloppy height behavior. If the torch rides too high, the arc loses focus, cut quality weakens, and the kerf widens. If the torch runs too close, the nozzle can contact the workpiece, consumables wear faster, and the process becomes unstable. The torch lifter exists to keep that distance under control instead of leaving it to manual adjustment and guesswork.
On a table with a well-designed lifter, the torch moves smoothly and responds quickly to changing conditions. On a table with a weak or poorly integrated lift system, the operator spends time correcting height manually, re-cutting parts, or replacing consumables that should have lasted longer.
Why Height Changes During Real Cutting
A flat CAD file does not guarantee a flat cutting situation. In real production, the torch-to-work distance changes because:
- Sheet or plate may not sit perfectly flat on the table.
- Material thickness and condition vary from one job to the next.
- Table supports and slats wear, sag, or shift over time.
- Heat buildup during longer runs can cause localized distortion in the material.
None of these conditions are exotic. They are normal shop-floor realities. That means the torch cannot simply be parked at one fixed height and left alone. The process needs a way to position the torch correctly at the start of the cut and maintain a workable separation as the cut progresses.
What the Torch Lifter Does in the Cutting Sequence
The hardware layout varies by machine builder, but the operating role is consistent. The torch lifter handles three practical moments in the cutting cycle:
- Moving the torch into the correct approach position before piercing.
- Setting an appropriate working height for the specific process stage.
- Adjusting vertical position when cut conditions require correction.
The lifter matters even on tables with excellent X and Y motion systems. The gantry decides where the torch goes across the sheet. The lifter decides where the torch sits relative to the sheet. Both are necessary for a clean, repeatable cut.
Torch Lifter vs. Torch Height Control: What Buyers Actually Need to Know
Suppliers often use torch lifter and torch height control almost interchangeably, which creates confusion during the buying process. It helps to separate the two concepts:
- The torch lifter refers to the Z-axis torch movement assembly—the physical mechanism that provides vertical travel.
- Torch height control refers to the broader function of maintaining a workable cut height during operation, which may include sensing, feedback, and automatic correction.
On some quotations, those boundaries are described clearly. On others, they are blended into a single feature bullet. Buyers should not get stuck on label purity. The better question is what the machine actually does during piercing, cutting, and height correction. If the supplier can explain that sequence clearly, the terminology matters less.
What Happens When the Torch-Lift System Is Weak
The easiest way to understand the value of a torch lifter is to look at what happens when it is undersized, slow, or poorly matched to the table. Common consequences include:
- Less consistent cut quality across a single sheet and between batches.
- Higher consumable waste, particularly nozzles and electrodes.
- More interruptions during production for manual height correction.
- Greater sensitivity to sheet irregularity and table condition.
- More operator intervention than the quotation implied.
The torch lifter should not be treated as a minor checkbox on a specification sheet. A table can still look attractive in a quotation while the height-control side of the system is only lightly explained. That gap usually becomes visible only after real production begins, when the operator is fighting the machine instead of running parts.
Judge It as Part of Process Stability, Not as an Isolated Feature
The wrong way to buy a plasma table is to isolate the torch lifter from the rest of the cutting system. The better way is to ask whether the table can hold process stability in ordinary work. That means asking:
- How does the system establish working height at the start of a cut?
- How does it respond when the material is not perfectly flat?
- How much operator correction is still expected during normal runs?
- How clearly does the supplier explain height-control behavior in the quote and support documentation?
- What part of consumable life and cut consistency depends on this subsystem?
These questions reveal more than simply asking whether a torch lifter is included. They force the supplier to explain how the machine behaves under real conditions rather than reciting feature names.
The Lifter Matters More on Inconsistent Material Than on Demo Pieces
Machine demonstrations usually happen on controlled sample material. The sheet is clean, flat, and properly supported. Real production is less polite. Once the shop is cutting sheets that vary in flatness, surface condition, or setup quality, the torch lifter becomes much more important.
A table that looks smooth in a demo can feel unstable when height conditions are no longer ideal. Buyers should push the conversation away from showroom language and toward workflow language. Ask how the machine behaves on imperfect material, not only on staged samples. If the supplier cannot answer that question with specifics, that is useful information in itself.
Why This Subsystem Matters Even If You Are Not Buying a Plasma Table
The torch-lift discussion is also relevant for shops that outsource plasma cutting rather than running it in-house. Understanding how torch height control works helps explain why one supplier delivers steadier output than another.
A fabricator with better height control and better general process discipline is usually easier to trust on repeat jobs than one that treats torch position as a secondary issue. For companies deciding whether to outsource cutting or bring more work in-house, the more useful question is not just who can cut the part once. It is who can hold output quality consistently across repeat orders and variable sheet conditions.
When the Torch Lifter Discussion Reveals a Process Mismatch
Sometimes the torch lifter conversation exposes a deeper issue: the buyer may be pushing plasma into a job where the process itself is a weak fit. If the material is highly sensitive to thermal side effects, or if downstream quality demands are too strict for the broader plasma workflow, then a better torch-lift system may improve control without changing the underlying process limitation.
In those cases, the more useful comparison is a process comparison rather than a subsystem comparison. Buyers weighing thick conductive material against heat-sensitive requirements should compare the broader tradeoffs in waterjet, plasma, and laser process selection before committing to a machine purchase.
Questions to Ask a Supplier Before Signing
If a supplier mentions torch lift, torch height control, or automatic height adjustment, ask:
- What does the height-control sequence look like in normal production, from initial positioning through the end of the cut?
- How does the system behave on material that is not perfectly flat?
- Which parts of cut consistency depend most on this subsystem?
- What level of operator intervention is still expected during a typical shift?
- How is this function described in the quoted scope and support package?
These questions usually reveal whether the supplier sees torch height as a real process-control issue or just as a feature bullet. If the quote itself already exists, it is worth comparing CNC machinery quotations line by line so the height-control conversation does not stay trapped in vague wording.
The Bottom Line on Torch Lifters
A plasma torch lifter is the part of the system that moves the torch vertically so the process can set and maintain a workable torch-to-material distance during cutting. That sounds simple, but the commercial effect is larger than the wording suggests.
Torch lift influences cut consistency, consumable life, operator workload, and how calmly the table handles real material instead of demo material. The best way to judge it is not as an isolated mechanical detail. Judge it as part of the table’s ability to keep plasma cutting stable when ordinary production conditions stop being ideal.
How Torch Lifters Interact With Piercing and Edge-Start Quality
The most demanding moment for any plasma torch lifter is not the steady-state cut. It is the pierce. When the torch first fires, the arc must establish itself through the full thickness of the material, and the height behavior during those first few hundred milliseconds sets the tone for the entire cut.
During piercing, the torch needs to be positioned differently than during cutting. A typical sequence starts with the torch lowered to a pierce height, fires the arc, and then transitions to a cutting height once the arc has fully penetrated the material. If the lifter is slow to react, the torch may dwell too long at the pierce height, which can cause the molten material to blow back onto the nozzle. If the lifter moves too aggressively, the torch can dive into the puddle before the cut is fully established.
Shops that cut thick plate repeatedly will notice this immediately. A torch lifter that handles thin sheet gracefully can struggle on thicker material where the pierce takes longer and the height transition window is narrower. Buyers should ask how the height-control system handles the pierce-to-cut transition specifically, not just how it maintains height during the steady-state portion of the cut.
Edge starts present a different challenge. When the torch begins cutting from the edge of a plate rather than piercing through the middle, the initial height reference may be established on a different surface condition. Scale, rust, or mill finish can confuse sensing systems that rely on electrical contact or arc voltage feedback. A well-designed torch lifter will establish a reliable reference point before the cut begins, rather than assuming the material surface is uniform across the entire sheet.
Arc Voltage Feedback vs. Contact Sensing: What the Shop Floor Actually Sees
Most CNC plasma tables use one of two approaches to height control: arc voltage feedback or contact sensing. The distinction matters because it affects how the machine behaves on real material.
Arc voltage feedback works by measuring the voltage across the arc during cutting. As the torch-to-work distance changes, the arc voltage changes in a predictable way. The controller compares the measured voltage to a target value and adjusts the lifter accordingly. This approach allows continuous correction during the cut, which is valuable on material that varies in flatness across the sheet.
Contact sensing works differently. The torch is lowered until it physically touches the material, then raised to a preset offset. This establishes a known starting height, but it does not provide continuous feedback during the cut. Once cutting begins, the torch holds that initial height unless the system also incorporates voltage feedback.
In practice, many production tables combine both approaches. Contact sensing establishes the initial reference, and voltage feedback maintains the height during cutting. Buyers should ask which method the table uses and how the system behaves when the material surface is not clean. Scale, oil, or paint can interfere with contact sensing, and voltage feedback can be affected by torch consumable wear. A good system will handle these conditions without requiring constant operator attention.
Consumable Life Is the Hidden Cost of Poor Height Control
The financial impact of a weak torch lifter often shows up in the consumables bin rather than in the cut quality report. Nozzles and electrodes are the components that wear fastest in plasma cutting, and their lifespan depends heavily on maintaining the correct torch-to-work distance.
When the torch runs too high, the arc stretches and the nozzle takes more thermal damage. When the torch runs too low, the nozzle can contact the workpiece, which causes immediate damage and accelerates electrode wear. In both cases, the operator replaces consumables more frequently, and the cost adds up across a production shift.
A shop cutting eight hours a day can easily go through multiple sets of consumables per week. If poor height control shortens consumable life by even 20 to 30 percent, that is a recurring cost that appears on every job. The torch lifter is not just a quality feature. It is a consumable-cost feature that affects the shop’s cost per part.
Operators often notice the pattern before management does. They start keeping spare nozzles and electrodes at the machine, and they learn to recognize the sound of a torch that is running too high or too low. When a table has good height control, the consumable usage becomes predictable, and the operator can focus on loading material and unloading parts instead of monitoring the torch.
Maintenance Considerations for Torch Lift Systems
The torch lifter is a mechanical system, and like any mechanical system on a CNC table, it requires attention. The vertical slide or guide rails need to stay clean, and the drive mechanism needs proper lubrication. Shops that ignore these basics will see the lifter degrade over time, which shows up as inconsistent height control even if the controller is functioning correctly.
Dust and cutting debris are the main enemies. Plasma cutting produces fine particulate that can work its way into linear guides and ball screws. A torch lifter that operates smoothly when new can become sticky or erratic after months of exposure to cutting dust. Regular cleaning and lubrication should be part of the machine’s preventive maintenance schedule.
The lifter also needs to be protected from the physical abuse that happens in real production. Torch crashes, where the torch collides with the material or a clamp, can bend the lifter mechanism or damage the height-sensing components. Some tables include crash protection that allows the torch to deflect on impact, but this protection needs to be reset properly after each incident. Shops should verify that the operator knows how to check the lifter after a crash and that the machine’s calibration is verified before returning to production.
Retrofit Considerations for Existing Tables
Shops that already own a plasma table without adequate height control sometimes consider retrofitting a torch lifter. This can be a practical option, but it is not always straightforward. The lifter must be compatible with the table’s existing control system, and the retrofit must include the sensing and feedback components, not just the mechanical Z-axis assembly.
A retrofit that only adds vertical motion without proper height sensing will not solve the underlying problem. The shop will still be adjusting torch height manually, just with a motorized assist. The value of a torch lifter comes from the closed-loop control that maintains height automatically, and that requires the controller to receive feedback from the cutting process.
Buyers considering a retrofit should also evaluate the age and condition of the rest of the table. If the gantry, drive system, or control software is already outdated, adding a new torch lifter may be putting new components on an aging platform. In some cases, the cost of a retrofit approaches the cost of a new table with better integrated height control, and the new machine will come with a warranty and current software.
How to Verify Height-Control Performance Before Purchase
A demonstration on clean, flat sample material will not reveal how the torch lifter performs under real conditions. Buyers should ask for specific evidence of height-control performance, and they should be prepared to test the machine on material that matches their actual production.
Ask the supplier to run a test cut on a sheet that has some variation in flatness. If the shop regularly cuts material with scale or surface irregularities, ask for a test on that material as well. Watch how the torch behaves during the pierce, how quickly it settles into the cutting height, and whether the operator needs to intervene during the cut.
It is also worth asking about the controller’s ability to log or display height data. Some systems can record torch height throughout the cut, which provides a useful record of how the lifter performed. If the supplier cannot show this data, that is a limitation worth noting.
Finally, ask for references from shops that run similar material and similar part sizes. A torch lifter that works well on a table cutting thin sheet in a clean shop may not perform the same way in a shop cutting thick plate with heavy scale. The reference check should focus on production conditions, not just on whether the machine works at all.