Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
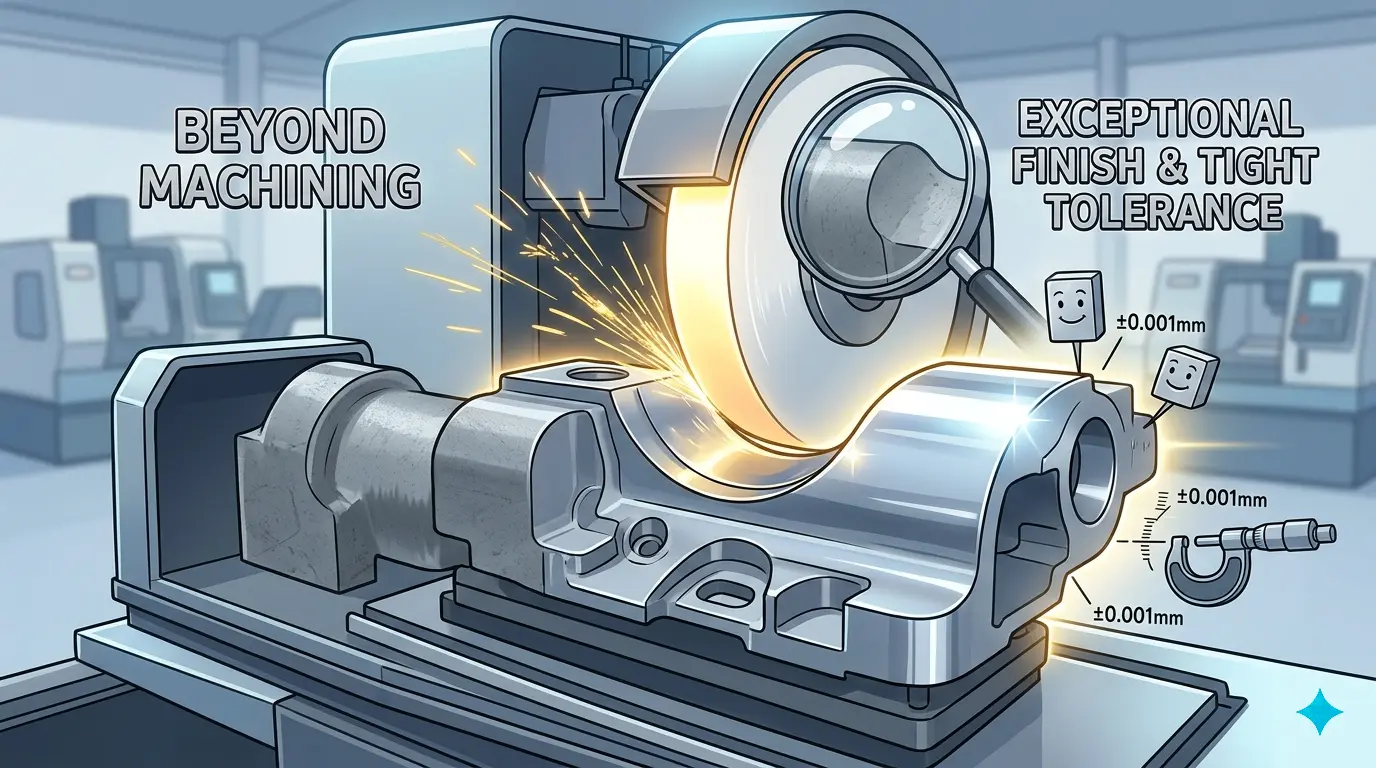
Most grinding decisions surface late in the route, after milling or turning has brought a part near size, after heat treatment has shifted the material, and after inspection exposes a bearing seat drifting across batches or a hardened journal losing roundness. At that release gate, the real question is not whether a grinder sounds more precise but which critical feature still carries unacceptable residual risk. Grinding enters when controlled removal, geometry control, and repeatable final condition matter more than bulk stock removal. Read the failing requirement first, then let that feature choose the machine family and justify the added process burden.
Grinding Enters the Route When the Last Few Microns Become the Real Bottleneck
Most grinding decisions are not made at the beginning of a production route. They are made at the end, after a part has already been milled or turned close to final size, after heat treatment has changed the material state, and after inspection or assembly has exposed a problem that earlier operations could not hold. The part looks nearly finished. The dimensions are close. But the bearing seat drifts across batches, the sealing face is functionally too rough, or the hardened journal no longer holds the roundness the drawing demands.
That is the moment grinding stops being a specialty topic and becomes a route-selection question.
The most useful way to evaluate grinding is not to start with wheel types or machine configurations. It is to start with a release gate. The part has passed through earlier operations but still cannot be released with confidence. Something about the final condition is not trustworthy enough. Grinding becomes relevant when that remaining gap is too expensive to leave unresolved and too disciplined to solve casually.
Grinding Is About Controlled Removal, Not Bulk Stock Removal
Shops rarely choose grinding because they need another way to remove large amounts of material. Milling and turning handle that efficiently. Grinding enters the conversation when the last small amount of material matters more than the earlier bulk removal. The part may already be close to size, but the final requirement demands a more controlled finishing process.
This distinction matters because process decisions become expensive when a team confuses removal with control. Primary machining routes are excellent at getting geometry close. Grinding usually enters when the remaining stock is no longer the main issue. What matters now is whether the final surface and dimensional condition can survive real production, real inspection, and real functional use.
The grinding question is rarely, “Can this part be machined?” It is, “Can this part be finished to its real requirement repeatably enough without grinding?”
Read the Requirement Before You Read the Machine Type
The better starting point is not “Do we need a grinder?” It is “What requirement is still failing after the earlier machining steps?”
In practical terms, the trigger is usually one or more of these:
- The part must hold a tighter final size window over batches.
- The surface is functionally important, not just visually smooth.
- Roundness or concentricity matters more than turning can hold comfortably.
- Flatness or parallelism is tied to sealing, mating, or reference accuracy.
- Heat treatment changed the part enough that the last operation needs better control.
If the drawing does not really demand one of those pressures, grinding may be unnecessary cost.
This is the first good filter because grinding is expensive when chosen from vague language. “Higher precision” is not yet a reason. “Better finish” is not yet a reason. The shop has to know which functional condition is still under threat and why the earlier route cannot hold it reliably enough. Without that clarity, grinding becomes a prestige answer instead of a process answer.
The Right Trigger Is Residual Risk, Not a Broad Preference for Precision
Many route discussions drift because people say they want “more accuracy” when what they really mean is that one residual risk is still open. A bearing seat may vary too much over batches. A shaft journal may be acceptable in one run and unstable in the next. A hardened face may come back from heat treat with too much movement. A sealing feature may be visually acceptable but functionally too rough.
Those are not abstract quality wishes. They are residual risks.
Grinding becomes a sensible route decision when the part has already moved through the main stock-removal steps and one critical risk still remains. In that situation, the grinder is not replacing the rest of the process. It is closing the specific gap the rest of the process is not holding well enough.
Let Geometry Pick the Grinding Family
Grinding is not one universal process. The geometry of the critical feature decides the right machine family.
Surface grinding is the natural discussion when the critical feature is flat: tooling plates, reference faces, sealing surfaces, or parts where the face relationship matters more than raw milling speed.
Cylindrical grinding becomes relevant when the part is built around journals, bearing fits, shaft diameters, and other round features where size and axis-based quality matter more than normal turning can hold reliably enough.
Internal grinding and other specialist variants matter too, but the core logic stays the same: let the feature shape choose the grinding route, not the machine label.
This matters because buyers sometimes ask for “a grinding machine” as if the family were interchangeable. It is not. If the job is about flatness, parallelism, and face condition, the logic is different from a job built around roundness, journal size, and concentricity.
Identify the Feature That Cannot Be Allowed to Drift
When a part has several features, the route becomes easier to judge by identifying which one absolutely cannot wander. That feature usually exposes whether grinding belongs in the plan.
Examples are straightforward:
- A journal that must carry a bearing fit consistently
- A sealing face that must remain flat and controlled
- A reference face that drives assembly stack-up
- A hardened wear feature that must survive final use without dimensional instability
Once that non-negotiable feature is identified, the grinding decision becomes less emotional. The team can ask whether the existing turning, milling, or heat-treat route protects that feature well enough in repeat production. If not, grinding may be justified for that one feature even if the rest of the part does not need such a finishing step.
Heat Treatment Often Creates the Real Need for Grinding
Many shops do not feel the grinding question until hardening enters the route. A part can machine well in a softer state, then move, distort, or become much less forgiving after heat treat. At that stage, the finishing route changes. The earlier operations still matter, but the last operation now has to recover final condition from a tougher material state.
This is why grinding often appears in hardened-shaft work, wear components, tool-steel features, and precision fits that must remain dependable after the part’s material condition changes.
Before heat treatment, the part may look stable and economical. After hardening, the same part may no longer behave like a forgiving machining job. The finishing burden shifts. The process is no longer simply about shape. It is about restoring the final condition after the material has changed.
Grinding Re-Establishes Trust After the Material Changes
This difference matters. A pre-heat-treat part can look excellent on a bench and still not survive the full route in a stable way. Once hardening enters, the part may shrink, move, or become much more sensitive to how the last finishing stock is managed.
Grinding becomes attractive in these cases because it helps re-establish trust after the part has gone through the step that changed it most. The question is no longer whether the earlier machining operation looked good. The question is whether the finished part still holds the relationship the drawing actually requires in its final material state.
Grinding Adds Capability, but It Also Adds a Real Production Burden
Grinding is not free precision. It brings wheel selection, dressing discipline, coolant management, heat control, inspection burden, and secondary handling. The machine may solve the finish or tolerance problem, but it also adds another process that has to stay stable every day.
The honest comparison is never just about whether grinding can hit the requirement. The comparison is whether the improvement in output is worth the extra process ownership.
The grinder does not arrive alone. It brings an operating discipline with it. Wheel behavior has to be managed. Dressing has to stay consistent. Coolant condition starts mattering differently. Thermal damage becomes a process concern. Inspection becomes more tightly tied to the finishing stage. The route gains capability, but it also gains obligations.
The Cost Question Is About Ownership, Not Only Cycle Time
Buyers sometimes compare grinding only by asking whether the extra cycle time fits the target price. That is too narrow.
The more complete question is whether the organization is prepared to own:
- Wheel management
- Dressing repeatability
- Coolant discipline
- Final stock consistency
- Inspection routines
- The scheduling effect of another finishing stage
If those elements are weak, the grinder may still hit a few parts successfully while remaining unstable as a production solution. If those elements are strong, grinding often pays for itself by reducing the cost of rejected final-condition parts.
Better Upstream Machining Sometimes Solves the Problem More Cheaply
Grinding should not be used to hide a weak earlier route. If the real issue is poor fixturing, unstable tooling, excess heat in milling, poor turning practice, or a process plan that leaves too much stock variation for the last step, a grinder may only mask the weakness temporarily.
At other times, the upstream process is already mature and the requirement still needs more finishing control than milling or turning can deliver economically. That is when grinding belongs in the route for the right reason.
Grinding should close a genuine residual gap, not absorb bad process design that should have been corrected earlier. If the part arrives at the grinding stage with too much variation, too much stock uncertainty, or unstable geometry, the finishing step is forced to do corrective work it was not meant to own.
Stock Allowance Discipline Decides Whether Grinding Feels Controlled or Wasteful
A grinding stage works best when the part enters with a sensible and repeatable finishing allowance. Too little stock can leave the grinder unable to clean up the feature reliably. Too much stock can burden the wheel, increase heat risk, and make the finishing step slower and less predictable than it should be.
Upstream control matters enormously here. Turning or milling does not have to produce the final feature, but it does have to deliver the feature honestly enough that grinding can behave like a controlled finishing step instead of a rescue operation.
When shops ignore this, they often blame the grinding process for instability that really started in how the part was handed to it.
Where Grinding Usually Pays Back
Grinding tends to justify itself when the part is already close to final geometry and the last remaining demand is expensive to miss. Typical examples include:
- Bearing fits that cannot drift from batch to batch
- Hardened shafts that still need dependable journal quality
- Sealing or mating faces where surface condition is functional
- Flat reference surfaces that affect later assembly or measurement
- Parts where one-off success is easy but repeat production is not
In those cases, grinding is not just another step. It is the process that closes the remaining risk.
Grinding pays back when missing the final requirement costs more than owning the finishing stage properly. That may be because the part is expensive, because assembly failure is painful, because post-heat-treat recovery is necessary, or because the part’s function depends on final-condition trust more than on raw machining speed.
Repeatability Justifies Grinding More Clearly Than One Good Sample Does
Many parts can be made to look acceptable once. That is not the same as having a repeatable route.
Grinding becomes much easier to justify when the issue is not whether one part can pass, but whether batches can pass without depending on unusually favorable conditions. If the earlier route only works when tooling is fresh, material behavior is friendly, setup is unusually calm, and inspection luck is good, the process may not really be strong enough.
Grinding often earns its place when it turns a fragile success into a dependable routine.
Where Shops Misread the Need
The most common mistake is using grinding language too loosely. “We need a smoother finish” or “we need tighter quality” is usually not enough. The shop has to know whether the real problem is size control, roundness, flatness, functional surface quality, or post-heat-treat recovery.
Another common mistake is reading a single successful sample as proof that the upstream process is enough. Repeat production is usually where the truth appears. If the route can only hit the target when conditions are unusually favorable, the process is not really stable.
There is also a commercial version of this mistake: asking for grinding because it sounds safer without identifying which feature is actually failing. That often leads to oversized process cost. The route becomes more complex, but the team still does not have a clear statement of what the grinder is supposed to guarantee.
Supplier Conversations Improve When You Ask Which Feature Grinding Is Protecting
This is often the most revealing question in quoting or route review.
Instead of asking only whether a supplier has grinding capability, ask:
- Which feature is the grinder protecting?
- Is the purpose final size, roundness, flatness, or functional finish?
- Does grinding occur before or after heat treat, and why?
- What stock condition is expected before the part enters grinding?
Not every tight-tolerance part needs grinding. A CNC grinding machine enters the process when the remaining risk on a feature is too high to leave to ordinary cutting alone. That risk may come from size variation, geometry drift, surface condition, hardened material, heat-treatment movement, or a combination of all of them. Grinding is not just “more precise machining.” It is usually the final-condition process selected when the part has reached a stage where the last bit of control matters more than the earlier bulk metal removal.
Grinding Usually Owns a Critical Feature, Not the Whole Component
In most production routes, grinding does not dominate the whole part. It is often assigned to a small number of features that carry the highest functional burden. That may include a shaft journal, a bearing seat, a precision bore, a flat reference face, a hardened outside diameter, or a surface whose finish affects sealing or rolling contact.
Grinding is often misunderstood as a superior replacement for milling or turning in general. That is usually the wrong frame. In many real jobs, roughing and semi-finishing are still done efficiently by other processes. Grinding appears later because one or two features have crossed into a tighter risk category.
When someone says a part needs grinding, the best response is usually not “Why can’t we just machine it?” The better question is “Which feature became too risky to leave to the previous process?”
Finish Alone Rarely Explains the Whole Decision
Grinding is strongly associated with fine surface finish, and that reputation is deserved. But finish alone usually does not explain why a shop adds grinding to a route. The real issue is often total feature behavior. A shaft journal may need controlled size, roundness, and surface integrity after hardening. A flat face may need to serve as a dependable datum in assembly. A bore may need repeatable performance, not just a nice-looking measured finish value.
Grinding decisions should not be reduced to a smooth-versus-rough conversation. The real question is what the feature must do in service and whether the upstream process can hold that behavior reliably. Surface finish may be part of the answer, but it is rarely the whole answer.
Grinding Is About Geometry Control as Much as Size Control
Beginners often hear grinding described as the process used when a shop needs very tight size. That is true, but incomplete. Grinding is often selected because it helps improve the geometric behavior of a feature as well.
Depending on the feature and machine style, grinding may be chosen to improve:
- Roundness
- Cylindricity
- Flatness
- Parallelism
- Runout
- The reliability of a datum surface
This broader view matters because a feature can be close on size and still behave poorly in service. A shaft can measure near nominal yet run badly if roundness and axis behavior are unstable. A flat face can hit thickness while still being a weak reference if the geometry is not controlled well enough. Grinding earns its place when that broader feature behavior matters, not only when a single linear dimension looks tight on a print.
Owning Grinding Means Owning a Process, Not Just Buying a Machine
Buyers sometimes underestimate what it means to add grinding capability. The cost is not just the machine price. The route also depends on wheel selection, dressing strategy, workholding stability, thermal control, coolant performance, inspection consistency, and people who understand how the grinding step fits the broader manufacturing sequence.
The machine purchase decision should always be tied to part mix and process frequency. A plant that regularly sees hardened shafts, precision bores, or critical datum faces may find that owning grinding improves schedule control and repeatability. A plant that sees these needs only occasionally may be better served by a supplier relationship instead of building a lightly used grinding cell.
The decision is rarely just about whether a grinder would be useful sometimes. It is about whether grinding is a recurring core route need or only an occasional exception.
Inspection Strategy Has to Match the Reason Grinding Was Added
If grinding is selected because the feature is functionally sensitive, inspection cannot be casual. The route needs a measurement plan that confirms the very thing grinding was supposed to control. That may include size checks, geometry checks, surface verification, and repeated monitoring across batches.
Without that feedback loop, the shop risks paying for a higher-control finishing step without proving the benefit it was meant to create. People talk about whether a grinder can hold a dimension, but the deeper question is whether the process can verify the feature behavior that justified grinding in the first place.
Buying Decisions Should Compare Route Fit, Support, and Cost Together
If the conversation turns from process theory to equipment purchase, the machine should never be judged in isolation. A grinder may be technically capable and still be the wrong investment if the route does not generate enough justified work for it. On the other hand, a shop that repeatedly depends on outside grinding for critical lead-time-sensitive features may benefit from internal control.
Buyers should compare more than motion specs or surface claims. Support expectations, process fit, quote scope, training, and the real cost of owning the finishing step matter just as much. It helps to compare CNC machinery quotations carefully so the decision reflects the full production burden rather than the machine alone. For broader context on machine families and industrial equipment categories, the Pandaxis equipment catalog is a practical starting point.
When Finish and Tolerance Require Grinding
A CNC grinding machine makes sense when a part reaches the stage where one or more critical features need tighter final-condition control than upstream machining can provide reliably and economically. That usually happens late in the route, after the component is already near finished shape. The reason is often not just surface appearance. It is the combined demand of size, geometry, material condition, and function.
Grinding is the process chosen when the last remaining risk on an important feature is too high to leave to ordinary cutting variation. Once you understand that, the route decision becomes much easier to judge. The question is no longer whether grinding sounds precise. The question is whether the feature has become important enough to deserve a dedicated final-condition process.
That is when finish and tolerance truly require grinding.