Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
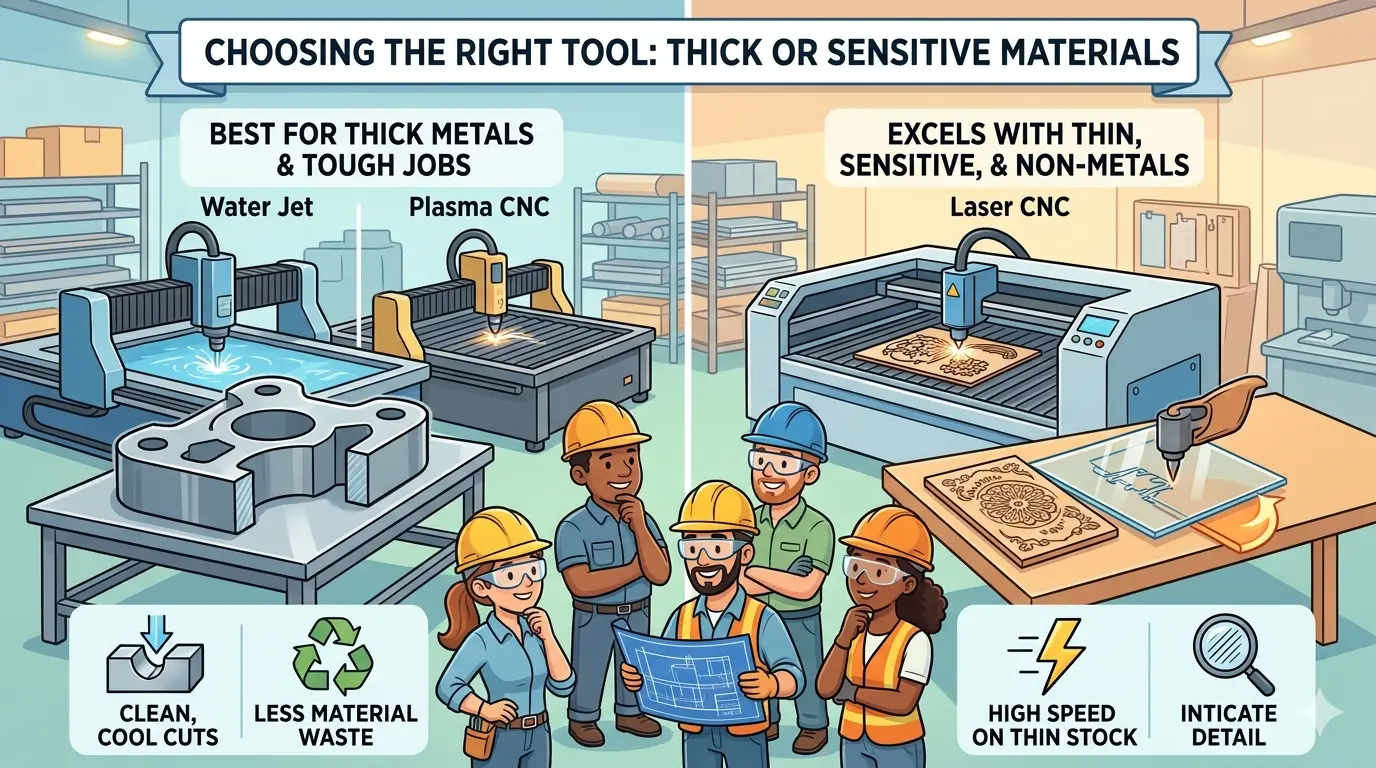
Buyers frequently collapse two distinct purchasing problems into one vague comparison: thick materials and sensitive materials. Thickness demands stable output, predictable throughput, and manageable post-cut cleanup, while sensitivity demands minimal heat exposure, distortion control, and preserved surface condition. A thick part is not automatically sensitive, and a sensitive part is not automatically thick. Mixing these frames produces a confused shortlist and a machine that solves the wrong problem well. Before comparing waterjet, plasma, or laser, separate the material-risk question from the production-burden question, then map what happens after the cut.
Thick and Sensitive Materials Are Not the Same Buying Problem
Most process comparisons start with the wrong premise. Buyers ask which cutting technology is better for thick or sensitive materials as if those two requirements point toward the same machine. They do not.
Thickness drives decisions about productivity, edge condition, and operating burden. Sensitivity drives decisions about heat exposure, distortion risk, finish protection, and downstream quality. A thick part is not automatically sensitive. A sensitive part is not automatically thick. When those two decision frames get mixed together, the shortlist becomes confused and the shop often ends up with a machine that solves the wrong problem well.
The safer way to approach this comparison is to separate the decision into two questions. First, what kind of material risk matters most during the cut? Second, what kind of production burden can the shop actually support every week? Answer those honestly and the technology choice becomes much clearer.
What Thick-Material Jobs Actually Demand
When buyers talk about thick material, they usually mean jobs where the cutting process has to maintain stable performance over long cycles. The concerns are operational rather than philosophical:
- Stable cutting performance across the full part run
- Predictable throughput that supports the production plan
- Edge condition that does not require excessive cleanup before the next step
- Power and support burden that matches the facility
- How much post-cut work remains before the part can move on
Thickness creates pressure on process stability. The machine has to keep cutting at a consistent quality level without frequent interruptions for consumable changes, maintenance, or adjustment. If the process drifts midway through a run, the shop ends up with parts that vary in quality and rework that was never quoted.
What Sensitive-Material Jobs Actually Demand
Sensitive materials create a different set of priorities. The buyer is not primarily worried about throughput. The buyer is worried about what the cutting process does to the material itself:
- Heat impact on the cut zone and surrounding material
- Distortion risk that creates fit problems downstream
- Surface condition after the cut
- Micro-cracking, charring, or other material damage that inspection will catch
- Whether downstream finishing becomes harder because of the chosen process
These concerns matter most when the part has to meet a visible finish standard, when the material has low thermal tolerance, or when the cut edge feeds directly into assembly or coating without an intermediate cleanup step. A process that leaves a thermal signature might still produce an acceptable part, but the cost of dealing with that signature often shows up later in the workflow.
Waterjet: The Strongest Answer When Heat Risk Is the Core Problem
Waterjet enters the conversation whenever the part or material is less forgiving about thermal input. The attraction is not simply that waterjet can cut. The attraction is that buyers are trying to protect the material condition while still producing the required shape.
Waterjet becomes defensible when the shop is dealing with:
- Heat-sensitive material behavior that rules out thermal processes
- Parts where thermal influence creates unacceptable downstream risk
- Mixed-material production where one thermal process is too limiting
- Jobs where preserving edge and surface condition matters enough to justify a heavier support burden
This does not mean waterjet is automatically the best answer for every delicate job. It means waterjet becomes much harder to ignore when heat damage, distortion, or material-condition risk is the first issue on the table.
The practical test is simple: can the buyer explain what specific business risk waterjet removes? If the answer is clear, waterjet belongs in the conversation. If the answer is vague, the shortlist may be using waterjet as a prestige placeholder rather than a process decision.
Waterjet is rarely the casual answer. It asks the buyer to support a broader operating structure, so it tends to punish vague logic. That is exactly why it becomes convincing when the job is real. If the part family genuinely depends on minimizing heat effect or preserving material condition across a wider material range, waterjet can be the most coherent answer even when the ownership burden looks heavier.
Plasma: A Fabrication Workflow Decision, Not Just a Cutting Decision
Plasma is commonly considered when the shop needs a practical cutting route for conductive metals and wants productive output without moving into a much heavier capital structure than necessary. In thick-material discussions, plasma earns attention because it can be commercially workable where buyers care more about throughput and cost realism than about the cleanest possible thermal history.
Plasma usually looks strongest when:
- The work is conductive metal
- The downstream workflow can tolerate the process signature
- The shop can support extraction and general fabrication burden
- The part family does not demand a non-thermal answer
Plasma looks weaker when the material is not tolerant of the heat effect or when downstream finishing cost starts erasing the advantage that made plasma appealing in the first place.
Plasma comparisons often go wrong when buyers look only at the promise of thick-metal productivity. The process should be judged through a fabrication lens. What edge condition is acceptable afterward? What cleanup burden can the team absorb? What extraction and support systems are already in place? Does the actual part family reward this process, or only tolerate it?
When those answers line up, plasma can be a very practical answer for thick conductive material work. When they do not, the machine can still cut the parts while quietly creating downstream cost that the initial comparison never captured.
Laser: A Conditional Answer, Not a Universal One
Laser is often mentioned in the same conversation, but buyers should be careful not to let the word laser hide the real process question. Laser can be a strong answer when precision, detail, and repeatable non-contact cutting matter on suitable material families. But in the specific question of thick or sensitive materials, laser is usually the most conditional of the three choices.
Laser can be a good fit when:
- The material sits inside a range the chosen laser configuration handles well
- Detail quality matters enough to justify the route
- The shop wants a non-contact process but does not need the broader heat protection logic that pushes many buyers toward waterjet
It becomes a weaker answer when the material or thickness profile pushes the process outside its comfortable commercial lane, or when heat sensitivity is the problem the buyer is actually trying to solve.
Laser earns its place when the work really values what laser is good at, not when buyers simply want a process that sounds more precise. For this specific comparison, the buyer should define which material family is actually in scope, whether the chosen laser route matches that material and thickness range, and whether detail, cut presentation, and repeatable non-contact behavior are commercially valuable enough to matter. If that justification is tight, laser may be the right answer. If the justification is loose, buyers usually drift into an expensive or mis-scoped conversation very quickly.
For wood, acrylic, and other non-metal materials, buyers should compare the job against laser cutters and engravers intended for those non-metal workflows rather than borrowing generic claims from unrelated metal-cutting conversations.
If Heat-Sensitive Material Is the Priority, Start With the Damage Question
Many buyers start with speed. For sensitive materials, that is often the wrong first move. Start here instead:
- What happens to the material when heat enters the cut zone?
- What kinds of distortion, discoloration, or finish loss become commercially unacceptable?
- Does the chosen process create downstream inspection or rejection risk?
- Will the cut condition force extra finishing work that the quote never counted?
If those questions lead to a low tolerance for thermal side effects, waterjet usually becomes much harder to ignore. If those questions reveal that the part can accept a thermal signature without meaningful business damage, then plasma or laser may stay commercially valid depending on the material family and required finish level.
If Thick Material Is the Priority, Start With Output Stability
For thick-material cutting, the comparison is often less philosophical and more operational. Buyers should ask:
- Which process can keep output stable on the actual part mix?
- How much post-cut cleanup sits outside the machine?
- How often will consumables or maintenance interrupt the run plan?
- Does the support burden match the facility that already exists?
- Are we paying for a premium process feature that the work does not need?
Thickness creates pressure on process stability. Sensitive materials create pressure on process gentleness. Those are related, but they are not the same purchase logic.
Separating the Real Tradeoffs
| Decision Area | Waterjet | Plasma | Laser |
|---|---|---|---|
| Main strength in this comparison | Protecting material condition when heat risk matters | Practical conductive-metal cutting when throughput and budget realism matter | Detail and non-contact precision on suitable material lanes |
| Thick-material logic | Strong when thickness also carries heat-risk concerns | Strong when conductive material and acceptable thermal effect align | Depends heavily on material and process scope |
| Sensitive-material logic | Often the most defensible route when heat damage is the core concern | Usually weaker if thermal effect creates business risk | Can fit some sensitive jobs, but not when the main issue is avoiding heat impact broadly |
| Facility burden | Broad support structure | Fabrication and extraction burden | Support burden depends heavily on application lane |
| Common buyer mistake | Paying for flexibility the workflow does not need | Underestimating cleanup and thermal consequences | Assuming laser automatically means best quality for every delicate job |
This table is not a substitute for quoting. It is a way to keep the conversation honest before quotation review begins.
The Better Process Often Depends on What Happens After the Cut
Many buying mistakes happen because the cut itself is treated as the whole job. It is not. The right process often becomes clearer once buyers look at the downstream steps:
- Does the edge move directly to the next process, or does it need cleanup?
- Does the material need to preserve surface condition for assembly, coating, or presentation?
- Does distortion create fit issues later?
- Does the chosen process create extra labor that was never visible in the machine comparison?
This is where a seemingly cheaper process can become expensive. If the part leaves the machine quickly but arrives at the next stage with more cleanup, more defect risk, or more variation, the cost advantage can disappear fast.
Supplier Comparison Matters Because Process Labels Hide Scope Gaps
Waterjet, plasma, and laser sound precise, but supplier scope can still vary widely. Support items, commissioning, training, extraction assumptions, and operating expectations can all be described differently. Buyers should normalize proposals before comparing them. If the project has already moved into quotation review, it helps to compare CNC machinery quotes line by line before trusting the base machine number. If laser equipment is involved, it also helps to compare laser quotations with the same discipline.
The process decision and the quote decision are related, but they are not the same. A good process lane can still be packaged inside a weak commercial scope.
How to Make the Shortlist Smaller Faster
If the shop wants to reduce confusion quickly, use this order:
- Define the real material family and thickness profile.
- Decide whether thermal side effects are acceptable.
- Map what happens immediately after the cut.
- Check whether the facility can support the chosen process calmly.
- Only then compare supplier packages and pricing.
That order prevents buyers from spending too much time on machines that solve the wrong problem well.
Which One Is Better?
Waterjet is usually the stronger answer when material sensitivity and heat-risk control are the deciding issues. Plasma is often the more practical answer when the job is thick conductive metal and the workflow can tolerate the thermal and cleanup burden. Laser can be the right answer when the material lane, thickness, and detail requirements line up cleanly, but it should not be treated as the automatic winner for every delicate or thick-material application.
The best machine is the one that protects the important part of the job without creating a bigger operational problem elsewhere. For many buyers, that means the decision is less about which process sounds most advanced and more about which one fits the real material risk, facility support level, and downstream workflow with the least hidden cost.