Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
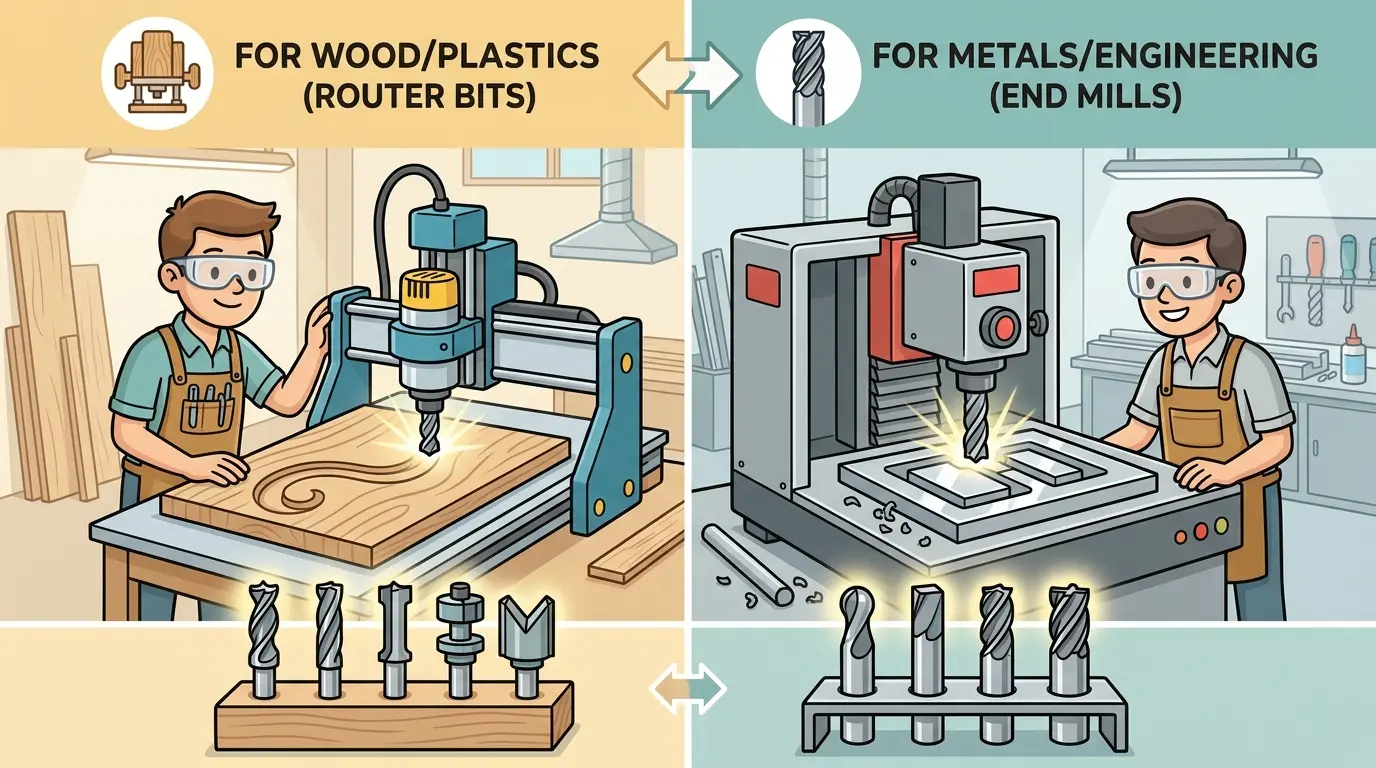
When a CNC line starts producing chipped edges, melted acrylic, or unstable small parts, the first instinct is often to blame the spindle, the vacuum table, or the machine frame. Yet the real culprit is frequently a cutter selected by habit rather than by failure analysis. Router bits and end mills are not interchangeable labels; their geometry reflects different priorities—edge protection versus chip evacuation and heat control. Before you open a catalog, diagnose the defect you are trying to prevent, because the wrong tool choice directly drives rejects, rework, and lost production time.
Start With The Defect, Not The Catalog
Tooling mistakes are one of the fastest ways to make a healthy CNC line look unreliable. Shops blame the spindle, the vacuum table, or the machine frame when the real mismatch is often simpler: the cutter was selected from the wrong logic. In conversation, router bits and end mills get treated as interchangeable labels for any spinning tool. On the production floor, that shortcut creates expensive confusion because the wrong geometry shows up as chipped edges, melted plastic, poor chip evacuation, short tool life, or unstable small parts.
The useful split is not mainly about names. It is about what the cut is failing to protect. Router-bit thinking usually starts from edge outcome and visible finish. End-mill thinking usually starts from chip behavior, heat, and tool engagement under load. There is overlap between the families, but the overlap only becomes productive when the shop stops arguing about labels and starts diagnosing the actual failure mode in the cut.
That is why the smartest way to choose between router bits and end mills is often to begin at the defect, not at the catalog.
Define The Failure Mode First
Before choosing any cutter, the shop should ask what the next bad outcome would cost most. Is the real concern top-edge chipping on laminated board? Bottom-face breakout on nested parts? Melted acrylic? Loaded chips in a deep slot? Short tool life in abrasive sheet goods? Small parts moving because the cut is pulling them the wrong way?
This question matters because it forces the tooling decision to start from production loss instead of from habit. If the job is mainly about protecting a visible edge, laminate face, finished profile, or surface ready for downstream assembly, router-bit logic often deserves priority. If the job is mainly about chip evacuation, heat control, stable engagement, or keeping the tool in a true cutting state through plastics, composites, or non-ferrous material, end-mill logic often becomes more useful.
That does not create a hard wall. It creates the right starting question. Good tooling decisions often begin with “what are we trying not to ruin?”
Router-Bit Logic: Edge Quality And Face Protection
Router bits come from routing culture, which is why their geometry is commonly described in terms that matter immediately to panel shops, sign makers, and routing lines: upcut, downcut, compression, spoilboard surfacing, V-grooving, profiling, laminate protection, and visible edge quality.
In cabinetry, signs, nested panel work, and decorative routing, the cutter is doing more than removing material. It is deciding how much sanding, trimming, touch-up, or reject risk the next person inherits. That is why shops running sheet-based production on CNC nesting machines usually care less about abstract tool families and more about the visible result left on the part after a full sheet has been converted into many finished components.
When the operator’s first complaint is about breakout, fuzzing, laminate damage, or visible edge quality, router-bit language is usually closer to the actual problem.
End-Mill Logic: Chip Control, Heat, And Engagement
End mills come from a milling-style decision process. The conversation more often begins with flute count, helix, chip space, radial engagement, heat, tool loading, and how the cutter behaves once the operation starts looking more like a machining problem than a classic routing problem.
This becomes especially useful in acrylic, engineering plastics, composites, and occasional non-ferrous work where the tool must stay in a clean shearing state instead of rubbing, recutting chips, or trapping heat. In those jobs, a cutter that looks acceptable from a routing perspective may still behave poorly because the chip cannot get out, the heat rises too fast, or the engagement is wrong for the material.
When the operator’s first complaint is melting, loading, poor chip evacuation, or erratic cut sound under sustained engagement, end-mill thinking is usually closer to the problem that needs solving.
Material Is A Filter, Not A Full Diagnosis
Material still matters, but it is not enough by itself. MDF, plywood, melamine, veneered board, solid wood, and many sign substrates often reward routing-focused geometry because visible face quality and profile finish dominate the commercial result. Acrylic, engineering plastics, composites, and some non-ferrous jobs often require closer attention to end-mill-style cutting behavior because chip and heat control become more critical.
The mistake is stopping there. Shops do not get stable results because they chose “wood tooling” or “metal tooling” as broad categories. They get stable results because the geometry matched the material and the operation. A cutter that is excellent on one acrylic profile can still be wrong in a deeper slot. A bit that performs beautifully on laminated board can still behave poorly when the cut changes from edge profile to pocketing.
Material is a filter. It is not the full diagnosis.
Let The Operation Drive The Decision
Profiling a nested sheet is a different problem from pocketing, surfacing, slotting, trimming acrylic, chamfering an edge, or cutting small retained parts out of thin stock. Each operation asks the cutter to do something different with chip flow, face protection, part support, and finish behavior.
That is why standardizing around one favorite cutter often fails. A tool that looks excellent on through-profiling in laminated board may become a weak choice in pocketing because chip behavior changes. A cutter that handles acrylic trim cuts well may struggle when the geometry traps chips or raises heat.
If the shop wants more reliable tooling rules, it should stop starting from “which tool do we like?” and start from “which operation are we actually solving?” The operation usually tells you faster whether routing language or milling language should dominate the decision.
Flute Direction: The First Lever For Face Failures
In many panel, sign, and decorative routing jobs, flute direction is not a minor tuning preference. It changes the commercial outcome directly.
Upcut geometry usually helps pull chips out of the cut, but it can damage the top face in some laminated or veneered materials. Downcut geometry often protects the top face and can help keep sheet stock flatter, but it may also trap chips or build heat if the process is not right. Compression geometry often becomes valuable when both faces matter and the depth of cut allows the tool to work in its intended zone.
This is why router-bit language stays useful on the floor. It maps directly to the visible failures that buyers, operators, and finishing teams actually care about. If the complaint is face quality, top-edge damage, or dual-face cleanliness, flute direction is often the first honest lever to examine.
Flute Count: A Chip-Space Question, Not A Quality Badge
Many shops still talk about flute count as if more flutes automatically means a better cutter. In practice, flute count is a tradeoff between the number of cutting edges, the space available for chips, and the tool’s ability to stay in a clean cutting state.
If the chip cannot leave the cut, finish quality falls, heat rises, and tool life often collapses. That is why flute count should be judged against the material response and the operation, not against a generic preference. In some jobs, more cutting edges are useful. In others, the tighter chip space becomes the problem.
This is where end-mill thinking often clarifies the decision. The right question is not “how many flutes sounds premium?” It is “how much chip can this cut make, and where can that chip go?”
Check The Machine Before You Blame The Cutter
The same cutter can behave beautifully on one router and badly on another. Machine rigidity, spindle runout, collet condition, tool stick-out, spoilboard truth, extraction, and hold-down all change what the cutter is allowed to do.
This is why tooling selection is never only a tooling decision. In thin sheet materials, small nested parts, or flexible sign stock, weak hold-down can make the right geometry look wrong. Shops routing visible parts often discover that hold-down and table behavior affect tooling success almost as much as flute design itself.
That means the correct troubleshooting order is often: confirm the machine condition, confirm the workholding, then judge the cutter. Otherwise the shop may keep changing tool geometry while the real defect is coming from a weak process environment.
A Defect Map For Faster Diagnosis
| If The Main Defect Is… | The Shop Should Usually Inspect First | The Better Starting Logic Is Often… |
|---|---|---|
| Top-edge chipping or laminate breakout | Flute direction and edge-protection geometry | Router-bit thinking |
| Bottom-face tear-out on through cuts | Downward cutting behavior and support at exit | Router-bit thinking |
| Melted acrylic or loaded chips | Chip space, flute count, and heat behavior | End-mill thinking |
| Poor slot quality under sustained engagement | Chip evacuation and tool loading | End-mill thinking |
| Small parts moving during cutout | Hold-down, cut direction, and part support | Tool plus process review |
| Short tool life in abrasive board | Application fit, wear behavior, and output goal | Mixed review, not name-based selection |
This kind of map works because it forces the conversation back onto cut behavior instead of letting the team argue over category names that are too broad to solve the problem.
Most Tooling Confusion Starts As Misdiagnosis
Shops often conclude that they need a stronger or more expensive tool when the real issue is different. Melted plastic may be blamed on tool quality when the real problem is heat and chip recutting. Poor edge finish may be blamed on spindle weakness when the real problem is the wrong flute direction. Moving small parts may be blamed on cutter geometry when the real issue is poor workholding or an unstable spoilboard.
That is why smart tooling standardization starts from symptoms. If the shop can name the failure mode precisely, the tool decision usually gets easier. If the shop keeps using broad phrases like “the cut looks rough” or “we need a better bit,” it will struggle to build repeatable rules.
This is also why overlap between router bits and end mills is not a problem by itself. The problem appears only when the shop expects names to do the diagnostic work that failure analysis should be doing.
Build A Material-Operation Matrix, Not A Preference List
The strongest shops eventually stop debating naming and start documenting what geometry works on which material, on which machine, for which operation, with which visible tradeoff. That is how cutter selection becomes a production rule rather than a preference.
These rules are often more useful than broad standardization because they reflect the actual cell:
- What works for full-sheet profile cuts in laminated board.
- What works for acrylic where heat is the main risk.
- What works for surfacing where finish and flatness dominate.
- What works when small parts are retained in a nested sheet.
- What fails when stick-out, hold-down, or collet quality drift.
That kind of documentation is much more valuable than insisting that one label family is always correct.
Judge Tooling By Cost Per Finished Part
The cheapest cutter is often the most expensive cutter in the shift if it creates sanding, rejects, re-cuts, unstable edge quality, or excessive machine babysitting. Good shops eventually judge tooling by finished-part value: usable edge quality, predictable life, lower cleanup burden, and fewer surprises in the route.
If the cutter plan is being reviewed alongside broader router capacity, it can also help to ask whether the line is still behaving like a general-purpose router cell or whether it is moving toward more throughput-heavy nested production. That distinction affects how much edge quality, chip evacuation, and part stability matter at scale.
The Right Name Is The One That Explains The Cut Correctly
That is the practical conclusion. Router bits usually become the clearer language when edge outcome, face protection, laminate behavior, and profile finish drive the decision. End mills usually become the clearer language when chip control, heat, engagement, and sustained cutting behavior drive the decision. In the overlap zone, the shop should stop trying to win a naming argument and instead build a sharper defect-based tooling rule.
That is what turns cutter choice from habit into process control. The right tool is not the one with the most familiar label. It is the one whose geometry solves the specific failure mode the cut is trying to avoid.