Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
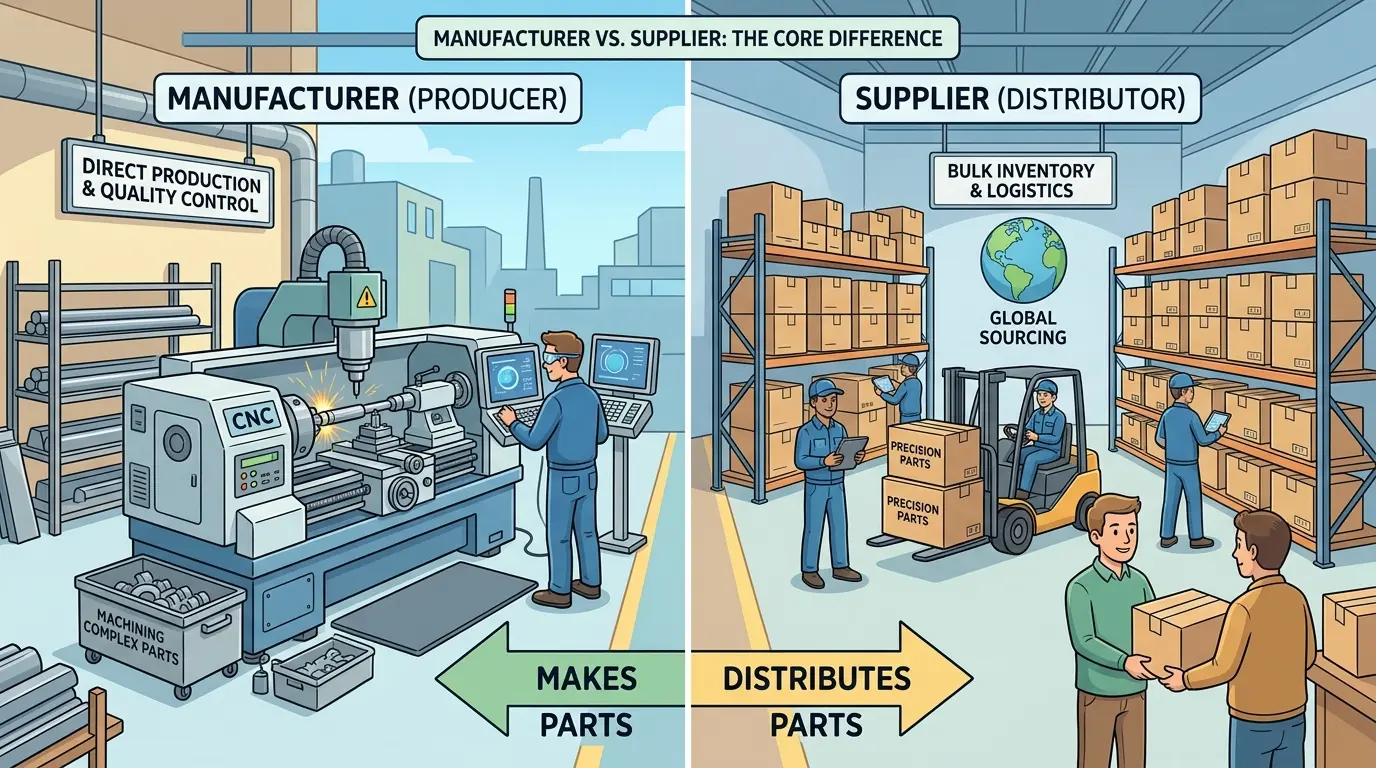
When a turned component drifts out of tolerance or a thread form starts to wander, the label on the quotation—supplier or manufacturer—stops being a formality and becomes a measure of technical distance. This article dissects that distinction by tracing the feedback loop from the first defect back to the machine-side process owner. It forces buyers to evaluate sourcing models on route control, corrective-action speed, and traceability rather than category names. For procurement teams and engineers, the decision hinges on who can turn an engineering revision into a concrete tooling or workholding change without losing clarity.
Why “Supplier” and “Manufacturer” Stop Being Interchangeable
The terms “supplier” and “manufacturer” feel interchangeable when the order is simple, the part is forgiving, and the drawing never changes. The distinction becomes real the moment something goes wrong: a diameter drifts out of tolerance, a thread form starts to wander, material certificates don’t match the lot on the shop floor, or engineering revises a shoulder length after the first quote. At that point, the label on the quotation matters far less than how many technical and commercial layers sit between you and the machine actually making the part.
Every extra layer can lengthen feedback loops, dilute ownership, and turn corrective action into a political exercise rather than a technical one. This is not to say suppliers are inherently weaker or manufacturers inherently stronger. It means the sourcing model changes how information, responsibility, and speed move once the order stops being routine.
Follow the Part Backward from the First Problem
A practical way to compare the two models is to ignore the sales label and imagine the first serious problem. A diameter goes out. A burr appears that wasn’t visible at the sample stage. Assembly reports a fit issue that traceability documents don’t explain. Now ask three questions: who receives that problem first, who can investigate it directly, and who has enough authority to change the process route?
If the commercial contact sits inside the same organization that runs the machines, the path from problem to action is usually shorter. If the commercial contact sits outside the machining environment and relays information through several parties, the loop can still work, but it depends heavily on how disciplined that organization is. The point is not whether the first email comes from a supplier or a manufacturer. The point is who can turn that email into machine-side action without losing time or technical clarity.
Commercial Contact and Process Owner Are Not Always the Same
Many buyers assume the company issuing the quote automatically controls the turning process. Sometimes that’s true. Often it’s only partly true. A manufacturer may turn the part in-house but outsource finishing, overflow volume, or second operations. A supplier may not own turning machines yet still control a tight production network with strong engineering review and disciplined release procedures. A hybrid source may do prototypes internally and shift production to another facility once demand rises.
This is why labels mislead so easily. Asking only, “Are you a manufacturer or a supplier?” is asking too little. The better question is, “Which exact operations do you control directly, and where does responsibility move if the route changes?” That question forces the source to describe the route instead of hiding behind a category name.
RFQ Stage Behavior Predicts Future Control
The request-for-quote stage is often the best early test of process ownership. A source that truly understands the turning route usually asks sharper questions before launch. They may challenge a groove width, question a tolerance stack, ask whether surface finish matters on the entire diameter or only one band, or flag that a thin wall may become fragile in production. Those questions are useful because they show someone is already thinking from the machine outward.
Weakly controlled sourcing models often sound different. The quote may come back quickly, but the feedback is broad, noncommittal, or commercial rather than technical. You hear general reassurance instead of feature-level analysis. That doesn’t automatically prove the source is poor, but it does show where risk may appear later. Strong turning sources—whether direct manufacturers or disciplined suppliers—usually say something concrete before the order starts.
Engineering Changes Stretch or Shorten the Loop
Drawings rarely stay fixed forever. A shoulder moves. A thread changes. Material is upgraded. Surface requirements tighten after assembly feedback. A quantity increase forces a route review. These moments reveal the real structure of the relationship. With a direct manufacturer, the same organization that quoted the work can often review the new condition against tooling, workholding, and cycle risk with fewer translation steps. That doesn’t guarantee a good answer, but it often produces a faster and more specific one.
With a supplier model, the result depends on how much real authority the supplier holds. Some suppliers manage change well because they have internal engineering discipline and direct factory leverage. Others become message relays. You still get an answer, but the route to that answer is longer, and accountability may blur if each party protects its own position first.
When comparing sourcing models, look beyond price and ask how engineering revisions move. The source that handles change cleanly is often safer than the source that merely looked convenient when the print was still stable.
Corrective Action Speed Shows Who Really Owns the Route
Nothing exposes ownership faster than corrective action. If a turned part shows size drift, burr issues, poor finish, unstable concentricity, or mixed material traceability, who isolates the issue? Who decides containment? Who approves route correction? Who communicates whether the problem came from tool wear, clamping, material variability, inspection escape, or process handoff?
If the answer is, “We will ask the factory and get back to you,” keep digging. That response may still be workable, but it describes a different risk profile from a source that can immediately explain which machine family ran the batch, which operation is under suspicion, and how containment will be handled before the next lot moves. Corrective action is not only about fixing the defect. It is about how close you are to the real process owner when time matters.
Traceability Gets Harder When Ownership Is Vague
Traceability sounds simple in sourcing meetings because everyone says they have it. It becomes more important when material substitution is not allowed, when batch-to-batch consistency matters, or when one suspect lot has to be isolated quickly without stopping the entire program. Direct manufacturers often have a natural advantage here because the path from receiving to machining to inspection sits inside one controlled system. But that advantage only matters if their internal discipline is strong.
Suppliers can also manage traceability well, especially when they are experienced in regulated or high-control sourcing environments. The difference is that you need to understand whether the supplier owns the traceability system or merely collects documents from other parties. Paper control is not the same thing as process control. When material risk matters, know exactly where certificates originate, how lot identity stays connected to the batch, and who can isolate a problem without starting a long investigation chain.
Suppliers Often Win When the Route Is Broader Than Turning Alone
The supplier model adds real value when you need more than one process coordinated well. If the job includes turning plus milling, heat treatment, plating, grinding, assembly preparation, or logistics consolidation across multiple part numbers, a capable supplier may simplify the commercial side of the program. Instead of managing several specialized sources directly, you get one point of coordination.
That advantage is real only if the supplier has disciplined control over the route. If the supplier truly manages quality expectations, engineering feedback, timing, and corrective action across its network, you may gain flexibility and lower administrative friction. If the supplier is only forwarding emails among loosely connected subcontractors, the convenience can become expensive once the first technical disruption appears.
Manufacturers Often Win When the Part Needs Tight Process Feedback
Direct manufacturers usually look strongest when the part itself creates technical risk that benefits from short feedback loops. Awkward grooves, thin walls, concentricity-sensitive features, challenging threads, finish-critical diameters, or recurring turned parts with narrow process windows often reward direct machine-side communication. In these cases, you gain by being closer to the people who own tooling, setup, inspection interpretation, and process revision.
That does not mean every turned part should go directly to a manufacturer. It means technically fragile parts often expose the cost of distance faster than straightforward ones do. The more you expect pre-launch manufacturability feedback and fast mid-program correction, the more valuable direct process visibility becomes.
Hybrid Models Are Common, So Ask for an Operation Map
Many of the best and worst sourcing arrangements are hybrid. A company may genuinely manufacture core turning operations while outsourcing coating, overflow capacity, or secondary machining. Another may own prototyping internally but shift production to a partner once demand stabilizes. None of that is automatically a problem. The danger comes when you never learn where those boundaries are.
That is why hybrid sources should be asked for an operation map, even if it stays at a high level. Which steps are always internal? Which ones can move outside? Can alternate factories be introduced without approval? Does the production route change after first article? Is inspection owned by the quoting company or by the external processor? These are not hostile questions. They are normal sourcing questions for buyers who want clear ownership.
Sample Success Does Not Prove Production Control
A clean sample can hide a weak production structure. Many sourcing models can produce a good first article if the order is watched closely enough. The bigger question is whether the sample route is the same route planned for repeat production. If the trial batch was made at one site, under one engineer, with one premium setup, but serial work may later move through a different path, the sample proves less than you think.
This is one reason to ask whether the process used for the quote sample is the same one intended for serial release. If not, the sourcing model deserves more scrutiny. What changes? Why? Who approves the move? A source that answers clearly usually understands its own route. A source that answers vaguely is asking you to accept future uncertainty without proper visibility.
The Strongest Sources Talk in Feature-Level Terms
Whether the company is a supplier or a manufacturer, one sign of strength is feature-level discussion. Can the source explain why a wall may be unstable, why a groove is awkward, where tool access will slow the cycle, or how secondary handling will affect cost? Can it separate commercial convenience from real process risk? Strong sources usually can. They do not hide behind generic confidence.
That kind of technical conversation matters because you are not only purchasing machine time. You are purchasing judgment. A source that can review the print intelligently before launch is often safer than one that offers a lower price but cannot discuss turned-part manufacturability in specific terms. This is also why it helps to compare the relationship against what you should expect from a machining supplier that really owns process communication rather than against price alone.
Questions Worth Resolving Before Approval
Before approving a source for turned components, several points should be explicit:
- Which operations are always internal, and which can be external
- Who owns final inspection and release decisions
- Whether the sample route matches the intended production route
- Whether alternate factories or processors can be introduced later
- Who leads corrective action if the batch drifts
- Who can discuss turned-part manufacturability directly, not only commercially
- How material traceability is maintained when several parties touch the route
These questions do not automatically favor manufacturers over suppliers. They favor sources with clear ownership.
Clear Ownership Is Safer Than a Better Label
The difference between a turned components supplier and a manufacturer is really a difference in technical distance and route ownership. Manufacturers often reduce that distance. Suppliers can still be excellent partners when they coordinate broader routes, logistics, or multi-process programs with real discipline. Hybrid models can work very well too, provided you understand exactly where the turning process sits and who acts when the route changes.
The safer source is not defined by the label printed on the quotation. It is defined by how clearly the source can show who makes the part, who controls the route, and who moves first when production stops being simple. Buyers comparing offers should therefore read sourcing structures with the same care they use when they compare machinery quotes line by line, because clarity of ownership is a production asset in its own right.