Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
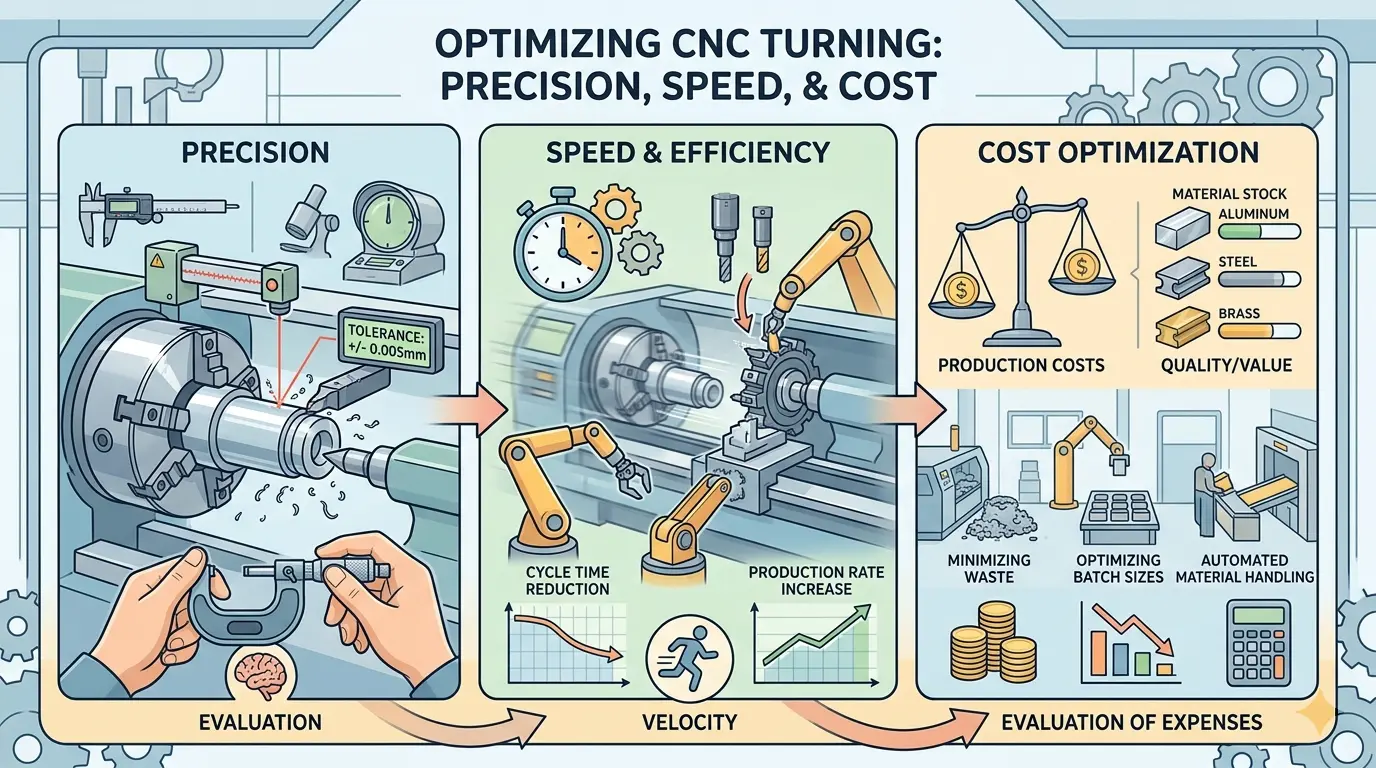
Procurement teams comparing CNC turning quotes often treat precision, speed, and cost as independent line items, but in real production they form a single interconnected decision. A quote is not a promise of machine hours; it is a compressed manufacturing plan that reveals how a supplier intends to route raw stock into accepted parts. Weak quotes hide route assumptions behind low numbers, while strong ones expose process control, inspection logic, and secondary operations. Before evaluating any bid, buyers must read the quote as a full production route, not a price sheet.
Precision, Speed, and Cost Are One Decision, Not Three
Buyers comparing CNC turning services often treat precision, speed, and cost as three separate columns on a comparison sheet. In real production, they are one interconnected decision. Precision depends on how the supplier plans the machining route, where it applies process control, and how well it actually reads the drawing. Speed is not spindle time alone—it includes material availability, setup load, inspection logic, secondary handling, and whether the quoted lead time reflects real capacity or optimistic scheduling. Cost is the sum of all of that, plus the risk the supplier left out of the price.
That is why a turning quote should be read as a compressed manufacturing plan. The supplier is not selling machine hours. It is proposing a route from raw stock to accepted parts. A good quote reveals how the supplier sees the part. A weak quote hides that view behind a low number or a generic promise.
For procurement teams, engineers, and owners sourcing turned parts, the most useful habit is to stop asking only whether the supplier can make the part and start asking how the supplier intends to make it repeatedly. If the route is vague, the price is probably vague too, even if the quotation sheet looks clean.
| Evaluation Area | What Buyers Should Look For | What Often Goes Wrong |
|---|---|---|
| Precision | Clear control of the features that drive fit, motion, sealing, or assembly | The supplier talks about “tight tolerances” without tying them to the real drawing |
| Speed | Lead time based on route stability, capacity, and required approvals | Buyers mistake fast quoting for fast production |
| Cost | A price that reflects turning, inspection, secondary work, and route risk honestly | A low quote leaves material, deburring, outside processing, or quality risk undefined |
Precision Means Repeatability on the Right Features
Almost every supplier describes itself as precise. That word is not useful until it is attached to the actual part. A serious turning supplier should be able to explain which features on the drawing deserve the strongest process control and why. On one component that may be a bearing diameter and a shoulder relationship. On another it may be a sealing surface, a concentric bore, or a thread that must assemble smoothly without hand chasing. Precision that is not tied to function is only marketing vocabulary.
This matters because turned parts rarely need the same level of control everywhere. When a supplier treats the whole drawing as equally critical, the price usually rises because too much process attention is spread across features that do not need it. When the supplier protects too little, the low quote eventually turns into rejects, rework, or arguments over acceptance. Strong turning services know how to separate function-driving geometry from general commercial finish.
Listen carefully to the language in the quote review. Does the supplier discuss datum logic, wall stability, burr risk, surface finish zones, and the features that actually matter in use? Or does the discussion stay at the level of “we can hold tight tolerance”? The more specific the conversation, the more likely the supplier has priced the work with real process understanding.
Speed Begins with Route Clarity, Not the Machine Calendar
Lead time gets distorted because buyers and suppliers often mean different things by “fast.” A buyer may hear a short lead time and assume rapid shipment. The supplier may only be describing how soon the job can enter a machine queue. Between those points lies the real route: material purchasing, bar preparation or blank prep, setup, first-article review, in-process inspection, deburring, secondary machining, surface treatment if required, final inspection, packing, and dispatch.
Turning work is especially vulnerable to this misunderstanding because many parts appear simple. A short shaft, bushing, spacer, or threaded pin can look like a quick machine job, but the route can still lengthen sharply if material needs confirmation, the part requires a secondary flat or cross hole, or the supplier plans to run the job through an overloaded cell. Lead time cannot be evaluated honestly until the whole chain is visible.
Ask what actually drives the promised delivery date. Is the route delayed by stock material? Does the part require new tooling or first-article approval? Is the job dependent on outside finishing? Does the supplier plan to run the turning internally but send the part elsewhere for heat treatment or coating? A lead time is credible when the supplier can explain what must happen between purchase order and shipment without hand-waving.
Cost Comparisons Fail When Suppliers Price Different Versions of the Same Job
The most common pricing mistake in turning sourcing is assuming that the RFQ sheet alone makes the job identical for every bidder. It does not. Two suppliers can look at the same drawing and build very different assumptions around setup discipline, inspection frequency, tool life, edge finish, secondary work, scrap allowance, and lot control. One supplier may price the route conservatively and clearly. Another may price only the most visible steps and leave important work undefined.
This is why unit price should never be read without route context. Does the price include edge break or only raw cut edges after turning? Does it include cleaning, thread verification, inspection records, packaging rules, or plating prep if needed? Are material certifications included? Is the job being priced around stable production or around an optimistic assumption that everything will run cleanly on the first try?
Low price can absolutely reflect good efficiency. But low price can also mean the supplier is transferring uncertainty to the buyer. Strong buyers do not reject a low quote automatically. They test whether the quote still makes sense after all expected route steps are made explicit.
Geometry and Material Explain Service Fit Better Than Sales Confidence
A supplier can be well managed, responsive, and still be the wrong fit for a particular turned part family. Geometry matters. Material matters. A short brass bushing, a thin-wall stainless sleeve, a titanium medical component, and a long steel shaft may all be “turned parts,” but they do not create the same process difficulty. A supplier strong on one family may be less effective on another.
Ask what kinds of turning work dominate the supplier’s real output. Does the shop mainly run bar-fed small components, larger chucking work, difficult alloys, precision concentric features, or turning-plus-secondary-process parts? That question often reveals whether the supplier’s price is based on actual familiarity or on the hope that the job is close enough to its normal mix.
Material fit matters just as much. Aluminum, stainless, brass, plastics, alloy steels, and tougher metals create different cutting behavior, burr formation, finish behavior, and tooling load. A credible quote reflects those differences. A weak quote often flattens them into a generic per-piece rate and hopes the part behaves kindly enough for the margin to survive.
Secondary Operations Are the Hidden Difference Between a Good Quote and a Painful Order
Many jobs described as turning services are not pure turning routes by the time the parts ship. They may need cross holes, flats, key features, milling, heat treatment, coating, marking, assembly prep, or washing to a defined cleanliness standard. The more the part depends on those added steps, the less useful it is to evaluate the supplier on turning alone.
This is where buyers frequently underestimate risk. A supplier may quote the turned geometry very competitively but rely on loosely coordinated outside processing for the rest. That is not automatically unacceptable, but it changes what “fast” and “low cost” really mean. Outside steps introduce lead time variability, lot-integrity risk, and another place where nonconformance can appear.
The useful question is not whether the supplier can manage one operation beautifully. It is whether the full route is coherent. If the supplier owns the full route in-house, that should be clear. If it uses outside partners, buyers should understand which operations those are, how the sequence is controlled, and who owns quality release at the end.
Inspection Discipline Separates Professional Turning Services from Opportunistic Quotes
Inspection language is another place where weak quotes often hide. A supplier may say that parts are checked carefully, but buyers need to know what that means in practice. Are critical diameters checked throughout the run or only during setup? How are threads confirmed? How is concentricity evaluated when the application depends on it? What happens if a feature trends toward the limit mid-batch? Is the final check tied to the real functional dimensions or only to a few easy-to-measure points?
This matters because good turned-part quality is not only about whether the first piece measures well. It is about whether the process stays under control as the batch runs. If a supplier’s inspection logic is weak, the part may look acceptable at first article and still drift later. Buyers should therefore prefer suppliers that can explain the check plan at the same level of clarity as the machining plan.
Strong inspection discipline does not always mean overcomplicated paperwork. It means the supplier understands which features need monitoring, how that monitoring is done, and how nonconformance is contained if something shifts.
The RFQ Quality Often Decides Whether the Quote Will Be Useful
Suppliers are easier to compare when the RFQ makes the drawing logic explicit. Buyers who only send the print and a quantity often receive prices that are superficially comparable and technically inconsistent. Better RFQs identify functional dimensions, highlight surfaces that matter, state material requirements clearly, define deburring or finish expectations, and disclose any secondary operations that are already known.
This is not about overloading the supplier with paperwork. It is about removing the exact assumptions that usually distort precision, speed, and cost. If a supplier has to guess whether the visible cosmetic face matters, whether the thread is assembly-critical, whether substitute material is acceptable, or whether plating comes later, the resulting quote may still be fast, but it will not be tightly comparable to a better-informed quotation from another source.
In practical sourcing, a cleaner RFQ often produces more useful price gaps than a wider supplier search. It reduces the number of surprises buried inside the offer.
Better Supplier Questions Reveal Whether the Quote Is Built on Real Process Ownership
The most effective supplier questions are not adversarial. They are clarifying. Which features on this part are the main process risk? What is the biggest cost driver? What actually controls the lead time on this route? Which operations are internal and which are external? How will the supplier check the critical features through the run? What assumptions in the quote should the buyer confirm before release?
These questions help because they force the supplier to expose how it sees the job. A strong turning service usually responds with operational clarity: which geometry is difficult, how the setup will be handled, where the route might slow down, and why the price is shaped the way it is. A weaker supplier often stays at the level of generic assurance because the route itself has not been thought through deeply enough.
The buyer is not looking for the supplier that talks the most. The buyer is looking for the supplier that makes the route understandable.
When the Higher Quote Is Actually the Safer Commercial Decision
Not every higher quote is better, but higher pricing sometimes reflects costs that a disciplined supplier chose to make visible rather than bury. That may include stronger inspection coverage, better-defined handling of outside processing, more realistic tooling allowance, cleaner material control, or a lead time that reflects real capacity instead of wishful scheduling. Those elements do not always win the price comparison, but they often reduce the total cost of failure.
Buyers should therefore ask what the higher price is buying. If it buys clearer route ownership, stronger repeatability, and fewer late surprises, it may be cheaper overall than a low quote that depends on optimistic assumptions. The mistake is not paying more. The mistake is paying less for a route that cannot reliably deliver what the drawing and schedule actually require.
Read the Quote as a Route, Not as a Promise
The strongest CNC turning services are not always the ones with the lowest unit price, the fastest quoted lead time, or the broadest precision claim. They are the ones that can explain the route clearly enough that the buyer understands where the real difficulty sits, how quality will be protected, and why the cost looks the way it does. Precision, speed, and cost become useful only when they are tied back to the drawing, the material, the sequence of operations, and the inspection method.
When buyers compare turning services on that basis, the conversation becomes far more practical. They stop rewarding quotes that only sound good and start rewarding quotes that are built on real process ownership. That shift usually leads to better suppliers, fewer late surprises, and much stronger decisions than comparing price and lead time in isolation ever can.