Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
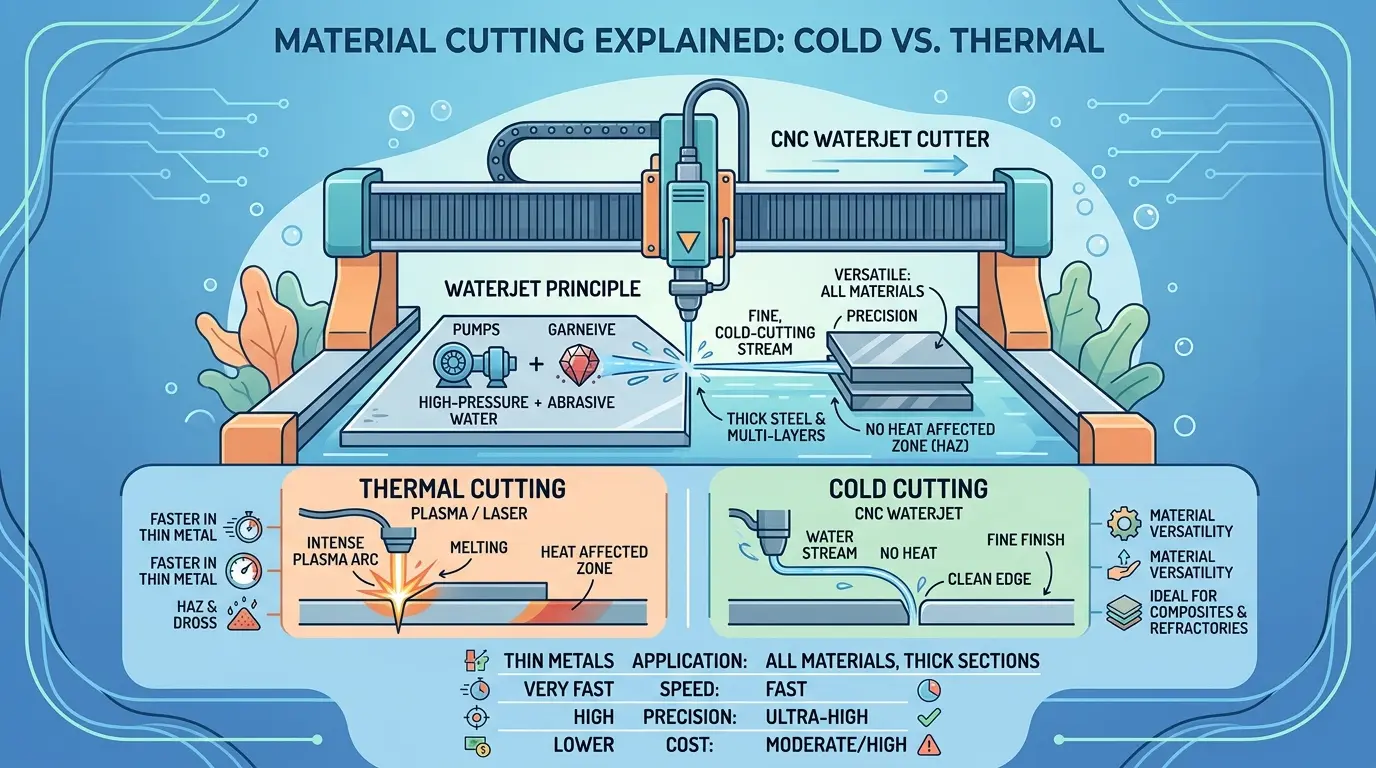
Define the workload before judging quoted cycle times on a laser, plasma, or water jet, ask what the process does to the material at the kerf. Thermal cutting conducts heat into the surrounding stock, and that energy shows up later as warped parts, burned coatings, delaminated layers, or hardened edges that force unplanned straightening and grinding. This article walks through the selection logic that matters on the floor: when part integrity after the cut outweighs raw speed, and when a cold-cutting route eliminates rework that thermal methods keep generating. The decision hinges on edge condition, not just machine rate.
Why Heat Is the Real Variable in Cutting Process Selection
Most cutting-machine comparisons start with price and speed. In practice, those are rarely the factors that determine whether a job runs profitably. The more decisive variable is what the process does to the material while it separates it. Thermal cutting methods—laser, plasma, oxy-fuel—rely on heat to melt or burn through stock. That heat does not stay neatly contained at the kerf. It conducts into the surrounding material, and the consequences show up downstream: warped parts, burned coatings, delaminated layers, discolored edges, hardened cut faces, and secondary cleanup that nobody budgeted for.
A CNC water jet cutter approaches the same separation task without that thermal input. It uses high-pressure water, often with an abrasive additive, to erode the material mechanically. The edge leaves the machine in a condition much closer to the parent material. That single difference changes the entire selection logic. The question stops being “how fast can this machine cut?” and becomes “what condition does the part need to be in when it leaves the cut?”
This is not an argument that water jet is universally superior. It has its own cost structure, taper characteristics, abrasive consumption, and cycle-time limits. But when heat is the root cause of rework, distortion, or material damage, cold cutting eliminates a problem that faster thermal processes keep recreating. In those jobs, water jet wins not by being the quickest machine on the floor, but by leaving the part in a usable state.
| Decision Factor | Why Water Jet Can Be Strong | When Thermal Cutting May Still Win |
|---|---|---|
| Heat sensitivity | Edge stays closer to original material condition | Material tolerates heat and throughput is the priority |
| Distortion risk | Lower thermal influence reduces warping and local damage | Simple geometry and thermal cleanup is acceptable |
| Coated, layered, or mixed materials | Cold cutting avoids burn and separation issues | Simple stack-up and edge condition is not critical |
| Thick or difficult stock | Attractive when hot cutting creates too much edge compromise | One material family dominates and high-speed cutting is acceptable |
Edge Condition, Not the Water, Is the Real Selling Point
The reason to choose water jet is not that it uses water. It is what the process does—or more precisely, what it avoids doing—at the edge of the part. When a laser or plasma arc cuts material, the edge can emerge with a heat-affected zone even when the dimensional result is perfectly acceptable. In many shops, that is fine. The part goes to the next operation and nobody notices. In others, it is the source of recurring problems that get blamed on everything except the cutting process.
Consider what happens after the cut. If the next operation is welding, a heat-hardened edge can create inconsistent penetration. If the part must remain flat, thermal stress can introduce bowing that requires straightening. If the material has a coating or laminate, heat can burn or separate the layers at the cut line. If the edge is visible in the finished product, discoloration becomes a cosmetic defect. In each case, the thermal process looked productive at the machine but created work for someone else downstream.
Water jet avoids that entire category of problems. The edge is mechanically eroded, not thermally altered. That makes the process valuable when the buyer cares about what happens after separation, not just about making the cut itself.
Material Sensitivity Determines Whether Cold Cutting Has Real Value
Some materials handle heat well enough that thermal cutting remains the efficient, economical choice. Mild steel plate, for example, cuts quickly with plasma or laser, and the heat-affected zone is often acceptable for the application. Other materials expose the limits of thermal cutting quickly. Coated stock, laminates, composites, thicker plate, reflective materials, and sensitive alloys all shift the balance toward cold cutting.
The material does not need to be exotic for this logic to apply. A painted panel, a laminated sheet, or a stacked assembly can all suffer from thermal input even if the base material is common. The key question is simple: what happens to this material when it is cut hot? If the answer is “nothing that matters,” water jet may not be necessary. If the answer includes hardening, discoloration, delamination, distortion, or uncertainty near the cut zone, cold cutting becomes relevant.
The stronger the material’s sensitivity to heat, the more the decision shifts away from nominal cycle time and toward part integrity. That is often where water jet earns its place economically, even when it does not lead on raw cutting speed.
Counting the Full Route: Distortion and Secondary Cleanup
Thermal cutting looks fast until the entire route is considered. If the part leaves the machine needing straightening, edge grinding, coating repair, or extra care before the next operation, the apparent speed advantage shrinks. Water jet often appears slower at the machine and stronger in the total process because it reduces what has to happen afterward.
This is one of the most important buying lessons in cutting technology. A process should not be judged only by how quickly it makes the kerf. It should be judged by how ready the part is for what comes next. If cold cutting preserves flatness, reduces burn damage, or protects material condition well enough to eliminate secondary work, its overall productivity can be better than the nominal machine cycle suggests.
That does not mean water jet always wins on total route efficiency. It means buyers need to count post-cut work honestly. Thermal methods are only cheaper when the problems they introduce are either acceptable or inexpensive to resolve.
Thick Stock and Mixed-Material Work Favor Cold Cutting
Water jet is frequently considered when thickness, material variation, or layer structure make thermal cutting less attractive. Thick sections can still be cut thermally, but the edge condition and downstream consequences become harder to ignore as material mass increases. Heat has more time to conduct into the surrounding material, and the resulting distortion or metallurgical change is more pronounced.
Mixed-material and layered products create even greater complications because heat does not affect all layers equally. A composite with a metal core and polymer skin will respond differently to thermal input at each interface. A coated panel may burn at the surface while the substrate remains unaffected. Water jet approaches these jobs without forcing the material combination into a heat-led compromise.
This is especially valuable in prototyping and custom work, where the buyer needs one process that can handle difficult materials without spending days managing unexpected edge behavior afterward. In volume production, the decision becomes more economic and should be tied to repeat job data, but the same principle holds: if cold cutting removes a recurring problem, the process may pay for itself through route stability.
Water Jet Still Has Its Own Edge Considerations
Cold cutting does not mean perfect cutting. Water jet avoids major thermal effects, but the edge still has to be evaluated for the application. Taper is the most common concern—the jet stream loses energy as it passes through the material, which can produce a slightly wider cut at the bottom of the part than at the top. Surface condition, kerf width, abrasive effects, and finish expectations all remain important.
A buyer choosing water jet only because it sounds gentle can still be disappointed if the actual edge requirement was never defined clearly. The process is strongest when the buyer knows exactly what the edge needs to preserve and what imperfections remain acceptable. Is the cut edge final, or will it be machined later? Is cosmetic appearance important? Does the part mainly require dimensional correctness with minimal thermal damage? Is slight taper acceptable in the real assembly, or does the downstream use demand tighter edge behavior?
These questions determine whether water jet is solving the right problem for the right reason. Without that clarity, one vague process promise simply replaces another.
The Value of What Water Jet Avoids
Some technologies win because of what they do better. Water jet often wins because of what it avoids. It avoids burning coatings. It avoids introducing a heat-affected zone. It avoids some of the warp and local metallurgical concerns that thermal cutting can create. It avoids making the next department compensate for a process choice that looked fast in isolation.
This negative-space advantage is easy to undervalue during equipment comparison. Buyers compare machine rates and overlook the cost of protecting the material from a process that is too aggressive for the part. Water jet may not look like the most productive cutter during a showroom conversation, but in the right job it is the cleaner route because it avoids creating defects the shop would otherwise have to spend time managing.
That is also why water jet should not be selected just for versatility. It should be selected when avoiding thermal side effects has real economic or quality value.
Thermal Cutting Still Wins Many Jobs
An accurate water-jet buying guide has to say this clearly: thermal cutting remains the better answer for many parts. If the material handles heat well, if edge cleanup is minimal, if production speed dominates the economics, and if downstream processes are not troubled by thermal effects, then laser, plasma, or other hot methods may remain the stronger route. Water jet is not better simply because it is more conservative toward the material.
Process choice should stay tied to the real part. If a shop chooses water jet for a job that does not need its cold-cutting advantage, the process may simply add cost and slow throughput. The mistake is not preferring thermal cutting. The mistake is preferring it when heat is the very problem the route is struggling to control.
Good buying discipline compares processes around the actual pain point. If the pain point is speed on tolerant material, thermal cutting often wins. If the pain point is heat damage, cold cutting becomes much harder to ignore.
Production Volume Refines the Economics, Not the Logic
Water jet can make sense in prototyping, low-volume custom fabrication, and repeated production, but the reason changes slightly in each case. In prototype work, material flexibility and route safety often matter most. In low-volume custom work, avoiding costly mistakes on difficult materials can outweigh slower cutting. In repeated production, the economics become more demanding, and the buyer should study whether the cold-cutting advantage still protects enough value to justify the operating model.
The underlying logic, however, stays the same. Does the process leave the part in a better condition for what comes next? If yes, the process deserves consideration. If not, its slower cycle time or higher operating burden may be hard to defend at scale.
Volume should refine the water-jet decision, not replace the material logic behind it.
Questions to Ask Before Committing to Water Jet
Useful water-jet questions are tied to the material and the route after cutting:
- Does the current or likely thermal process introduce distortion, discoloration, or a problematic heat-affected edge?
- Does the material include coatings, laminates, or mixed layers that respond badly to heat?
- How much secondary edge work is acceptable in the current route?
- Is the cut edge final, intermediate, or cosmetic?
- Does the part need to remain flat or materially stable near the cut zone?
- Is the job occasional prototype work, mixed low-volume cutting, or repeated volume?
- Does the route gain enough from cleaner edge condition to offset slower machine time?
If water jet is being considered primarily because it sounds flexible, that is not yet a strong enough reason. If it is being considered because thermal cutting keeps creating an avoidable problem, the case is much stronger.
Choosing Cold Cutting for the Right Production Reason
CNC water jet cutting makes the most sense when cold cutting solves a problem that thermal cutting keeps creating. Its value is not just that it can cut. Its value is that it can cut while leaving the surrounding material closer to its original condition. That matters on heat-sensitive, thick, coated, layered, or distortion-prone work where the edge condition influences what happens next.
Water jet should not be treated as a universal replacement for thermal machines, and thermal cutting should not be dismissed where it clearly fits the job. The right decision is the one that leaves the part in the best usable state at the right total cost. When heat is the hidden cause of rework, distortion, or material damage, water jet often becomes the stronger route not because it is faster, but because it stops the route from creating the wrong kind of damage in the first place.