Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
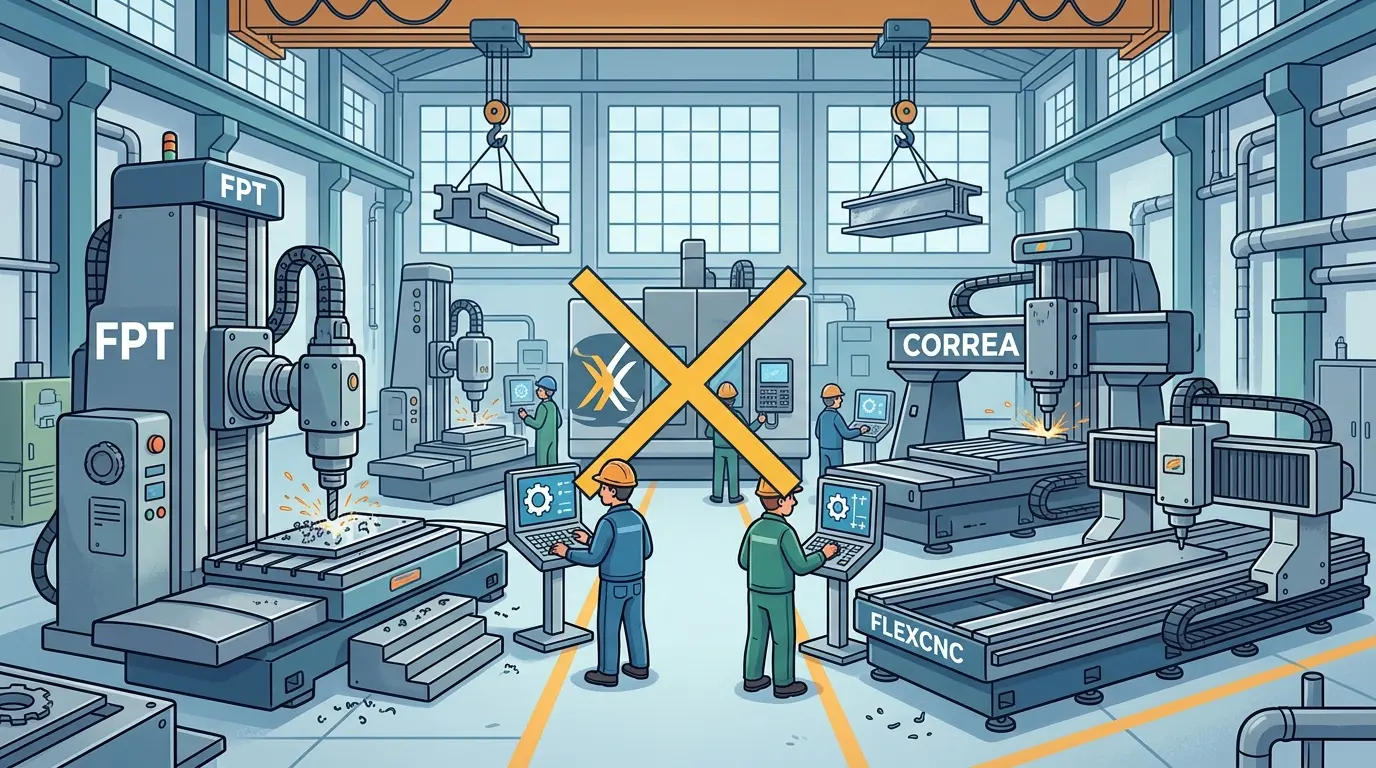
Industrial milling procurement often stalls when buyers compare FlexCNC, FPT, Correa, and similar names side by side without first defining the machine class their work actually demands. These brands are not interchangeable substitutes: FlexCNC-type platforms suit industrial routing on lighter large-format materials, while FPT and Correa belong in heavier bridge, gantry, or floor-type milling conversations for demanding cut loads. Shortlisting before separating these application families produces a structurally unreliable list. The decision hinges on identifying your dominant part family, material removal burden, and workflow fit firstâthen comparing brands that genuinely solve that same production problem.
Why These Brands Keep Appearing in the Same Search
When buyers type FlexCNC, FPT CNC, Correa CNC, and other industrial milling names into one comparison, the search usually reflects a procurement problem, not a brand problem. The buyer knows a serious milling platform is needed, but the machine class that actually fits the work has not been defined yet. That distinction matters more than any logo recognition.
These names all belong to the broad industrial machining conversation, but they are not direct substitutes. FlexCNC-type platforms typically serve industrial routing and lighter large-format work. FPT and Correa machines belong in heavier large-part milling discussions involving bridge, gantry, or floor-type architectures. Comparing them as if they solve the same job produces a shortlist that looks thorough but is structurally unreliable.
The first rule in any shortlist discussion is to separate machine class before comparing brand reputation. Start with the work. Are you machining large plates, structural weldments, mold bases, patterns, fixtures, or wide-format aluminum components? Do the parts demand deep heavy cutting, long travels, five-face access, or mainly plate-style processing with production flexibility? These answers determine the correct machine architecture far more than brand familiarity does.
| Shortlisting Question | Why It Matters Before Brand Comparison | What Goes Wrong If Skipped |
|---|---|---|
| What part size and geometry dominate? | Determines whether you need routing-style flexibility, gantry-style heavy milling, or another format | Buyers compare unlike machines as if they solve the same job |
| What materials and removal demands matter? | Changes the rigidity and spindle burden the machine must carry | A machine may sound industrial yet still misfit the actual cut load |
| Is the work high-mix or dominated by a few large-part families? | Affects flexibility, setup logic, and route integration | The shortlist rewards names instead of production fit |
| What support model do you require? | Installation, training, and recoverability matter as much as table travel | The brand looks right until downtime becomes the real cost |
FlexCNC-Type Searches Usually Signal an Industrial Routing Requirement
When FlexCNC appears alongside heavier industrial milling brands, the first question should be whether the real job is closer to industrial routing logic or closer to heavier machine-tool logic. That is not a judgment of quality. It is a question of application fit.
Some shops need larger-format routing behavior on lighter materials, aluminum plate, plastics, composites, or broad-format work where a heavy traditional large-part mill is not the most natural answer. Others genuinely need more rigid large-part milling for demanding cut loads and higher-value components. If buyers do not make this distinction early, the shortlist becomes confused. A brand can look cheaper, larger, or more accessible only because it is being judged inside the wrong comparison class.
The correct question is what kind of work the machine is meant to support repeatedly. A shop running varied panel work, acrylic sheets, composite blanks, or aluminum plate with moderate tolerance demands will find more value in a routing-style platform with flexible tooling and faster positioning. A shop cutting deep pockets into steel weldments or hogging material from large blocks needs the rigidity and spindle stability that only a heavier machine-tool architecture provides.
FPT, Correa, and Similar Names Belong in a Heavier Large-Part Milling Discussion
Brands commonly associated with larger industrial milling platforms appear when buyers deal with more demanding workpiece mass, substantial material-removal expectations, or a machine-tool route closer to heavy machining than to industrial routing. The important point is not the brand label itself. It is the class of work the brand is usually considered for.
Buyers should ask whether their workload truly belongs in that heavier conversation. If the shop needs structural rigidity, long-travel large-part machining, broader spindle stability under harder cuts, or high-value components where machine behavior under load matters greatly, then those names deserve closer attention. If the plant really needs flexible routing-style processing on lighter work, the same shortlist may be structurally wrong from the beginning.
Brand grouping should follow application family. When it does, the shortlist becomes a real procurement tool instead of a list of search results. A bridge-type or floor-type milling machine from FPT or Correa brings different workholding logic, chip management, and spindle behavior than a gantry router. Understanding which one matches your dominant part family prevents expensive misclassification.
The Best Shortlist Starts With Part Families, Not With Spec Sheets
Industrial machine procurement often becomes spec-heavy too early. Table size, travel, spindle figures, control options, and axis counts are useful later, but they are poor first filters if the part family is not already clear. Buyers should first describe what the machine must do most of the time.
What is the largest common workpiece? What material mix dominates? How many setups are typical? How sensitive is the work to rigidity, finish, or positional accuracy over longer distances? Is the goal flexibility across varied jobs or efficiency around a narrower family of large parts?
Those questions produce the right shortlist because they reveal whether different brands are solving the same real production problem. Once that is clear, specifications become meaningful instead of merely interesting. This step matters especially in mixed-capability plants that do some plate work, some large-part machining, some composite or aluminum processing, and some prototype or tooling work. In those environments, the temptation to buy a do-everything machine is high. The better answer is often to identify which work truly drives the business and shortlist around that dominant value instead of around imagined versatility.
Support, Installation, and Recoverability Belong Near the Top of the Filter
In larger industrial milling purchases, support quality matters because downtime is expensive and installation is rarely trivial. Buyers often spend too much time comparing machine features and too little time comparing who will help the plant keep the route stable after commissioning. That is a mistake, especially when the machine is expected to become central to plant capacity.
Brand shortlisting should include service reach, commissioning quality, spare-parts access, training, and the practical reality of who helps when something drifts or stops. A technically strong machine can still be the wrong choice if the support model is too weak for your location, your staffing profile, or your uptime requirements.
This is one of the areas where buyers should be least romantic about brand name. A machine is not just bought for its best day. It is bought for its recoverability under ordinary industrial life. Ask each supplier how many service technicians cover your region, what the response-time commitment is, and whether critical spindles or controls are stocked locally. The answers separate marketing claims from operational reality.
Floor Layout and Material Handling Can Disqualify a Brand Before Specs Ever Matter
Large-format and industrial milling purchases affect more than cutting time. They influence crane access, fork movement, floor loading, workholding strategy, CAM workflow, tooling storage, inspection routing, and how parts move before and after machining. A good shortlist usually becomes smaller when plant integration is reviewed honestly.
A brand may offer an impressive machine, but if the surrounding factory cannot load, fixture, program, and inspect the parts efficiently on that platform, the theoretical value will be much harder to realize. Conversely, a machine that looks less dramatic on paper can become the smarter choice because it fits the plant’s real process more cleanly.
Consider the full material flow. How does a 3-meter plate reach the table? Does the machine design allow overhead crane access across the full travel? Can the workholding system handle the part distortion you see with your current processes? Where does the part go after machining for inspection or secondary operations? The right shortlist depends on machine fit plus plant fit. Buyers who separate those two concepts avoid many expensive category mistakes.
Buyers Should Shortlist for Dominant Work, Not for Edge Cases
Another common error is letting rare edge cases dominate the shortlist. A shop may occasionally machine one especially large or awkward part and then build its entire comparison process around that outlier. That often distorts the decision. Industrial machine selection should usually reflect the dominant part family, not the rare exception.
This does not mean edge cases should be ignored. It means they should be weighed honestly. If the shop’s main value is in long repeated work on one class of parts, shortlist around that class. If the business wins work because it can handle a wide range of large parts with reasonable efficiency, shortlist around flexibility. But do not let one unusual drawing push you into the wrong machine class for the other 80 percent of the business.
That is one of the most practical ways to keep a shortlist disciplined. Document the last six months of production by part family, material, and cycle time. The pattern that emerges should drive the machine class decision, not the occasional job that required special arrangements.
High-Mix Plants and Dedicated Large-Part Plants Should Not Shortlist the Same Way
Two factories can both say they need industrial milling and still require very different brand shortlists because their production logic differs. A high-mix plant may value broader usability, changeover flexibility, and route adaptability. A more dedicated large-part plant may value sustained stability and heavy-duty behavior around a narrower family of components.
Buyers should state the operating model clearly before comparing names. Are you building a shortlist for a flexible plant that wins work through variety? Or for a plant that wins through concentrated capacity on a more stable family of large parts? The answer should change who makes the shortlist and why.
Without that filter, brand research becomes directionless. The buyer ends up comparing reputation rather than machine logic. A high-mix job shop running prototype work and short production runs needs quick changeovers, flexible workholding, and a control that operators can adapt to new jobs rapidly. A plant producing the same large structural component every week needs sustained cutting stability, predictable tool life, and a machine that holds tolerance over long cycles. These are different purchasing decisions.
Control, Automation, and Axis Counts Should Be Compared Late, Not Early
Once the right class of machine is clear, then it becomes sensible to compare control preferences, automation options, tool-management strategies, and axis layouts. These are meaningful differentiators, but only after the shortlist already contains machines built for the same job family.
When buyers compare those details too early, they often overvalue features that sound advanced but matter less than the machine’s basic application fit. An elegant control does not fix a misclassified machine. A higher axis count does not erase an application mismatch. The strongest procurement sequence always keeps architecture and workload ahead of feature fascination.
This approach usually shortens the decision cycle because the conversations become more concrete. Instead of debating control brands in the abstract, you can ask how the control handles your specific CAM post-processor, how tool offsets are managed across long production runs, and what the automation interface looks like for your planned pallet or shuttle system.
A Useful Shortlist Is Usually Much Shorter Than the Internet Suggests
Search results encourage buyers to compare many names at once. Real procurement becomes better when the list becomes smaller. A disciplined shortlist may contain only a few brands because the plant has already filtered by machine class, part family, support need, and workflow compatibility. That is not a limitation. It is a sign that the process is becoming more intelligent.
If a buyer still feels compelled to compare very different industrial milling names in one conversation, that often means the machine category has not yet been defined clearly enough. The best next step is usually not more brand research. It is a better understanding of the work.
How Buyers Should Use This Kind of Search Productively
If you are searching FlexCNC, FPT CNC, Correa CNC, and similar names together, treat that search as a signal to step back. Ask first whether your plant needs industrial routing logic, heavy large-part milling logic, or another specific machine class. Build the shortlist only after you know which of those problems you are actually trying to solve. Then compare the brands that genuinely live in that same problem space on support, route fit, plant integration, and recoverability.
That sequence turns a broad brand search into a useful procurement method. Without it, the shortlist remains too mixed to be reliable no matter how much time is spent collecting brochures.
Demonstrations Should Be Built Around Your Dominant Job Family
Once the shortlist is reduced to the right machine class, buyers should become much more demanding about how brands are evaluated. A generic demonstration may be informative, but it rarely answers the question that matters most: how well does this platform support the kind of work our factory actually runs?
The strongest brand review happens when the supplier discussion is anchored around your dominant part family, your loading condition, your material burden, and the production discipline your plant really needs. Bring your own CAD files. Ask to run your own test cuts. Request a cycle-time estimate based on your actual tooling strategy and spindle speed limitations.
This approach quickly exposes whether a brand belongs on the shortlist for sound reasons or only because its general reputation sounded strong at the search stage. A machine that looks impressive in a generic showcase may be much less convincing when the conversation turns to real workholding, real part access, real setup behavior, and the specific workflow limits of your facility.
Price Anxiety Should Not Recreate a Category Mistake
Buyers also need to separate capital-cost discomfort from machine suitability. In larger industrial purchases, it is easy to assume that the more expensive or more massive platform must be the more serious answer. But seriousness only matters when it matches the dominant production problem. A plant buying too much machine for the wrong class of work is not buying safety. It is buying mismatch.
Shortlist logic should keep returning to machine architecture, material route, workflow burden, and support. If the part family does not demand a heavier class of solution, heavier branding does not improve the decision. If the work truly does demand that class, then lower-cost alternatives from another category should stop being treated as equivalent substitutes. The shortlist becomes far cleaner once the buyer stops comparing seriousness in the abstract and starts comparing operational fit.
Shortlist the Machine Logic First, Then the Brand
Buyers should shortlist industrial milling brands only after they have identified the machine class their work truly needs. Searches that combine FlexCNC, FPT CNC, Correa CNC, and other industrial names often mix platforms built for different types of large-format or industrial machining work. The first task is therefore not ranking the brands. It is separating the applications.
Once that is done, the best shortlist is the group of brands whose machine architecture, material fit, support model, and workflow compatibility match the actual part family. That is how buyers move from brand curiosity to a defensible industrial machine decision. In large machine procurement, the strongest shortlist is not the loudest one. It is the one that follows the work most honestly.
For shops that land on the routing side of that distinction, reviewing industrial router and nesting platforms alongside the milling conversation can clarify the boundary between the two machine classes. The goal is not to blur the categories further but to confirm which one your production pattern actually belongs to before you commit capital.