Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
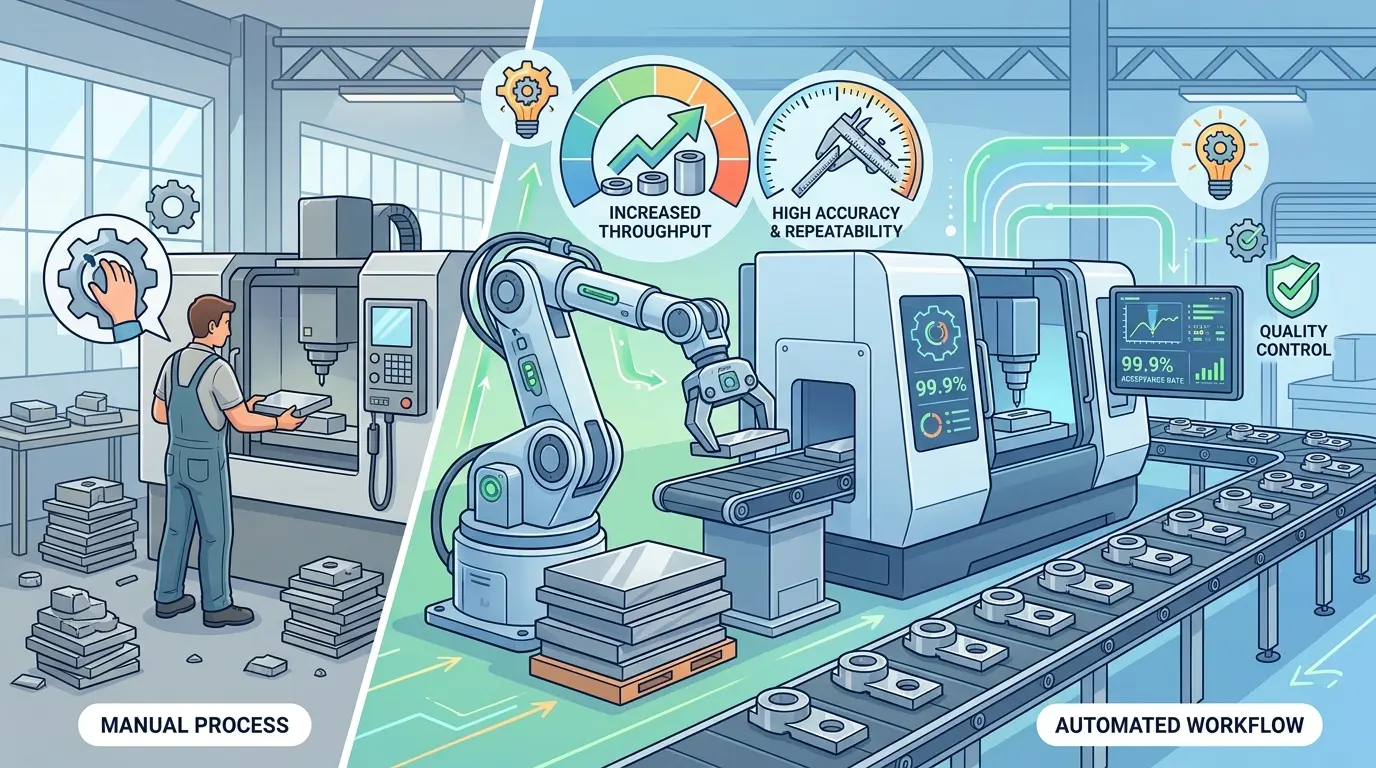
Most shop-floor automation conversations stall on robots, yet the real leverage for CNC buyers sits in the layers that control variation before the spindle even starts. This article forces a practical reassessment of how accuracy, throughput, and repeatability actually improve: not through lights-out theater, but through probing routines, disciplined tool offsets, pallet systems, and locked program release. The decision that matters is not which accessory sounds advanced, but which layer attacks the largest source of uncontrolled variation in your specific process—because automating a weak foundation only accelerates confusion and unstable output.
Why CNC Automation Deserves a Broader Definition
Most shop-floor discussions about CNC automation start and end with robots. That framing misses where the real value sits for most manufacturers. Automation begins much earlier: when manual positioning decisions become stored routines, when offsets are managed systematically, when probing replaces guesswork, and when the machine moves from one valid job to the next without relying on an operator’s memory.
Understood that way, CNC automation improves more than labor utilization. It improves the predictability of the process itself. Accuracy rises when datums and tool offsets are controlled consistently. Throughput rises when non-cutting minutes shrink. Repeatability improves when the same verified routine runs across shifts instead of being rebuilt from scratch in each operator’s head. The gains are real, but they are not automatic. Automation rewards disciplined processes and exposes weak ones faster.
Controlled Repetition, Not Lights-Out Theater
The most useful definition of CNC automation is simple: any layer that reduces uncontrolled variation in how work is set up, measured, moved, and repeated. That includes automatic tool changers, probing, pallet systems, bar feeders, loaders, centralized program release, and software templates that standardize tool libraries and cycle structure. None of those features matter because they sound advanced. They matter because they reduce decision noise around each part.
This is why shops with modest automation often outperform shops with more dramatic hardware but weaker discipline. If the process is standardized, the same machine produces stable output shift after shift. If the process is vague, expensive automation simply runs mistakes faster.
So automation should not be framed as “less labor” or “lights-out theater.” It is better understood as controlled repetition with fewer opportunities for accidental variation. Once buyers understand that, investment decisions become much more rational.
Accuracy Improves When the Process Shares a Stable Reference Language
Accuracy improves when the machine and the process speak a common reference language. In a heavily manual environment, part location may depend on feel, repeated indicating, and local habits that vary by operator. In a stronger CNC automation environment, work coordinate systems, tool length offsets, probing routines, and machine compensation create a more repeatable path from raw stock to finished feature.
On-machine probing is especially valuable because it allows the machine to confirm where the part actually is instead of assuming the setup is perfect. That reduces cumulative error and supports in-process verification on critical jobs. Tool management matters just as much. When tools are measured consistently and wear offsets are adjusted deliberately, the process does not have to rely on last-minute intuition to protect tolerance.
But automation does not erase weak fundamentals. If the fixture moves, the stock varies, thermal behavior is unstable, or the probing routine itself is poorly maintained, accuracy still suffers. The difference is that automated systems reveal those weaknesses more quickly because the same bad condition repeats more consistently.
Throughput Gains Come From the Minutes Around the Cut
Most throughput gains from CNC automation come from the time surrounding the cut, not only from the cut itself. Shops often obsess over feed rates and rapid speed while ignoring the minutes lost to repeated setup entry, tool searching, waiting for the correct program, manual loading delays, verification pauses, or uncertainty around job release.
Automation attacks those losses in several ways:
- Automatic tool changers reduce manual interruption between operations.
- Pallets or quick-change fixtures reduce idle time between jobs.
- Program management systems prevent wrong-file delays.
- Feeders and loaders keep spindle-ready work moving.
- Probing reduces hand-checking time.
- Digital labeling and job sequencing prevent a good machine from waiting on basic instructions.
In practice, throughput rises when more of the shift becomes controlled production time instead of preparation, hesitation, rechecking, or recovery.
Repeatability Is Often the Most Valuable Outcome
Accuracy gets more attention because it is easy to explain, but repeatability is often the more valuable business result. A part made once to size is useful. A part made the same way every time, by different people on different shifts, is what production systems actually need.
Repeatability improves when revisions, tools, fixtures, offsets, inspection checkpoints, coolant condition, and handoff rules are all governed deliberately. CNC automation supports that because the machine does not improvise unless people let it. That may sound obvious, but it is one of the biggest economic advantages of automation. A stable process can be taught, documented, audited, and improved. An informal process depends too heavily on memory and heroics.
This is also why quality teams usually value automation when it is implemented well. Stable routines produce cleaner histories, clearer traceability, and better root-cause analysis when something starts to drift.
Different Automation Layers Solve Different Problems
Not every shop needs the same automation stack. The right layers depend on part mix, lot size, staffing, and capital tolerance. Still, most automation value tends to come from a few recurring areas, each solving a different problem:
- Automatic tool changing reduces manual wrench time and allows more complex jobs to run in one cycle.
- Probing supports setup verification and in-process correction.
- Pallets and quick-change workholding protect spindle time by moving loading work outside the main cut cycle.
- Material handling automation extends productive runtime when raw stock is consistent enough to trust.
- Software automation, including templates, locked tool libraries, and centralized file release, reduces variation before the machine even starts.
These layers should not be treated as interchangeable signs of sophistication. A shop may gain more from disciplined probing and file control than from a loader. Another may gain more from pallets than from adding more CAM seats. The right sequence depends on where instability currently lives.
Start by Asking Where Variation Enters
Before buying automation, ask where the process actually loses control. Does variation enter at setup? At material loading? At tool measurement? At revision release? At operator handoff? At inspection? The answer matters because automation only pays back cleanly when it attacks a real source of waste.
For example, if the biggest problem is wrong or outdated programs reaching the machine, adding a part loader will not fix much. If the main problem is long idle time between repeated fixtures, a pallet system may help more than yet another manual quality check. If dimensional drift is recurring because stock origin is inconsistent, probing may create more value than another spindle-speed conversation.
The practical point is simple: do not buy automation as a category. Buy the layer that attacks the largest source of uncontrolled variation.
The Hidden Requirements Behind Good Results
Buyers sometimes expect automation to compensate for weak organization. In reality, automation raises the value of fixturing, tool management, maintenance, software discipline, and revision control. The machine can only automate what the process defines clearly enough to repeat.
That means tooling libraries need to stay organized. Fixtures need to locate reliably. Maintenance needs to happen before drift appears in finished parts. Program revisions must be governed so the correct file reaches the correct machine with the correct setup assumptions. Shops that ignore those requirements often conclude that automation “did not deliver,” when the real mistake was treating automation as a hardware purchase instead of a process commitment.
Maintenance becomes especially important once automation increases runtime. Bearings, sensors, probes, tool changers, vacuum systems, conveyors, and loading devices all become more central to output once the process depends on them every shift. If maintenance remains reactive, automated capacity erodes quickly.
People Still Matter, But Their Work Moves Upstream
Automation does not remove the need for skilled operators. It changes where their skill matters most. Instead of spending the shift on repeated positioning or routine loading, operators increasingly become process monitors, exception handlers, and first-article decision makers. They need to recognize bad sound, poor chip behavior, unusual finish, drifting offsets, tool wear signals, or a labeling mismatch before those issues spread through a batch.
Programmers and manufacturing engineers feel the change as well. More standardized automation means more value from clean templates, better setup sheets, verified posts, and disciplined data handoffs. Maintenance teams see a similar shift. As automation rises, reactive fixing becomes more expensive, so predictive habits become much more valuable.
In other words, automation increases the importance of process stewardship. The work becomes less about repeated manual action and more about protecting system stability.
Benefits Arrive in Different Orders on the Shop Floor
On paper, people often describe automation benefits in a neat order: first accuracy, then throughput, then repeatability. Real plants often experience the sequence differently. Some see repeatability first because the same setup begins behaving more consistently. Some see throughput first because setup friction falls immediately. Some see accuracy first when probing or better tool control replaces manual variation.
This matters because buyers should not expect every automation layer to improve every metric equally on day one. A pallet system may help throughput dramatically while changing dimensional capability only indirectly. Probing may tighten setup accuracy without adding much raw capacity until the team changes how it sequences jobs. Software templates may reduce repeat mistakes before anyone notices a gain in spindle hours.
The right expectation is not instant perfection. It is targeted improvement in the category of variation the automation layer is designed to control.
The Biggest Mistake Is Automating Disorder
The most expensive automation mistake is not buying the wrong accessory. It is automating a weak process. If incoming material varies, fixtures are inconsistent, the tool library is messy, and the team lacks revision discipline, automation will accelerate confusion. It will look efficient while producing unstable output.
That is why the first automation investments often belong in standard work, setup clarity, measurable control points, and process documentation. Once those exist, more advanced automation layers have something solid to amplify. Without that foundation, the machine may move faster while the plant does not actually produce more good parts.
A useful rule is this: if people cannot describe the current process clearly, the machine will not automate it reliably.
Automation Looks Different Across Production Families
In metal machining, automation often centers on probing, pallets, feeders, tool management, and part handling. In woodworking, the pattern is different. Automated nesting, drilling coordination, labeling, loading, unloading, and downstream part identification often matter more than the pallet logic common in machining centers. In laser work, job sequencing, alignment, exhaust stability, and nesting discipline matter. In stone processing, profile consistency, tool libraries, water delivery, and repeatable finishing logic matter.
That is why automation should be judged by process family rather than by a generic technology checklist. A panel factory and a precision machining cell both benefit from automation, but the value sits in different layers.
Pandaxis is useful here because its product categories naturally force line-level thinking. In panel production, CNC nesting machines only create real gains when sheet flow, labeling, and downstream assembly logic are ready. Different machine family, same lesson: automation works when the sequence is coordinated, not when one machine is overloaded with expectations.
A Staged Roadmap Beats a Single Large Purchase
Many shops benefit more from staged automation than from one dramatic purchase. A probing package, better tool management, locked program release, and quick-change workholding may together create more stable output than a larger automated handling investment added to a chaotic foundation.
This does not mean large automation is wrong. It means sequence matters. A good roadmap often starts by stabilizing reference control and process documentation, then protecting spindle time, then extending unattended or semi-attended runtime once the upstream variation is under control.
Buyers should therefore ask not only what they want the machine to do, but what their plant is ready to support without creating new disorder.
Turning Good Habits Into a System
CNC automation improves accuracy by managing datums, offsets, and verification more consistently than manual repetition can. It improves throughput by shrinking the non-cutting minutes that quietly consume shifts. It improves repeatability by making the process teachable, documentable, and stable across people and time.
But automation is not a shortcut around weak basics. It works best where fixturing, tooling, maintenance, and program control are already taken seriously. When those foundations are in place, automation becomes more than convenience. It becomes a reliable way to turn good process habits into durable production capacity.