Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
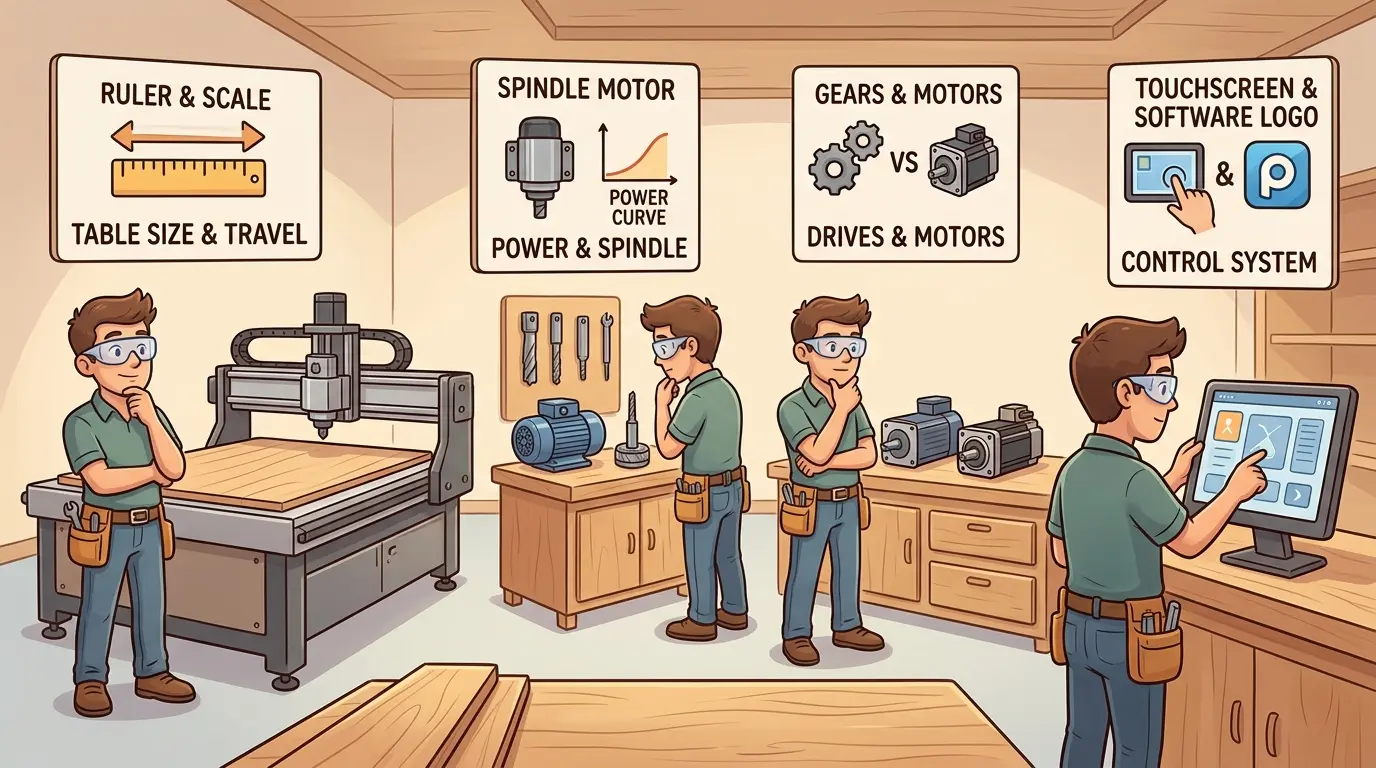
Selecting a CNC router for a woodworking plant fails most often when buyers compare spindle power and travel specs before documenting what the machine must do across a real shift. This article forces the decision back to production reality: sheet sizes actually purchased, part mix, hold-down demands, dust extraction, software flow, and the downstream stations that depend on routed output. The critical distinction is whether your plant needs flexible standalone routing or integrated nesting logic, and whether automation attacks the true bottleneck. Match the machine to the line you run daily, not the brochure you admire.
Start With the Workload, Not the Machine Brochure
Choosing a CNC router for woodworking starts with a clear picture of what the machine will actually do on a typical shift. The right choice depends far less on maximum travel or spindle power than on how your plant processes material day to day. Before comparing models, document the parts you cut, the sheet goods you buy, and the stations that depend on routed output.
Ask yourself what the router must handle. Are you cutting nested cabinet parts from full sheets? Running mixed profiles, grooves, and drilling patterns? Processing MDF, plywood, melamine, particle board, acrylic, solid wood, or a shifting blend of decorative materials? Each material class changes the demands on tooling, hold-down, and dust control.
Material flow matters just as much as material type. If routed parts move to labeling, edgebanding, boring, sanding, or assembly, then accuracy and part identification become workflow issues, not just cutting issues. A shop running mostly one-off custom work may value flexibility over maximum sheet throughput. A plant feeding a stable line with repeat panel sizes should prioritize automation and handling integration.
The most common buying mistake is comparing machines before this process context is clear. Without it, every router looks promising and every quotation feels incomplete.
Decide Between a Standalone Router and a Nesting Cell
Not every woodworking plant needs the same routing solution. Some shops genuinely need a flexible standalone router for varied work, prototyping, shaped parts, or mixed custom furniture jobs. Others are solving a panel-processing problem and should compare routing against more integrated nesting logic. Still others cut large volumes of rectangles and might be better served by stronger upstream sizing rather than making the router carry work that belongs elsewhere.
A router excels when you need profile freedom, routed features, and software-controlled flexibility. It is less efficient when the workload is dominated by straight rectangular breakdown that could be handled faster upstream. In factories where flexible sheet processing is the priority, CNC nesting machines often provide the better comparison point because they frame the decision around complete panel workflow instead of router travel alone.
Resist the urge to make one machine solve every cutting task. The best result usually comes from matching the router to the work that genuinely benefits from programmable routing.
Match Bed Size to Real Sheets and Real Handling Habits
Router size should be based on the material you actually buy and the margins you really use, not on optimistic brochure assumptions. Think beyond nominal sheet size. You need room for hold-down zoning, onion-skin habits, spoilboard resurfacing, tool access, sheet skew, labeling space, and safe clearance during loading and unloading.
Larger beds are not automatically better. They increase floor-space pressure, vacuum demand, handling complexity, and sometimes idle loading distance. Smaller beds can be productive when the job mix supports them, but they become expensive when operators constantly trim, rehandle, or re-sequence material just to fit the machine. The correct bed size is the one that fits purchased material and supports the way the plant actually runs over a full shift.
Future product direction matters too. If your sales pipeline suggests larger panels, wider nested layouts, or more sheet-based custom production, sizing too tightly creates avoidable limits. But oversizing without a corresponding hold-down and handling plan can be just as costly.
Spindle and Tooling Follow Material Behavior
Spindle selection should follow material behavior, cutter mix, and cycle expectations. MDF, plywood, laminated panels, solid wood, plastics, and composite decorative boards do not create the same cutting demands. The question is not which spindle sounds more powerful in isolation. The better question is whether the spindle, holders, collets, and tool library together support the way your parts are really cut.
Automatic tool changing becomes valuable quickly when programs mix profiling, drilling, grooving, surfacing, and specialized features in one cycle. But richer tool-changing capability also raises the need for discipline. If the plant cannot maintain tool libraries, naming standards, holder consistency, and basic tool-life habits, an impressive tool system can create confusion instead of capacity.
Downstream cut quality matters as well. Poor tooling choices show up later as chipped edges, weak glue-line appearance, excess sanding, or inconsistent feature sizing in assembly. That is why spindle and tooling should be evaluated with the whole route in mind, not as a stand-alone speed discussion.
Hold-Down Strategy Deserves the Same Attention as the Frame
Vacuum is not a side accessory. It is one of the main reasons routed parts stay dimensionally trustworthy from program start to part release. Weak hold-down turns a good toolpath into a scrap generator. Small-part movement, sheet slip, porous board behavior, and inconsistent spoilboard condition can create errors that get blamed on software or operators even though the real problem is hold-down.
Buyers should ask how zoning, pump capacity, gasket logic, spoilboard maintenance, and typical part sizes interact. A machine that looks impressive mechanically may still perform poorly if the hold-down system is under-matched to the work. Shops processing small nested parts, mixed sheet sizes, or porous boards should pay especially close attention here.
The practical question is not merely whether a vacuum pump is included. It is whether the hold-down system is suited to the real part mix and whether the plant is prepared to maintain it consistently.
Dust Extraction Changes Uptime and Finish Quality
Wood dust is a production issue, a maintenance issue, and a safety issue. Poor extraction affects visibility, finish quality, cabinet cleanliness, electrical reliability, guide life, and operator comfort. Fine dust also hides gradual machine decay because it accumulates around sensors, moving parts, and wiring.
Router selection should include extraction design from the beginning. Hood behavior, duct sizing, airflow, cleanup access, and filter discipline all matter. A router cutting MDF all day without a strong extraction plan will not behave like the same machine in a demonstration room.
This is one of the clearest cases where under-investing upstream creates visible downstream waste. A router cannot stay productive if every shift is fighting dust that the process should have controlled at the source.
Software Flow Adds or Destroys Router Capacity
A router is only as useful as the data that reaches it cleanly. If programming output is slow, inconsistent, or vulnerable to version confusion, capacity disappears on the screen before it disappears on the floor. Buyers should ask not only which controller the machine uses, but how postprocessors are maintained, how CAM output is verified, how job files are named, and how revisions reach the operator.
This matters even more in high-mix environments, where the router’s flexibility depends on the plant’s ability to move the correct data into production without hesitation. In a panel factory, labeling and part identification can be nearly as important as the toolpath itself, because routed parts often need to reach edgebanders or boring and drilling machines in the correct order with minimal confusion.
Software discipline is not glamorous, but it is one of the biggest reasons one router cell feels calm while another feels permanently rushed.
Evaluate the Router Inside the Whole Woodworking Sequence
Router decisions improve when buyers look beyond the router. What happens before cutting? What happens after cutting? Does upstream sizing deliver clean, square sheets? Do downstream stations receive parts in a sequence they can actually absorb? Is the router expected to compensate for scheduling chaos elsewhere in the plant?
In many factories, the router is only one node inside a larger chain that may include panel saws, edgebanding, drilling, sanding, and assembly. A router that looks excellent in isolation may still disappoint if the line around it is poorly balanced.
Buy the machine that fits the sequence, not the machine that photographs best. The router that works well on a Tuesday afternoon when production is crowded and the next shift is waiting is the one matched to the line you actually run.
Automation Should Attack the Real Bottleneck
Automatic loading, unloading, labeling, nesting optimization, and drilling integration can all create real value, but only when they attack the right problem. If the real pain point is setup delay, faster handling may help. If the real pain point is lost parts or sequence confusion, labeling and data discipline matter more. If the real pain point is line imbalance after routing, the router may not be the first investment to optimize.
Automation should follow bottleneck diagnosis rather than marketing appeal. A simple, stable router cell can outperform a more elaborate installation if the plant around it is not ready to support the higher complexity.
Recovery Time Matters as Much as Cutting Speed
Speed sells routers. Recovery time keeps them useful. Ask what happens when vacuum performance drifts, when the spindle needs service, when a controller problem repeats, or when new staff need training six months after commissioning. A router that is technically capable but slow to recover from common failures will not feel productive for long.
Training should be evaluated realistically. Can operators and programmers attend it without production chaos? Will the plant document feeds, tooling choices, and standard work so performance survives turnover and vacations? Is there a clear spare-parts path for wear items and critical assemblies?
Factory-direct purchases can be excellent, but they need disciplined verification. The real difference between smooth commissioning and painful commissioning often appears in service detail, not in headline price.
Use a Selection Matrix That Reflects Plant Behavior
The table below keeps comparisons tied to production fit rather than broad specification lists.
| Question | Why It Matters |
|---|---|
| What materials dominate the workload? | Drives spindle, tooling, and dust strategy |
| Are most jobs nested sheet parts or varied custom pieces? | Separates nesting logic from general routing needs |
| How small are the finished parts? | Determines hold-down demands |
| What downstream stations depend on routed output? | Connects router choice to line balance |
| How stable is programming and file control today? | Reveals whether software will support machine flexibility |
| What service and spare-part response is realistic? | Protects uptime after commissioning |
| What is the actual current bottleneck? | Prevents buying features that do not solve the main problem |
This kind of comparison is more useful than ranking machines by broad specification lists that ignore process fit.
Choose the Router That Fits the Line You Actually Run
Many poor router purchases come from buying for peak possibility instead of daily reality. The plant imagines future complexity, maximum sheet throughput, or perfect software coordination, then buys a machine around that story. Months later, the real shop is still fighting hold-down, file control, dust, and line sequencing.
The best router purchase often looks less dramatic. It is the one whose bed size suits real sheets, whose tooling plan matches real parts, whose vacuum system can hold the actual job mix, whose software flow is supportable, and whose service model fits the plant’s tolerance for downtime.
Start with part flow, material behavior, and the stations that depend on routed output every day. Then match bed size, spindle and tooling, hold-down, extraction, software flow, automation level, and service depth to that reality. Routers are strongest where programmable flexibility creates real production value. They are weaker when buyers expect them to solve every upstream and downstream problem by themselves. The best purchase is the router that fits the line you actually run.