Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
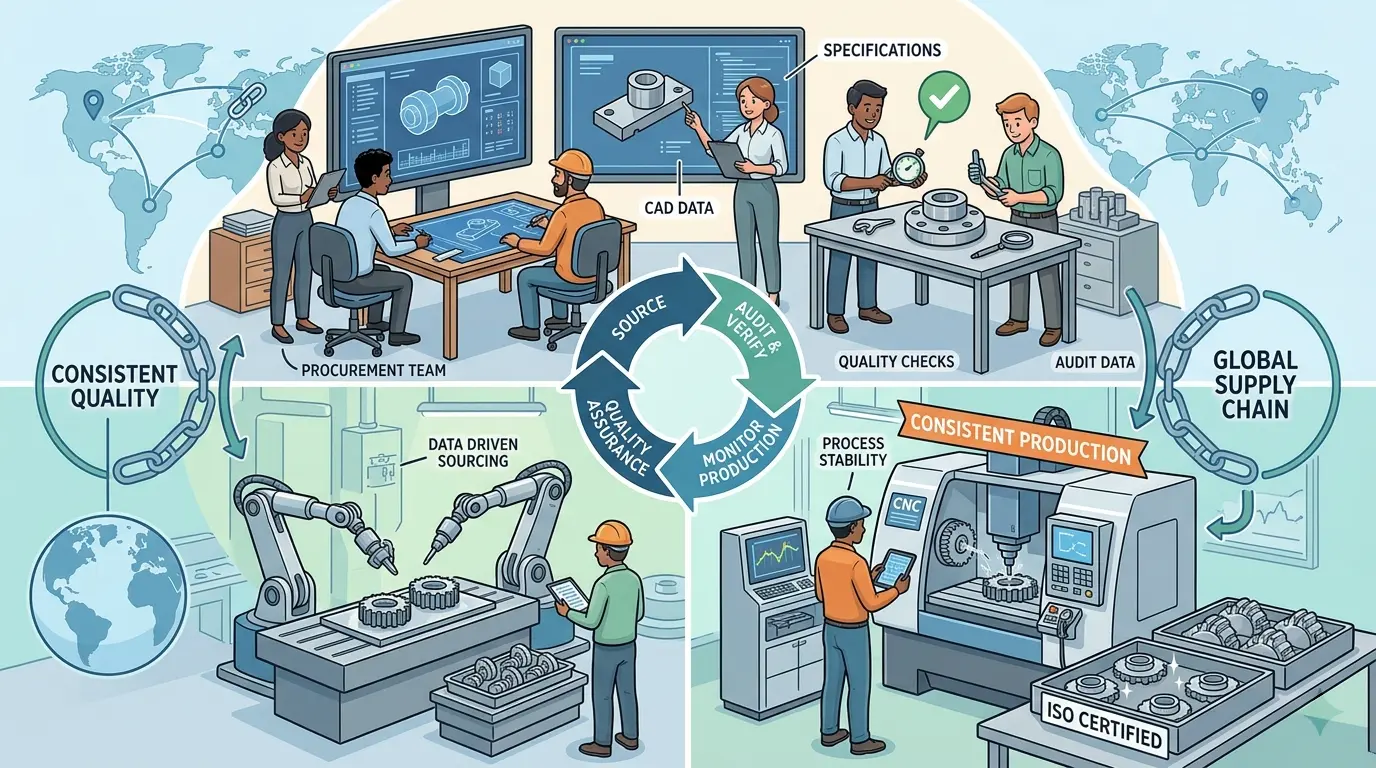
Most quality problems in CNC-machined components surface long after incoming inspection, when assembly stops, warranty claims climb, or field failures trace back to hole-position drift that no routine check caught. The gap between what buyers assume and suppliers interpret creates variation before the first chip is cut. This article addresses that sourcing breakdown directly: how to define consistency in measurable terms, express manufacturing intent on drawings, screen suppliers against critical features rather than generic capability, and build closed-loop quality systems that survive personnel changes and repeat lots. The decision matters because treating machined parts as interchangeable commodities converts hidden interpretation risk into expensive downstream failure.
Consistent Machined Parts Start With Requirements, Not Incoming Inspection
Most quality problems in CNC-machined components are not discovered at incoming inspection. They are created earlier, in the gap between what the buyer assumes and what the supplier interprets. A part can pass a routine receiving check and still cause trouble in assembly, secondary processing, or field service because the requirements that actually mattered were never made explicit.
Buyers who treat machined parts as interchangeable commodities usually learn this the hard way: through warranty claims, repeated lot disputes, or assembly-line stops caused by hole position drift or surface variation that no casual inspection would catch. The fix is not a stricter final check. It is a sourcing system that controls how parts are defined, how suppliers are screened, how critical features are prioritized, and how variation is handled when it appears.
Define Consistency in Measurable Terms Before You Source
“Consistent quality” means different things to different teams. Engineering may care about dimensional repeatability across months. Assembly may care about interchangeability. Sales or field service may care about cosmetic uniformity on visible surfaces. A supplier cannot optimize for all of these at once unless you explain which one drives the real risk.
Write consistency in measurable terms before sending an RFQ. Which dimensions control fit? Which surfaces affect sealing, appearance, or downstream coating? Which features become sensitive after heat treatment, grinding, or anodizing? Which variations create real pain on the shop floor, and which ones only look uncomfortable on a print?
Without that clarity, suppliers will optimize around whatever seems safest during quoting. That may not match your assembly risk or field-performance risk. The sourcing conversation improves immediately when you stop asking for “good parts” and start specifying the exact behaviors that must remain stable.
Drawings Must Express Manufacturing Intent, Not Just Geometry
Many sourcing problems begin with drawings that are technically complete but operationally ambiguous. Conflicting notes, unclear datum logic, mismatches between the CAD model and the print, over-tolerancing copied from older revisions, and vague surface callouts all create room for interpretation. Different suppliers may quote the same part while understanding different jobs.
Review drawings through a manufacturing lens before sourcing. Ask whether a competent programmer, machinist, and inspector would interpret the same intent the same way. Ask whether edge conditions, burr expectations, cosmetic standards, and key characteristics are explicit enough to survive staff turnover on either side.
If the drawing invites multiple plausible process routes, variation has already entered the program before production starts. Reducing interpretation risk before the first RFQ leaves your office is the cheapest quality improvement available.
Screen Suppliers Against Your Critical Features, Not Generic Capability
No supplier is excellent at everything. A shop that handles straightforward prismatic parts well may struggle with thin-wall stability, cosmetic control, difficult materials, or tight positional accuracy on precision bores. The supplier selection process should match capability to the features that carry your real risk.
Identify critical characteristics first, then screen suppliers against those specific requirements. Over-tightening everything is counterproductive: if every dimension is marked equally important, the supplier receives no prioritization signal, prices rise, and the assembly still does not feel better. Quality sourcing works when you know which features deserve the most scrutiny and why.
Material Control Is a Quality Variable, Not a Purchasing Detail
Material discipline is often reduced to a line item, but it directly influences machining behavior, secondary-process response, corrosion resistance, finish outcome, and lot-to-lot consistency. Specifying “aluminum” or “steel” is not enough when part behavior depends on alloy, temper, certification, or allowable substitutions. Material ambiguity is one of the quietest ways to create variation before the first chip is cut.
Make material definition explicit in the RFQ and maintain it through receiving, production, and any outside processing. Loose substitution language allows machining behavior and downstream response to drift more than you may realize. Consistency starts in raw stock, not in the final inspection report.
First Article Review Should Teach the Process, Not Just Approve a Part
A first article is most valuable when it aligns supplier process understanding with your measurement logic. It should clarify how datums are applied, how key characteristics are measured, what the supplier considers stable, and where the part still carries risk. Treated only as a pass-fail checkpoint, it loses most of its value.
The best first-article reviews are collaborative and specific. They expose interpretation differences, measurement disputes, process sensitivities, and feature-risk patterns before recurring production begins. That early learning is far cheaper than later blame. This matters most when the part carries multiple datums, cosmetic expectations, close-tolerance assemblies, or downstream operations that amplify small deviations.
Inspection Strategy Should Evolve as the Process Matures
New or unstable processes justify deeper inspection. Mature, well-controlled processes support smarter sampling. The mistake is treating one inspection intensity as universally correct. Over-inspection creates cost and delay; under-inspection ships risk downstream.
Ask what phase the part is in: prototype, pilot, or recurring stable production. The answer should determine how the part is verified. Quality plans that ignore phase create either waste or false confidence. Consistency improves when inspection strategy changes deliberately as the process becomes better understood, rather than staying frozen at whatever level was chosen during launch anxiety.
Apply Control-Plan Thinking Even Without Formal PPAP
Many machining programs do not operate under a heavy automotive-style submission process, but they still benefit from control-plan logic. What are the critical characteristics? What is measured every lot? What is sampled periodically? Which process variables tend to drift first? Which defects are containment issues, and which require root-cause analysis?
Even a lightweight version of this thinking improves repeat supply because it gives both buyer and supplier a shared map of what must stay stable. Without that map, quality is reactive. With it, quality becomes directional. The point is not bureaucracy; it is making repeat output less dependent on memory and luck.
Corrective Action Should Strengthen the Process, Not Just Rescue the Lot
When a lot escapes or a non-conformance appears, the supplier’s response reveals the real maturity of the relationship. Sorting and rework may solve the immediate shipment problem, but they do not automatically strengthen the process. The deeper question is whether the cause was traced to setup, tooling, environment, measurement, program behavior, material variation, or drawing interpretation—and whether the response reduces recurrence.
Insist on evidence rather than apologies. What changed? How was it verified? What prevents the same failure mode from reaching another lot? A supplier that answers those questions clearly is more valuable than one that only reacts quickly in the moment. Quality consistency grows when both sides treat errors as process data, not as embarrassment to be hidden.
Rework, Outside Processing, and Handling Need Explicit Rules
Many quality problems appear after machining rather than during it. Coating, heat treatment, grinding, deburring, cleaning, packaging, and handling can alter part condition or damage features that were previously acceptable. If those steps are not included in the sourcing plan, you are only sourcing partial quality.
RFQs and supplier agreements should address what happens after the cut cycle. How is the part protected? How are reworked lots identified? How are outside-process effects expected and controlled? How does traceability survive through those steps? What happens if outside processing changes appearance, edge feel, flatness, or thread behavior? A part that was stable at the machine but unstable at assembly is still a sourcing failure.
Receiving Quality Must Match Supplier Quality or the Loop Breaks
Buyers sometimes blame suppliers for inconsistency when their own receiving process is equally unstable. If incoming inspection uses inconsistent gages, weak environmental control, unclear acceptance rules, or different inspectors interpreting the print differently, the feedback loop becomes noisy. Good suppliers cannot improve against unclear signals.
Sourcing consistent quality also requires internal discipline. Inspection criteria, gage suitability, escalation paths, lot segregation, and deviation review need to be as stable on your side as you expect them to be on the supplier’s side. When the buyer’s incoming process is inconsistent, the supplier receives mixed messages, and the program drifts administratively before the machining process drifts physically.
Lot Integrity and Revision Control Matter More Over Time Than at Launch
Consistency depends on what survives after the original launch. If the program needs spares or repeat lots over years, documentation quality matters deeply. Drawings, inspection logic, revision history, fixture assumptions, packaging rules, and lot identity need to remain usable after personnel change on both sides.
Lot integrity deserves deliberate rules. Mixed lots, poorly tracked rework, unclear revision acknowledgment, or undocumented process substitutions create apparent randomness later, even when the machining process was once stable. Long-term sourcing quality depends on administrative clarity as much as on machining capability. Quality programs often fail quietly when memory becomes the main archive.
A Practical Supplier Review Matrix Exposes Where “Good” Means Different Things
Use a simple review matrix so sourcing and quality teams judge the same things.
| Review Area | What To Check | Why It Matters |
|---|---|---|
| Drawing interpretation | Datum clarity, notes, revision alignment | Prevents hidden interpretation drift |
| Material discipline | Alloy, temper, certs, substitution rules | Protects machining and downstream behavior |
| Critical-feature capability | Tolerance, finish, position, repeatability | Matches supplier strength to actual part risk |
| First-article method | Measurement logic, open issues, process learning | Builds a stable launch instead of a one-time approval |
| Ongoing inspection | Sampling logic, trend review, containment response | Supports long-term consistency |
| Rework and outside processing | Identification, traceability, handling rules | Prevents hidden lot instability |
| Documentation depth | Revision history, lot identity, escalation records | Protects long-term supply quality |
This matrix helps stop generic statements like “they’re a good shop” from replacing actual quality reasoning.
Review Suppliers on Trends, Not Only on Incidents
A mature sourcing program watches trend quality, not only dramatic failures. One bad lot deserves attention, but recurring small shifts in finish, lead time, documentation accuracy, or first-pass acceptance often tell the more important story. Supplier reviews should look at patterns over time rather than waiting for a major escape to trigger concern.
This approach helps buyers reward early transparency and process improvement instead of only reacting once variation becomes expensive. It also helps separate isolated events from real process decay. Consistency is usually lost gradually before it is lost dramatically.
Supplier Onboarding Should Include More Than a Quote Win
Many programs go unstable because the supplier was effectively onboarded by winning the price discussion rather than by proving a repeatable understanding of the part. A healthy onboarding process checks more than commercial agreement. It confirms revision control, contact ownership, escalation paths, first-article timing, gage strategy, packaging expectations, material traceability, and how non-conforming product will be contained if something goes wrong.
This matters most when moving a part from one source to another or launching a part that will matter commercially after the first few lots. Without a structured onboarding step, each side quietly fills in the gaps with its own assumptions. That is how one team believes a feature is critical while the other sees it as routine. It is how packaging damage gets classified as “shipping noise” instead of preventable process variation. It is also how traceability becomes incomplete without anyone noticing until a field issue forces a records review.
Good onboarding is not bureaucracy for its own sake. It is the cheapest place to surface mismatch before repeat supply begins.
Separate Critical Characteristics From General Conformance
Another common sourcing mistake is forcing the supplier to treat every dimension like a business-critical characteristic. That usually raises cost, slows inspection, and still fails to protect what truly matters. The more effective approach is to distinguish between general print conformance and the smaller set of features that drive assembly, function, sealing, appearance, wear, or interchangeability.
Once that distinction is clear, the supplier can align process attention appropriately. Gaging, sampling, setup verification, and corrective action intensity can be stronger where the business risk actually lives. This makes the quality loop more intelligent instead of merely more expensive.
It also improves cross-functional communication inside your own organization. Engineering, quality, sourcing, and production often use the word “critical” differently. Forcing the team to identify which features truly carry cost-of-failure risk usually improves both supplier performance and internal decision quality.
Consistent quality rarely comes from inspecting everything harder. It usually comes from understanding which features deserve the deepest control and building the supplier relationship around that reality.
The Same Discipline Applies to Internal Capability Planning
The same logic that governs part sourcing applies when comparing machinery. Clear scope, real workflow fit, and normalized quotes matter in both cases. For factories balancing outsourced components with internal capability planning, it helps to understand how to compare CNC machinery quotes without missing the real scope differences. And when production planning extends across several machine families instead of one part type, the Pandaxis product catalog becomes the better planning surface.
The principle is the same in both sourcing and equipment decisions: stable output comes from matched process design, not from vague optimism or generic supplier labels.
Consistency Comes From Closed Loops, Not One-Time Approval
Sourcing consistent machined parts requires more than finding a capable supplier. It requires drawings that express intent clearly, material definitions that hold up through processing, first-article review that teaches the process, inspection plans tied to risk and maturity, corrective actions that strengthen the system, and documentation good enough to support repeat supply over time.
Treat quality as a closed loop of controlled decisions rather than as a final inspection event. That mindset usually reduces surprises faster than any single certificate, sample lot, or impressive shop tour ever will.