Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
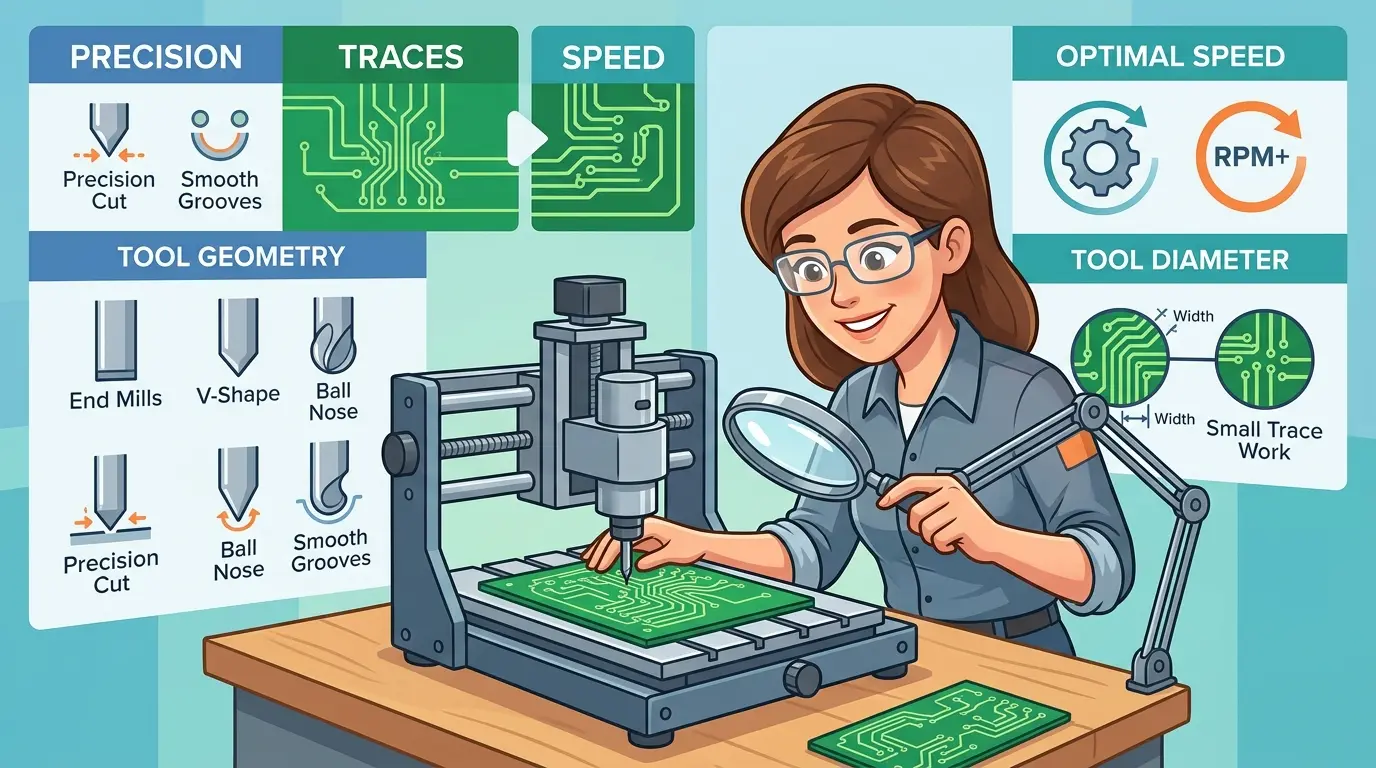
Before you open a tool catalog for a small-trace PCB job, the real decision is whether your board objective, machine condition, and depth-control discipline can support the cutter you are considering. A 6-mil trace layout does not automatically justify a 0.2 mm tool if your spindle runout, collet grip, or board flatness will make that cutter behave 20 percent wider than its nominal diameter. This article walks through how to measure effective cutting width, why process stability beats aggressive tool choice, and when to standardize on a conservative cutter library instead of chasing the smallest catalog number.
Define the Board Objective Before Opening the Tool Catalog
The most common mistake in PCB prototyping is selecting a cutter before defining what the board actually needs to prove. Are you validating connector placement and mounting holes? Checking broad electrical continuity? Or are you trying to confirm that a dense layout with tight trace spacing can be isolated cleanly?
These questions matter because the cutter operates as part of a system. The right tool depends on the isolation width your design requires, the consistency of the board surface, and how repeatably your machine can hold depth across the full board area. A cutter that looks acceptable on wide isolation paths can fail quickly once trace spacing tightens or the laminate surface varies.
If the design is already pushing the comfortable limit of your process, tooling decisions need to be conservative and tightly controlled. If the board only needs to answer a broad validation question, chasing the most aggressive fine-feature tool adds risk without adding useful information.
Consider a typical scenario: an engineering team receives a revised layout with 6-mil traces and 6-mil spacing, down from 10-mil features in the previous revision. The immediate reaction is to order the smallest cutter available. But if the board’s purpose is to verify that the new power distribution network delivers correct voltages to critical ICs, the fine trace geometry is secondary. A stable 0.8 mm cutter that isolates reliably at 12-mil spacing will answer that question without introducing the fragility of a 0.2 mm tool. The board objective, not the layout density alone, should drive the purchase.
Process Stability Beats Aggressive Tool Choice
When features get small, the instinct is to reach for the finest-looking cutter available. That instinct often backfires. A delicate cutter may look ideal on paper, but if the spindle has noticeable runout, if depth control drifts across the board, or if the hold-down is inconsistent, the result becomes less reliable, not more precise.
Small trace work rewards process stability more than cutter ambition. A slightly more conservative tool running in a stable, predictable setup typically produces better practical results than a fragile cutter pushed into an unstable process. The smartest selection method starts with the machine’s real behavior, not the ideal behavior implied by the tool catalog. Small trace work does not reward optimism for long.
Think about what happens during a typical isolation routing pass. The cutter spins at 30,000 to 60,000 RPM while traversing narrow channels between copper features. At these speeds, any vibration source becomes amplified. A spindle with 0.01 mm runout might be invisible on a 2 mm tool but will cause a 0.3 mm cutter to wobble enough that the effective cutting diameter grows by 20 percent or more. That wobble translates directly into wider isolation channels, torn copper edges, and inconsistent depth. The machine’s mechanical condition sets a floor on what any cutter can achieve, regardless of how well the tool is ground.
Depth control is equally critical. Most PCB routers rely on mechanical Z-axis stops or touch-off routines to establish the cutting depth relative to the board surface. If the zeroing method depends on a single reference point, and the board has any warp or bow, the effective depth will vary across the surface. A cutter that works perfectly at the reference corner may cut too shallow in the center of the board, leaving copper bridges between traces, or too deep at the opposite edge, cutting into the substrate and weakening the board structure.
Geometry Matters, But Only in Context
Cutter geometry determines how cleanly material is isolated and how sensitive the process becomes to depth variation. Tip condition matters just as much. Very small features deteriorate quickly if the cutting edge is worn, damaged, or inconsistent from the start.
PCB milling cutters typically use a V-shaped or fishtail geometry. V-shaped tools with an included angle of 30 to 60 degrees are common for isolation routing because they allow narrow channels while maintaining adequate tool strength. Fishtail cutters, with a flat bottom and two cutting edges, are better suited for pocketing and clearing larger areas. The choice between these geometries depends on the specific operation and the material being cut.
For standard FR-4 laminate, a V-shaped cutter with a 30-degree included angle and a tip diameter of 0.2 to 0.5 mm is a common starting point for fine trace work. The sharp tip penetrates the copper layer cleanly and creates a narrow isolation channel. However, the same geometry that makes the tool effective for fine features also makes it fragile. A 0.2 mm tip has very little material supporting it, and any lateral force can cause it to snap or deflect.
For softer materials like Rogers or PTFE-based laminates, the cutting forces are lower, but the material can deform or smear if the cutter geometry is not optimized. A sharper cutting edge with a higher rake angle reduces smearing but increases the risk of edge chipping. The material properties, not just the trace width, should influence the geometry selection.
That is why cutter selection must be tied to inspection and replacement discipline. If the shop cannot tell whether a small cutter is still performing properly, the process will drift without obvious warning. Surface appearance alone is not always enough to catch the problem early. A cutter strategy needs to include not only what tool to buy, but how the team will monitor wear and recognize when the process has become unreliable. Small-trace performance is rarely separated from wear control for very long.
Effective Behavior, Not Nominal Diameter, Sets the Real Limit
Many newcomers focus only on nominal cutter size. That is understandable but incomplete. The machine never cuts with catalog theory alone. It cuts with the real behavior of the spindle, collet, holder, material flatness, and zeroing method combined.
The tool diameter printed on the package is not the whole story. If runout, vibration, or unstable depth make the tool behave larger than intended, the process limit arrives sooner than the catalog suggests. That is why two shops can use nominally similar cutters and get very different outcomes. Good teams think in terms of effective process capability, not just nominal tool size.
Here is a practical way to measure effective behavior. Run a test pattern on a scrap board with the cutter you plan to use. The pattern should include isolation channels at several widths, from the nominal cutter diameter up to three times that diameter. After routing, inspect the channels under magnification. Measure the actual channel width at several points along each path. If the measured width is consistently 20 percent wider than the nominal cutter diameter, you have identified the effective cutting width for your setup. That number, not the catalog value, is what you should use when planning trace spacing and isolation paths.
This measurement also reveals depth consistency. If the channel width varies significantly along its length, the depth is drifting. That drift can come from board flatness, Z-axis repeatability, or thermal expansion of the spindle as it warms up. Identifying the source of the drift is the first step toward controlling it.
Runout and Collet Quality Often Outweigh the Cutter Brand Story
Small trace work exposes machine weaknesses quickly. If spindle runout is high, if the collet does not hold the tool consistently, or if the Z reference shifts, even a well-chosen cutter produces poor results. Tool choice cannot be separated from machine condition.
Many PCB milling frustrations are blamed on cutter style when the real problem lies in setup repeatability. The cutter receives the blame because it is the visible consumable. But small-trace routing is a system problem. The spindle, board flatness, zeroing method, and depth consistency all interact with the tool. If the spindle and holding system are not calm, smaller cutters often magnify the instability instead of solving it.
Collet quality deserves particular attention. A standard ER collet that has been used heavily may have worn slots or slight deformation that prevents it from gripping the cutter shank evenly. That uneven grip translates into runout at the tip, even if the spindle itself is in good condition. Precision collets with tighter tolerances, or hydraulic tool holders, can reduce runout significantly. The cost difference is modest compared to the improvement in process reliability.
Tool shank diameter also matters. A 3.175 mm shank is standard for many PCB cutters, but some fine tools use smaller shanks. A smaller shank is more flexible and more prone to deflection under load. If the machine can accommodate a larger shank, that is usually the better choice for stability, even if the cutting tip is the same diameter.
Board Flatness and Depth Control Decide Isolation Quality
Depth control matters enormously in PCB milling because the process window is narrow. If one area of the board sits slightly higher or lower, the same cutter either fails to isolate cleanly or cuts too aggressively. Board support and zeroing method are therefore central to cutter performance.
A tool that worked yesterday may look poor today if the board mounting changed, the reference point shifted, or the sacrificial surface is no longer as flat as assumed. Users often interpret that as tool inconsistency when the deeper cause is depth inconsistency. A shop choosing cutters for small trace work should ask not only what tool fits the design, but whether the board can actually be held and referenced well enough to let that tool behave predictably.
Board support is the first line of defense. A vacuum table provides uniform hold-down across the entire board surface, which is ideal for thin laminates that tend to bow. Mechanical clamps work but can introduce localized stress that distorts the board. A sacrificial layer beneath the board, such as a phenolic or acrylic sheet, provides a consistent cutting surface and protects the machine table. The sacrificial layer must be flat and must be replaced before it becomes too scarred to provide a reliable reference.
Zeroing method is the second critical factor. A touch-off routine that senses the board surface at multiple points and calculates a best-fit plane is far more reliable than a single-point reference. Some machines offer automatic surface sensing that maps the board topography before routing begins. If your machine lacks this feature, consider adding a manual height probe and checking the board at several locations before starting a critical job.
Depth control during routing is the third factor. The ideal depth for isolation routing on standard 1.6 mm FR-4 with 1-ounce copper is typically 0.1 to 0.15 mm below the copper surface. That depth removes the copper layer completely while leaving the underlying substrate intact. Cutting deeper risks weakening the board and creating stress points that can cause delamination. Cutting shallower leaves copper residue that creates electrical shorts. The window is narrow, and any depth variation across the board pushes parts of the job outside it.
Conservative Tooling Is Faster in an Immature Process
If your board-routing process is still developing, choose tooling that gives you practical margin rather than the most aggressive theoretical capability. That does not mean giving up on precision. It means reducing the number of variables that can fail at the same time.
In an immature process, a slightly less demanding cutter paired with stable hold-down and careful setup teaches more than an ultra-fine tool that forces the process past its reliable limit. Once machine behavior is better understood, tooling decisions can become more ambitious. This staged approach is usually faster overall because it reduces troubleshooting noise. Instead of guessing whether failures came from the tool, the board, the spindle, or the CAM choices, the team gains a more readable process.
A practical example: a lab that is new to PCB milling starts with a 0.5 mm V-shaped cutter and a standard FR-4 board. The team runs a test pattern, measures the results, and adjusts the depth and feed rate. After a few iterations, they achieve consistent isolation at 10-mil spacing. They then try a 0.3 mm cutter and find that the machine’s runout causes the effective width to be nearly the same as the 0.5 mm tool. The smaller cutter adds no capability, only fragility. The team returns to the 0.5 mm tool and focuses on improving depth control instead. That is a faster path to better results than forcing the smaller cutter to work.
Standardization Beats Constant Tool Experimentation
Labs and engineering groups often waste time by constantly changing cutter styles in search of a perfect answer. That creates more confusion than improvement. If the machine is used repeatedly for similar prototype work, standardize around a small, well-understood cutter library and a consistent replacement rule.
Standardization narrows the variables. The team learns what surface quality, isolation behavior, and life expectancy to expect from each tool under known settings. That makes troubleshooting more honest. If the result changes, the team has fewer places to look. Repeated success with a slightly less ambitious cutter is usually more valuable than occasional success with an extreme tool that behaves differently every time conditions drift.
A typical cutter library for a prototyping lab might include three tools: a 0.5 mm V-shaped cutter for general isolation routing, a 1.0 mm fishtail cutter for clearing and pocketing, and a 0.2 mm V-shaped cutter reserved for the most demanding fine-feature work. Each tool has a documented feed rate, spindle speed, and depth setting. The team logs usage hours for each tool and replaces them on a fixed schedule, such as every 50 linear meters of routing or after any visible edge damage. This discipline removes the guesswork from tool management and makes process drift easier to detect.
Replacement rules should be based on measurable criteria, not intuition. A simple log sheet that records the date, board type, routing distance, and observed surface quality for each tool provides the data needed to set realistic life expectations. Over time, the team learns that a particular cutter brand and geometry consistently delivers 80 meters of reliable routing on FR-4 before the edges dull noticeably. That knowledge allows proactive replacement before failures occur.
A Practical Selection Framework
| Process Condition | Better Cutter Strategy |
|---|---|
| Early-stage board prototyping with moderate features | Choose a cutter that offers stability and repeatability over maximum theoretical fineness |
| Small trace work on a well-understood machine | Use tooling matched to the real depth and runout capability of the setup |
| Inconsistent board flatness or zeroing confidence | Avoid overly delicate tooling until setup control improves |
| Repeat lab use with established workflow | Standardize around cutters the team can inspect and replace reliably |
| Very demanding feature density | Reassess whether the process or external fabrication route is more practical |
The table is intentionally process-focused because tool choice without process context usually leads to disappointment. Each row pairs a common shop-floor condition with a sensible tooling response. The goal is not to prescribe a specific cutter model but to guide the decision toward the factor that actually limits performance.
Cutter Choice Should Follow Prototype Purpose
Not every prototype board needs the same tooling ambition. If the board mainly exists to validate connector positions, mounting holes, or broad electrical layout logic, a stable and repeatable cutter choice is better than an aggressive one. If the board is pushing toward more demanding feature definition, machine condition and depth control must be strong enough to support that jump.
Prototype purpose should always guide cutter choice. A tool that is ideal for one validation stage may be inefficient or fragile for another. Teams that remember this make calmer decisions because the cutter is judged against the board question, not against an abstract idea of maximum precision.
Consider two boards that look similar on the surface. The first is a mechanical validation board with large pads, wide traces, and a handful of mounting holes. The second is an electrical test board with fine-pitch components and dense routing. The first board can be routed successfully with a 1.0 mm cutter at moderate feed rates. The second board demands the finest tool the process can support. Using the same cutter for both boards either wastes time on the first or risks failure on the second. Matching the tool to the board’s purpose is not just about capability; it is about efficiency and reliability.
Wear Monitoring Is Part of the Selection Decision
Very small tooling only works well when the shop has a believable way to tell whether the tool is still usable. Wear monitoring is not a maintenance afterthought. It is part of tool selection.
If your team cannot inspect small cutters confidently, cannot log usage, or cannot tell whether isolation quality drift comes from wear rather than setup, the practical tool choice needs to reflect that weakness. A theoretically superior cutter that the team cannot manage consistently is not a superior process choice. The best tool is often the one that the actual team can control, replace, and trust under real working habits.
Visual inspection under a microscope is the most direct method for checking cutter condition. Look for chipped edges, rounded tips, and copper buildup on the flutes. A cutter that shows any of these signs should be replaced immediately. For very small tools, the damage may not be visible without magnification, so a routine inspection schedule is essential.
Electrical testing provides a complementary check. After routing a test board, measure the isolation resistance between adjacent traces. A drop in resistance indicates that copper residue remains, which can come from a worn cutter, incorrect depth, or both. Tracking these measurements over time reveals whether the process is drifting and helps separate tool wear from setup issues.
When Tooling Problems Mean the Process Has Reached Its Limit
Repeated tooling problems are not always tooling problems. If users keep chasing smaller cutters, adjusting settings constantly, and still seeing inconsistent results, the issue may be that the board design is no longer a good fit for the in-house milling process.
Recognizing that limit is part of good process judgment. The goal is not to prove that the machine can be forced to work. The goal is to choose the route that teaches the design team the most with the least wasted effort. That is also why it helps to connect cutter decisions back to the bigger question of whether in-house board milling is still the right method. If your team needs a broader process filter, the companion discussion on when PCB CNC is actually practical for board prototyping is often the better place to start before changing tooling again.
There is a clear threshold where in-house milling stops being practical. When trace widths drop below 4 mils, when the board uses exotic laminates with uneven copper distribution, or when the design requires multiple layers with precise registration, external fabrication becomes more reliable and often faster. The in-house process remains valuable for quick iterations and mechanical validation, but it cannot replace a professional PCB fab for the most demanding work. Knowing where that threshold sits for your shop prevents wasted effort and frustrated engineers.
Choose Process Margin, Not the Smallest Catalog Number
The right PCB milling cutter for small trace work is the one that matches your board objective, machine condition, depth-control quality, and process maturity. Small trace work rewards stable systems more than overly ambitious tool selection. Cutter geometry matters, but so do runout, flatness, hold-down, and wear control.
Teams that choose cutters conservatively and in context usually learn faster and waste less time. Teams that chase the finest possible tool without stabilizing the process often end up troubleshooting symptoms instead of improving the real workflow. For shops evaluating compact CNC options that can support this kind of disciplined prototyping work, the Pandaxis shop offers a practical starting point for comparing machine capabilities before committing to a tooling strategy.
The decision framework is straightforward. Define what the board must prove. Measure the machine’s real behavior. Match the cutter to the process, not the catalog. Standardize once the process is stable. Monitor wear with discipline. And know when the process has reached its limit. Following these steps will produce better boards, fewer failed runs, and a calmer engineering team.