Español
 Italiano
 Deutsch
 Français
 Português
 العربية
 Türkçe
 Русский
 Tiếng Việt
 한국어
 日本語
 简体中文
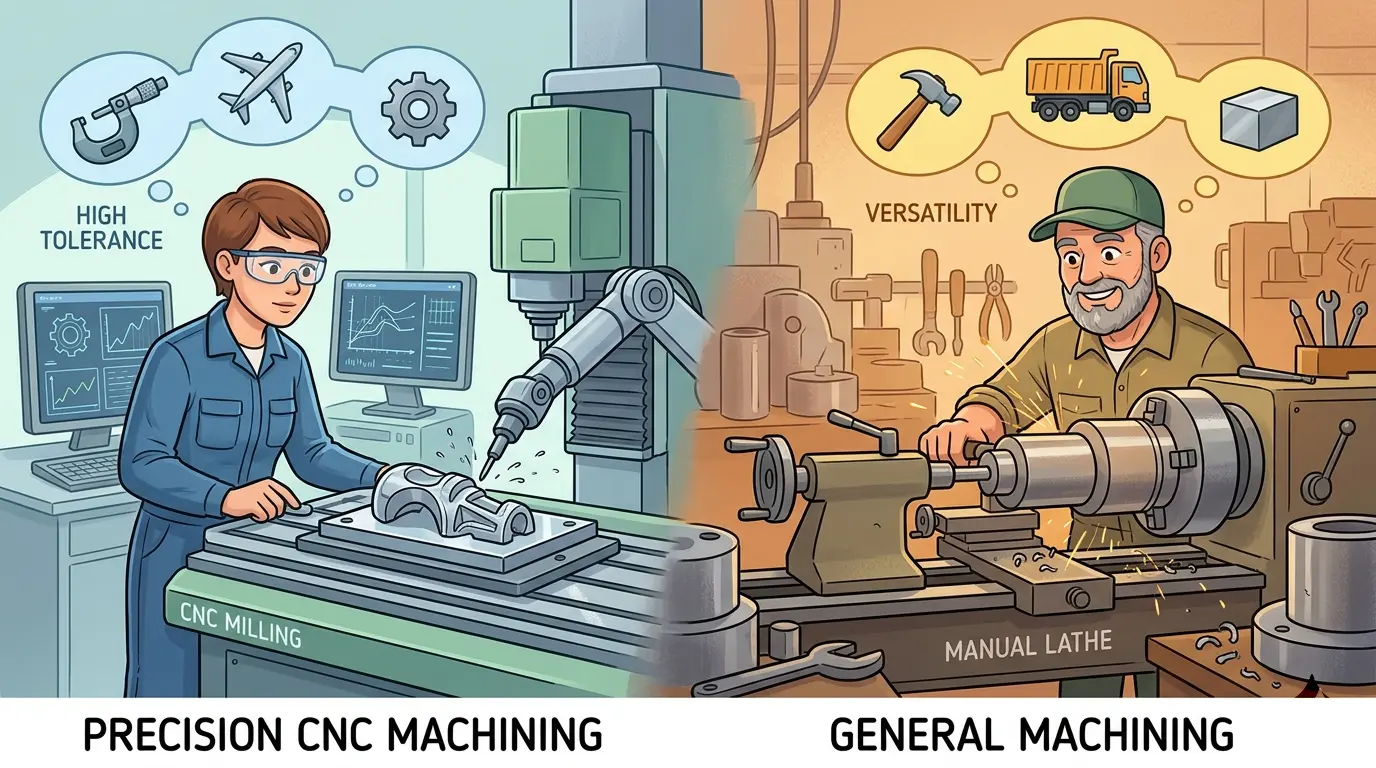
Procurement teams routinely split suppliers into “precision” and “general” machining buckets, yet the real boundary is process discipline, not machine labels. The costly mistake is choosing based on how impressive a tolerance sounds rather than what happens when a dimension drifts in service. A simple bracket with a few holes can be a commodity part—or it can create recurring assembly delays, manual fitting, rework, and field failures if its features interact to locate a mating component. Before you send an RFQ, you need to determine whether variation actually hurts your downstream workflow or just sits harmlessly on the drawing. That functional-consequence test, not the label, decides whether tighter control is an upgrade or pure added cost.
Start With the Part’s Consequence, Not the Label
Procurement teams and engineers often treat “precision CNC machining” and “general machining” as two distinct supplier categories. In practice, the boundary is less about the machine itself and more about the level of process discipline the part actually requires. A standard 3-axis CNC mill can produce parts across a wide spectrum of tolerance and repeatability, depending on how the work is set up, fixtured, inspected, and documented.
The practical question for a buyer is not whether precision sounds more impressive. It is what happens downstream when a dimension drifts within a normal commercial tolerance band. If the answer is “nothing meaningful,” a general machining approach is likely the cost-effective choice. If the answer involves assembly delays, manual fitting, rework, scrap, or field failures, then the tighter process control of precision CNC machining is not an upgrade—it is the least expensive path over the full production lifecycle.
This distinction matters most when parts look simple on the drawing but carry functional relationships that are strict. A bracket with a few holes can be a commodity part. The same bracket, if it locates a component that must align with a mating assembly, can create recurring cost problems when sourced through a process that is too loose for the job.
What General Machining Delivers Well
General machining is not a synonym for poor quality. It describes a process aligned with parts whose functional requirements are forgiving. Typical work includes brackets, base plates, covers, guards, spacers, weld-prep components, shop aids, and low-risk mechanical hardware. These parts tolerate normal commercial variation without creating assembly or performance issues.
For this category of work, the machining process is centered on producing usable parts efficiently. Setup is straightforward, inspection is practical, and documentation is proportionate to the risk. A well-run general machining shop can deliver good parts at a competitive price because the process is not burdened with control steps that add cost without adding value.
Over-specifying precision for these parts is a common buying mistake. It narrows the supplier pool, inflates quotes, and adds process burden that never pays back in the application. The correct process is the one that matches the part’s actual consequence in service, not the one that sounds safest on paper.
What Precision CNC Machining Adds When Risk Is Real
Precision CNC machining becomes relevant when the part’s function depends on tighter dimensional relationships, batch-to-batch repeatability, controlled surface outcomes, or predictable process behavior. The trigger is rarely a single tight tolerance callout. It is usually how multiple features interact in assembly or performance.
Consider a housing where a bore, a face, and a bolt pattern must work together to keep a shaft aligned or prevent seal damage. Each feature viewed individually may look ordinary. Viewed as a system, their combined relationship determines whether the assembly performs reliably. In this situation, variation does not stay on the drawing. It shows up as fit problems, vibration, leakage, or unstable product behavior.
Precision machining protects the function of the system, not merely the appearance of the part. It typically involves stronger setup control, clearer inspection planning, better fixture discipline, and a more deliberate relationship between drawing intent and machining method. The value is not in the label. It is in the consistency of the output across batches and over time.
Feature Interaction Is the Hidden Trigger
Buyers often evaluate risk by looking at one dimension and asking whether it is “tight.” That test is incomplete. Many expensive problems come from the interaction of features rather than from any single dramatic number.
A part may have a bore, a locating face, and a bolt pattern that all fall within acceptable individual tolerances. But if those features must work together to maintain alignment or sealing, their combined relationship becomes the critical requirement. This is why parts that seem easy on paper can become expensive when sourced through a general machining process that does not account for feature interaction.
In practical terms, the question is not only how close each dimension is to nominal. The question is whether the part still behaves correctly when those dimensions interact in the assembly. That distinction separates parts that need precision process discipline from parts that do not.
Assembly Cost Is Where General Machining Stops Being Cheap
One of the clearest indicators that precision matters is assembly behavior. If a team must sort parts, hand-file edges, adjust fits manually, or chase alignment variation during build, the upstream machining decision is already affecting cost.
This is where buyers misread price. A cheaper machining route can become the more expensive route once labor, inspection, rework, scrap, and production delay are included. A part that installs smoothly every time may justify a higher piece price if it removes recurring assembly friction.
The issue becomes more serious when field service is involved. A low-cost part that creates intermittent fit problems in the factory is an annoyance. A low-cost part that creates failures in the field becomes a much more expensive purchasing decision, especially when warranty, reputation, and customer retention are factored in.
Material Behavior and Surface Demands Push Parts Into Precision Sooner
The distinction between precision and general machining is not driven only by nominal size and tolerance. Material behavior and surface expectations matter significantly.
Certain materials are more sensitive to heat, tool wear, burr formation, or distortion. Parts that seal, slide, or locate may require consistent surface finish. Edge quality may matter for downstream handling or assembly. A drawing may still look simple, yet the part may require stronger process control because the material and finish expectations leave little room for casual execution.
This does not mean every difficult material automatically becomes a precision job. It means the buyer should be careful about assuming that normal commercial practice will protect the part if material behavior amplifies variation. The decision should account for how the material responds to machining, not just what the drawing says.
When Precision Is Unnecessary Cost
It is equally important to recognize when precision adds cost without adding value. If the part has broad fit tolerance, low functional consequence, and a forgiving assembly environment, a general machining route is completely appropriate.
This applies to early development parts, rough structural work, non-critical supports, temporary tooling, internal-use components, and low-risk hardware where acceptable variation is wider and the business does not need a highly documented machining process. In these cases, paying for higher control than the application requires slows supplier selection, reduces competitive quoting, and creates a process burden that never pays back.
The right decision is not the one with the most serious-sounding label. It is the one that fits function without adding unnecessary cost.
Decision Table for Buyers
| Part Condition | General Machining Often Fits | Precision CNC Machining Often Fits |
|---|---|---|
| Broadly tolerant support parts | Yes | Only if a specific feature truly drives function |
| Parts with critical mating features | Sometimes not enough | Often the safer choice |
| Prototype parts for concept checks | Often yes | Use precision only where function requires it |
| Repeated production parts with tight assembly dependence | Sometimes risky | Often justified |
| Parts where field failure is costly | Often insufficient | Usually worth stronger control |
| Parts requiring stable finish, alignment, or sealing behavior | Sometimes marginal | Commonly more appropriate |
The table is not meant to glorify precision. It ties process discipline to functional consequence, which is the only useful basis for the decision.
Reading Drawings for Risk Without Over-Specifying
One practical skill buyers need is the ability to read a drawing for risk instead of for fear. If every tighter-looking dimension automatically triggers a precision buying decision, cost inflation follows quickly.
Start by identifying which features actually drive part function. Which surfaces mate? Which bores locate? Which dimensions influence motion, sealing, balance, or repeat build quality? Which tolerances exist because the part genuinely needs them, and which were inherited from a design habit or template without much thought?
That conversation often clarifies the sourcing route. Some parts need tight control only on a few critical features. Others truly need a precision-oriented process across the whole workflow. The more clearly engineering communicates that distinction, the better suppliers can quote and plan honestly.
Questions to Ask Before Defaulting to Precision Language
Before specifying a precision requirement, ask a few hard questions:
- Which dimensions actually drive part function?
- What happens if variation increases within a practical but less controlled range?
- Does the part locate, seal, rotate, align, or otherwise influence system performance?
- Is this a one-off, prototype, or repeat production run?
- Will inconsistent parts create assembly labor, scrap, or field-service cost?
These questions force the conversation back toward function. Buyers who cannot explain why tighter control is needed usually end up paying for a label. Buyers who can explain the operational consequence get better supplier responses and clearer process planning.
RFQ Strategy Should Match the Risk Level
Cost differences between precision and general machining are frequently misread because the RFQ is weak. Buyers sometimes compare a precision quote and a general quote without understanding why they differ. The visible difference may look like margin, but the real cause is often process burden.
Precision work usually demands tighter setup control, stronger fixturing logic, more careful inspection, more stable tooling practice, and more disciplined process management. That burden is justified when the part requires it. It is wasteful when the part does not.
This is why quote review matters. If a precision process is being requested, the buyer should be able to explain what feature relationships or operational risks justify it. If they cannot, the specification may be carrying cost without carrying value.
Supplier Selection Changes Once Precision Truly Matters
Once a part crosses from general to more demanding precision expectations, supplier evaluation should change. Buyers should care more about process stability, inspection discipline, fixture logic, communication clarity, and the supplier’s understanding of the part’s critical features.
This does not mean every supplier needs the same process depth. It means the buyer should stop evaluating only by machine count, broad capability claims, or a generic “we do precision work” statement. The real question is whether the supplier can protect the features that matter consistently.
This principle applies across industries. The part does not need to look complicated to carry expensive consequences. Many of the worst purchasing mistakes come from underestimating simple-looking parts whose functional relationships are actually strict.
Matching Machine Capability to Manufacturing Need
The same logic that governs outsourcing decisions applies to in-house capability planning. Investing in a machine category should follow from the parts you actually produce and the variation that hurts your workflow. If your production involves panel processing, edgebanding, or nesting work where repeatability and edge quality drive downstream assembly, the machine selection should reflect those requirements.
For teams comparing outsourcing choices with longer-term in-house capability planning, reviewing equipment in machine-category terms rather than only piece-price terms is useful. The Pandaxis shop provides a reference point for thinking through that logic. The same buying principle applies in both cases: invest where variation hurts, and avoid paying for complexity that the workflow does not need.
Choose the Level of Control the Part Can Actually Justify
Precision CNC machining and general machining are not opposing identities. They are different process responses to different levels of part consequence. Choose general machining when the part is forgiving and the broader process burden of precision would add cost without real benefit. Choose precision CNC machining when variation creates assembly risk, performance risk, or long-term business cost.
The difference matters most when the part has functional relationships that cannot tolerate casual variation. If buyers stay focused on that principle, the machining strategy becomes much easier to specify, quote, and source correctly. The best decision is not the one that sounds more advanced. It is the one that gives the part exactly the level of control its real job requires.